G050
User´s Guide
(
ø
26, S45C,
V
c
= 100 m/min,
f
= 0.1 mm/rev)
100 mm
User ’s
Gu ide-
Techn i ca l Reference
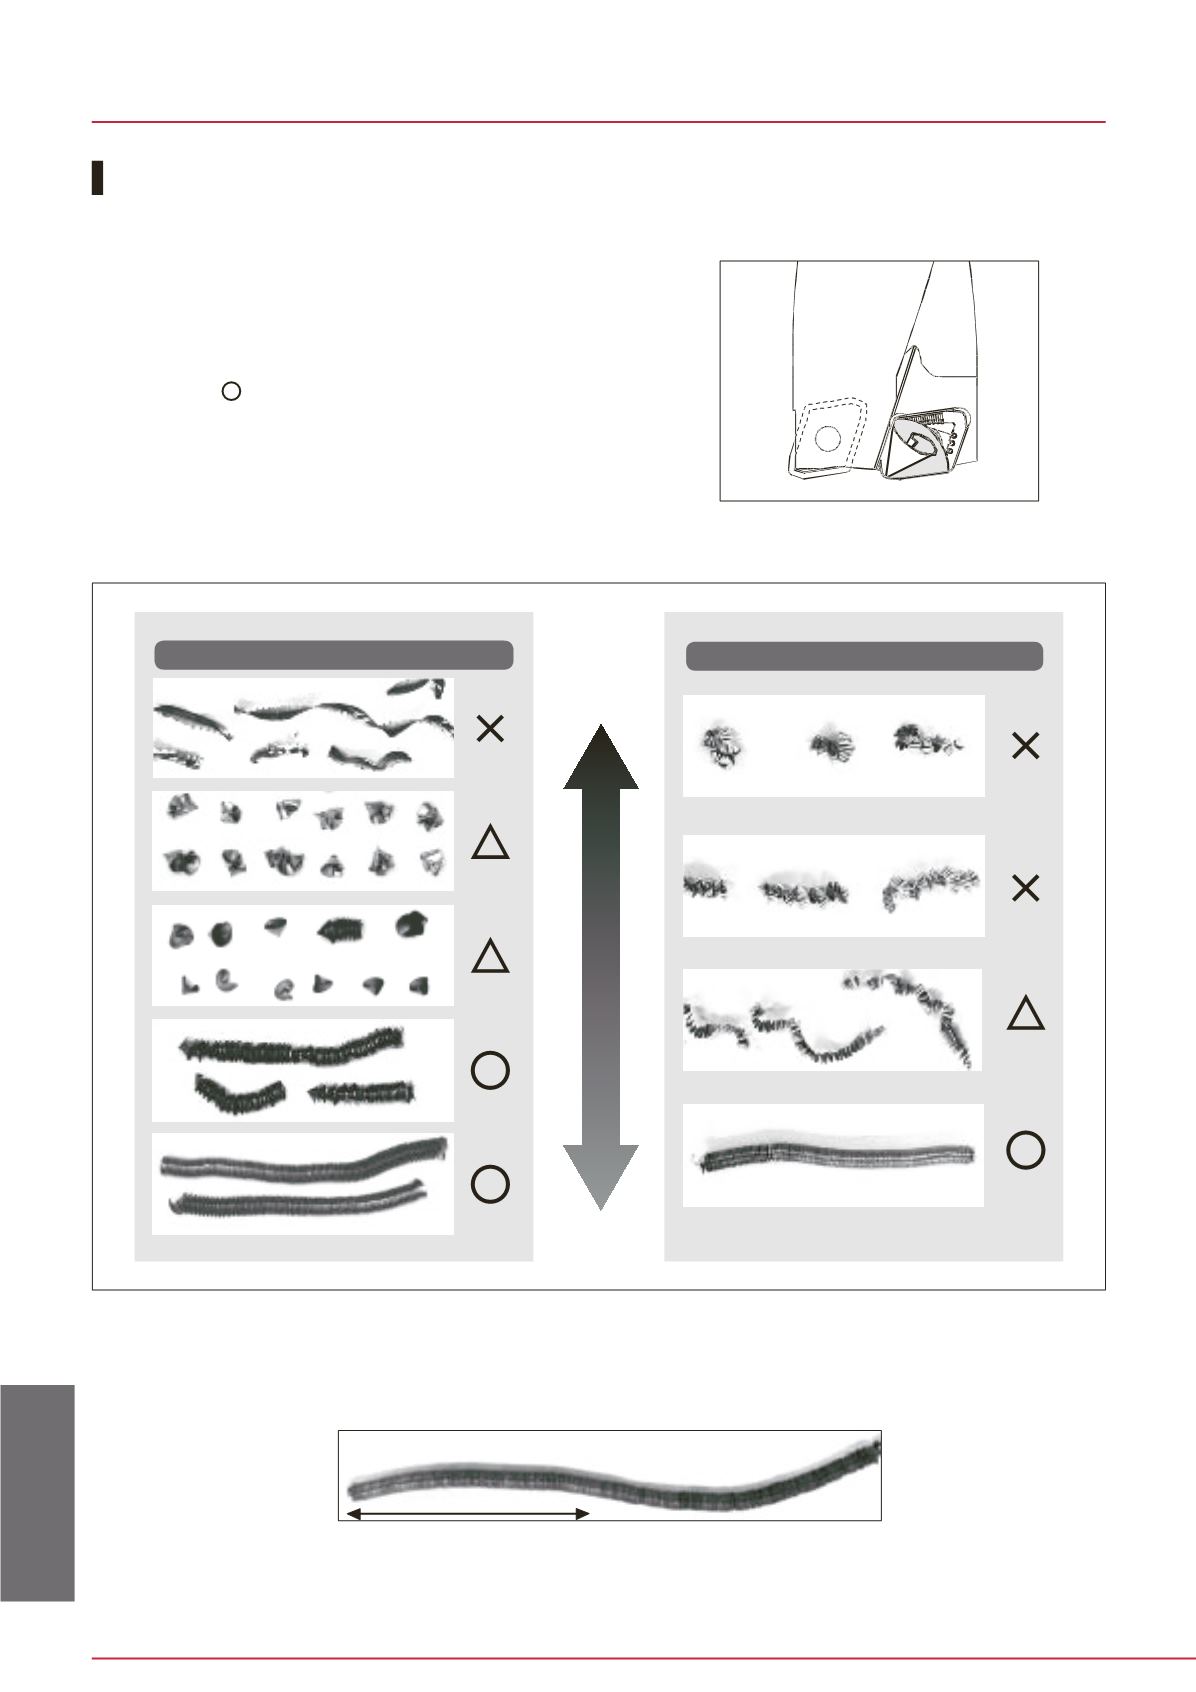
Chip shapes
Chip shape produced with central insert
• A conical coil shape whose apex point coincides with the rotating cen-
ter of the drill is the basic shape. The chips are broken into small sec-
tions with increases in feed. However, excessively high feed causes
the chip to increase in thickness and develops vibration which dis-
turbs stable machining.
• In TDX drills, marked chips shown below are the most preferable
shapes. This type of chip is broken into adequate lengths by centrifu-
gal forces when used in tool-rotating condition. On the other hand,
when used in work-rotating condition such as on a lathe, a continu-
ously long chip is often produced without entangling.
Relation between chip shapes and feeds
(In the case of central insert)
Example of chip shape in work-rotating applications
(In the case of central insert)
Dr i l l ing Tool s
Low carbon steels, stainless steels, etc.
Carbon steels, alloy steels, etc.
Higher
Feed
Lower


