G043
User´s Guide
Tungaloy
γ
α
1° ~ 3°
30° ~ 45°
0° ~ 3°
¡
™
£
¢
User ’s
Gu ide-
Techn i ca l Reference
A
B
C
Regrinding of end relief angle
Notice of regrinding
(1) If, after checking the damage of the cutting edge, the
damage is as case “A” or “B” of the flow chart, the tool
must be reground.
Too much damage of the cutting edge requires too much
stock removal and thus reduces tool life.
(2) Please use diamond grinding wheel.
(3) Peripheral relief angle must be ground between 18° and
10°.
Relief angle of small diameter cutters for aluminium
machining must be a large degree.
(4) First check if “C” in flow chart can be adapted for the case
of coated endmill or not.
If procedure “C” can be adapted for regrinding, tool life
after the grinding would be more improved than new one.
The reason is remaining coated layer of cutting edge and
shorter tool length will keep much higher rigidity of the tool
than before regrinding.
(5) Please check run out of peripheral cutting edge, face
cutting edge, with Vee block after regrinding.
The value of the run out must be controlled within 0.01
mm.
Notice for regrinding of ball nose endmill
- Regrinding of relief angle only is available. The dimension
of nose radius will be smaller after grinding.
- Honing of cutting edge is necessary after regrinding.
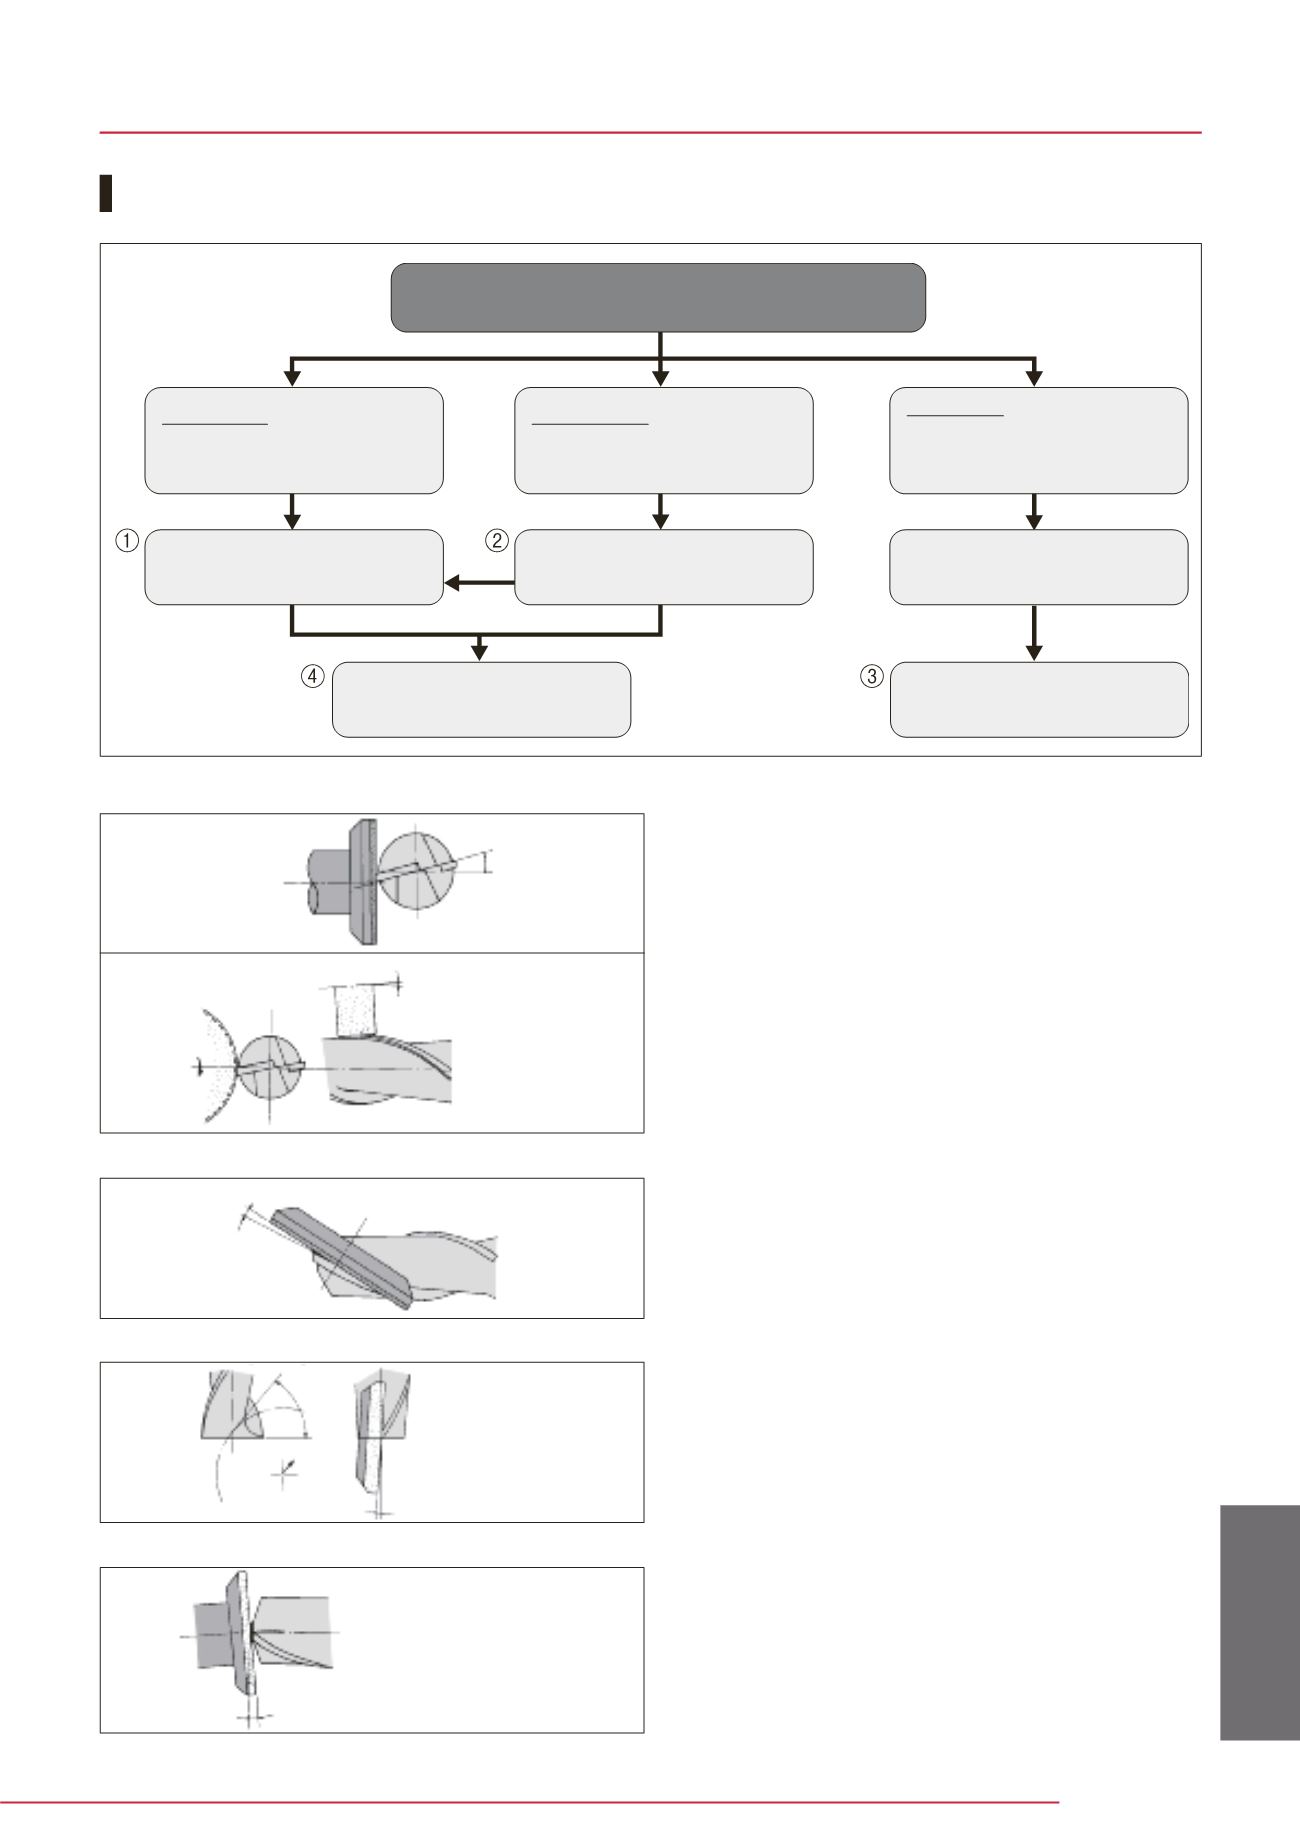
1. for using cup type
diamond wheel
Regrinding procedures of sol id carbide endmi l l
relief angle
Use 400 to 600 mesh
diamond wheel
2. for using straight
type diamond wheel
grinding
wheel
Setting angle of
grinding wheel
Formular of setting
angle
α
tan
α
= tan
β
x tan
θ
β
: peripheral relief angle
θ
: spiral angle
Regrinding of peripheral rake angle
Cup type diamond wheel
Regrinding of end rake angle (End gash)
For 2 flutes endmill:
straight type diamond
wheel
For
≥
3 flutes endmill:
cup type diamond wheel
Regrinding of end relief angle
Cup type diamond wheel
γ
: 1st end relief angle: 5° ~ 7°
2nd end relief angle: 15° ~ 20°
Flank wear
at the peripheral cutting
edge
Regrinding of peripheral
relief angle
Crater wear
at the rake face
Regrinding of peripheral
rake angle
Breakage
Checking, if the tool has
enough length of cutting
edge as unused part.
Cutting off damaged part
Regrinding of end relief
angle
Grinding of end rake angle
and end relief angle
Check damage on cutting edge
Sol id Carbide Endmi l ls


