G036
User´s Guide
V
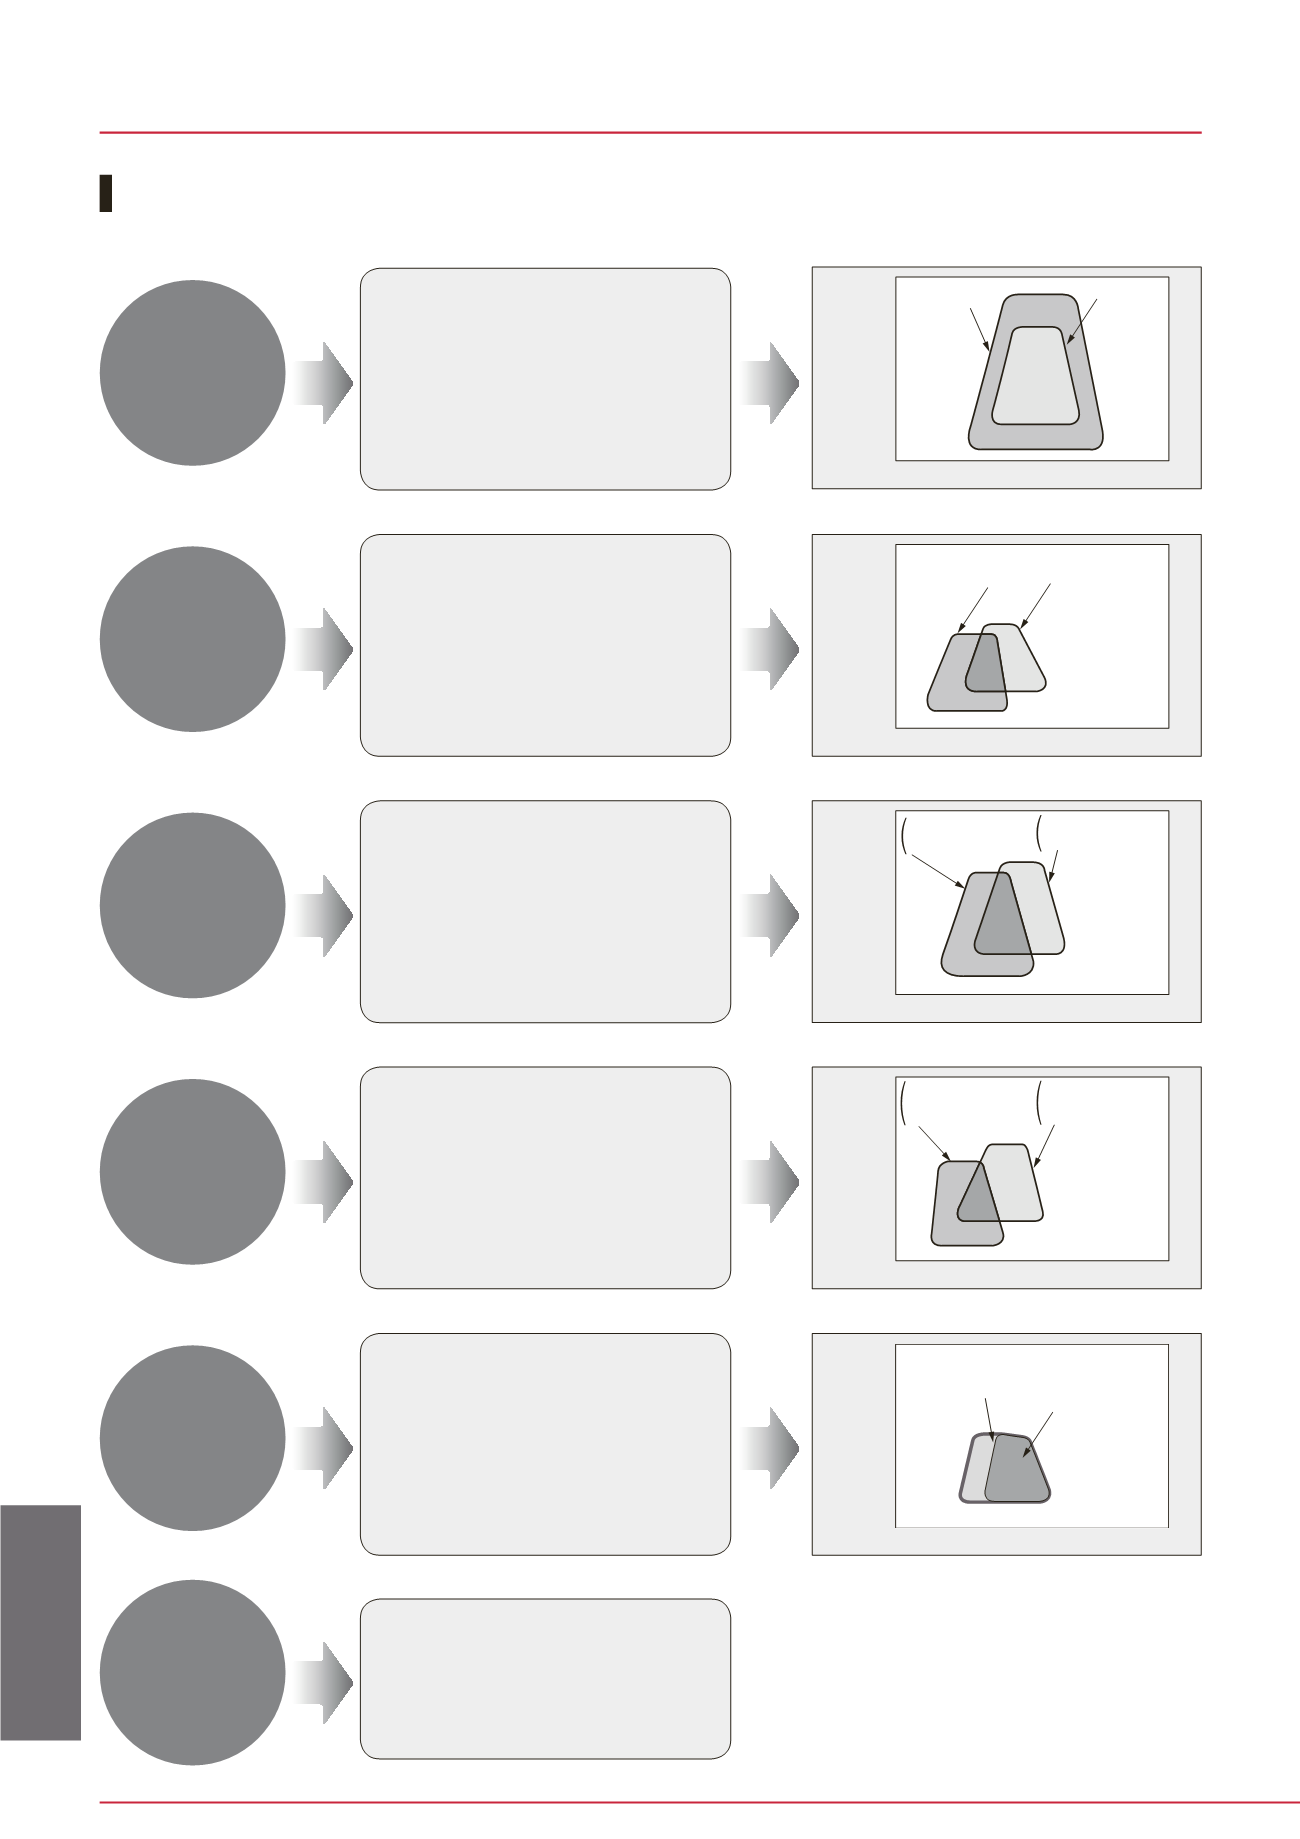
c = 200 m/min
V
c = 100 m/min
User ’s
Gu ide-
Techn i ca l Reference
• Of these, feed has the greatest effect
followed by depth of cut and cutting speed
in order listed.
• Feed is proportionate to the thickness of
chips.
• Depth of cut is proportionate to the width of
chips.
• There are optimum values (effective range) in
feed and depth of cut.
• Cutting speed is in inverse proportion to chip
thickness. Effective range becomes narrow
at high speed.
• These are related to thickness of chips
and ease of curling.
• Mild steel chips are thicker than those of
hard steel.
• Hard steel chips are liable to curl more
than those of mild steel.
• Chips that do not curl are thin. As an
exception, in case of mild steel even if
thick, may not curl.
• Side cutting edge angle is relative to chip
thickness and width
• Side cutting edge angle is preferably
small.
• Nose radius is relative to thickness and
width and the direction of flowing out.
• In finishing, small nose radius, whilst for
rough cutting, large nose radius is better.
• Effective range is wider with wet cutting.
• Especially at low feed range is liable to
curl.
• Rake angle is in inverse proportion to chip
thickness.
• Depending on the Workpiece material,
there is an optimum value.
• Chipbreaker width is selected
proportionately to feed.
• Narrow at low feed and wide at high feed.
• Chipbreaker depth is to be selected so as
to be inversely proportionate to feed.
• Deep at low feed and shallow at high feed.
• The machine has enough power and
mechanical strength.
• Select the machine consistent with the
size of Workpiece material to be used.
Factors af fect ing chip cont rol
(1) Cutting conditions
1 Feed
2 Depth of cut
3 Cutting speed
(2) Workpiece material
1 Alloy element
2 Hardness
3 Heat treatment
condition
(3) Tool geometry
1 Side cutting
edge angle
2 Nose radius
(4) Shape of chipbreaker
1 Rake angle
2 Chipbreaker width
3 Chipbreaker depth
(5) Coolant
(6) Machine
1 Rigidity
2 Power limit
Effective
range
Depth of cut:
a
p (mm)
Feed:
f
(mm/rev)
Depth of cut:
a
p (mm)
Feed:
f
(mm/rev)
Depth of cut:
a
p (mm)
Feed:
f
(mm/rev)
Depth of cut:
a
p (mm)
Feed:
f
(mm/rev)
Depth of cut:
a
p (mm)
Feed:
f
(mm/rev)
S.C.E.A: small
Nose radius: small
S.C.E.A: large
Nose radius: large
Rake angle: small
Breaker width: small
Breaker depth: large
Rake angle: large
Breaker width: large
Breaker depth: small
Wet cutting
Dry cutting
Mild steel
Hard steel
Chipbreakers


