G042
User´s Guide
ø
D
c
ø
D
c
ø
D
c
ø
D
c1
User ’s
Gu ide-
Techn i ca l Reference
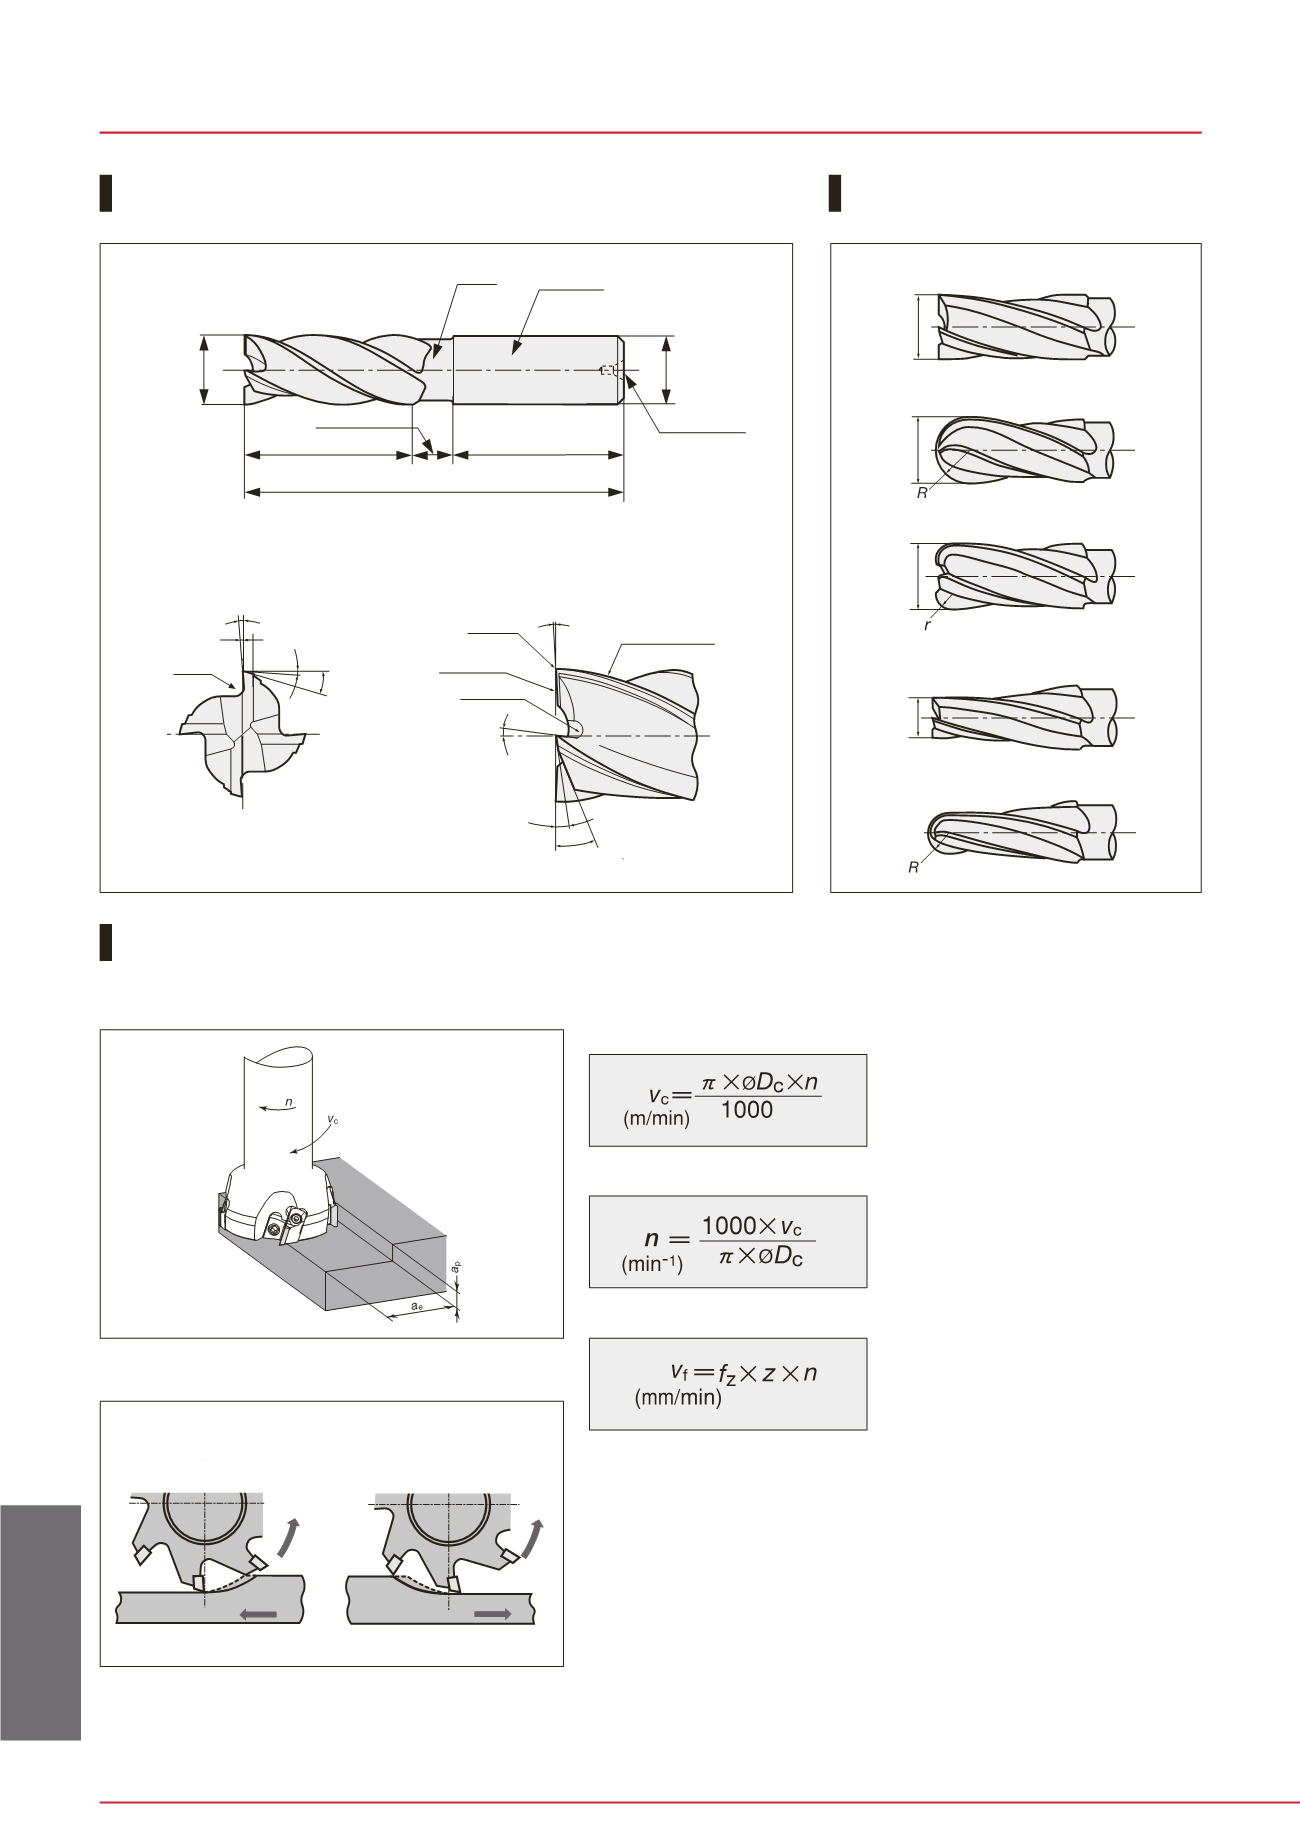
Square
Ball nose
Radius
Taper neck
Ball nose with taper neck
Par t detai l s
Types
Outside diameter
Shank diameter
Neck length
Shank length
Neck
Shank
Flute length
Radial rake
Centre hole
Overall length
1st radial relief
Concave angle
Flute
2nd radial relief
Axial rake
End
cutting edge
Corner
Peripheral
cutting edge
End gash
Land width
2nd end relief
1st end relief
Cut t ing condi t ion of Endmi l ls
Cutting
The necessary capacity of the machine is limited by the length
of cut edge of the endmill.
Up milling and down milling
Down milling generally produces better tool life and surface
roughness.
In case of cast iron sand inclusion or welding surface, up
milling is recommended.
Up milling
Down milling
Cutting speed
v
c
: Cutting speed (m/min)
ø
D
c
: Effective diameter (mm)
n
: Number of revolutions (min -
1
)
π
≈
3.14
Cutting speed
(Calculated from number of revolutions)
Number of revolution
(Calculated from cutting speed)
Feed speed and feed per tooth
v
f
: Feed speed (mm/min)
f
z
: Feed per tooth (mm/t)
z : No. of teeth of the endmills
n
: Number of revolutions (min -
1
)
Sol id Carbide Endmi l ls


