G040
User´s Guide
ø
D
c
10
30
50
100
125
150
200
300
500
800
1,000
2,000
4,000
10
318
955
1,592
3,184
3,980
4,777
6,369
9,554
15,923
25,477
31,847
63,694 127,388
12
265
796
1,326
2,653
3,317
3,980
5,307
7,961
13,269
21,231
26,539
53,078 106,157
16
199
597
995
1,990
2,488
2,985
3,980
5,971
9,952
15,923
19,904
39,808
79,617
20
159
477
796
1,592
1,990
2,388
3,184
4,777
7,961
12,738
15,923
31,847
63,694
25
127
382
636
1,273
1,592
1,910
2,547
3,821
6,369
10,191
12,738
25,477
50,955
30
106
318
530
1,061
1,326
1,592
2,123
3,184
5,307
8,492
10,615
21,231
42,462
32
99
298
497
995
1,244
1,492
1,990
2,985
4,976
7,961
9,952
19,904
39,808
35
90
272
454
909
1,137
1,364
1,819
2,729
4,549
7,279
9,099
18,198
36,396
40
79
238
398
796
995
1,194
1,592
2,388
3,980
6,369
7,961
15,923
31,847
50
63
191
318
636
796
955
1,273
1,910
3,184
5,095
6,369
12,738
25,477
63
50
151
252
505
631
758
1,011
1,516
2,527
4,044
5,055
10,110
20,220
80
39
119
199
398
497
597
796
1,194
1,990
3,184
3,980
7,961
15,923
100
31
95
159
318
398
477
636
955
1,592
2,547
3,184
6,369
12,738
125
25
76
127
254
318
382
509
764
1,273
2,038
2,547
5,095
10,191
160
19
59
99
199
248
298
398
597
995
1,592
1,990
3,980
7,961
200
15
47
79
159
199
238
318
477
796
1,273
1,592
3,184
6,369
250
12
38
63
127
159
191
254
382
636
1,019
1,273
2,547
5,095
315
10
30
50
101
126
151
202
303
505
808
1,011
2,022
4,044
fx
fy
v
f
f
z
SS400
520
2150
2000
1900
1750
1650
S55C
770
1970
1860
1800
1760
1620
SCM435
730
2450
2350
2200
1980
1710
SKT4
(HB352)
2030
2010
1810
1680
1590
SC450
520
2710
2530
2410
2240
2120
FC250
(HB200)
1660
1450
1320
1150
1030
Al
(Si)
200
660
580
522
460
410
500
1090
960
877
760
680
( mm )
THF4400
TGP4100
TGP4200
TSP4000
TGD4400
TSE4000
TGN4200
TRD6000
1800
1600
1400
1200
1000
800
600
400
200
-200
0
User ’s
Gu ide-
Techn i ca l Reference
MPa
0.1 (mm/t)
0.15 (mm/t)
0.2 (mm/t)
0.3 (mm/t)
0.4 (mm/t)
Tensile strength
Value of specific cutting force on feed per tooth
k
c
(N/mm
2
)
Workpiece material
(JIS)
Conversion from cutting speed to number of revolutions
(
unit
:
min
-1
)
P
c
: Net power requirement (kW)
k
c
: Specific cutting force (N/mm
2
)
[Refer to the Table below]
a
p
: Depth of cut (mm)
a
e
: Width of cut (mm)
v
f
: Feed speed (mm/min)
Because practical power requirements depend on the type of mill
(proportional to the true rake angle) and the motor efficiency of the
machine used, the result calculated from the above formula should be
considered as a rough guide.
Values of cutting force (
k
c
)
Note: In this table, the effects of centrifugal force on the rotating balance of the tool and the toolholder, flying risk of cutter parts, and limited value of toolholder
destruction are not considered. Therefore, when using the tool at high speeds, be sure to observe the specified condition range.
Ca l cul at ing power requi rement
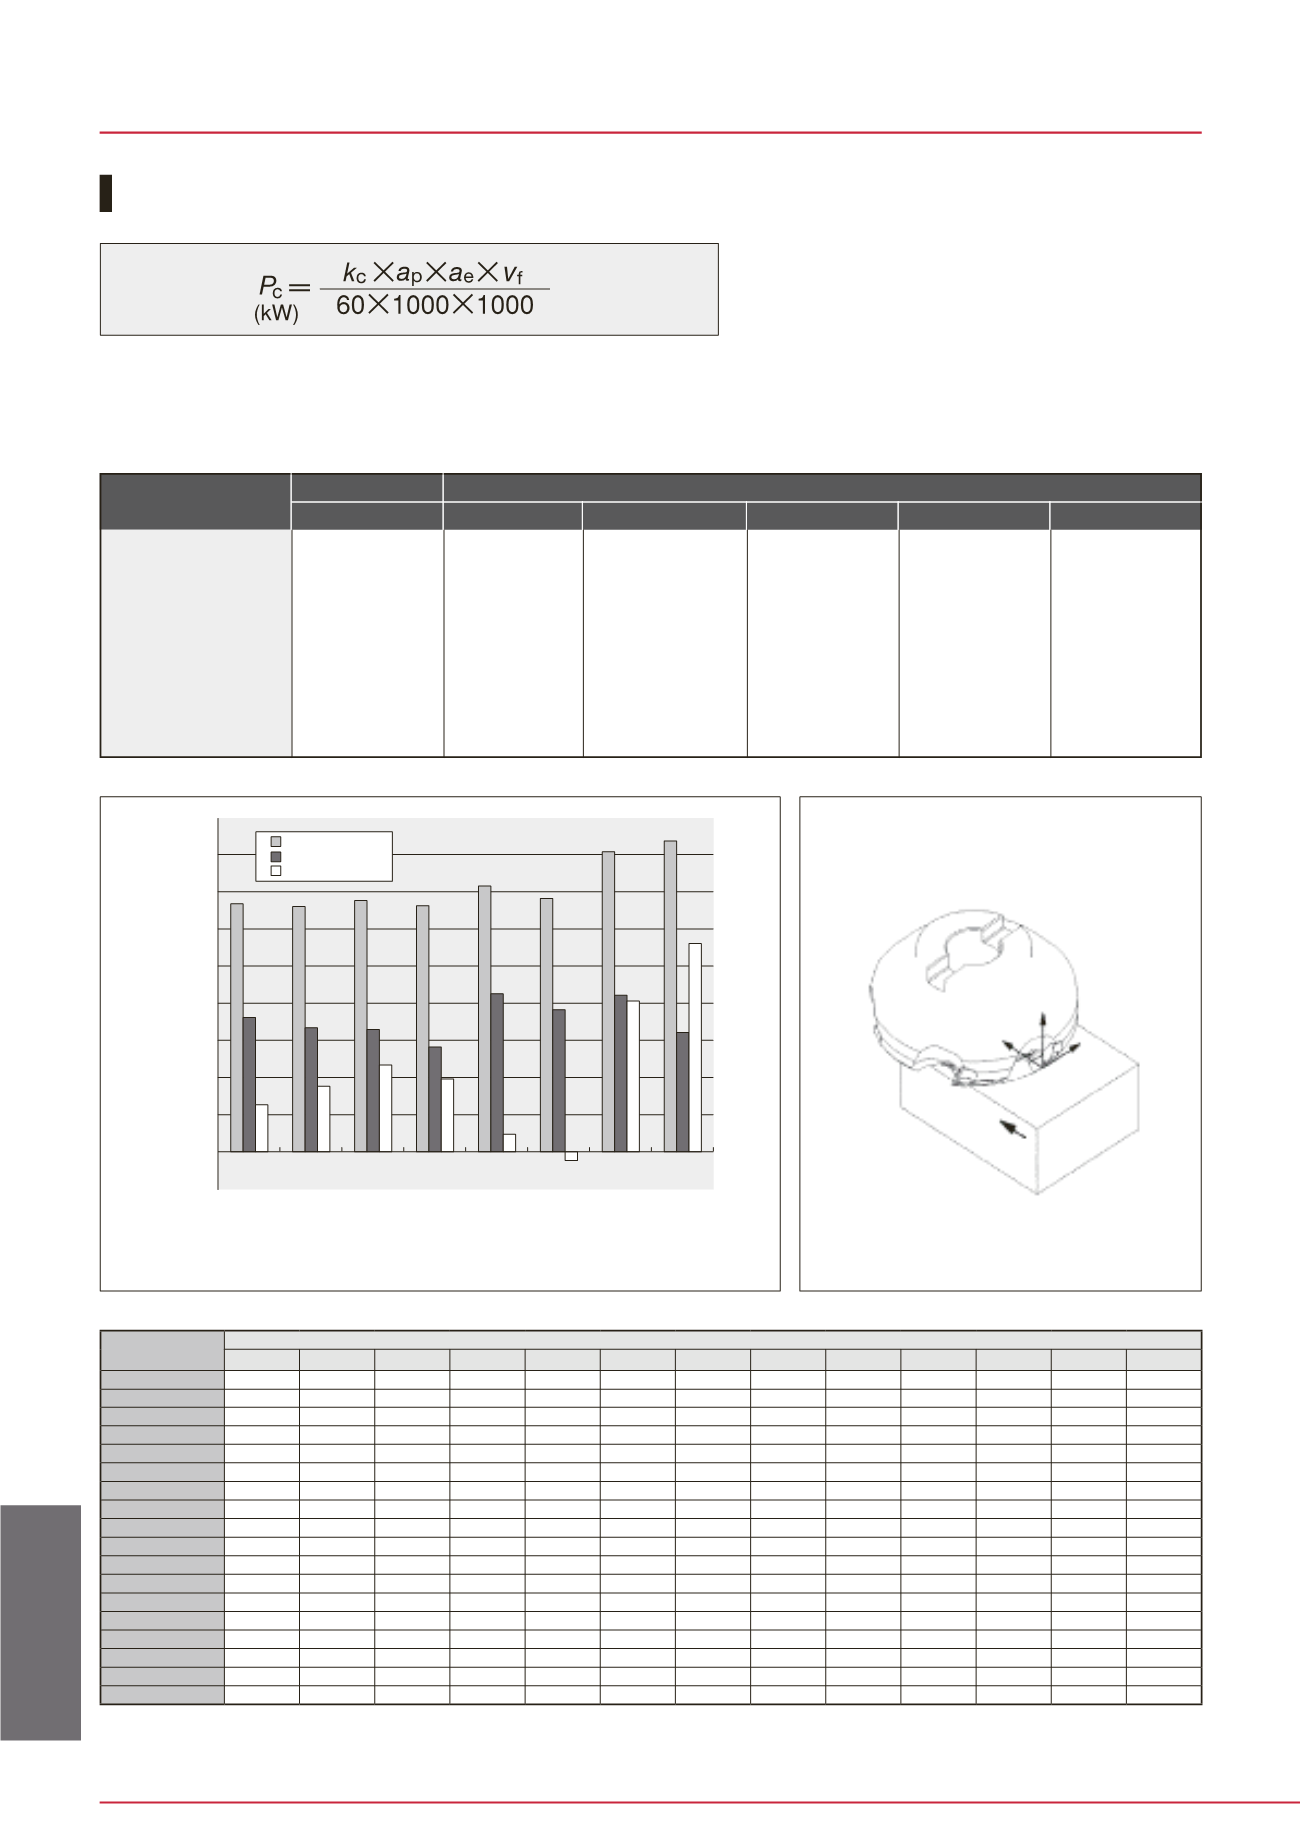
Principal force
Feed force
Back force
fy
fx
fz
Cutting force (N)
Workpiece material : S50C (210HB), Diameter of mill :
ø
160
mm
Cutting speed :
V
c
= 150
m/min
, Feed per tooth:
f
z = 0.20
mm/t
Depth of cut:
a
p
= 3
mm,
Cutting by a single edge, dry
Cutter diameter
Cutting speed (
v
c
) m/min
Brass
Mi l l ing Tool s
Values of specific cutting force (
k
c
)


