G032
User´s Guide
ø
D
s
c
(kW)
(
MPa
)
(
MPa
)
(
mm
)
(
mm
)
390
590
785
980
1765 ( 56HRC )
( 160HB )
( 200HB )
( 89HB )
100
170
230
300
56HRC
160
200
89
3430
4220
4900
5390
8390
2550
3330
1350
1050
390
1080
2840
3490
4020
4410
6870
1960
2550
1130
870
390
1080
2450
2940
3430
3780
5880
1630
2110
950
740
390
1080
2080
2500
2940
3240
5000
1340
1750
810
640
390
1080
1700
2080
2400
2650
4120
1030
1340
670
520
390
1080
User ’s
Gu ide-
Techn i ca l Reference
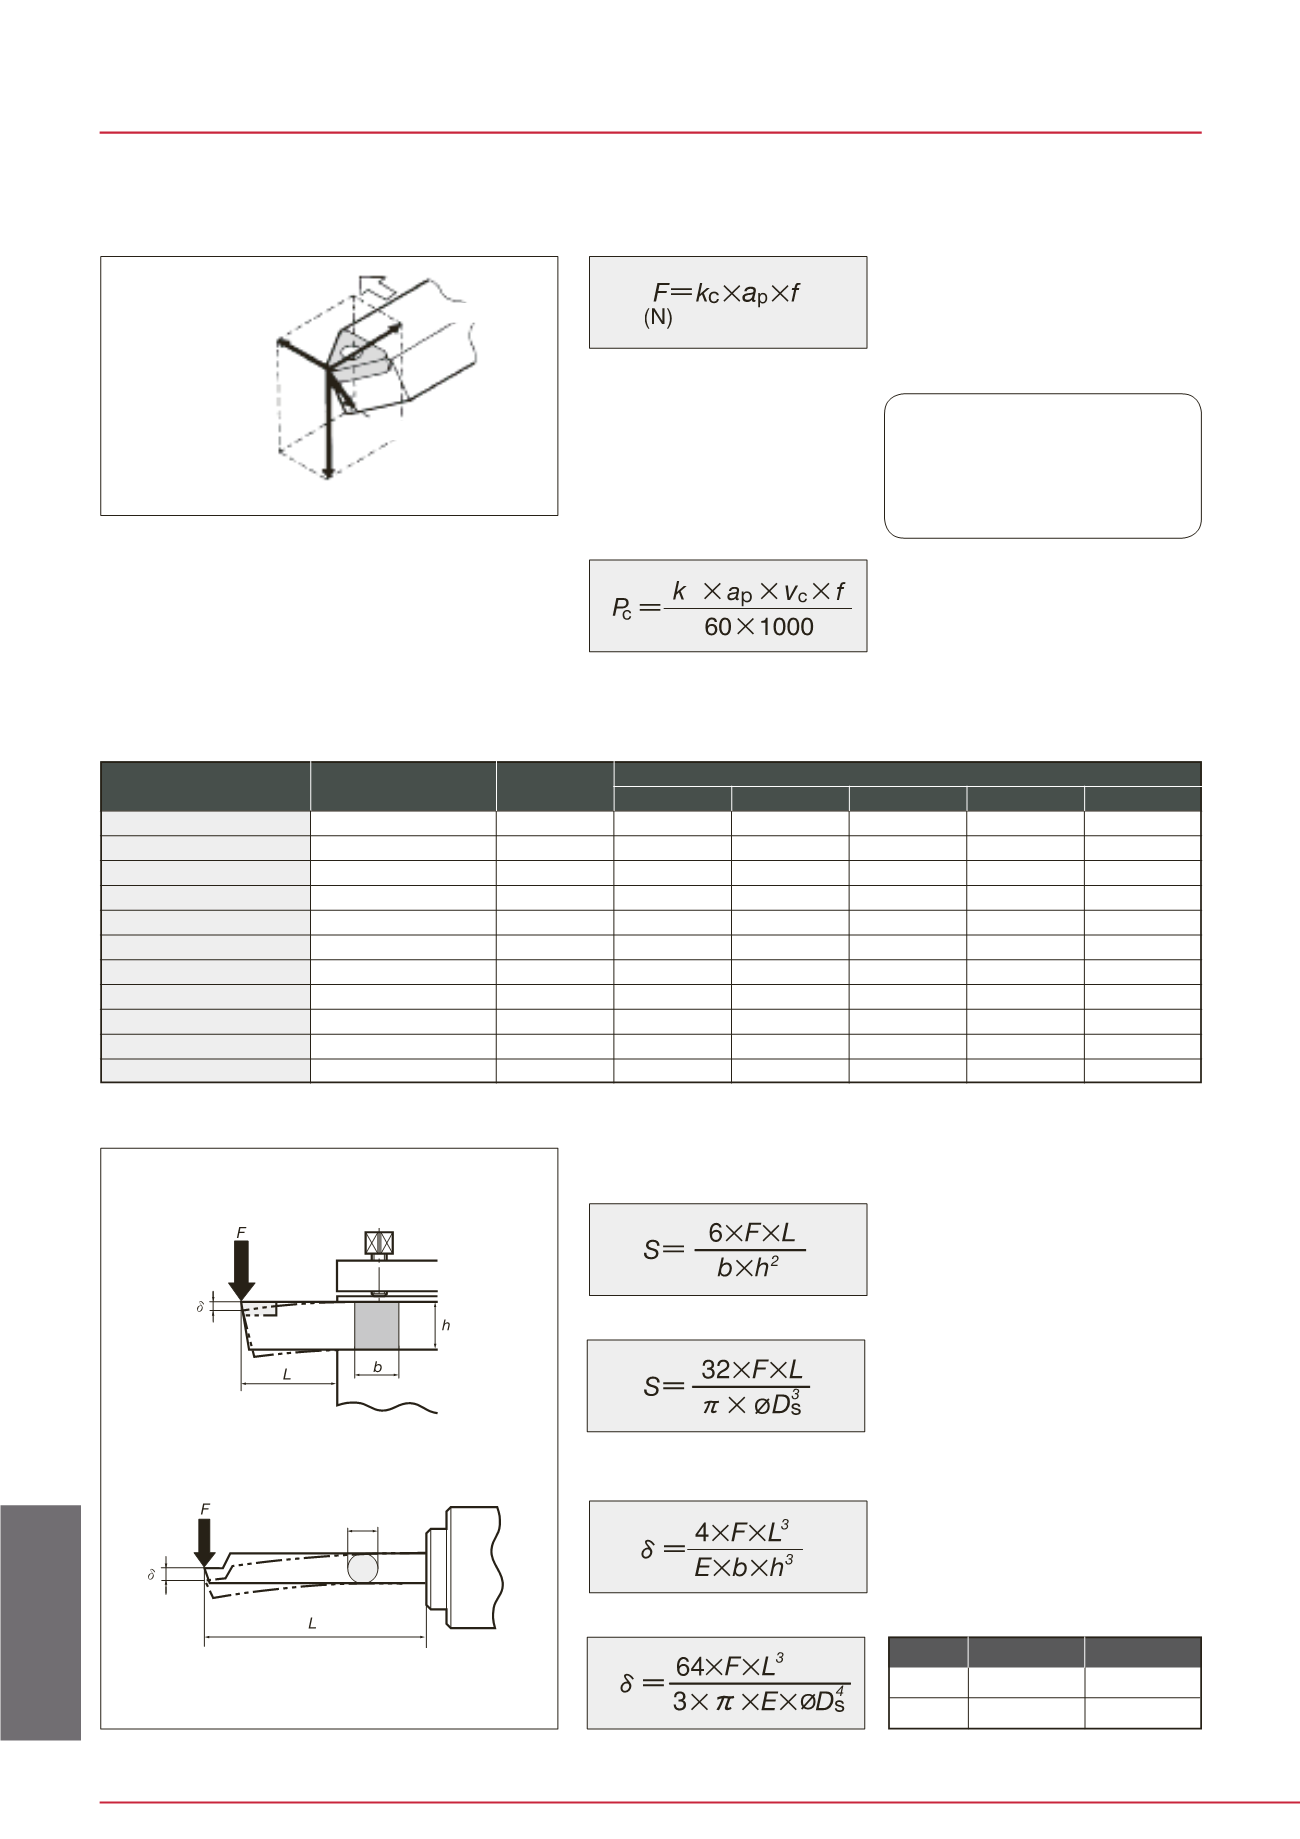
F
: Cutting force (N)
k
c
: Specific cutting force (N/mm
2
)
[Refer to the Table below]
a
p
: Depth of cut (mm)
f
: Feed (mm/rev)
Example :
Calculating the cutting force when
cutting a high carbon steel (ISO C55)
at
f
= 0.2 mm/rev and
a
p = 3 mm.
F
= 3430
3
0.2 = 2058N
Cutting forces
(1) Finding from the diagram based on experimental data.
(2) In case determining by simplified equation:
P
c
:
Net power requirement (kW)
k
c
: Specific cutting force (N/mm
2
)
[Refer to the Table below]
v
c
: Cutting speed (m/min)
a
p
: Depth of cutting (mm)
f
: Feed (mm/rev)
Calculating power requirement
Principal force
Cutting force in turning
Feed force
Bending stress and tool deflection
0.04
(mm/rev)
0.1
(mm/rev)
0.2
(mm/rev)
0.4
(mm/rev)
1.0
(mm/rev)
Tensile strength (MPa)
SS400, S15C
S35C, S40C
S50C, SCr430
SCM440, SNCM439
SDK
FC200
FCD600
Aluminium alloy
Aluminium
Magnesium alloy
Brass
Workpiece material
(JIS)
Hardness (HB)
Value of specific cutting force on feed
k
c
(N/mm
2
)
Bending stress
(1) Square shank
(2) Round shank
Tool defection (mm)
(1) Square shank
(2) Round shank
S
: Bending stress in shank (MPa)
F
: Cutting force (N)
L
: Overhang length of tool (mm)
b
: Shank width (mm)
h
: Shank height (mm)
ø
D
s
: Shank diameter (mm)
E
: Modulus of elasticity of shank
material (MPa)
Square shank
Round shank
(Ref.) Values of E
Material
MPa (N/mm
2
)
{kgf/mm
2
}
Steel
210,000
21,000
560,000~620,000 56,000~62,000
Cemented
Carbide
Resultant cutting force
Back force
Turning Tool s
Value of specific cutting force (
k
c
)


