G058
User´s Guide
User ’s
Gu ide-
Techn i ca l Reference
Trouble
Countermeasure
Possible cause
¡
Enlarge chamfer angle and
increase stock allowance
¡
Reduce cutting speed to prevent
peripheral wear of edge
¡
Increase lubricity of cutting fluid
¡
Improve filtering accuracy
¡
Change to fluid with higher lubricity
¡
Increase fluid pressure
¡
Repair electrical system
¡
Improve clamping method of workpiece
¡
Reduce fluid pressure
¡
Increase number of teeth
¡
Reduce chamfer angle
¡
Reduce back taper
¡
Improve run out accuracy
¡
Improve run out accuracy
¡
Remove residual damage completely
¡
Reduce fluid pressure
¡
Increase activity and lubricity of the fluid
¡
Correct spindle run out and
bushing clearance and alignment
¡
Improper clamping position
¡
Increase clamping force
¡
Correct bushing clearance
¡
Correct spindle run out and alignment
¡
Correct peripheral run out
¡
Increase reamer rigidity
¡
Change clamping position
¡
Reduce reamer guide width
(margin width)
¡
Increase chamfer angle
¡
Decrease cutting speed
¡
Increase lubricating capacity
¡
Increase regrinding stock amount
Increased burnishing torque
due to excessively small
stock allowance
Sticking
Mechanical trouble
Excessive feed rate per tooth
Improper tool specifications
Faulty regrinding
Improper cutting fluid
Faulty machine accuracy
Faulty clamping of workpiece
Faulty machine accuracy
Improper tool specifications
Unevenness in wall thickness of workpiece
Chamfer angle small
Excessive wear in
peripheral cutting edge
Faulty regrinding (residual damage)
Breaking of reamer
Faulty machining accuracy
¡
Chamfer angle small
¡
Excessive wear in peripheral
cutting edge.
¡
Faulty filtering of cutting fluid
¡
Incorrect selection of cutting fluid
¡
Insufficient cutting fluid pressure
¡
Excessive chamfer angle
¡
Excessive back taper
¡
Peripheral run out excessive
¡
Cutting edge run out is large
¡
Residual damage of preceding process
¡
Excessive fluid pressure
¡
Improper selection of cutting fluid
¡
Clamping position wrong
¡
Clamping force inadequate
¡
Excessive bushing clearance
¡
Faulty spindle run out and alignment
¡
Outer run out of reamer large
¡
Insufficient reamer rigidity
¡
Too high cutting speed
¡
Faulty lubricity of cutting fluid
Unacceptable
surface
roughness
Too large and
inconsistent
over size
Defective
out-of-roundness
Insufficient
oversize
allowance
Faulty clamping position of workpiece
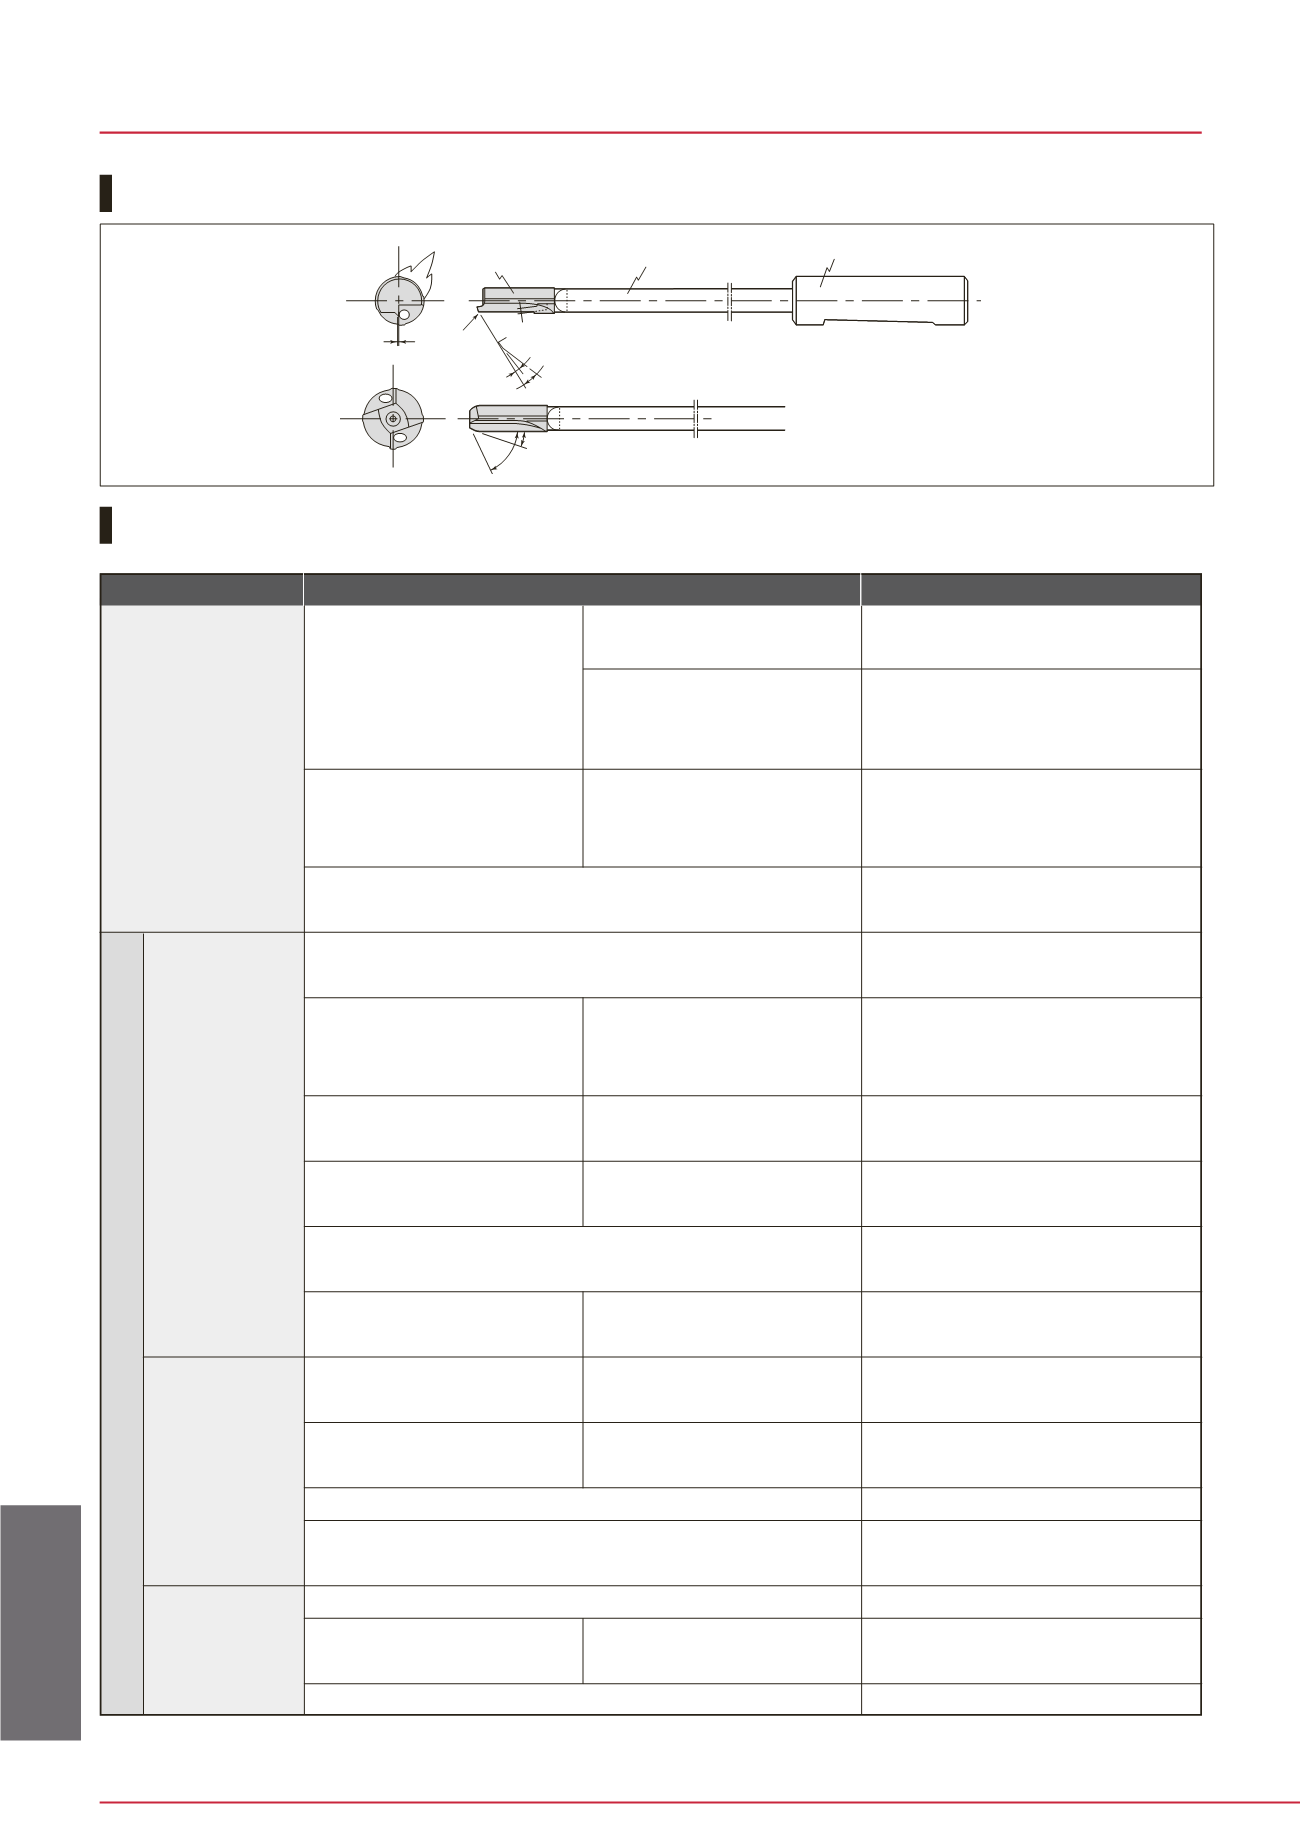
Nomenc l ature for gun reamer
Troubleshoot ing in gun reaming
Guide pad
Driver
Primary engage angle
Shank
Secondary engage angle
Secondary clearance angle
Oil hole
Primany
clearance angle
Corner
Tip
Margin
Dr i l l ing Tool s


