D211
Tungaloy
Profile Milling
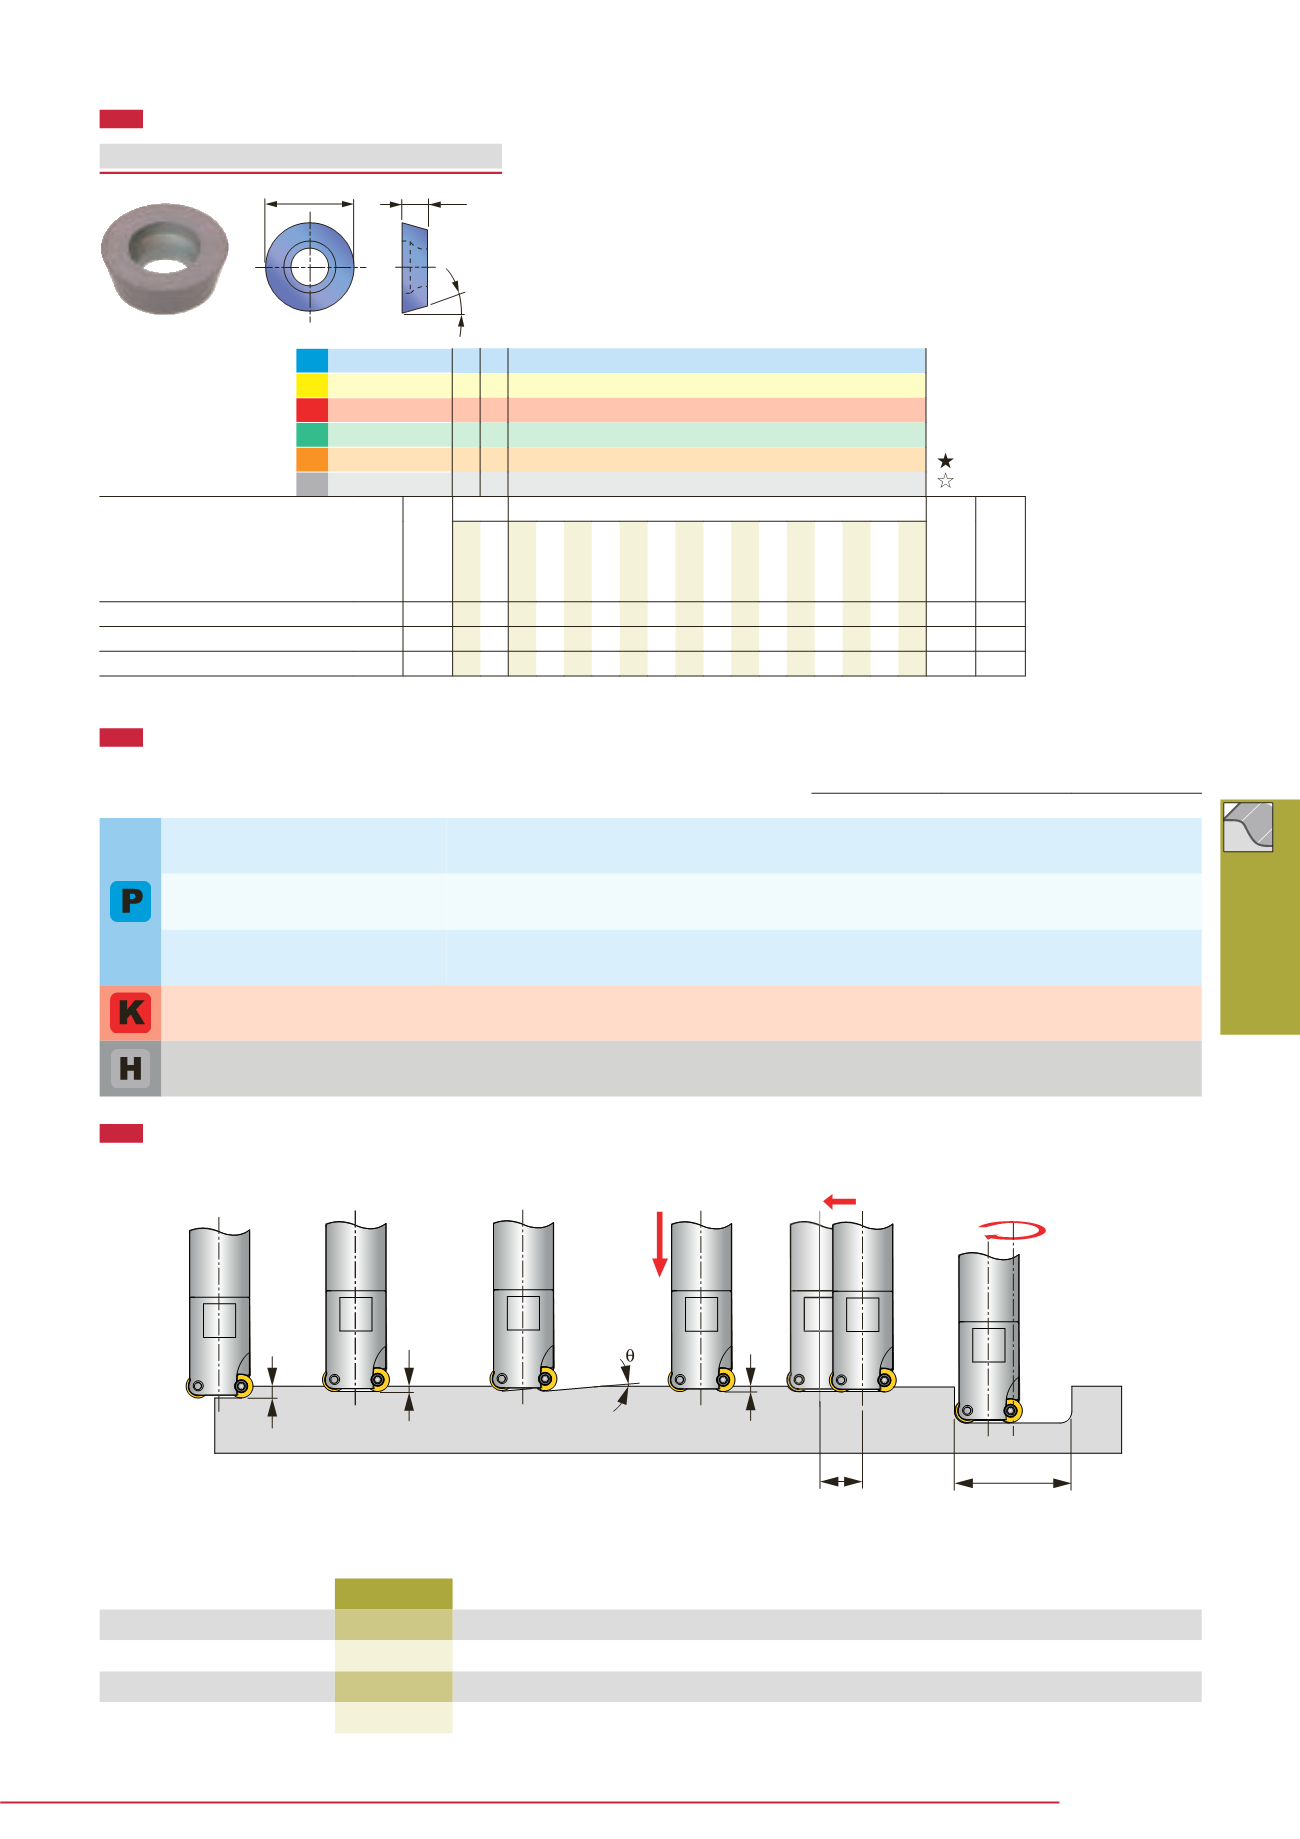
RDMW05/07/10
INSERT
A
T
15°
APPLICATION RANGE
Tool-ø
Max.
depth of cut
Max.
ramping
Max.
plunging
depth
Machining length
for removing
uncut portion
Max.
machining
*Max.
machining
Designation
øDc
ap
θ˚
A
L
øD
1
øD
2
HWD07R015MM08-03
15
3.5
25
2
ø
D
c - 6
23
28
HWD07R020MM10-04
20
3.5
11
2
ø
D
c - 6
33
38
HWD07R025MM12-05
25
3.5
7
2
ø
D
c - 6
43
48
HWD07R030MM16-05
30
3.5
5.5
2
ø
D
c - 6
53
58
STANDARD CUTTING CONDITIONS
ISO
Workpiece material
Grade Cutting speed
Vc (m/min)
Feed per tooth
fz (mm/t)
Depth of cut ap (mm)
Cutter dia. ø10, 12 Cutter dia. ø15, 20 Cutter dia. ø25
Carbon steels
C45, etc.
< 300 HB
AH120
200 ~ 500
0.15 ~ 0.45
~ 0.5
~ 0.7
~ 1
Alloy steels
42CrMo4 etc.
< 300 HB
AH120
120 ~ 350
0.15 ~ 0.35
~ 0.5
~ 0.7
~ 1
Die steels
X40CrMoV5-1 etc.
< 300 HB
AH120
100 ~ 300
0.1 ~ 0.3
~ 0.5
~ 0.7
~ 1
Cast irons
250, etc.
AH120
200 ~ 500
0.2 ~ 0.5
~ 0.5
~ 0.7
~ 1
Hardened steels,
Prehardened steels < 40HRC
AH120
70 ~ 200
0.1 ~ 0.25
~ 0.5
~ 0.7
~ 1
P Steel
M Stainless
K Cast iron
N Non-ferrous
S Superalloys
H Hard materials
Designation
Max.
a
p
Coating
A T
AH120
RDMW0501M0
2.5
l
5 1.4
RDMW0702M0
3.5
l
7 2.38
RDMW1003M0
5.0
l
10 3.18
: First choice
: Second choice
A
ø
D
1,2
L
a
p
a
p
l
: Line-up
*For flat bottom hole
Slotting
Plunging
Ramping
Shoulder
milling
Helical
interpolation
Traversing


