D221
Tungaloy
Profile Milling
ISO Workpiece material
Grade
Cutting speed Vc (m/min)
Feed per tooth fz (mm/t)
Carbon steels, Alloy steels
AH120
100 ~ 200
0.1 ~ 0.3
T3130
150 ~ 250
0.1 ~ 0.25
Die steels
< 300 HB
AH120
100 ~ 200
0.1 ~ 0.3
T3130
150 ~ 250
0.1 ~ 0.25
Prehardened steels < 45 HRC
AH120
60 ~ 120
0.1 ~ 0.2
Cast irons
AH120
100 ~ 200
0.1 ~ 0.3
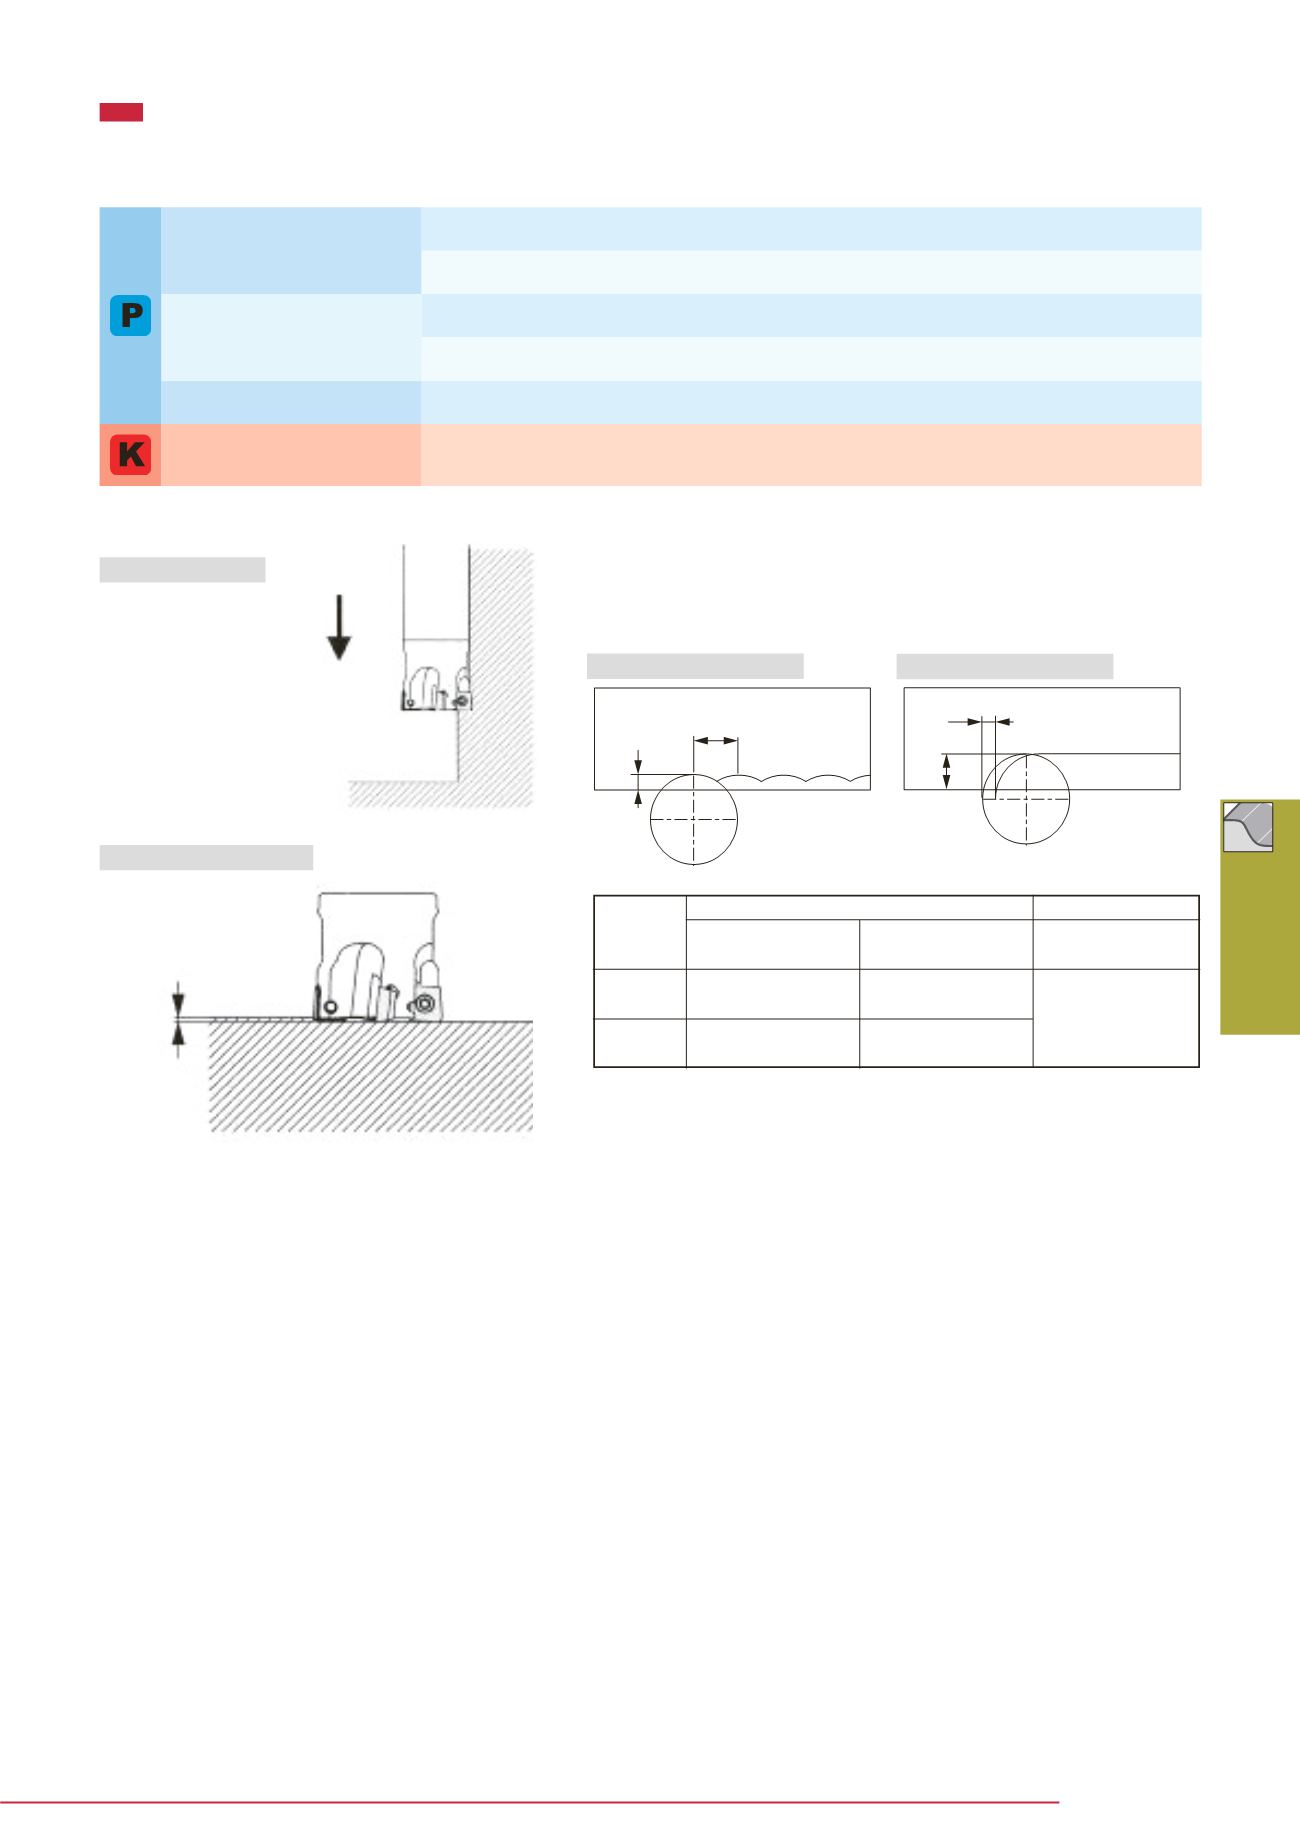
STANDARD CUTTING CONDITIONS
Z-feed milling
p
f
p
f
a
e
a
e
f
f
a
e
a
e
a
p
(1)
(2)
~ 0.5
Traverse feed milling
Machining method (1)
Machining method (2)
Note: In Z-feed milling, select either of the machining method (1) or (2) and
decide the depth of cut according to the application.
Pick feed
p
f (mm)
Tool dia. øD/2
Within effective
cutting edge length
Machining
method
Z-feed milling
Traverse feed milling
Radial depth of cut
a
e (mm)
Within effective
cutting edge length
Tool dia. øD/2
Depth of cut
a
p (mm)


