D217
Tungaloy
Profile Milling
STANDARD CUTTING CONDITIONS
ISO Workpiece material
Grade
Machining
type
Cutting speed
Vc (m/min)
Table feed vf (mm/min)
Tool dia. ø20 Tool dia. ø25 Tool dia. ø30
Carbon steels
C55, etc.
< 300 HB
AH120
(1)
200 (170 ~ 230)
760 (610 ~ 910)
610 (460 ~ 760)
510 (360 ~ 660)
AH120
(2)
230 (200 ~ 260)
1100 (900 ~ 1300)
880 (680 ~ 1080)
730 (530 ~ 930)
AH120
(3)
180 (150 ~ 200)
570 (420 ~ 350)
460 (310 ~ 610)
380 (230 ~ 530)
Alloy steels
42CrMo4, etc.
< 300 HB
AH120
(1)
180 (150 ~ 210)
680 (530 ~ 830)
550 (400 ~ 700)
450 (300 ~ 600)
AH120
(2)
210 (180 ~ 240)
1000 (800 ~ 1200)
800 (600 ~ 400)
670 (470 ~ 870)
AH120
(3)
160 (130 ~ 180)
510 (360 ~ 660)
400 (250 ~ 550)
340 (190 ~ 490)
Die steels
X96CrMoV12, etc.
< 300 HB
AH330
(1)
150 (120 ~ 180)
570 (420 ~ 720)
460 (310 ~ 610)
380 (230 ~ 530)
AH330
(2)
180 (150 ~ 210)
860 (660 ~ 1060)
690 (490 ~ 890)
570 (370 ~ 770)
AH330
(3)
130 (100 ~ 150)
410 (260 ~ 560)
330 (180 ~ 480)
280 (130 ~ 430)
Cast irons
250, etc.
AH120
(1)
200 (170 ~ 230)
950 (800 ~ 1100)
760 (610 ~ 910)
640 (490 ~ 790)
AH120
(2)
230 (200 ~ 260)
1200 (900 ~ 1400)
1000 (700 ~ 1200)
830 (530 ~ 1030)
AH120
(3)
180 (150 ~ 200)
570 (420 ~ 720)
460 (310 ~ 610)
380 (230 ~ 530)
Hardened steels
Prehardened steels
< 45 HRC
AH120
(1)
80 (60 ~ 100)
250 (150 ~ 350)
200 (100 ~ 300)
160 (100 ~ 260)
AH120
(2)
100 (70 ~ 130)
310 (160 ~ 460)
250 (100 ~ 400)
210 (100 ~ 360)
AH120
(3)
60 (40 ~ 80)
190 (140 ~ 240)
150 (100 ~ 200)
130 (80 ~ 180)
ISO
Workpiece material
Grade
Machining
type
Cutting speed
Vc (m/min)
Table feed vf (mm/min)
Tool dia. ø40
Tool dia. ø50
Carbon steels
C55, etc.
< 300 HB
AH120
(1)
180 (150 ~ 210)
490 (400 ~ 570)
390 (330 ~ 460)
AH120
(2)
200 (170 ~ 230)
480 (410 ~ 550)
380 (330 ~ 440)
AH120
(3)
160 (130 ~ 190)
260 (210 ~ 300)
200 (160 ~ 240)
Alloy steels
42CrMo4, etc.
< 300 HB
AH120
(1)
160 (130 ~ 190)
430 (350 ~ 510)
350 (280 ~ 410)
AH120
(2)
180 (150 ~ 210)
430 (360 ~ 500)
340 (290 ~ 400)
AH120
(3)
140 (110 ~ 170)
220 (180 ~ 270)
180 (140 ~ 220)
Die steels
X96CrMoV12, etc.
< 300 HB
AH120
(1)
140 (110 ~ 170)
380 (300 ~ 460)
300 (240 ~ 370)
AH120
(2)
160 (130 ~ 190)
380 (310 ~ 460)
310 (250 ~ 360)
AH120
(3)
120 (90 ~ 150)
190 (140 ~ 240)
150 (120 ~ 190)
Cast irons
250, etc.
AH120
(1)
200 (170 ~ 230)
640 (510 ~ 680)
510 (410 ~ 540)
AH120
(2)
220 (190 ~ 250)
600 (510 ~ 680)
480 (410 ~ 540)
AH120
(3)
180 (150 ~ 210)
340 (290 ~ 400)
280 (230 ~ 320)
Hardened steels
Prehardened steels
< 45 HRC
AH120
(1)
90 (70 ~ 110)
210 (160 ~ 260)
170 (130 ~ 210)
AH120
(2)
100 (80 ~ 120)
200 (160 ~ 250)
160 (130 ~ 200)
AH120
(3)
60 (50 ~ 90)
100 (80 ~ 140)
80 (60 ~ 120)
Notes:
• Cutting speeds shown in the left table are of the most outer diameter of the tool.
• The values of the cutting speeds and feeds shown in the table are of under general cutting conditions. The values should be modified depending on the power
and rigidity of the machine to be used, and work holding conditions.
• When using the long shank type, the depth of cut, pick feed, cutting speed, and table feed should be reduced to 70 %-90 % of the values shown in the tables.
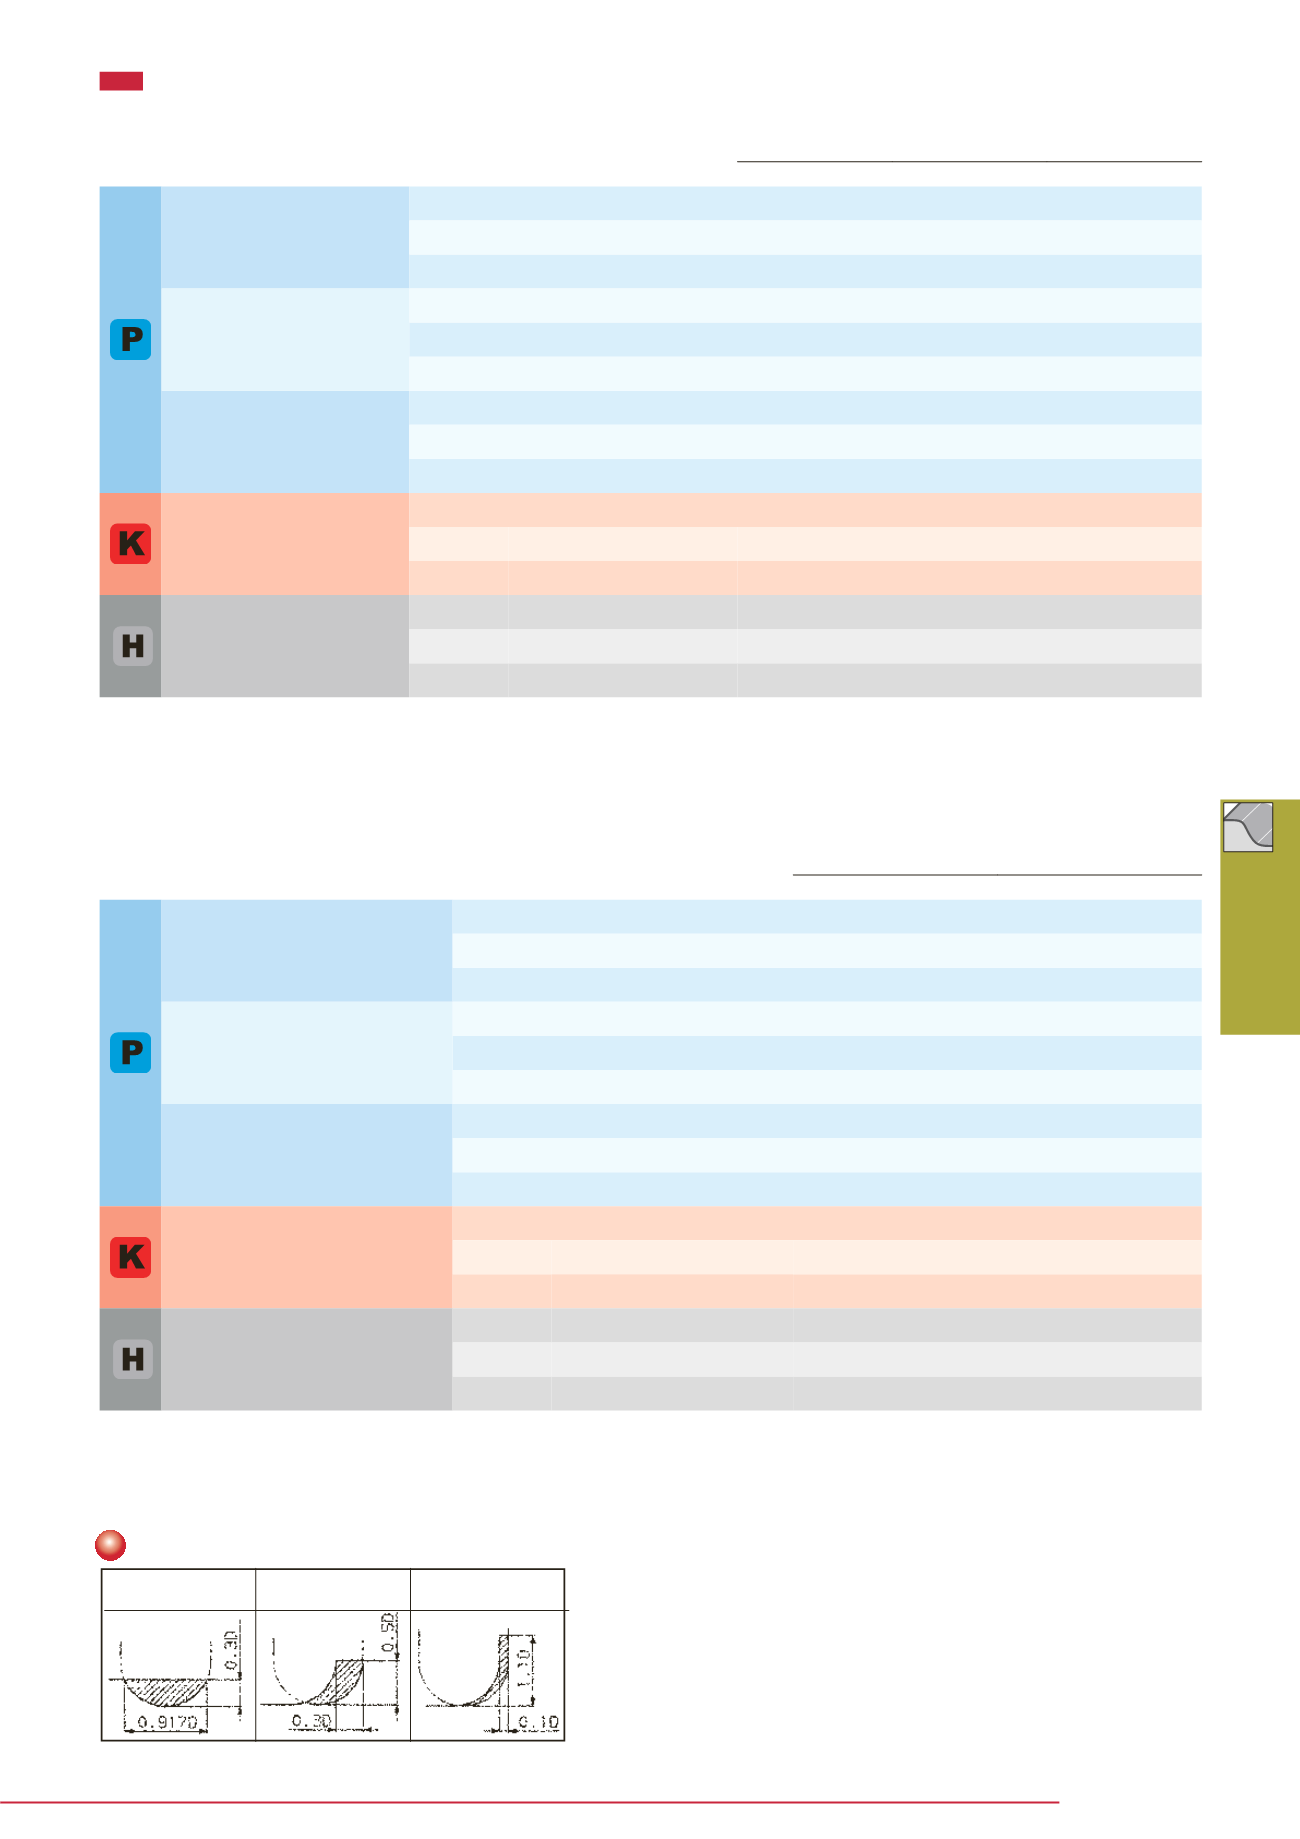
Machining types
EBP
EBD
Notes:
• Cutting speeds shown in the left table are of the most outer diameter of the tool.
• The values of the cutting speeds and feeds shown in the table are of under general cutting conditions. The values should be modified depending on the power
and rigidity of the machine to be used, and work holding conditions.
• When using the long shank type, the depth of cut, pick feed, cutting speed, and table feed should be reduced to 70 %-90 % of the values shown in the tables.
(1) Grooving
(3) Shouldering at
deep depth of cut
(2) Shouldering at
shallow depth of cut


