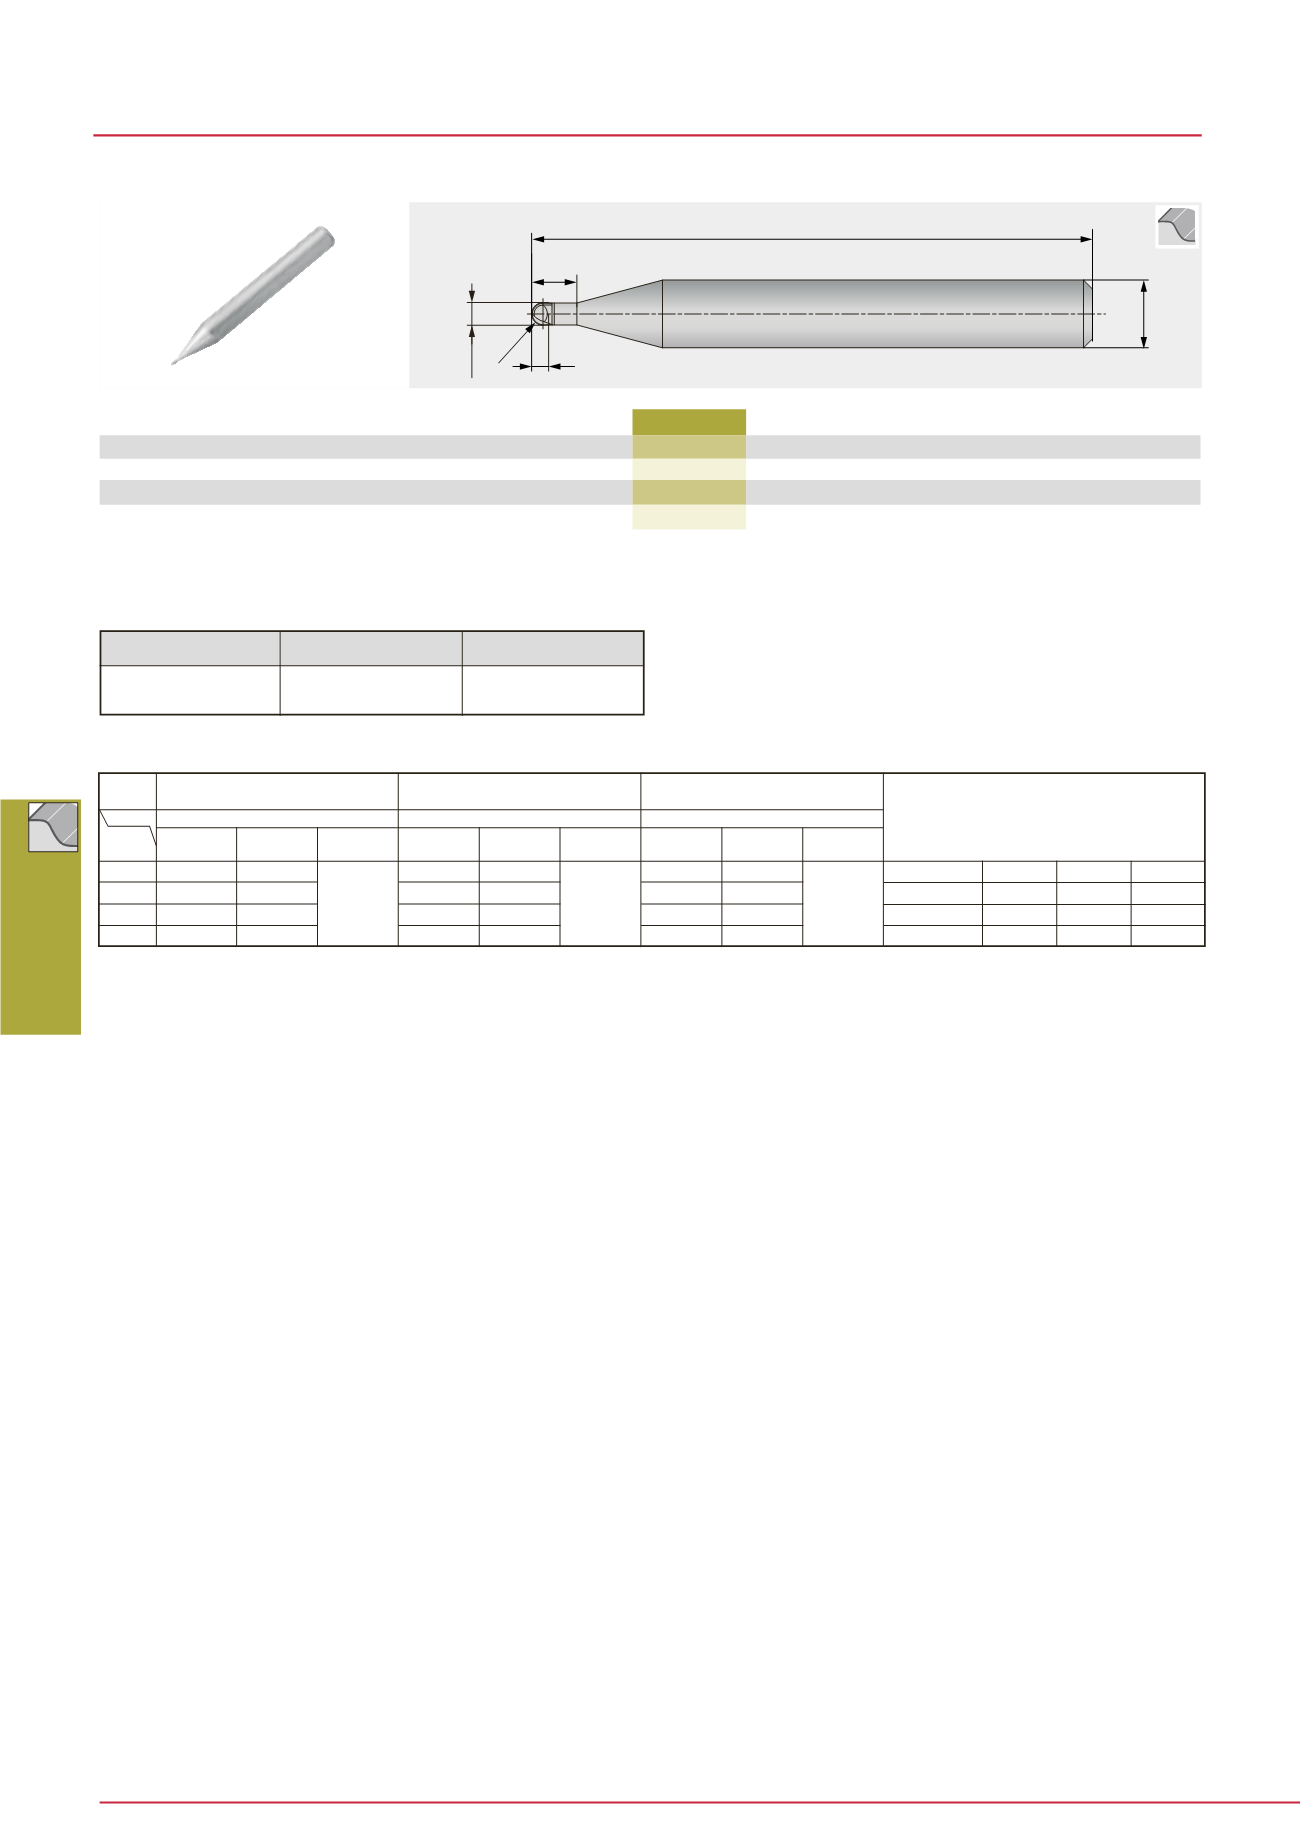
D218
Profile Milling
L
R
øDc
L
3
øDs
R
0.3 ~ 1.0
±0.005
h6
0.3
0.4
0.5
1.0
0.02×0.03
0.03×0.05
0.05×0.05
0.10×0.10
2,000
2,000
3,000
5,000
50,000
0.01×0.02
0.02×0.03
0.03×0.05
0.05×0.05
2,000
2,000
3,000
5,000
50,000
0.01×0.02
0.01×0.03
0.02×0.03
0.03×0.05
1,500
1,500
2,000
3,000
50,000
0°30
́
/1.25
0°30
́
/1.65
0°30
́
/2.05
0°30
́
/4.15
1°/1.30
1°/1.70
1°/2.10
1°/4.25
2°/1.35
2°/1.80
2°/2.25
2°/4.50
3°/1.45
3°/1.90
3°/2.40
3°/4.80
BBB2000
T-CBN ball endmills
Tolerance
(BBB2000)
Mill dia.
Tolerance on dia. Tolerance on shank
~ 52 HRC
~ 62 HRC
~ 70 HRC
Inclined angle of workpiece (
θ
1)/
Effective neck length (Z)
Notes:
• Depths of cut (
a
p) shown in the table are the allowable maximum values.
• Mist cooling or air blow is recommended.
• The maximum number of revolutions of the machine to be used is lower than 50,000 min
-1
,
the revolutions and feed rate should be modified at same rate.
• Use smallest possible overhang.
BBB2000 (T-CBN Ball Endmills)
Prehardened steels (NAK80, etc.)
Die steels (JIS SKD61, etc.)
Depth of cut
a
p ~
p
f (mm)
Feed rate
(mm/min)
No. of
revolutions
n
(min -1 )
Die steels
(JIS SKD11, DRM1 & 2, etc.)
Ball
radius
(R)
Depth of cut
a
p ~
p
f (mm)
Feed rate
(mm/min)
No. of
revolutions
n
(min -1 )
Depth of cut
a
p ~
p
f (mm)
Feed rate
(mm/min)
No. of
revolutions
n
(min -1 )
Workpiece
material
Hardness
High speed steel and die steel
(JIS SKH, DRM3, etc.)
Designation
BX850
z
R
øD
c
ℓ
L
3
L
øD
s
BBB2006
l
2
0.3
0.6
0.5
1.2
50
6
BBB2008
l
2
0.4
0.8
0.6
1.6
50
6
BBB2010
l
2
0.5
1
0.7
2
50
6
BBB2020
l
2
1
2
1.5
4
50
6
l
: Line-up


