D223
Tungaloy
Profile Milling
ISO Workpiece material
Grade
Cutting speed Vc (m/min)
Feed per tooth fz (mm/t)
Carbon steels, Alloy steels
< 300 HB
NS740
300 (150 ~ 400)
0.15 (0.05 ~ 0.2)
AH740
250 (150 ~ 350)
0.15 (0.05 ~ 0.2)
Cast irons 250, etc.
AH740
300 (200 ~ 500)
0.15 (0.05 ~ 0.2)
Ductile cast irons
600-3, etc.
AH740
250 (150 ~ 350)
0.15 (0.05 ~ 0.2)
Prehardened steels, Hard materials
40-55 HRC
AH740
150 (100 ~ 200)
0.1 (0.05 ~ 0.15)
a
p
p
f
a
e
0.5 ~ 1
~ 0.5
~ 0.5
Cautionary points in use
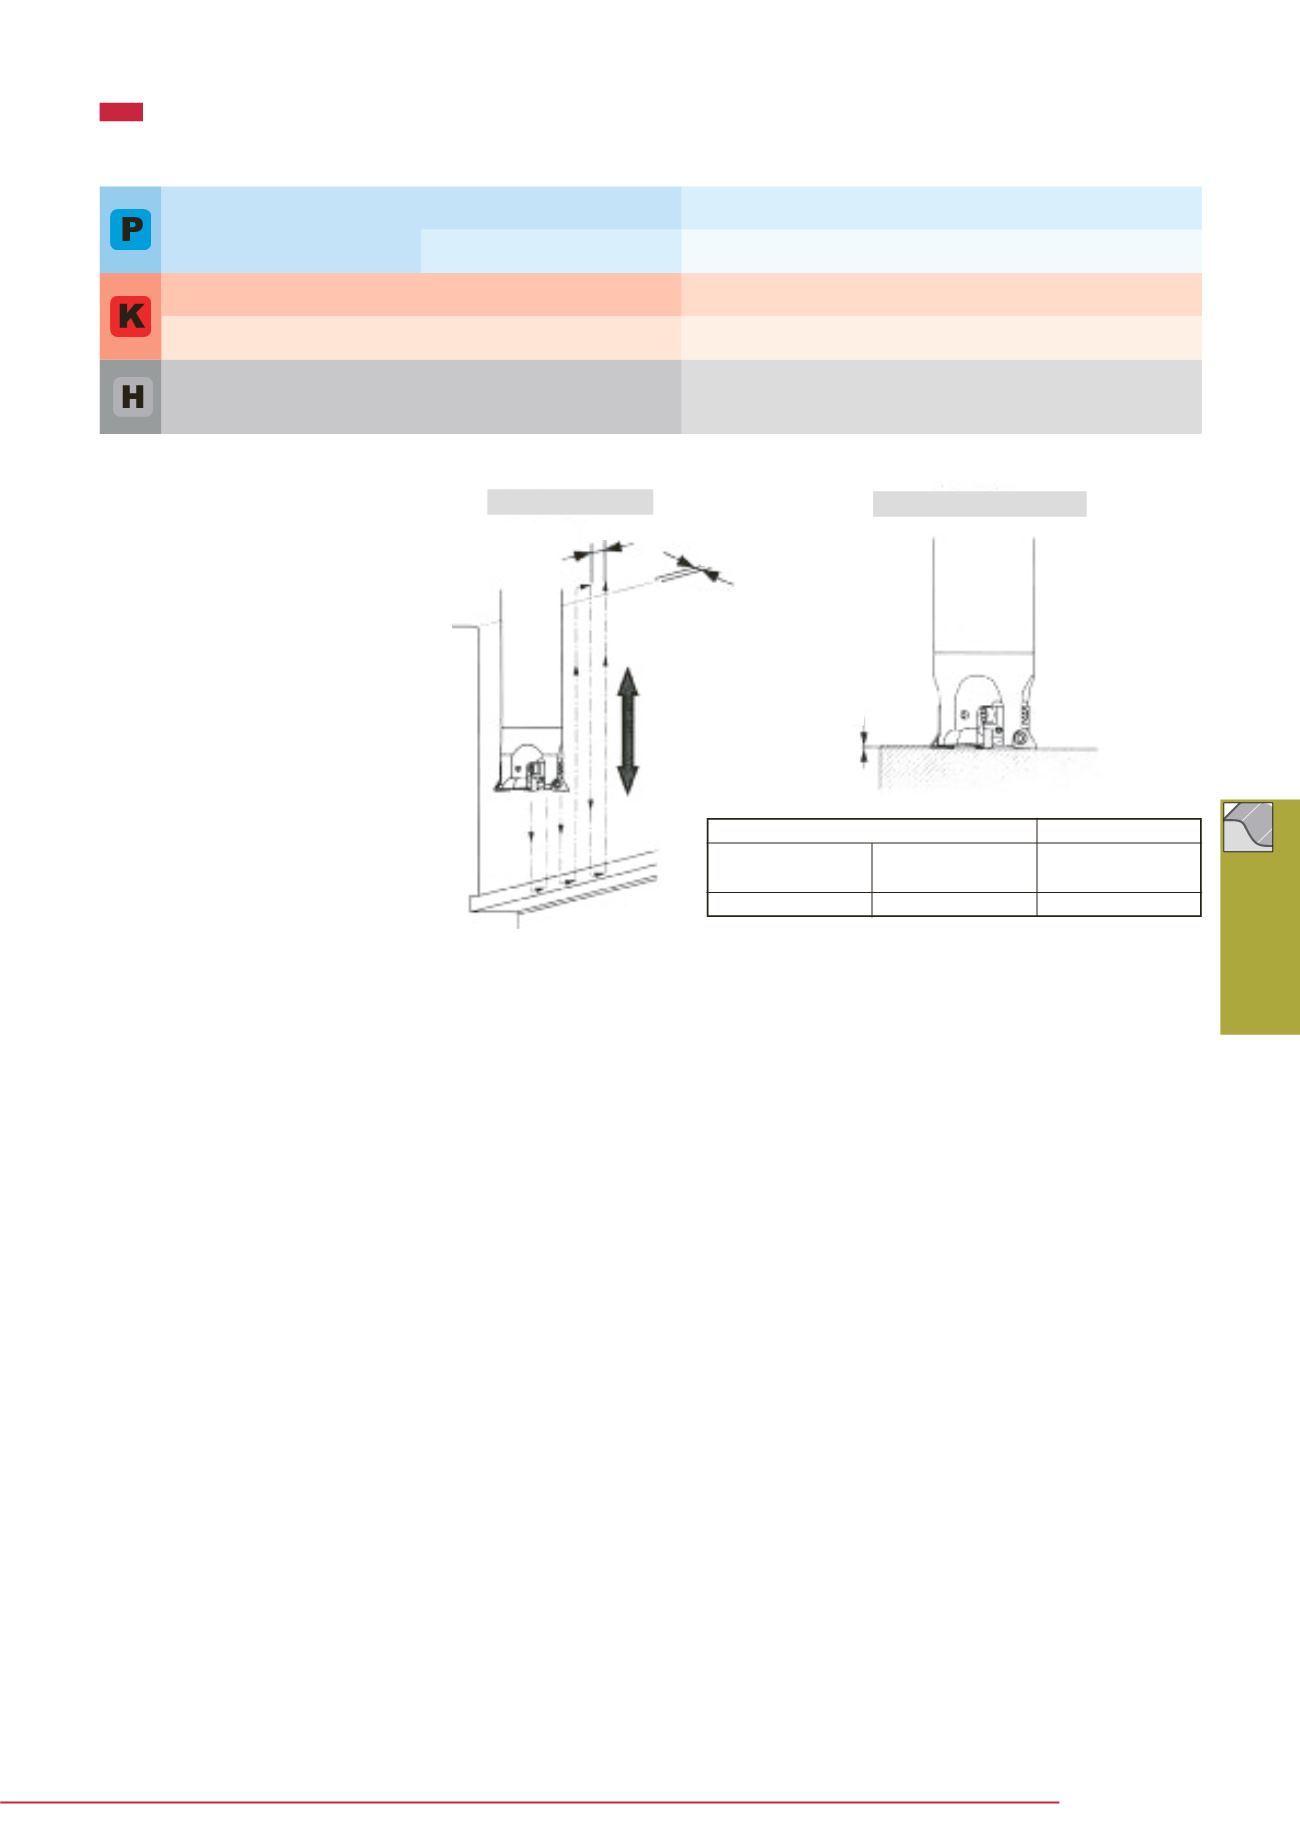
• Use the cutter for finish milling of vertical wall surfaces requiring
long tool-overhang of L/D > 6.
• Radial cutting edge run-out should be adjusted within 0.01 mm.
• In addition to Z-feed milling, TZF11 type cutters can be also used for
traverse feed milling. (
a
p
≤
0.5 mm)
• Dry cutting (or air blow) at a depth of
cut up
a
e to 0.3 mm (allowable max.
0.5 mm) and a pick feed
p
f from 0.5
to 1.0 mm is recommended.
• TZF11 type cutters are not designed
to adjust dynamic balance. Therefore,
when the tool’s overhang ratio (cutter
diameter-to-length) exceeds 6:1,
special care should be taken with
the revolution speed. (At first, start
the machining at 50 % of the speed
shown in the table of the standard
cutting conditions, and then gradually
increase the speed whilst confirming
safety.)
• To produce highly accurate surface
finish, use the cutter on a machine
with sufficient rigidity.
STANDARD CUTTING CONDITIONS
Traverse feed milling
Z-feed milling
Z-feed milling
Traverse feed milling
Pick feed
p
f (mm)
Radial depth of cut
a
e (mm)
Depth of cut
a
p (mm)


