D015
Tungaloy
High-Feed Milling
The above table shows the conditions for standard shank type cutters.
When using long shank type cutters, the number of teeth may be dierent.
In this case, the cutting conditions should be changed by referring to: “The
usage of standard and long shanks” shown in previous page.
Cutting conditions are generally limited by the rigidity and power of the
machine and the rigidity of the workpiece. When setting the conditions, start
from half of the values of the standard cutting conditions and then increase
the value gradually while making sure the machine is running normally.
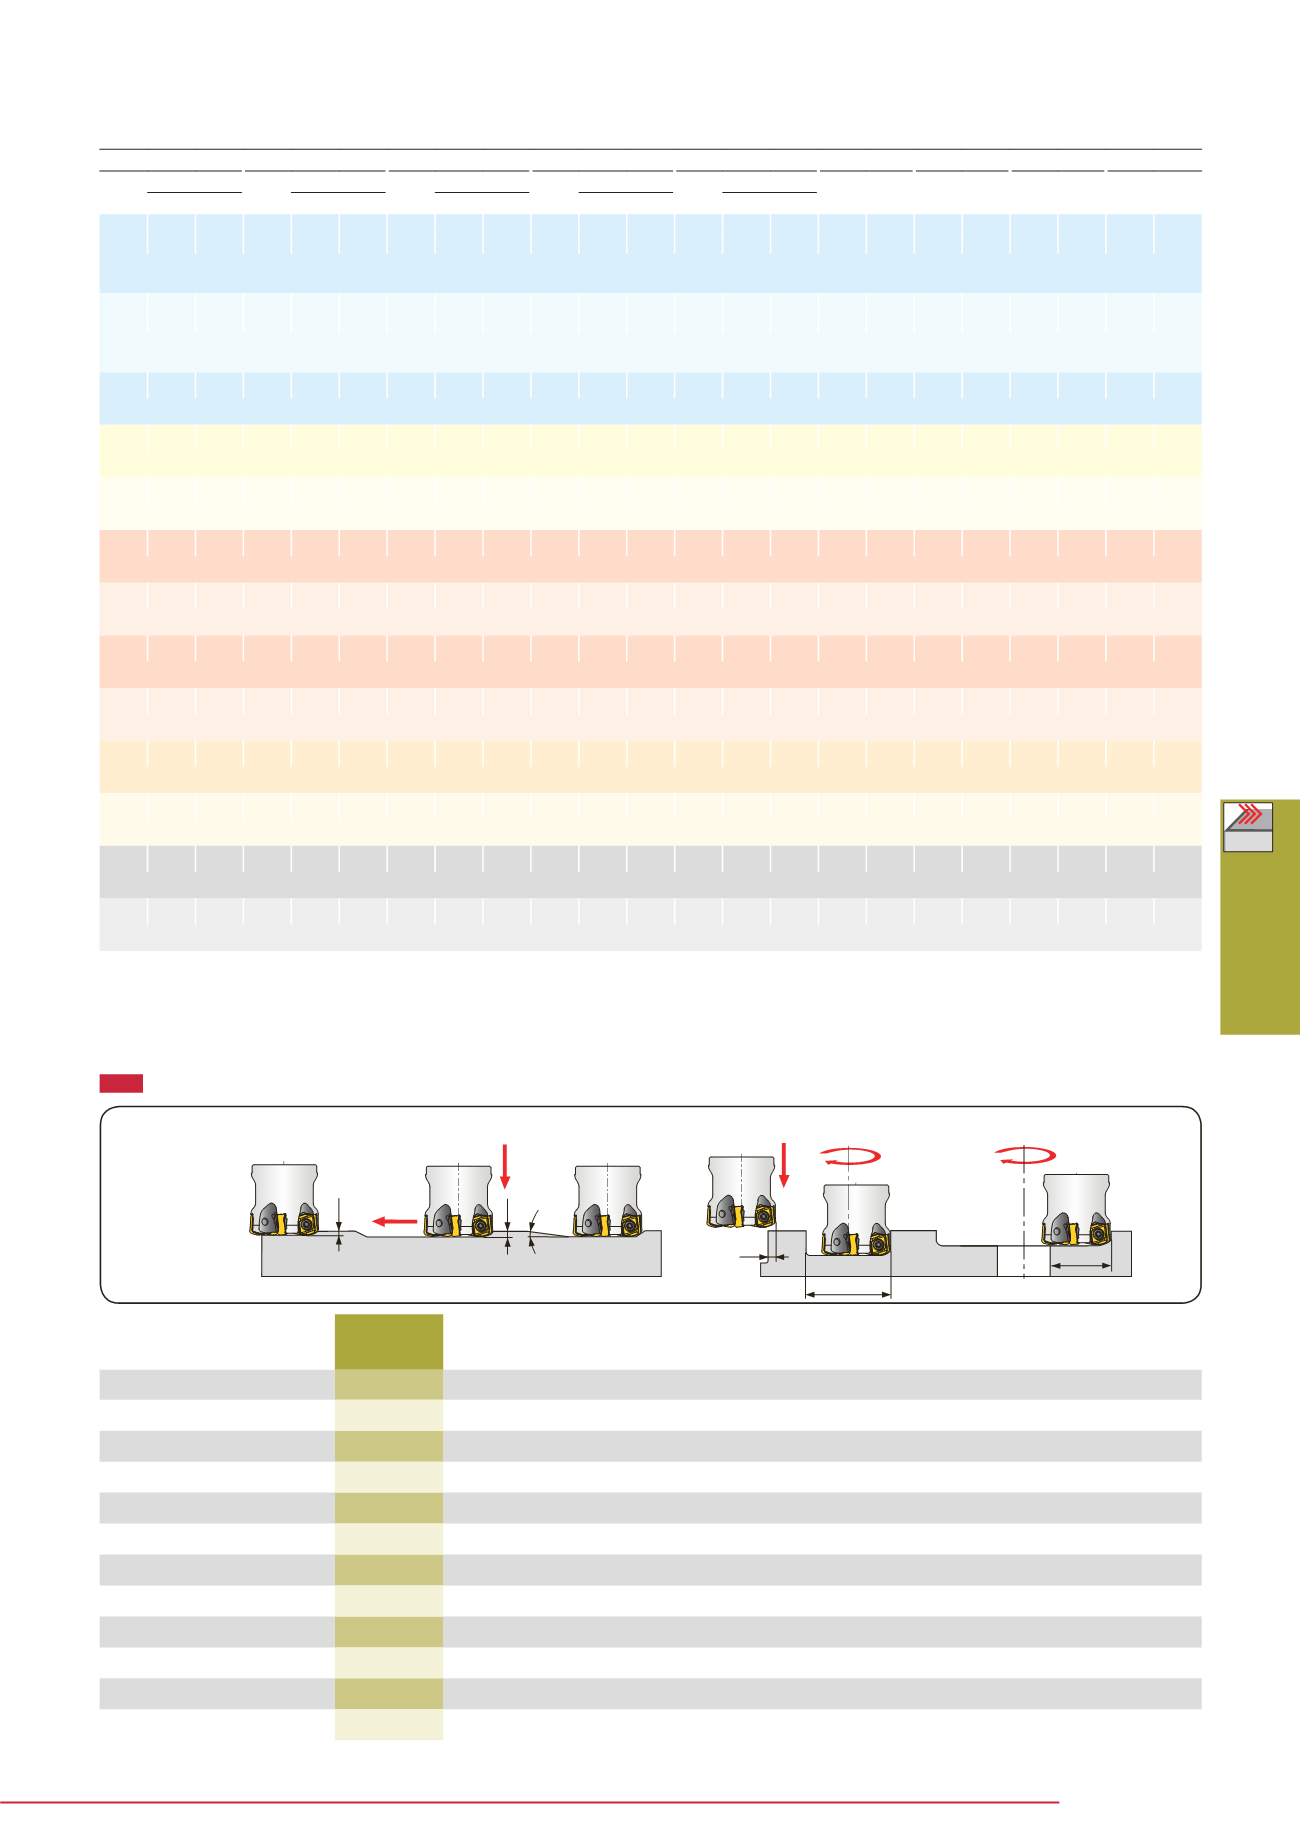
Tool dia.
Max. depth
of cut
Max. ramping
angle
Max. plunging
depth
Max. cutting width
in plunging
Min.machinable
hole dia.
Max.machinable
hole dia.
Max. cutting width
in enlarged hole
Designation
øD
c
Max. ap
θ°
A
W
øD1
øD2
ae
EXN06R032M...
ø32
1.5
2
0.5
6
47
59
25
EXN06R035M...
ø35
1.5
1.7
0.5
6
53
65
28
EXN06R040M...
ø40
1.5
1.3
0.5
6
63
75
33
TXN06R050M...
ø50
1.5
0.9
0.5
6
83
95
43
TXN06R052M...
ø52
1.5
0.8
0.5
6
87
99
45
TXN06R063M...
ø63
1.5
0.6
0.5
6
109
121
56
TXN06R066M...
ø66
1.5
0.5
0.5
6
115
127
59
TXN06R080M...
ø80
1.5
0.5
0.5
6
143
155
73
TXN06R100M...
ø100
1.5
0.34
0.5
6
183
195
93
TXN06R125M...
ø120
1.5
0.26
0.5
6
223
235
108
TXN06R160M...
ø160
1.5
0.2
0.5
6
303
315
153
TXN06R200M...
ø200
1.5
0.15
0.5
6
383
395
193
· For øDc above 100 mm, slot milling, ramping or contouring is not recommended as chips may be re-cut.
ø
D
1, ø
D
2
θ
a
p
A
a
e
W
Shoulder
milling
Traversing
Small depth
plunging
Ramping
Plunging
Drilling
(Helical feed)
Enlarged hole
APPLICATION RANGE
Tool dia.: øDc (mm), Number of revolutions: n (min
-1
), Feed speed: Vf (mm/min), Max. depth of cut: ap = 1.5 mm, No. of inserts: z
ø50
ø52
ø63
ø66
ø80
ø100, z = 6 ø125, z = 8 ø160, z = 10 ø200, z = 12
n
Vf
n
Vf
n
Vf
n
Vf
n
Vf
n Vf
n Vf
n Vf
n Vf
z = 4 z = 5
z = 4 z = 5
z = 4 z = 6
z = 4 z = 6
z = 5 z = 8
1,270 5,080 6,350 1,220 4,880 6,100 1,010 4,040 6,060 960 3,840 5,760 800 4,000 6,400 637 3,822 510 4,076 398 3,981 318 3,822
Vc = 200 m/min, fz = 1 mm/t
950 3,800 4,750 920 3,680 4,600 760 3,040 4,560 720 2,880 4,320 600 3,000 4,800 478 2,866 382 3,057 299 2,986 239 2,866
Vc = 150 m/min, fz = 1 mm/t
950 3,040 3,800 920 2,940 3,680 760 2,430 3,650 720 2,300 3,460 600 2,400 3,840 478 2,293 382 2,446 299 2,389 239 2,293
Vc = 150 m/min, fz = 0.8 mm/t
760 1,520 1,900 730 1,460 1,830 610 1,220 1,830 580 1,160 1,740 480 1,200 1,920 382 1,146 306 1,223 239 1,194 191 1,146
Vc = 120 m/min, fz = 0.5 mm/t
760 1,820 2,280 730 1,750 2,190 610 1,470 2,200 580 1,390 2,090 480 1,440 2,300 382 1,376 306 1,468 239 1,433 191 1,376
Vc = 120 m/min, fz = 0.6 mm/t
1,270 5,080 6,350 1,220 4,880 6,100 1,010 4,040 6,060 960 3,840 5,760 800 4,000 6,400 637 3,822 510 4,076 398 3,981 318 3,822
Vc = 200 m/min, fz = 1 mm/t
1,270 4,060 5,080 1,220 3,900 4,880 1,010 3,230 4,850 960 3,070 4,610 800 3,200 5,120 637 3,057 510 3,261 398 3,185 318 3,057
Vc = 200 m/min, fz = 0.8 mm/t
950 3,800 4,750 920 3,680 4,600 760 3,040 4,560 720 2,880 4,320 600 3,000 4,800 478 2,866 382 3,057 299 2,986 239 2,866
Vc = 150 m/min, fz = 1 mm/t
950 3,040 3,800 920 2,940 3,680 760 2,430 3,650 720 2,300 3,460 600 2,400 3,840 478 2,293 382 2,446 299 2,389 239 2,293
Vc = 150 m/min, fz = 0.8 mm/t
250 500 630 240 480 600 200 400 600 190 380 570 160 400 640 127 382 102 408 80 398 64 382
Vc = 40 m/min, fz = 0.5 mm/t
190 150 190 180 140 180 150 120 180 140 110 170 120 120 190 96 115 76 122 60 119 48 115
Vc = 30 m/min, fz = 0.2 mm/t
640 510 640 610 490 610 510 410 610 480 380 580 400 400 640 318 382 255 408 199 398 159 382
Vc = 100 m/min, fz = 0.2 mm/t
380 80 100 370 75 90 300 60 90 290 60 85 240 60 100 191 57 153 61 119 60 96 57
Vc = 60 m/min, fz = 0.05 mm/t


