D006
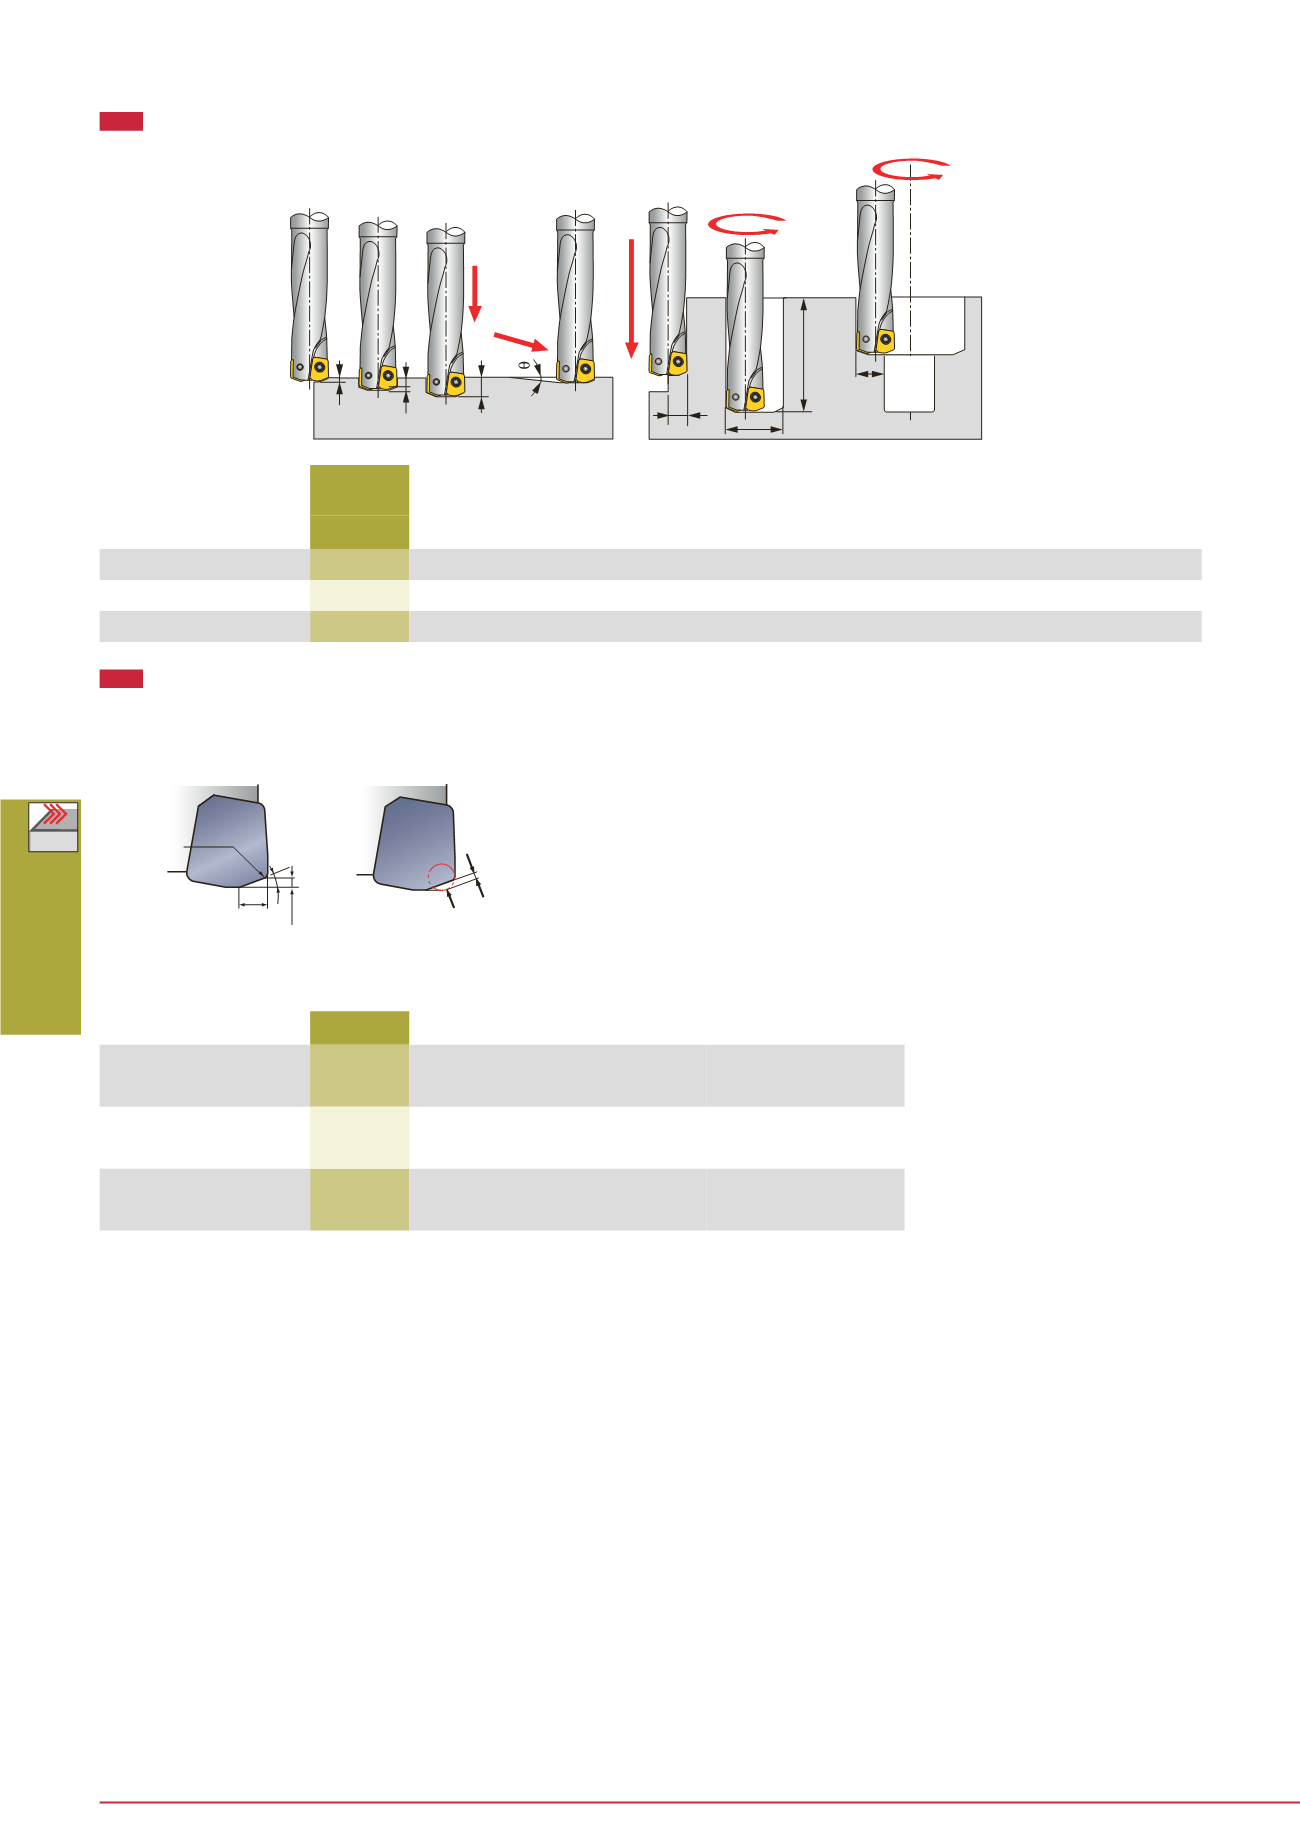
High-Feed Milling
H
W
H1
a
p
a
p
a
e
D
1,
D
2
øDc
ap
H
W
θº
D1
D2
ae
H1
EXH06R010M10.0-02
10
0.6
5
5
5
12
19
7
30
EXH07R012M12.0-02
12
0.6
6
6
5
14
23
9
36
EXH09R016M16.0-02
16
0.8
8
8
5
18
31
12.5
48
Designation
Designation
When using CAD/CAM, please program it as for radius cutter.
The following table shows actual cutting edge geometry and
amount of unfinished work cut.
W
a
p
20˚
øDc
ap
r
ε
W
t
R
EXH06R010M10.0-02
10
0.6
0.5
2.5
0.7
R0.5
0.6
R1.0
EXH07R012M12.0-02
12
0.6
0.5
2.5
0.7
R0.5
0.6
R1.0
EXH09R016M16.0-02
16
0.8
0.8
3
0.8
R0.5
0.7
R1.0
0.6
R1.5
Shoulder
milling Slotting
Plunging
Enlarging hole
Drilling
(Helical feed)
Drilling
Ramping
t: Amount
of uncut
Corner radius in
programming R
Corner
of insert
r
ε
(Max. depth of cut)
Max. cutting
width in
enlarging hole
Max.depth
of boring
Max.
machinable
hole dia.
Min.
machinable
hole dia.
Max.depth
of drilling
Max. cutting
width in
plunging
Max. depth
of cut
Max.
ramping
angle
Corner
radius in
programming
Corner
of insert
Wide
of tooth
Max.
depth
of cut
Amount
of uncut
APPLICATION RANGE
TOOL GEOMETRY ON PROGRAM
Tool dia.


