D199
Tungaloy
Profile Milling
ø20
ø25
ø32
ø35
ø40
ø50
ø63
n
Vf
n
Vf
n
Vf
n
Vf
n
Vf
n
Vf
n
Vf
E/HRP10
E/HRP10,
E/HRP12
E/HRP10E/HRP12
ERP10
TRP10 ERP12 ERP16
ERP12
TRP12 TRP16
2870 2870 2290 2290 1790 3580 2690 1640 3280 1430 3580 2860 1430 1150 2880 910 2730 2280
Vc = 180 m/min, fz = 0.5 mm/t
2870 2870 2290 2290 1790 3580 2690 1640 3280 1430 3580 2860 1430 1150 2880 910 2730 2280
Vc = 180 m/min, fz = 0.5 mm/t
2710 2160 2170 1740 1690 2700 2030 1550 2480 1350 2700 2160 1080 1080 2160 860 2060 1720
Vc = 170 m/min, fz = 0.4 mm/t
2710 2160 2170 1740 1690 2700 2030 1550 2480 1350 2700 2160 1080 1080 2160 860 2060 1720
Vc = 170 m/min, fz = 0.4 mm/t
2070 1240 1660 1000 1290 1550 1160 1180 1420 1030 1550 1240 620 830 1250 660 1190 990
Vc = 130 m/min, fz = 0.3 mm/t
2710 2160 2170 1740 1690 2700 2030 1550 2480 1350 2700 2160 1080 1080 2160 860 2060 1720
Vc = 170 m/min, fz = 0.4 mm/t
2710 2160 2170 1740 1690 2700 2030 1550 2480 1350 2700 2160 1080 1080 2160 860 2060 1720
Vc = 170 m/min, fz = 0.4 mm/t
3180 2540 2550 2040 1990 3180 2390 1820 2910 1590 3180 2540 1270 1270 2540 1010 2420 2020
Vc = 200 m/min, fz = 0.4 mm/t
3180 2540 2550 2040 1990 3180 2390 1820 2910 1590 3180 2540 1270 1270 2540 1010 2420 2020
Vc = 200 m/min, fz = 0.4 mm/t
2870 2870 2290 2290 1790 3580 2690 1640 3280 1430 3580 2860 1430 1150 2880 910 2730 2280
Vc = 180 m/min, fz = 0.5 mm/t
2390 2390 1910 1910 1490 2980 2240 1360 2720 1190 2980 2380 1190 950 2380 760 2280 1900
Vc = 150 m/min, fz = 0.5 mm/t
1590 630 1270 510 990 790
590 910 730 800 800 640 320 640 640 510 610 510
Vc = 100 m/min, fz = 0.2 mm/t
640 150 510 120 400 190
140 360 170 320 190 150 75 250 150 200 140 120
Vc = 40 m/min, fz = 0.12 mm/t
OK
Tool dia.: øDc (mm), Number of revolutions: n (min -1 ), Feed speed: Vf (mm/min), Depth of cut: ap = 2.0 mm
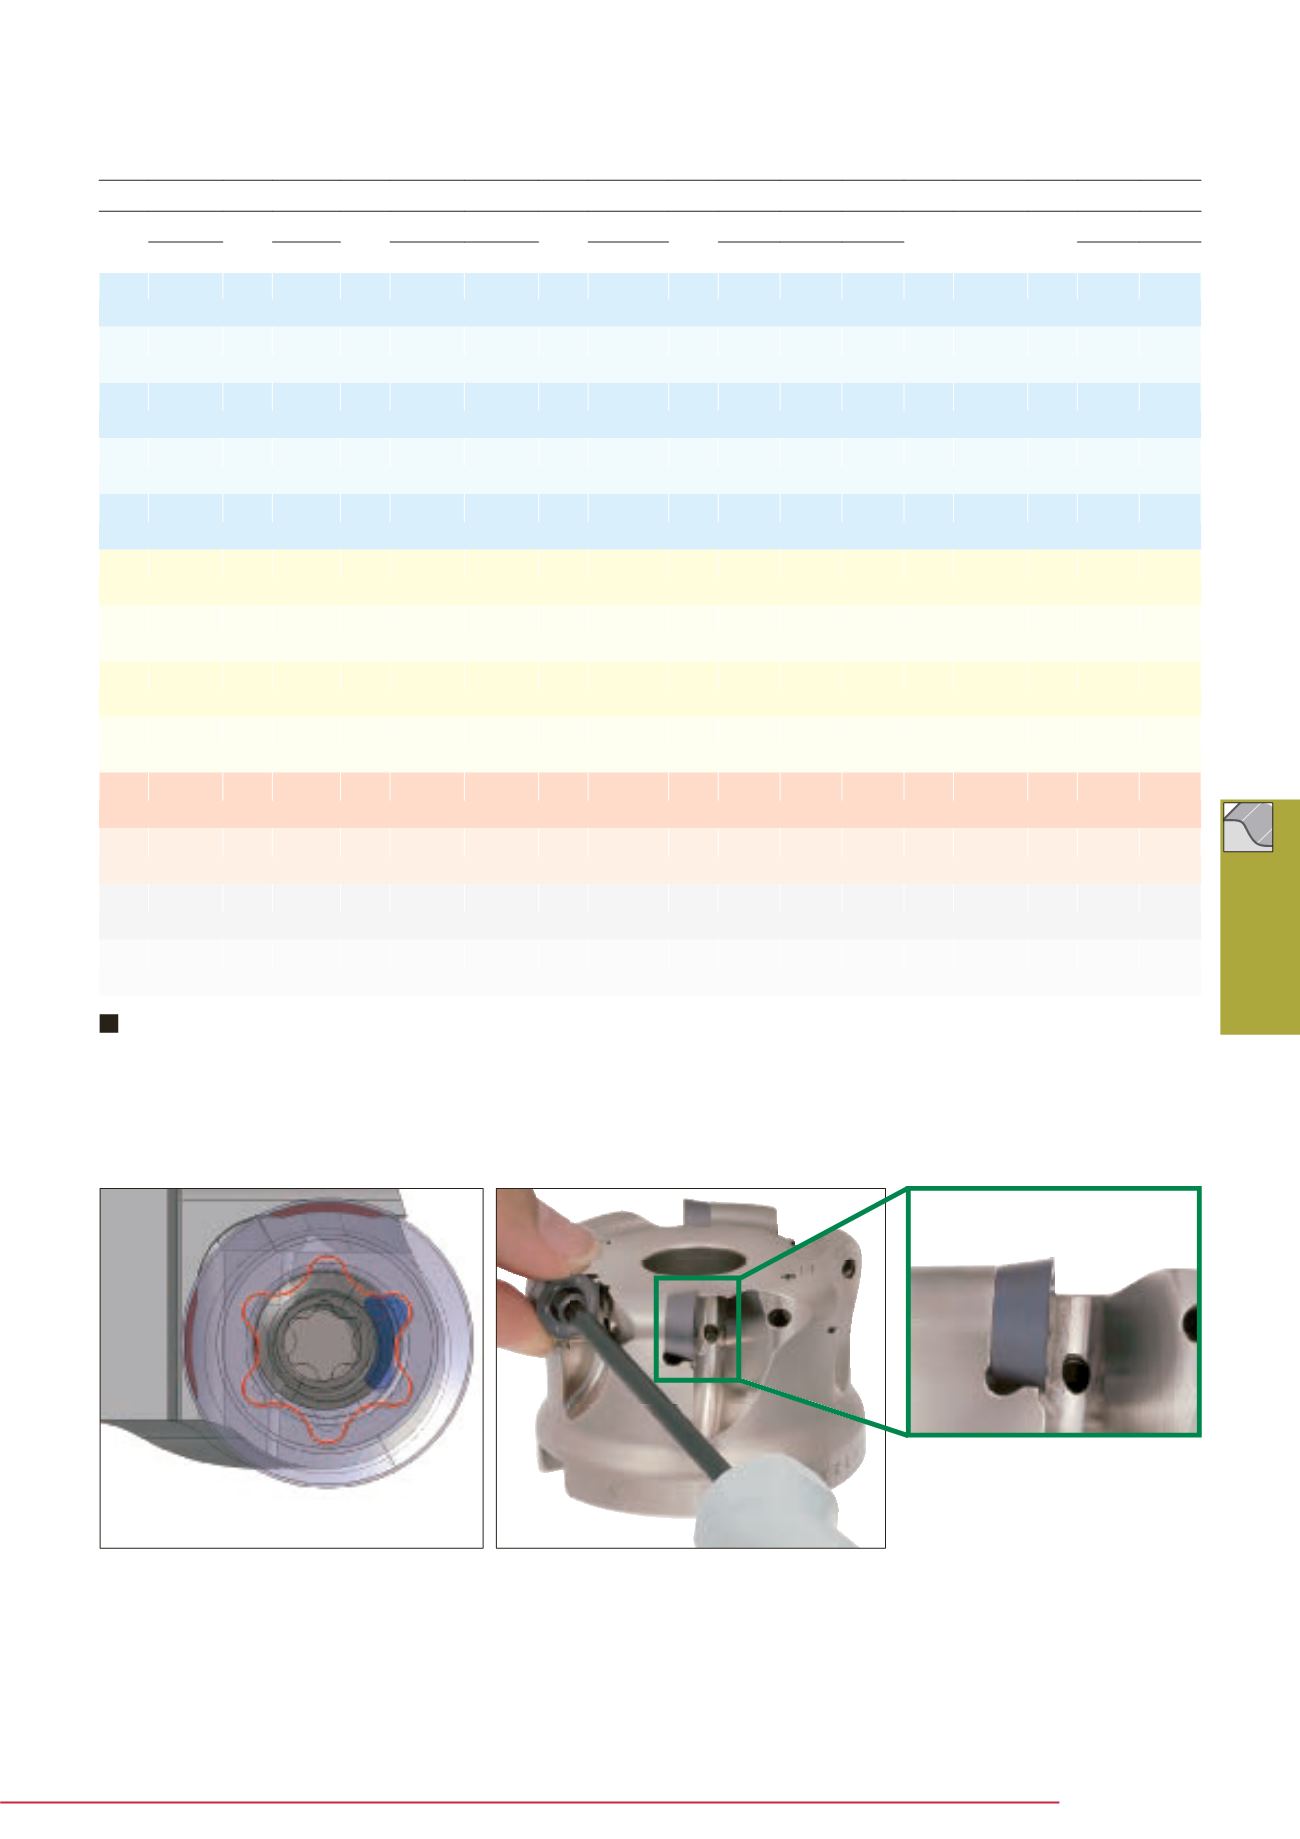
Notification for clamping
·
When installing the insert, please carefully locate the insert in the seat and fasten the screw.
Make sure the insert cavity fits the protrusion
on the body


