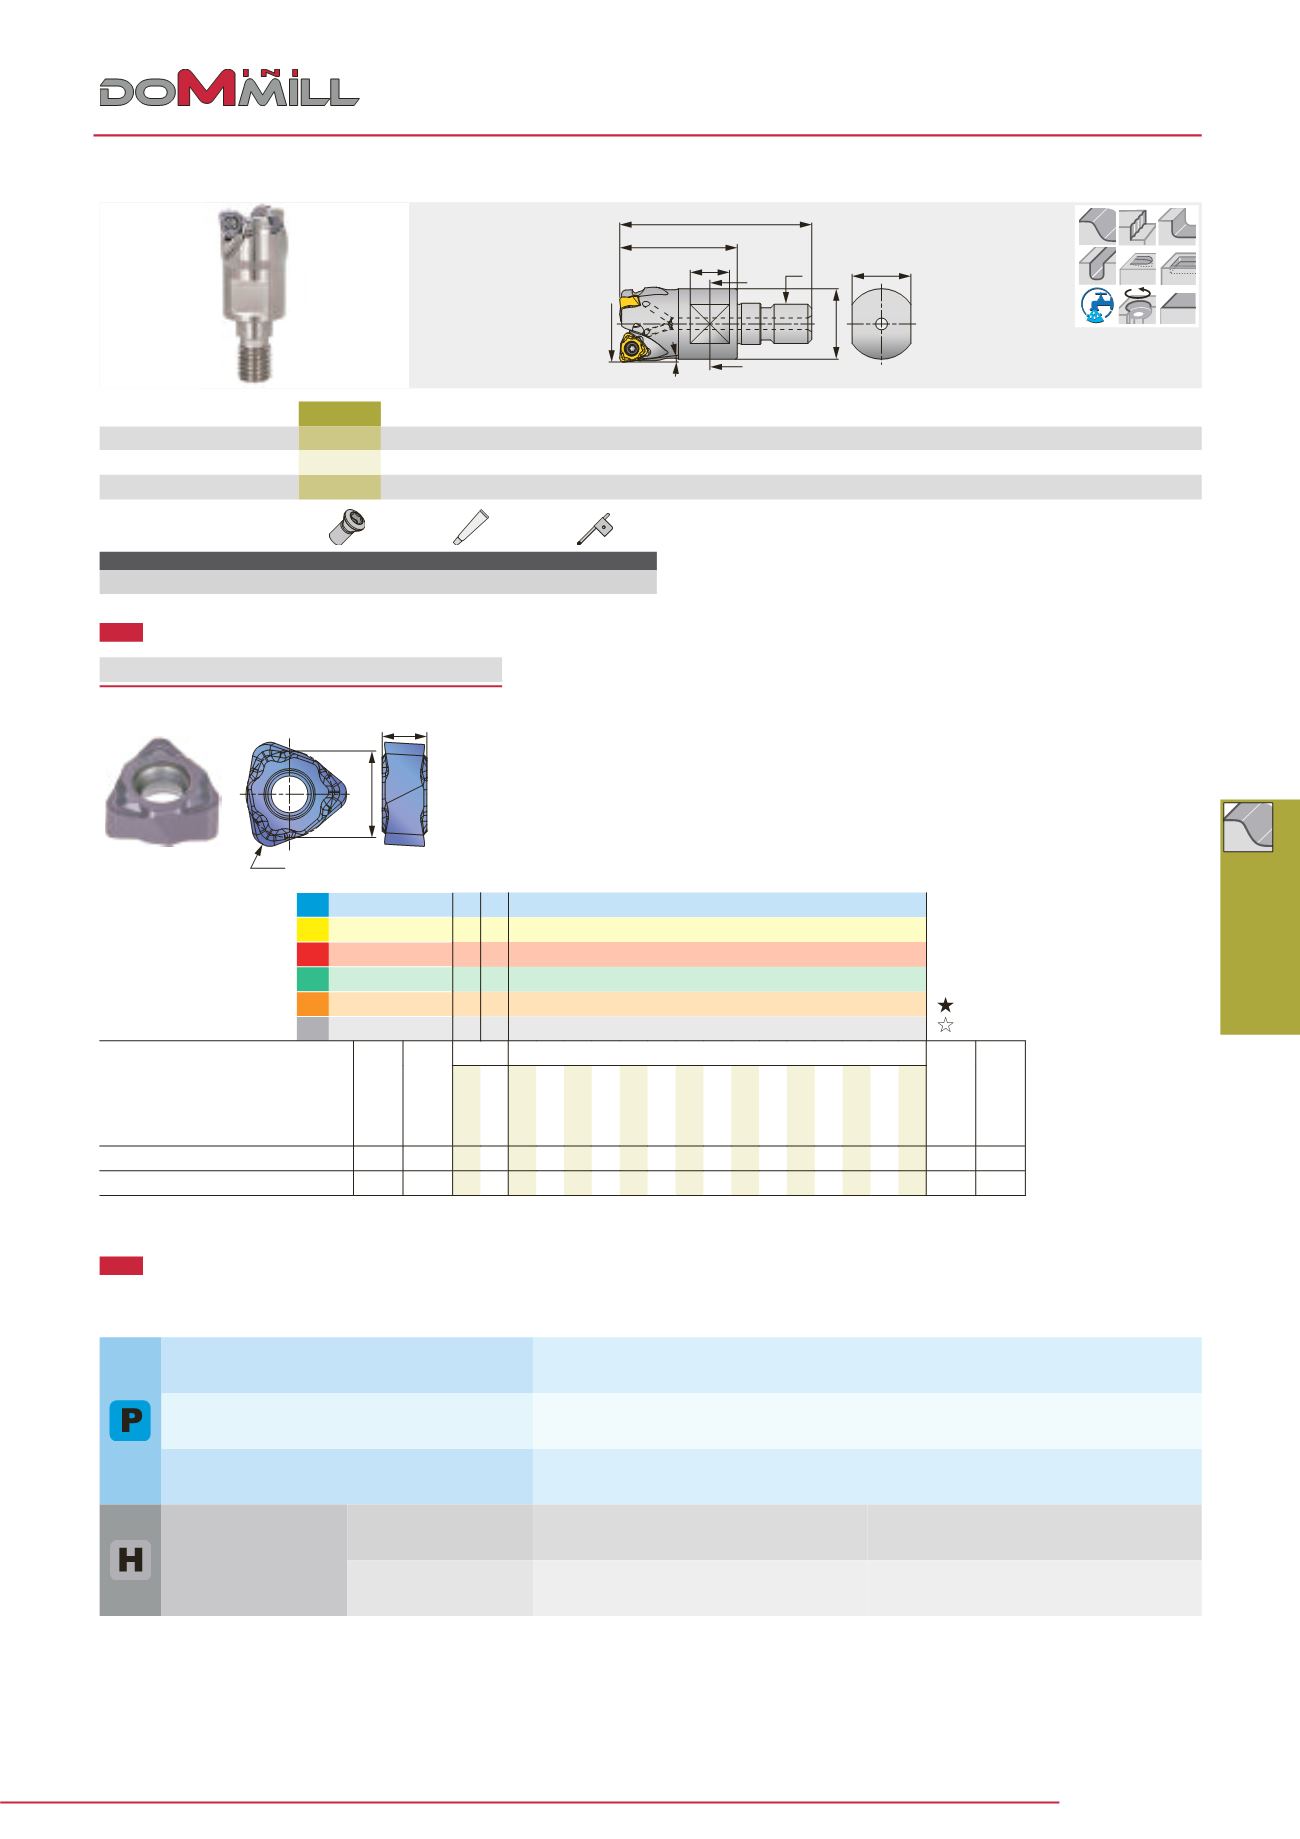
D195
Tungaloy
Profile Milling
øDc
C
Lf
L
6
øD
3
T
A
A
4°
Ts
A - A cross section
R
R R
Designation
øD
c
z
L
6
L
f
C
T
øD
3
Ts
Kg Air hole Insert
HFWX04M016M08R02
16
2
42
25
8
10
13
M8
0.03
with WXHU04...
HFWX04M020M10R03
20
3
49
30
10
15
18
M10
0.05
with WXHU04...
HFWX04M025M12R04
25
4
52
30
10
17
21
M12
0.09
with WXHU04...
SPARE PARTS
Designation
Clamping screw Lubricant
Wrench
HFWX04M...
SR34-514
M-1000
T-7F
HFWX04-M
Small-radius cutter for finishing operation; Modular head with TungFlex threaded adaptation
INSERT
WXHU-MJ
T
ød
r
ε
ap
P Steel
M Stainless
K Cast iron
N Non-ferrous
S Superalloys
H Hard materials
Designation
r
ε Max.
a
p
Coating
ø
d
T
AH110
WXHU040305R-MJ
0.5 0.5
l
6.35 3.18
WXHU040310R-MJ
1 1
l
6.35 3.18
ISO
200 - 300 HB
AH110
100 - 300
0.1 - 0.3
150 - 300 HB
AH110
100 - 300
0.1 - 0.3
30 - 40 HRC
AH110
100 - 300
0.05 - 0.3
40 - 50 HRC
AH110
80 - 130
0.1 - 0.3
50 - 60 HRC
AH110
50 - 100
0.05 - 0.15
STANDARD CUTTING CONDITIONS
*
For plunging
,
width up to
2
mm is possible.
l
: Line-up
: First choice
: Second choice
Cutting speed
Vc (m/min)
Feed per tooth
fz (mm/t)
Workpiece material
Grade
Hardness
High carbon steel
C45, C55, etc.
Alloy steel
42CrMo4, SCr145, etc.
Prehardened steel
NAK80, PX5, etc.
Hardened steel
X40CrMoV5-1, etc.
X153CrMoV12, etc.


