D102
Shoulder Milling
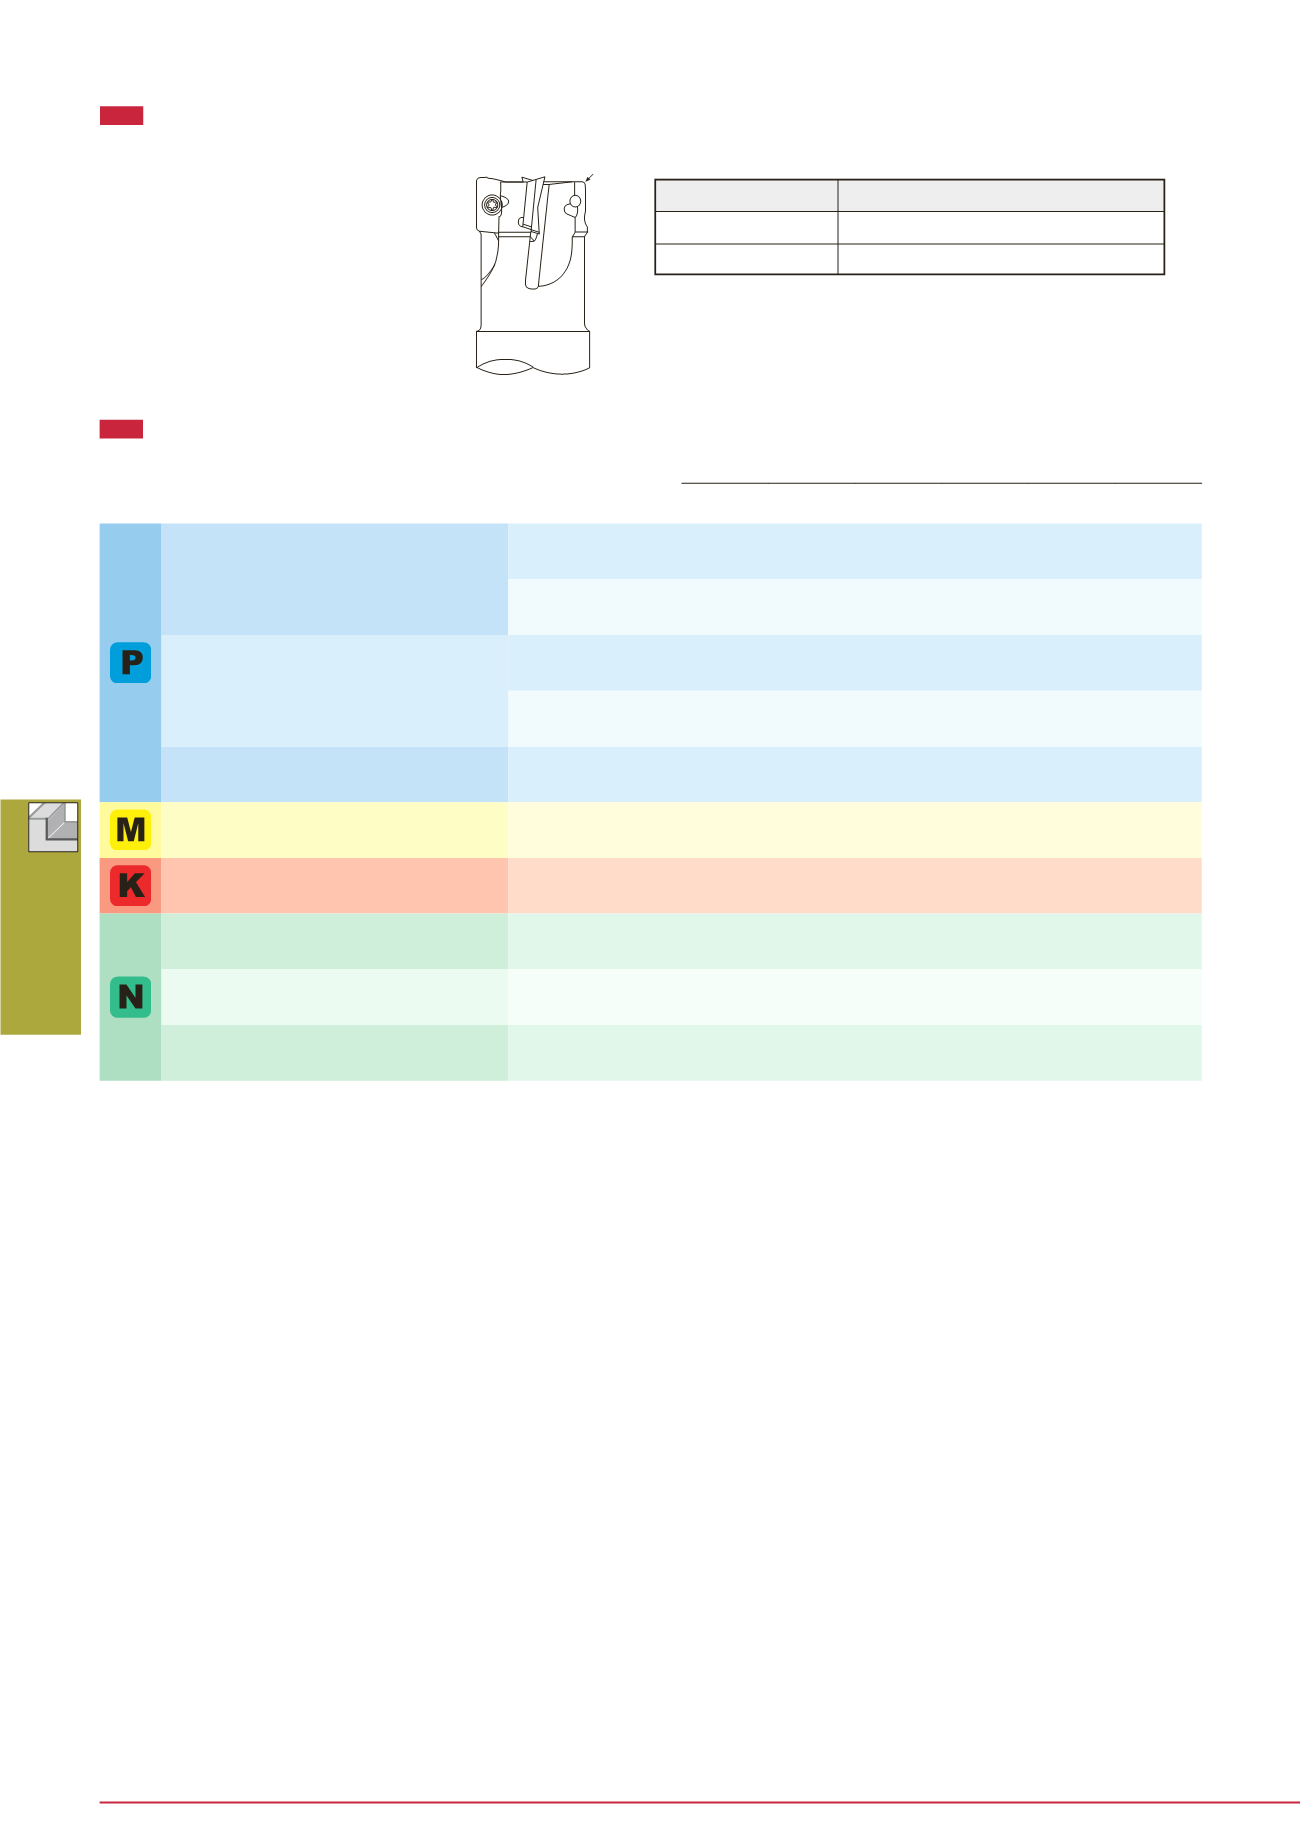
CAUTIONARY POINT IN MODIFYING CUTTER BODIES
0.4 ~ 1.6
2.0 ~ 3.2
2
R
When using inserts with corner radius
r
ε
≥
2.0 mm, standard cutter bodies
have to be modified “R”.
Unnecessary
Corner radius
r
ε
(mm)
The dimension of modifying (mm)
Notes: • When using at L/D
≥
4, machining at the lower feed rate.
• This TAC mill is not designed to cope with the centrifugal force and
dynamic balance at high speeds over 1000 m/min.
Therefore, the cutting speed in the outer diameter of the mill should
not exceed 1000 m/min.
STANDARD CUTTING CONDITIONS
ISO
Workpiece material
Grade Chip-
breaker
Cutting speed
Vc
(m/min)
Feed per tooth fz (mm/t)
Cutter dia.
ø12
Cutter dia.
ø16, ø20
Cutter dia.
> ø25
Cutter dia.
ø12
Cutter dia.
ø16, ø20
Cutter dia.
> ø25
Mild steel, Low Carbon steels
C10, E275A, etc. < 180HB
NS740
MJ
80 ~ 100 100 ~ 120 100 ~ 150 0.05 ~ 0.08 0.05 ~ 0.12 0.05 ~ 0.15
AH120
MJ
80 ~ 100 100 ~ 150 100 ~ 150 0.05 ~ 0.1 0.12 ~ 0.2 0.12 ~ 0.2
Carbon steels, Alloy steels
C55, 42CrMo4, etc. < 300HB
NS740
MJ
80 ~ 100 80 ~ 100 80 ~ 120 0.05 ~ 0.08 0.05 ~ 0.08 0.05 ~ 0.1
T3130
MJ
80 ~ 100 80 ~ 120 100 ~ 200 0.05 ~ 0.1 0.10 ~ 0.15 0.1 ~ 0.2
Die steels
X96CrMoV12, etc. < 300HB
T3130
MJ
80 ~ 100 80 ~ 120 100 ~ 150 0.05 ~ 0.1 0.1 ~ 0.15 0.12 ~ 0.2
Stainless steels
X5CrNi18-9, etc. < 250HB
AH130
MS 80 ~ 100 100 ~ 150 100 ~ 200 0.05 ~ 0.1 0.12 ~ 0.15 0.12 ~ 0.2
Grey Cast irons, DuctileCast irons etc.
250, 400-15S, etc.
T1115
MJ
80 ~ 100 100 ~ 150 100 ~ 200 0.08 ~ 0.12 0.12 ~ 0.2 0.15 ~ 0.25
Aluminium alloys
Si < 13%
DS1100
AJ 300 ~ 1000 300 ~ 1000 300 ~ 1000 0.05 ~ 0.2 0.05 ~ 0.2 0.05 ~ 0.2
Aluminium alloys
Si ≥ 13%
DS1100
AJ
100 ~ 200 100 ~ 200 100 ~ 200 0.05 ~ 0.2 0.05 ~ 0.2 0.05 ~ 0.2
Copper alloys
KS05F
AJ
200 ~ 500 200 ~ 500 200 ~ 500 0.05 ~ 0.2 0.05 ~ 0.2 0.05 ~ 0.2


