D104
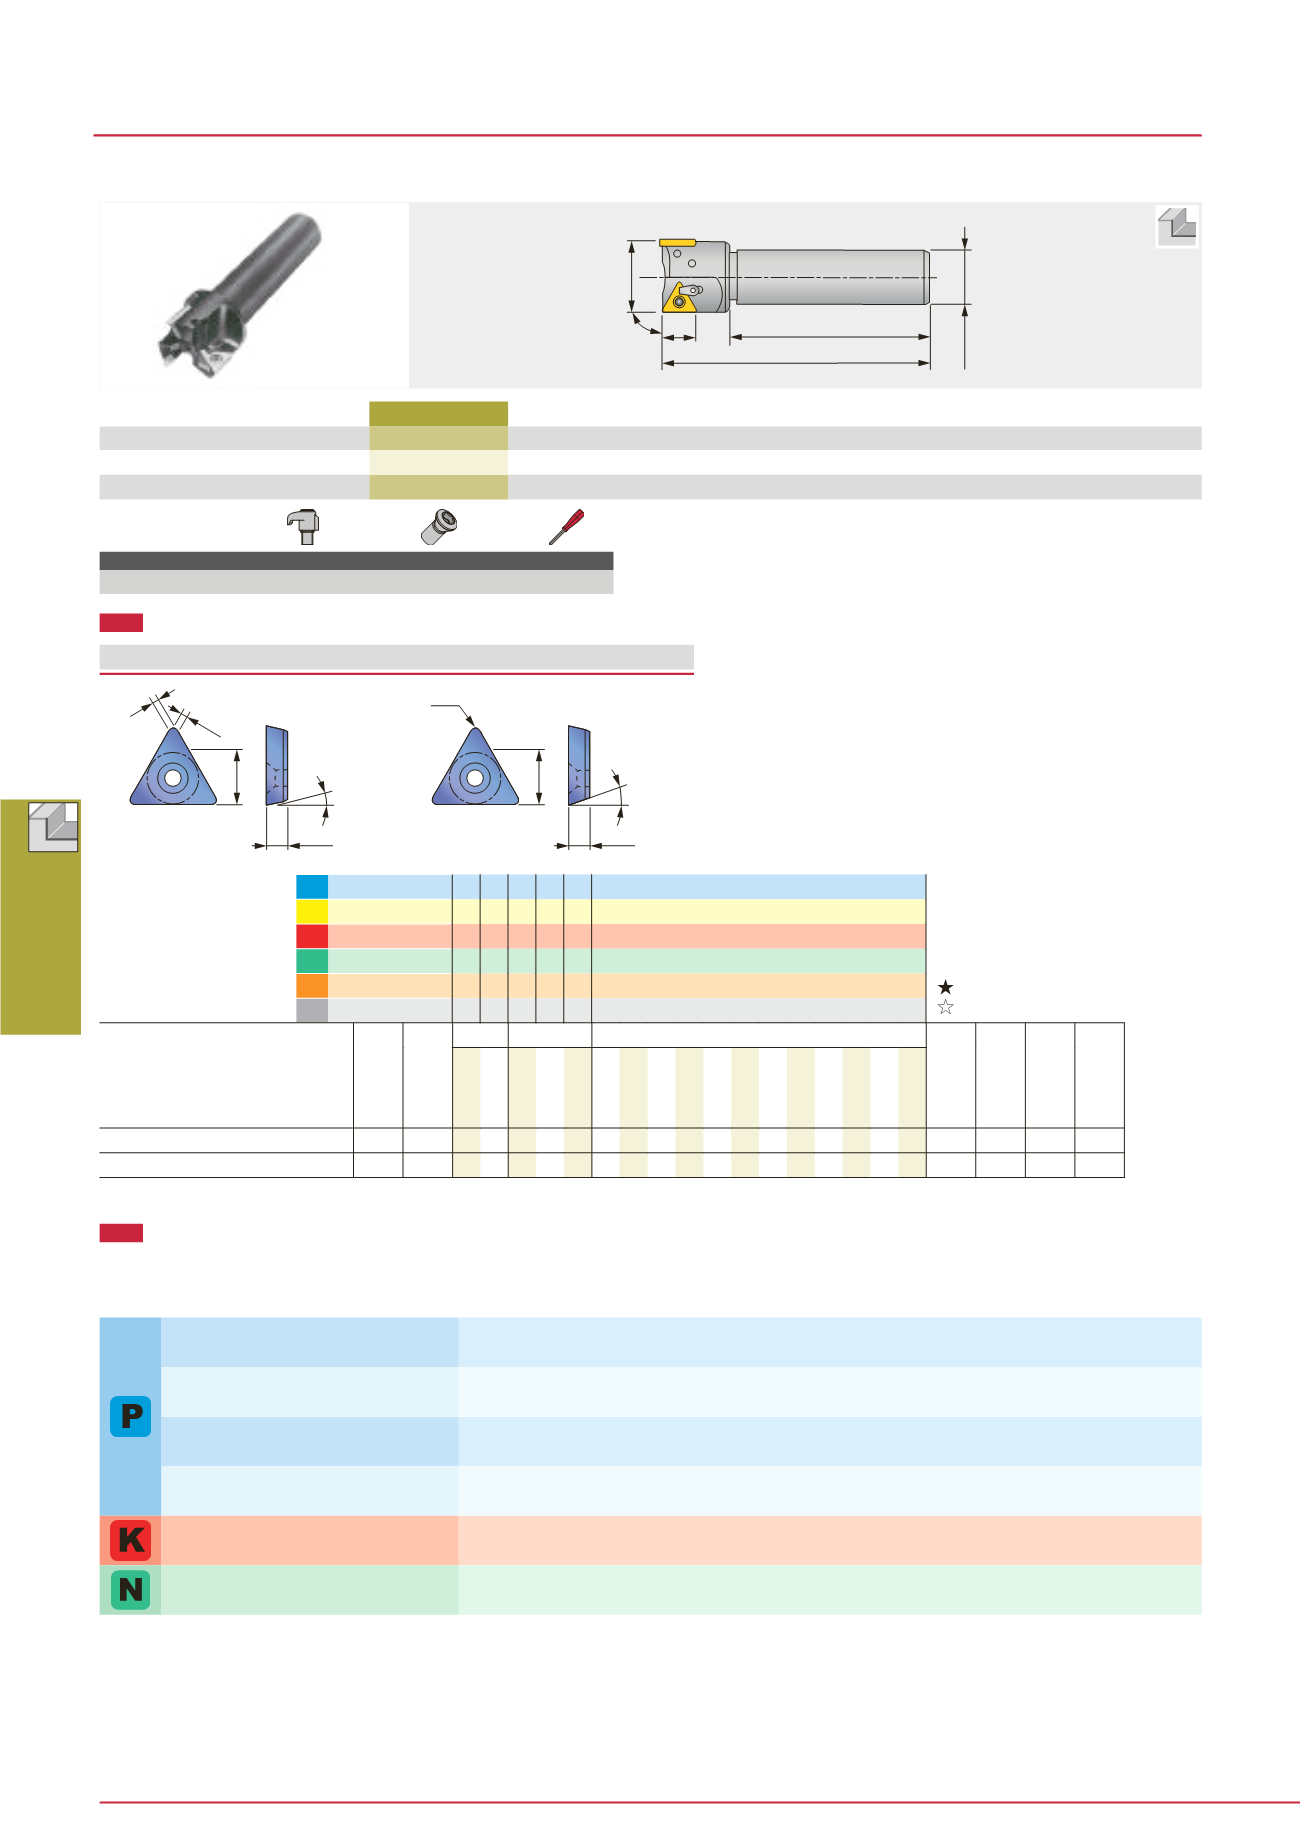
Shoulder Milling
øDc
R
s
L
ap
90°
Ø
D
s
h6
Designation
Max. ap
øD
c
z
øD
s
ℓ
s
L
Insert
PES1535R
19
35
2
32
120
160
TP*A43...
PES1540R
19
40
2
32
120
160
TP*A43...
PES1550R
19
50
3
32
120
160
TP*A43...
SPARE PARTS
Designation
Clamp set
Clamping screw Wrench
PES15...
CSG-5T
CSTA-4
T-15D
PES1500
Square shoulder endmills with triangle inserts
TPCA/TPMA
ød
11º
11º
Fig.1
Fig.2
T
0.5
bs
ød
T
r
ε
INSERT
P Steel
M Stainless
K Cast iron
N Non-ferrous
S Superalloys
H Hard materials
Designation
r
ε Max.
a
p
Cermet Uncoated
ø
d
T bs Fig.
NS740
UX30
TH10
TPCA43ZTRW1
-
19
l
12.7 4.76 1 1
TPMA432TNW1
0.8 19
l l l
12.7 4.76 -
2
l
: Line-up
: First choice
: Second choice
STANDARD CUTTING CONDITIONS
ISO
Workpiece material
Grade
Cutting speed Vc (m/min)
Feed per tooth fz (m/min)
Mild steels
UX30
100 ~ 150
0.1 ~ 0.3
Carbon steels
UX30
100 ~ 120
0.1 ~ 0.25
Alloy steels
UX30
80 ~ 100
0.1 ~ 0.2
Die steels
20 ~ 30HRC
UX30
50 ~ 70
0.1 ~ 0.2
Cast irons
TH10
70 ~ 90
0.1 ~ 0.3
Non-ferrous metals
TH10
200 ~ 500
0.05 ~ 0.2
• No. of revolutions (min
-1
) = Cutting speed 1000 ÷ 3.14 ÷ Cutter diameter
• Table feed (mm/min) = No. of revolutions Feed per tooth No. of inserts
A.R. = +3°~ +5°, R.R. = -8°~ 0°


