D096
Shoulder Milling
•
V
c: Cutting speed
•
f
z: Feed per tooth (Feed per revolution is
f
z 2 as effective number of teeth is equal to two)
Notes : • To get the best of the tool’s performance, use of a high-accuracy, side-lock type toolholder or milling chuck which has a high gripping force is
recommended.
• Excessive tool overhang from the toolholder should be avoided to prevent chatter.
ISO Workpiece material
Grade
Cutter diameter (mm)
ø
25
ø
32
ø
40
Vc
(m/min)
fz
(mm/t)
Vc
(m/min)
fz
(mm/t)
Vc
(m/min)
fz
(mm/t)
Mild steels, Low carbon steels
E275A, C15E4, etc.
T3130
(AH120)
60 ~ 150
0.08 ~ 0.2
60 ~ 150
0.1 ~ 0.3
60 ~ 150
0.1 ~ 0.3
High carbon steels, Alloy steels
C55, 42CrMo4, etc.
T3130
(AH120)
60 ~ 120
0.08 ~ 0.2
60 ~ 120
0.1 ~ 0.3
60 ~ 120
0.1 ~ 0.3
Die steels
X153CrMoV12, etc.
T3130
(AH120)
60 ~ 100
0.08 ~ 0.2
60 ~ 100
0.1 ~ 0.3
60 ~ 100
0.1 ~ 0.3
Stainless steels
X5CrNi18-9, etc.
AH140
70 ~ 120
0.08 ~ 0.2
70 ~ 120
0.1 ~ 0.3
70 ~ 120
0.1 ~ 0.3
Cast irons
250, 450-10S, etc.
AH120
60 ~ 150
0.08 ~ 0.2
60 ~ 150
0.1 ~ 0.3
60 ~ 150
0.1 ~ 0.3
ISO Workpiece material
Grade
Cutter diameter (m
m)
ø32
ø40
ø50
ø63
Vc
(m/min)
fz
(mm/t)
Vc
(m/min)
fz
(mm/t)
Vc
(m/min)
fz
(mm/t)
Vc
(m/min)
fz
(mm/t)
Mild steels, Low carbon steels
E275A, C15E4, etc.
T3130
(AH120)
60 ~ 150 0.1 ~ 0.3 70 ~ 150 0.1 ~ 0.3 70 ~ 150 0.1 ~ 0.3 70 ~ 150 0.1 ~ 0.3
High carbon steels, Alloy steels
C55, 42CrMo4, etc.
T3130
(AH120)
60 ~ 120 0.1 ~ 0.3 60 ~ 120 0.1 ~ 0.3 60 ~ 150 0.1 ~ 0.3 60 ~ 150 0.1 ~ 0.3
Die steels
X153CrMoV12, etc.
T3130
(AH120)
60 ~ 100 0.1 ~ 0.3 60 ~ 100 0.1 ~ 0.3 60 ~ 120 0.1 ~ 0.3 60 ~ 120 0.1 ~ 0.3
Stainless steels
X5CrNi18-9, X5CrNiMo17-12-3, etc.
AH140 70 ~ 120 0.1 ~ 0.3 60 ~ 120 0.1 ~ 0.3 60 ~ 120 0.1 ~ 0.3 60 ~ 120 0.1 ~ 0.3
Cast irons
250, 450-10S, etc.
AH120 60 ~ 150 0.1 ~ 0.3 60 ~ 150 0.1 ~ 0.3 60 ~ 150 0.1 ~ 0.3 60 ~ 150 0.1 ~ 0.3
ELP* *RA
type
STANDARD CUTTING CONDITIONS
• No. of revolutions (min
-1
) = Cutting speed 1000 3.14 Cutter diameter
• Table feed (mm/min) = No. of revolutions Feed per tooth No. of inserts
•
V
c: Cutting speed
•
f
z: Feed per tooth (Feed per revolution is
f
z
2 as effective number of teeth is equal to two)
Notes : • Dry cutting (or air-blowing) is generally recommended. When chips tend to adhere
to the cutting edges such as in milling stainless steel, use a water-soluble cutting
fluid.
• When the cutting width is larger than a half of the cutter diameter or chips tend to
stay in the cutting area, use an air blast to remove chips.
• To get the best of the tool performance, use of a high-accuracy, side-lock type
toolholder or milling chuck which has a high gripping force is recommended.
Excessive tool overhang from the toolholder should be avoided to prevent chatter.
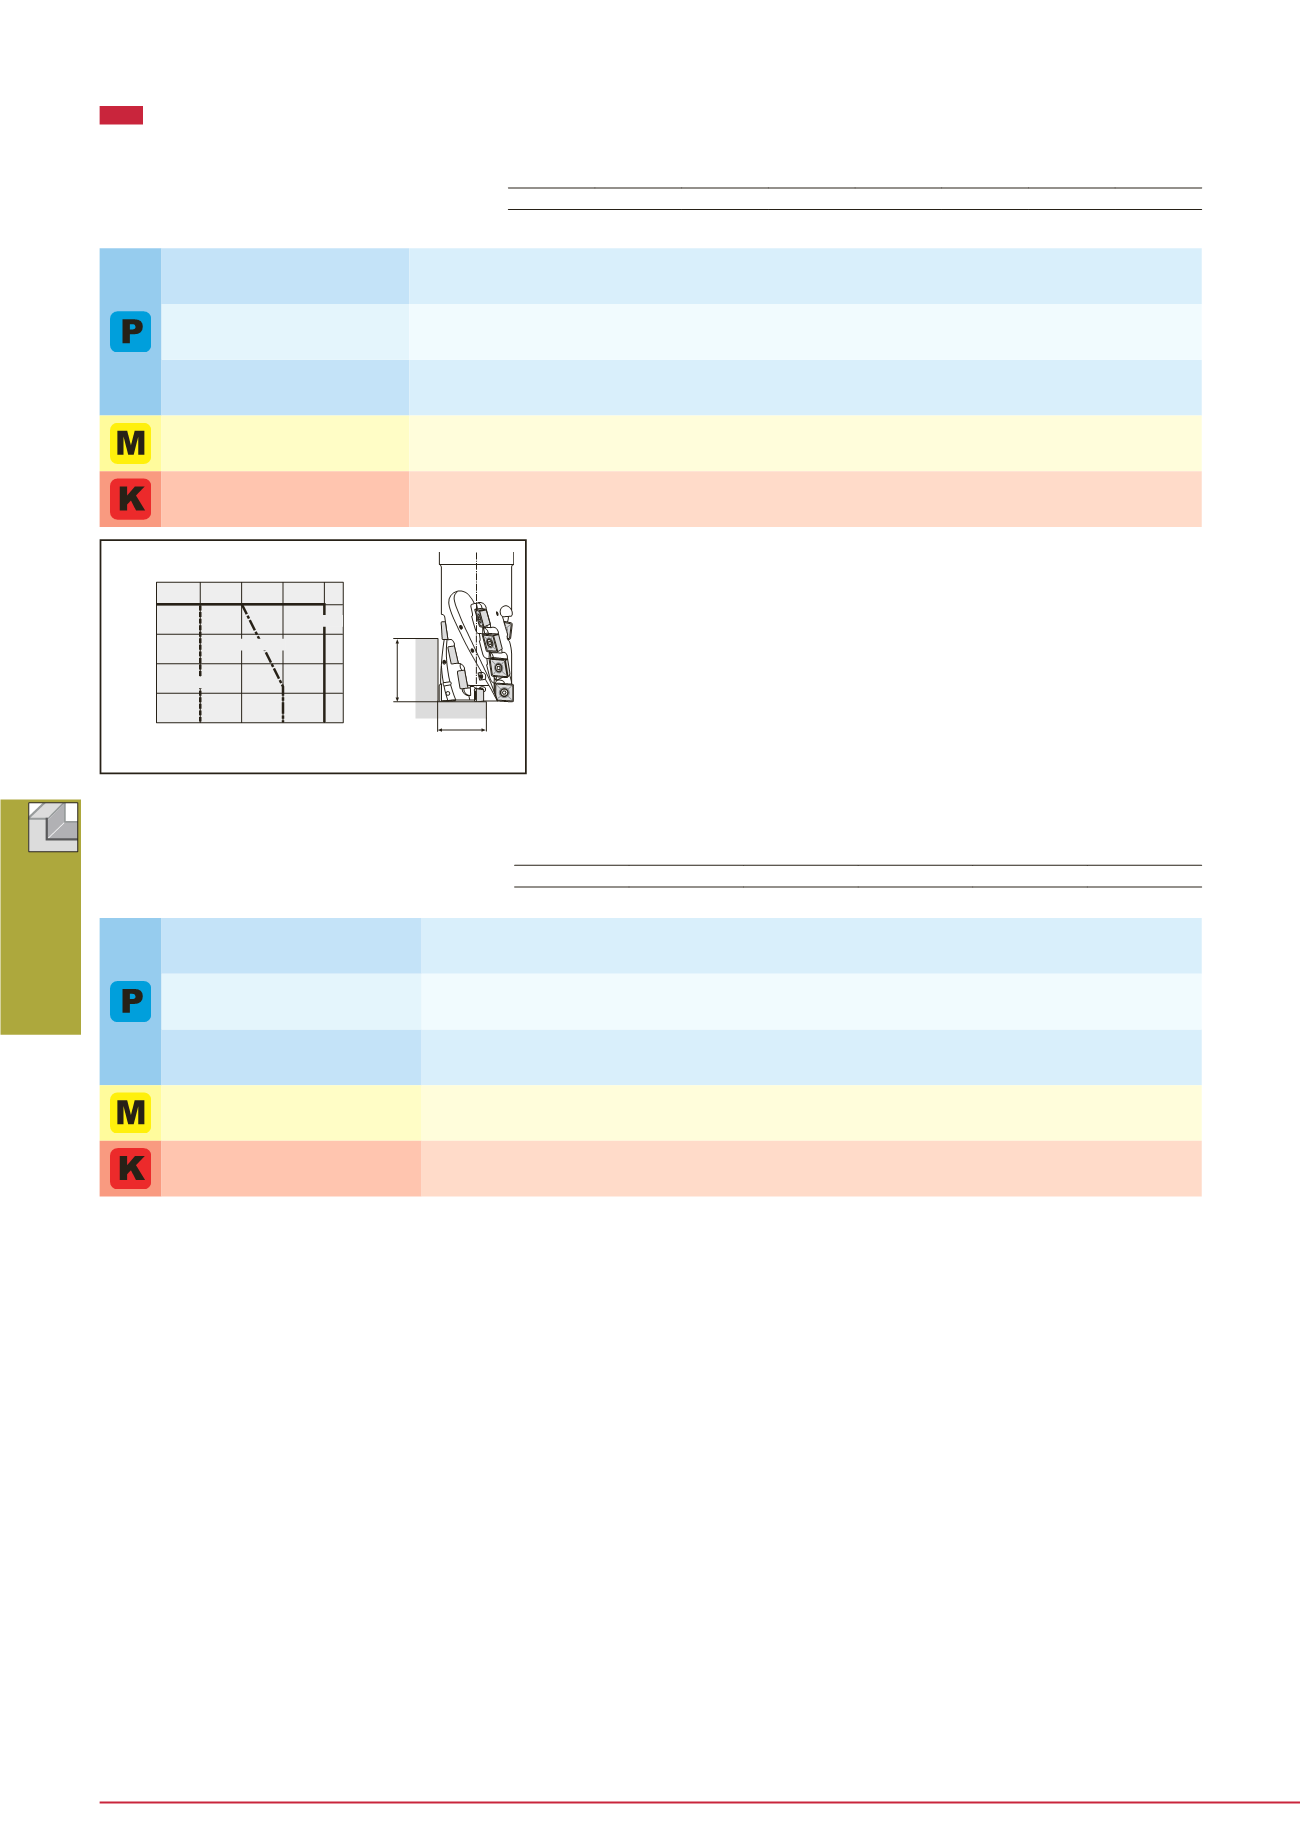
a
p
a
e
D
3D/4
D/2
D/4
0
0
D/4
D/2
3D/4
D
f
z = ~ 0.3
f
z = ~ 0.2
f
z = ~ 0.07
Cutting width (Radial depth of cut)
a
e
D: Cutter dia. (mm)
f
z: Feed per tooth (mm/t)
(Groove)
ELP t ype
a
p: Axial depth of cut
a
(mm)


