D092
Shoulder Milling
STANDARD CUTTING CONDITIONS
a
p
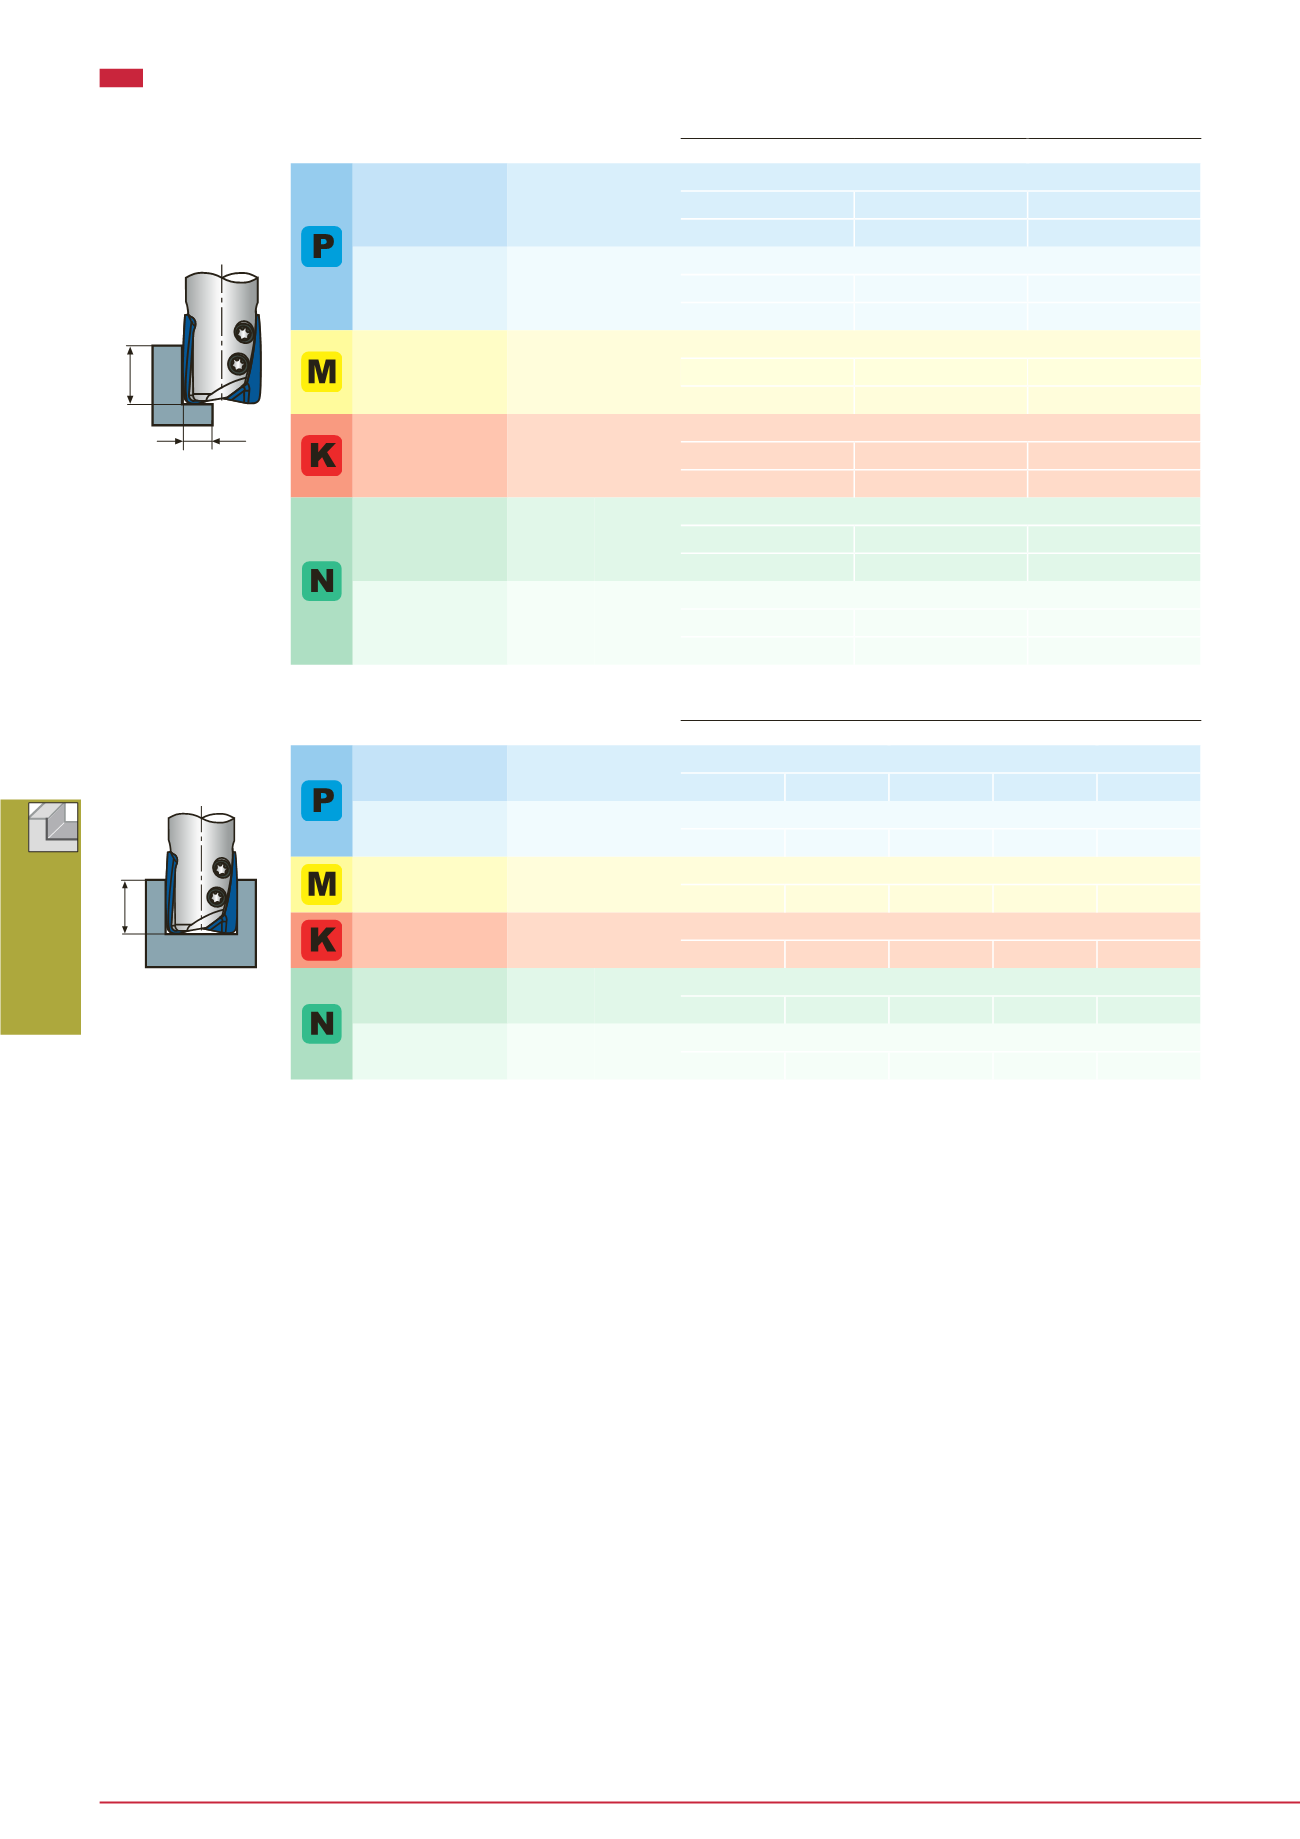
Slotting
Shoulder milling
a
p
a
e
a
p: Axial depth of cut
a
e: Radial depth of cut
≤
≤
≤
≤
≤
≤
≤
≤
≤
≤
≤
≤
≤
≤
≤
≤
≤
≤
≤
≤
≤
≤
≤
≤
≤
≤
≤
≤
≤
≤
≤
≤
≤
≤
≤
≤
≤
≤
≤
≤
Tool overhang length must be as short as possible to avoid chatter. When
the tool overhang length is long, decrease the number of revolutions and
feed.
Cutting conditions are generally limited by the rigidity and power of the
machine and the rigidity of the workpiece. When setting the conditions, start
from half of the values of the standard cutting conditions and then increase
the value gradually while making sure the machine is running normally.
Notes:
When slotting, use a rigid machine.
When chips stay in the cutting zone during slotting or pocketing, use air to remove
chips from the work area.
If chips tend to stick to the cutting edge (such as aluminium alloy machining), use a
water soluble cutting fluid.
If cutting a casting skin or heavily interrupted work surface, decrease the feed per
tooth and maximum depth of cut to 1/2 to 2/3 times the values shown in the table.
≤
≤
≤
≤
≤
≤
≤
≤
≤
≤
≤
≤
≤
≤
≤
≤
≤
≤
≤
≤
≤
≤
≤
≤
≤
≤
≤
≤
≤
≤
≤
≤
≤
≤
≤
≤
ISO Workpiece
material
Cutting
speed
Vc (m/min)
Feed
rate
fz (mm/t)
Cutting conditions
ø10 øDc < ø12 ø12 øDc < ø16 ø16 øDc ø26
Carbon steels
Alloy steels
< 30HRC
60 ~ 180 0.03 ~ 0.1
V
c = 120 m/mim,
f
z = 0.08 mm/t
ap
7.5 mm
ap
9 mm
ap
12 mm
ae
1.5 mm
ae
1.5 mm
ae
2 mm
Alloy steels
prehardened steels
30 ~ 40HRC
50 ~ 150 0.03 ~ 0.08
V
c = 100 m/min,
f
z = 0.05 mm/t
ap
5.5 mm
ap
6.5 mm
ap
9 mm
ae
1.5 mm
ae
1.5 mm
ae
2 mm
Stainless steels
< 250HB
50 ~ 150 0.03 ~ 0.06
V
c = 100 m/min,
f
z = 0.04 mm/t
a p
4.5 mm
a p
5.5 mm
ap
7.5 mm
ae
1.5 mm
ae
1.5 mm
ae 2 mm
Cast irons
80 ~ 200 0.03 ~ 0.1
V
c = 140 m/min,
f
z = 0.08 mm/t
ap
9.5 mm
ap
11.5 mm
ap
15.5 mm
ae
2 mm
ae
2 mm
ae
3 mm
Aluminium alloys
Si < 12% 100 ~ 300 0.03 ~ 0.1
V
c = 200 m/min,
f
z = 0.07 mm/t
ap
9.5 mm
ap
11.5 mm
ap
15.5 mm
ae
2 mm
ae
2 mm
ae
3 mm
Aluminium alloys
Si > 13% 80 ~ 180 0.03 ~ 0.08
V
c = 130 m/min,
f
z = 0.06 mm/t
ap
9.5 mm
ap
11.5 mm
ap
15.5 mm
ae
2 mm
ae
2 mm
ae
3 mm
ISO Workpiece
material
Cutting
speed
Vc (m/min)
Feed
rate
fz (mm/t)
Cutting conditions
ø10 øDc < ø12 ø12 øDc < ø16 ø16 øDc ø18 ø18 < øDc ø21 ø21 < øDc ø26
Carbon steels
Alloy steels
< 30HRC
60 ~ 180 0.03 ~ 0.1
V
c = 100 m/mim,
f
z = 0.06 mm/t
ap 1.5 mm ap 2 mm ap 3 mm ap 2.5 mm ap 2.5 mm
Alloy steels
prehardened steels
30 ~ 40HRC
50 ~ 150 0.03 ~ 0.08
V
c = 70 m/min,
f
z = 0.05 mm/t
ap 1 mm ap 1.5 mm ap 2 mm ap 1.5 mm ap 1.5 mm
Stainless steels
< 250HB
50 ~ 150 0.03 ~ 0.06
V
c = 70 m/min,
f
z = 0.04 mm/t
ap 1 mm ap 1 mm ap 1.5 mm ap 1.5 mm ap 1.5 mm
Cast irons
80 ~ 200 0.03 ~ 0.1
V
c = 120 m/min,
f
z = 0.07 mm/t
ap 3.5 mm ap 4 mm ap 4.5 mm ap 3.5 mm ap 3 mm
Aluminium alloys
Si < 12% 100 ~ 300 0.03 ~ 0.1
V
c = 150 m/min,
f
z = 0.07 mm/t
ap 3.5 mm ap 4 mm ap 4.5 mm ap 3.5 mm ap 3 mm
Aluminium alloys
Si > 13% 80 ~ 180 0.03 ~ 0.08
V
c = 110 m/min,
f
z = 0.06 mm/t
ap 3.5 mm ap 4 mm ap 4.5 mm ap 3.5 mm ap 3 mm


