E023
Tungaloy
3
2
1
0
26
30
35
41
30
20
10
0
26
30
35
41
2-e ective Drill
ISO
ø26 - ø29.9 ø30 - ø35.9
ø36 - ø41
80 - 140
0.2 - 0.5
0.2 - 0.5
0.2 - 0.55
80 - 130
0.2 - 0.5
0.2 - 0.5
0.2 - 0.55
50 - 100
0.2 - 0.5
0.2 - 0.5
0.2 - 0.55
40 - 80
0.15 - 0.3
0.15 - 0.3
0.2 - 0.35
80 - 180
0.25 - 0.55
0.25 - 0.55
0.3 - 0.6
80 - 140
0.25 - 0.55
0.25 - 0.55
0.3 - 0.6
100 - 200
0.4 - 0.6
0.4 - 0.6
0.5 - 0.7
20 - 50
0.1 - 0.2
0.1 - 0.2
0.1 - 0.25
30 - 60
0.1 - 0.3
0.1 - 0.3
0.1 - 0.35
20 - 60
0.1 - 0.2
0.1 - 0.2
0.1 - 0.25
STANDARD CUTTING CONDITIONS
Workpiece material
Cutting speed
V
c (m/min)
Low carbon steels
C15, C20, etc.
Carbon steels, Alloy steels
C55, 42CrMoS4, etc.
Prehardened steels
NAK80, PX5, etc.
Stainless steels
X5CrNi18-9, X5CrNiMo17-12-2, etc
Grey cast irons
250, 300, etc.
Heat-resistant alloy
Inconel718, etc.
Titanium alloys
Ti-6Al-4V, etc.
Hardened materials
Ductile cast irons
400-15, 600-3, etc.
Non ferrous materials
Feed:
f
(mm/rev)
ø
D
c (mm)
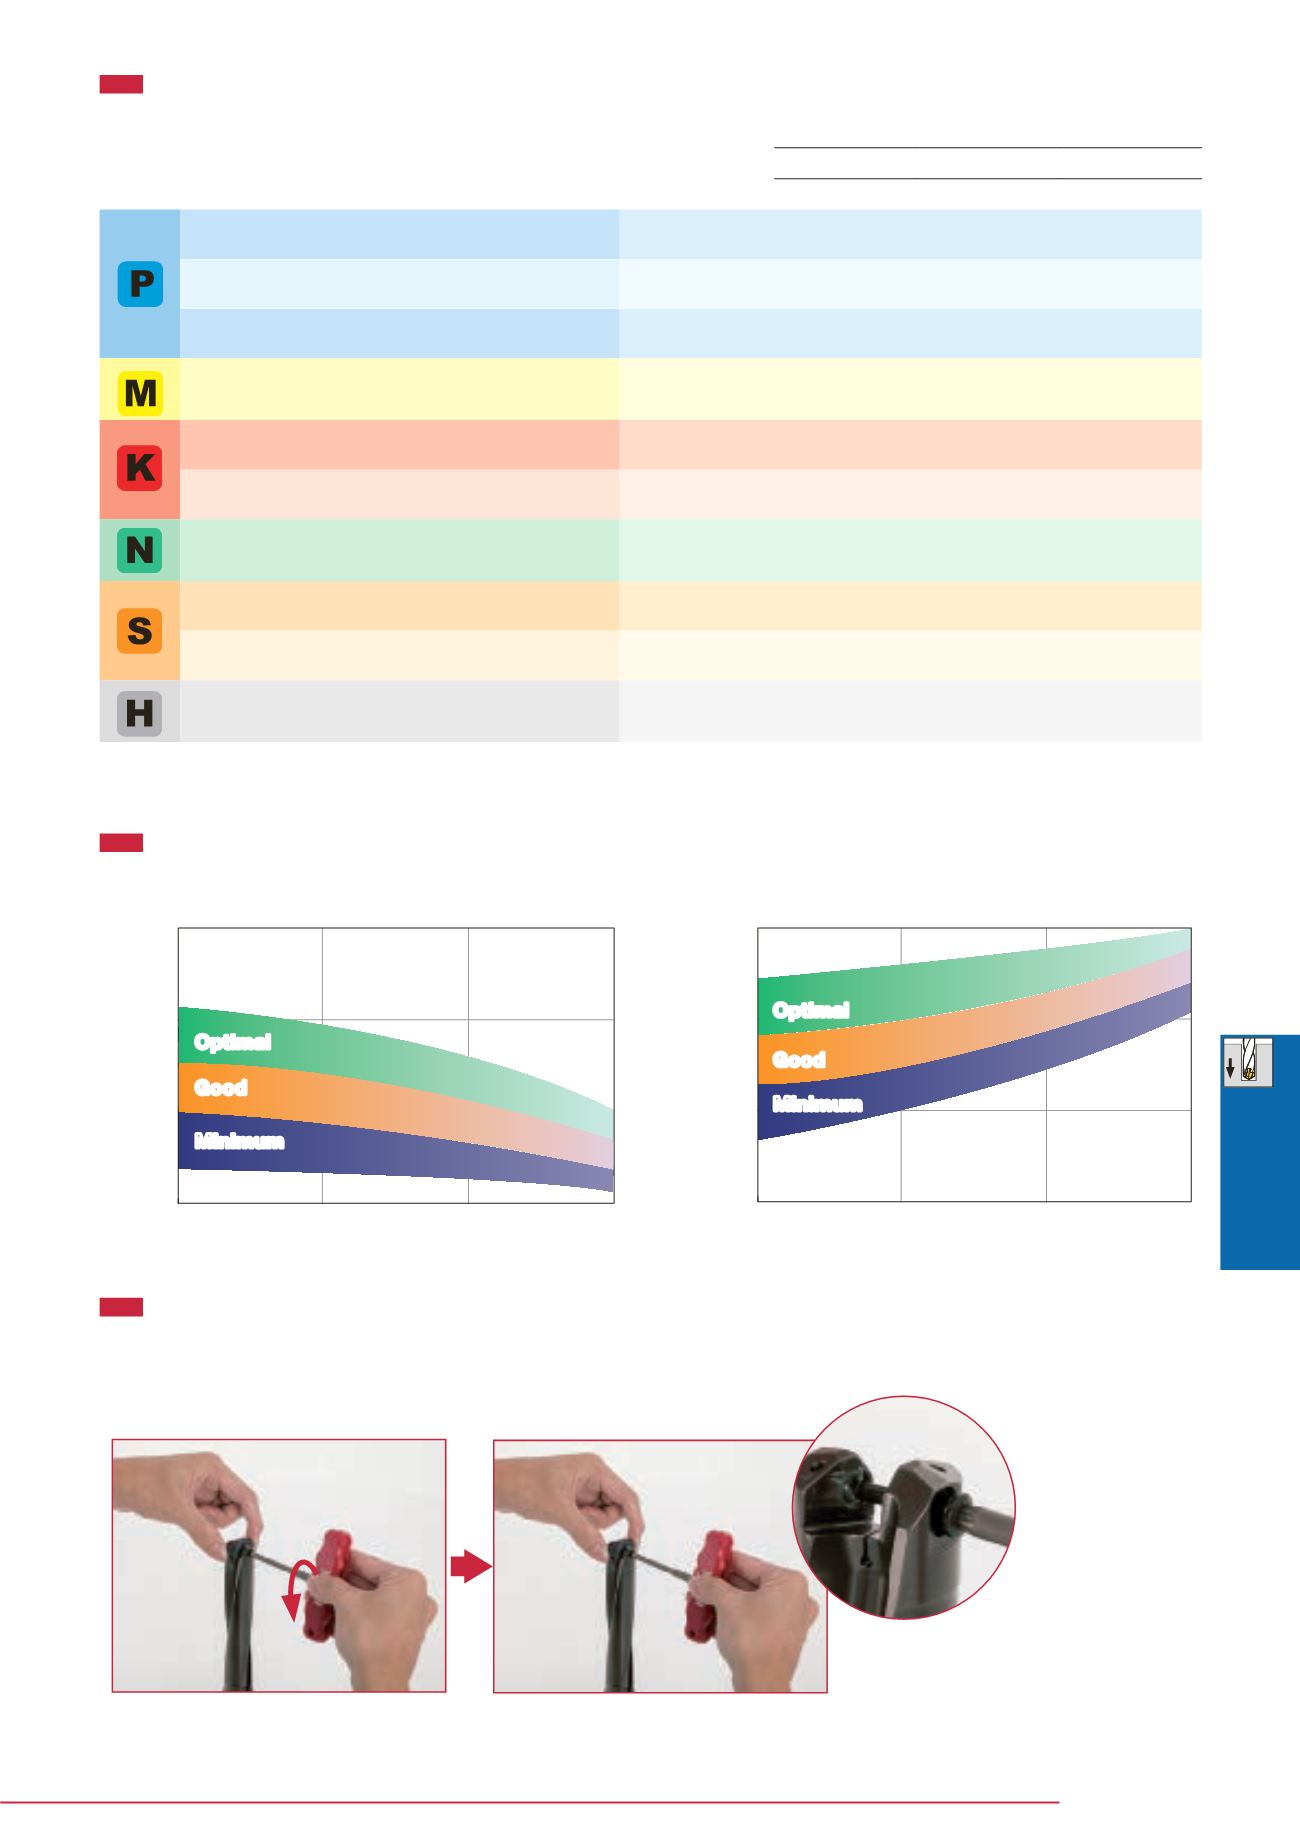
RECOMMENDED COOLANT PRESSURE AND VOLUME
Coolant pressure (MPa)
Coolant volume (l/min)
Drill diameter: øDc (mm)
Drill diameter: øDc (mm)
Optimal
Optimal
Good
Good
Minimum
Minimum
- Please change the screw to new one when the screw does not rotate smoothly
HOW TO CHANGE DRILL HEAD
To unclamp rotate the screw 3-5
times counter-clockwise.
No need to remove the screw from
the body.


