D256
Multi Function
STANDARD CUTTING CONDITIONS
APPLICATION RANGE
Note:
• In slotting or pocketing where chips tend to stay in the cutting zone, use
an air blast to remove chips to prevent chip recutting.
• When chips tend to weld excessively on the cutting edge such as in ma-
chining aluminium alloys, use a water soluble cutting fluid.
• In the case of cutting a casting skin or a heavily interrupted work surface,
decrease the feed per tooth and the maximum depth of cut to 1/2 to 2/3
times the values shown in the table.
• Tool overhang length must be as short as possible to avoid chatter. When
the tool overhang length is long, decrease the number of revolutions and
feed.
• Cutting conditions are generally limited by the rigidity and power of the
machine and the rigidity of the workpiece. When setting the conditions,
start from half of the values of the standard cutting conditions and then
increase the value gradually whilst making sure that the machine is running
normally.
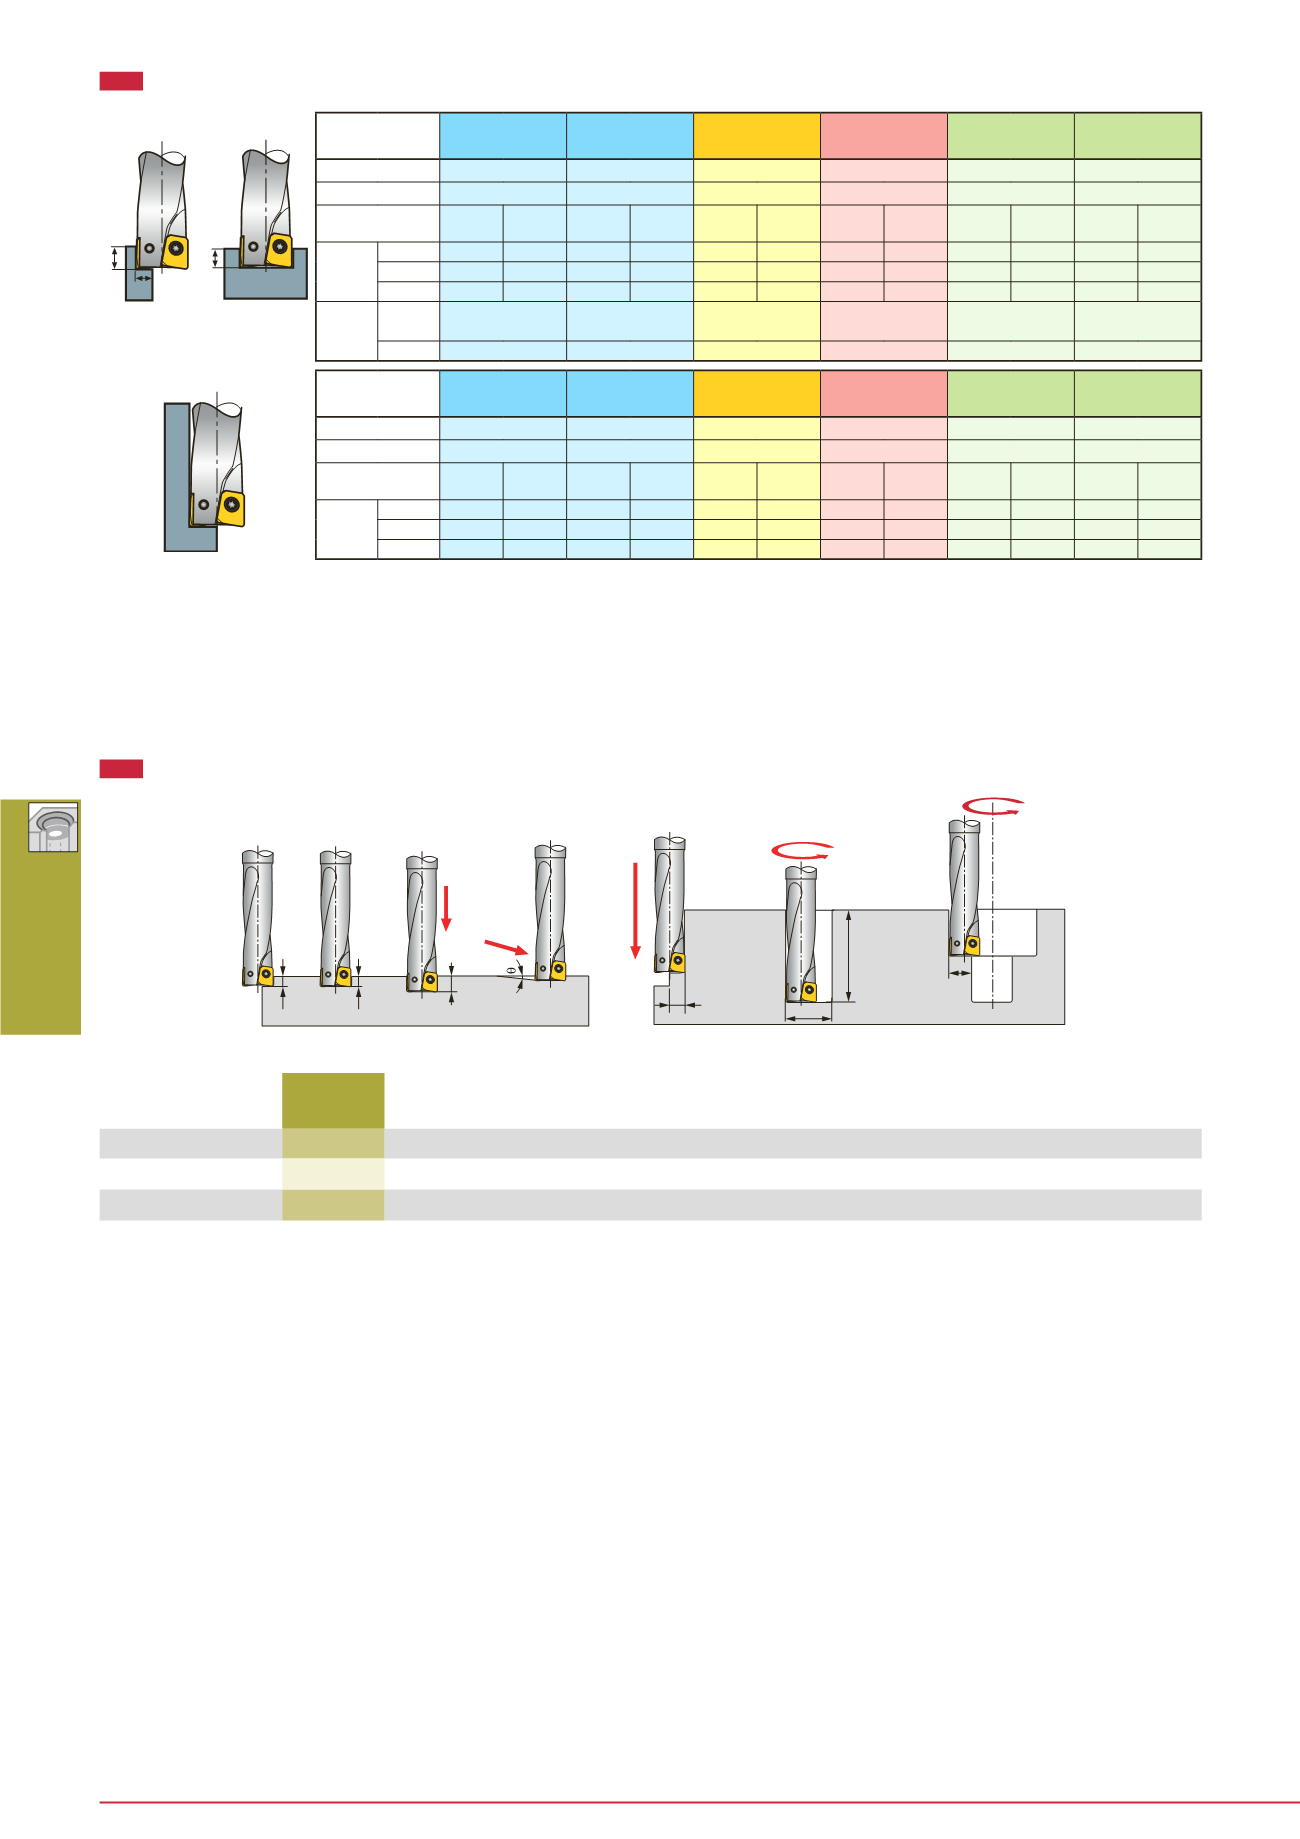
a
p
a
p
a
e
a
p
: Axial depth of cut
a
e
: Radial depth of cut
Side cutting Slotting
Shoulder milling
,
Slotting
Drilling
•
Plunging
< 30HRC
30 ~ 40HRC
< 250HB
-
-
-
V
c = 50 ~ 120 m/min
V
c = 30 ~ 100 m/min
V
c = 50 ~ 120 m/min
V
c = 60 ~ 140 m/min
V
c = 100 ~ 300 m/min
V
c = 100 ~ 200 m/min
2550 380 1910 190 2550 380 3180 510 6370 1020 4770 670
2120 320 1590 160 2120 320 2650 420 5300 850 3980 560
1590 240 1190 120 1590 240 1990 320 3980 640 2980 420
a
p
< 0.25D
a
e
< 0.2D
a
p
< 0.25D
a
e
< 0.2D
a
p
< 0.25D
a
e
< 0.2D
a
p
< 0.25D
a
e
< 0.3D
a
p
< 0.25D
a
e
< 0.3D
a
p
< 0.25D
a
e
< 0.3D
a
p
< 0.1D
a
p
< 0.1D
a
p
< 0.1D
a
p
< 0.15D
a
p
< 0.2D
a
p
< 0.2D
< 30HRC
30 ~ 40HRC
< 250HB
-
-
-
V
c = 50 ~ 120 m/min
V
c = 30 ~ 100 m/min
V
c = 50 ~ 120 m/min
V
c = 60 ~ 140 m/min
V
c = 100 ~ 300 m/min
V
c = 100 ~ 300 m/min
2550 130 1910 80 2550 130 3180 190 6370 450 4770 290
2120 110 1590 65 2120 110 2650 160 5300 370 3980 240
1590 80 1190 50 1590 80 1990 120 3980 280 2980 180
Workpiece
material
Carbon steels and
alloy steels
Alloy steels and
prehardened
steelst
Stainless steels Cast irons
Aluminium alloys
(Si
<
13%)
Aluminium alloys
(Si
≥
13%)
Hardness
Cutting speed
Conditions
No. of rev.
n
min
-1
v
f
mm/min
No. of rev.
n
min
-1
v
f
mm/min
No. of rev.
n
min
-1
v
f
mm/min
No. of rev.
n
min
-1
v
f
mm/min
No. of rev.
n
min
-1
v
f
mm/min
No. of rev.
n
min
-1
v
f
mm/min
Tool dia.
(mm)
ø10
ø12
ø16
Depth of
cut
Side
cutting
Slotting
Workpiece
material
Carbon steels and
alloy steels
Alloy steels and
prehardened
steelst
Stainless steels Cast irons
Aluminium alloys
(Si
<
13%)
Aluminium alloys
(Si
≥
13%)
Hardness
Cutting speed
Conditions
No. of rev.
n
min
-1
v
f
mm/min
No. of rev.
n
min
-1
v
f
mm/min
No. of rev.
n
min
-1
v
f
mm/min
No. of rev.
n
min
-1
v
f
mm/min
No. of rev.
n
min
-1
v
f
mm/min
No. of rev.
n
min
-1
v
f
mm/min
Tool dia.
(mm)
ø10
ø12
ø16
Feed
speed
Feed
speed
Feed
speed
Feed
speed
Feed
speed
Feed
speed
Feed
speed
Feed
speed
Feed
speed
Feed
speed
Feed
speed
Feed
speed
Ramping
Plunging
H
Drilling
W
H1
°
a
p
a
p
Shoulder
milling
Slotting
a
e
ø
D
1,
ø
D
2
Enlarging hole
Drilling
(Helical feed)
Tool dia.
Max. depth
of cut
Max.drilling
depth
Max.cutting
width in plunging
Max. ramping
angle
Min. machinable
hole dia.
Min. machinable
hole dia.
Max. cutting width
in enlarging hole
Max.depth
of boring
Designation
ap
(mm)
H (mm)
W (mm)
θ°
øD1(mm) øD2 (mm)
ae
(mm)
H1 (mm)
EVH06R010M10.0-02
ø10
3
5
5
5
12
19
9
30
EVH07R012M12.0-02
ø12
3.5
6
6
5
14
23
11
36
EVH09R016M16.0-02
ø16
4.5
8
8
5
18
31
15
48


