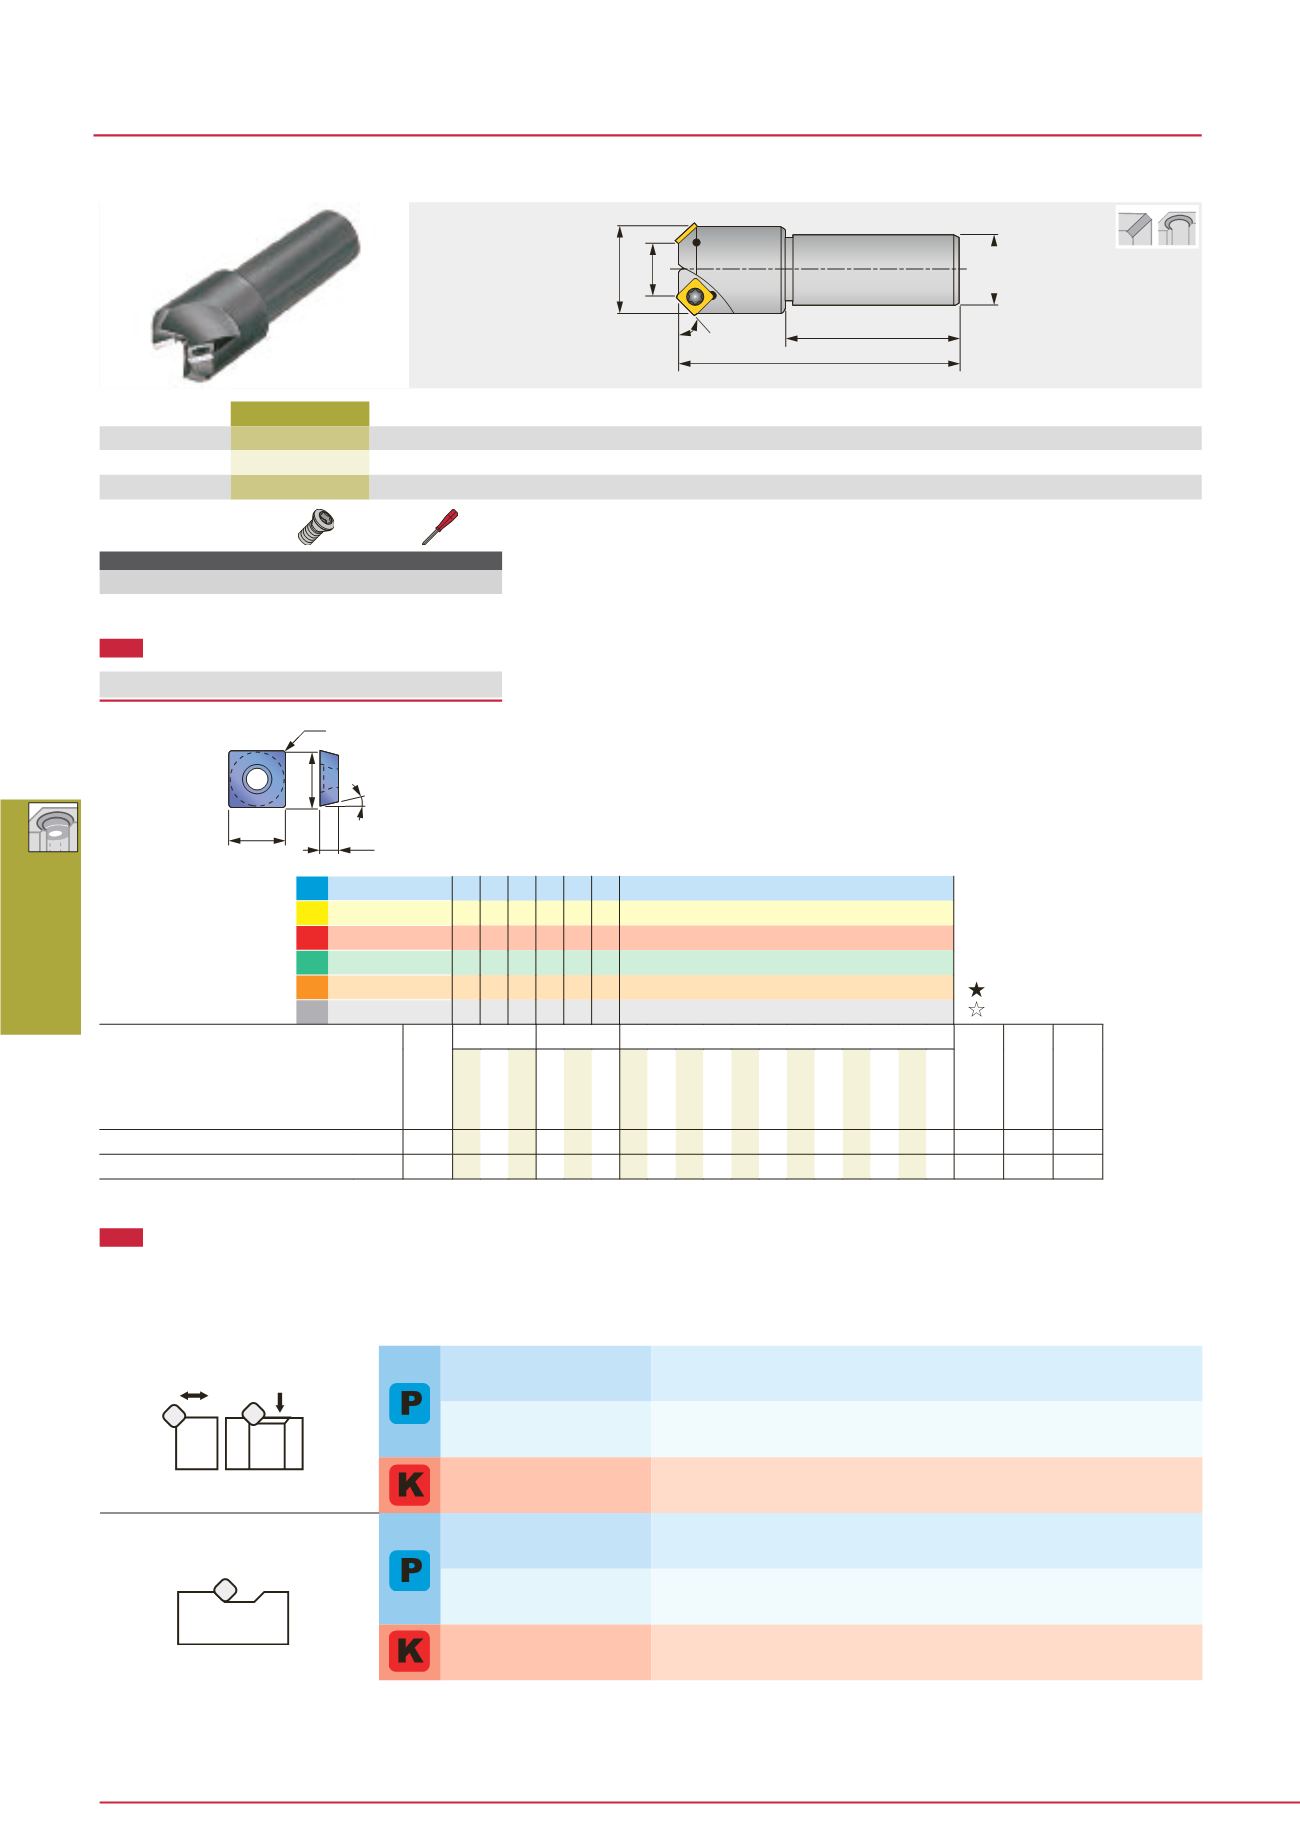
D262
Multi Function
øD
1
øDc
45˚
L
R
s
øDs
h6
Designation
øD
c
z
øD
1
øD
s
L
ℓ
s
Insert
ECP440AR
10
1
27.5
32
130
80
SPMA422*N
ECP4423R
23
2
40.3
32
130
80
SPMA422*N
ECP4436R
36
3
53.3
32
130
80
SPMA422*N
SPARE PARTS
Designation
Clamping screw Wrench
ECP44...
CSTA-4
T-15D
ECP4400R
Indexable chamfering cutter with square insert
SPMA42
T
B
A
r
ε
11°
INSERT
STANDARD CUTTING CONDITIONS
Notes:
• When chamfering stainless steel, down-milling is recommended. Conventional milling may cause edge chipping.
• When chamfering above C3.0, the feed per tooth should be set up the lower side of the value shown in the above table.
P Steel
M Stainless
K Cast iron
N Non-ferrous
S Superalloys
H Hard meterials
Designation
r
ε
Cermet Uncoated
A B T
NS740
N308
UX30
TH10
SPMA422TN
0.8
l l l
12.7 12.7 3.18
SPMA422FN
0.8
l
12.7 12.7 3.18
l
: Line-up
: First choice
: Second choice
Operations
Workpiece material
Grade
Cutting speed
Vc (m/min)
Maximum
depth of cut
ap (mm)
Feed per tooth
fz (mm/t)
Carbon steels, Alloy steels
< 300HB
NS740
·
N308
UX30
100 - 150
-
0.2 - 0.5
Die steels
< 30HRC
NS740
·
N308
UX30
50 - 70
-
0.15 - 0.4
Cast irons
TH10
90 - 110
-
0.2 - 0.6
Carbon steels, Alloy steels
< 300HB
NS740
·
N308
UX30
100 - 150
3
0.1 - 0.15
Die steels
< 30HRC
UX30
50 - 70
2
0.1 - 0.15
Cast irons
TH10
90 - 110
3
0.1 - 0.15
Single or double chamfering hole chamfering
Facing Grooving


