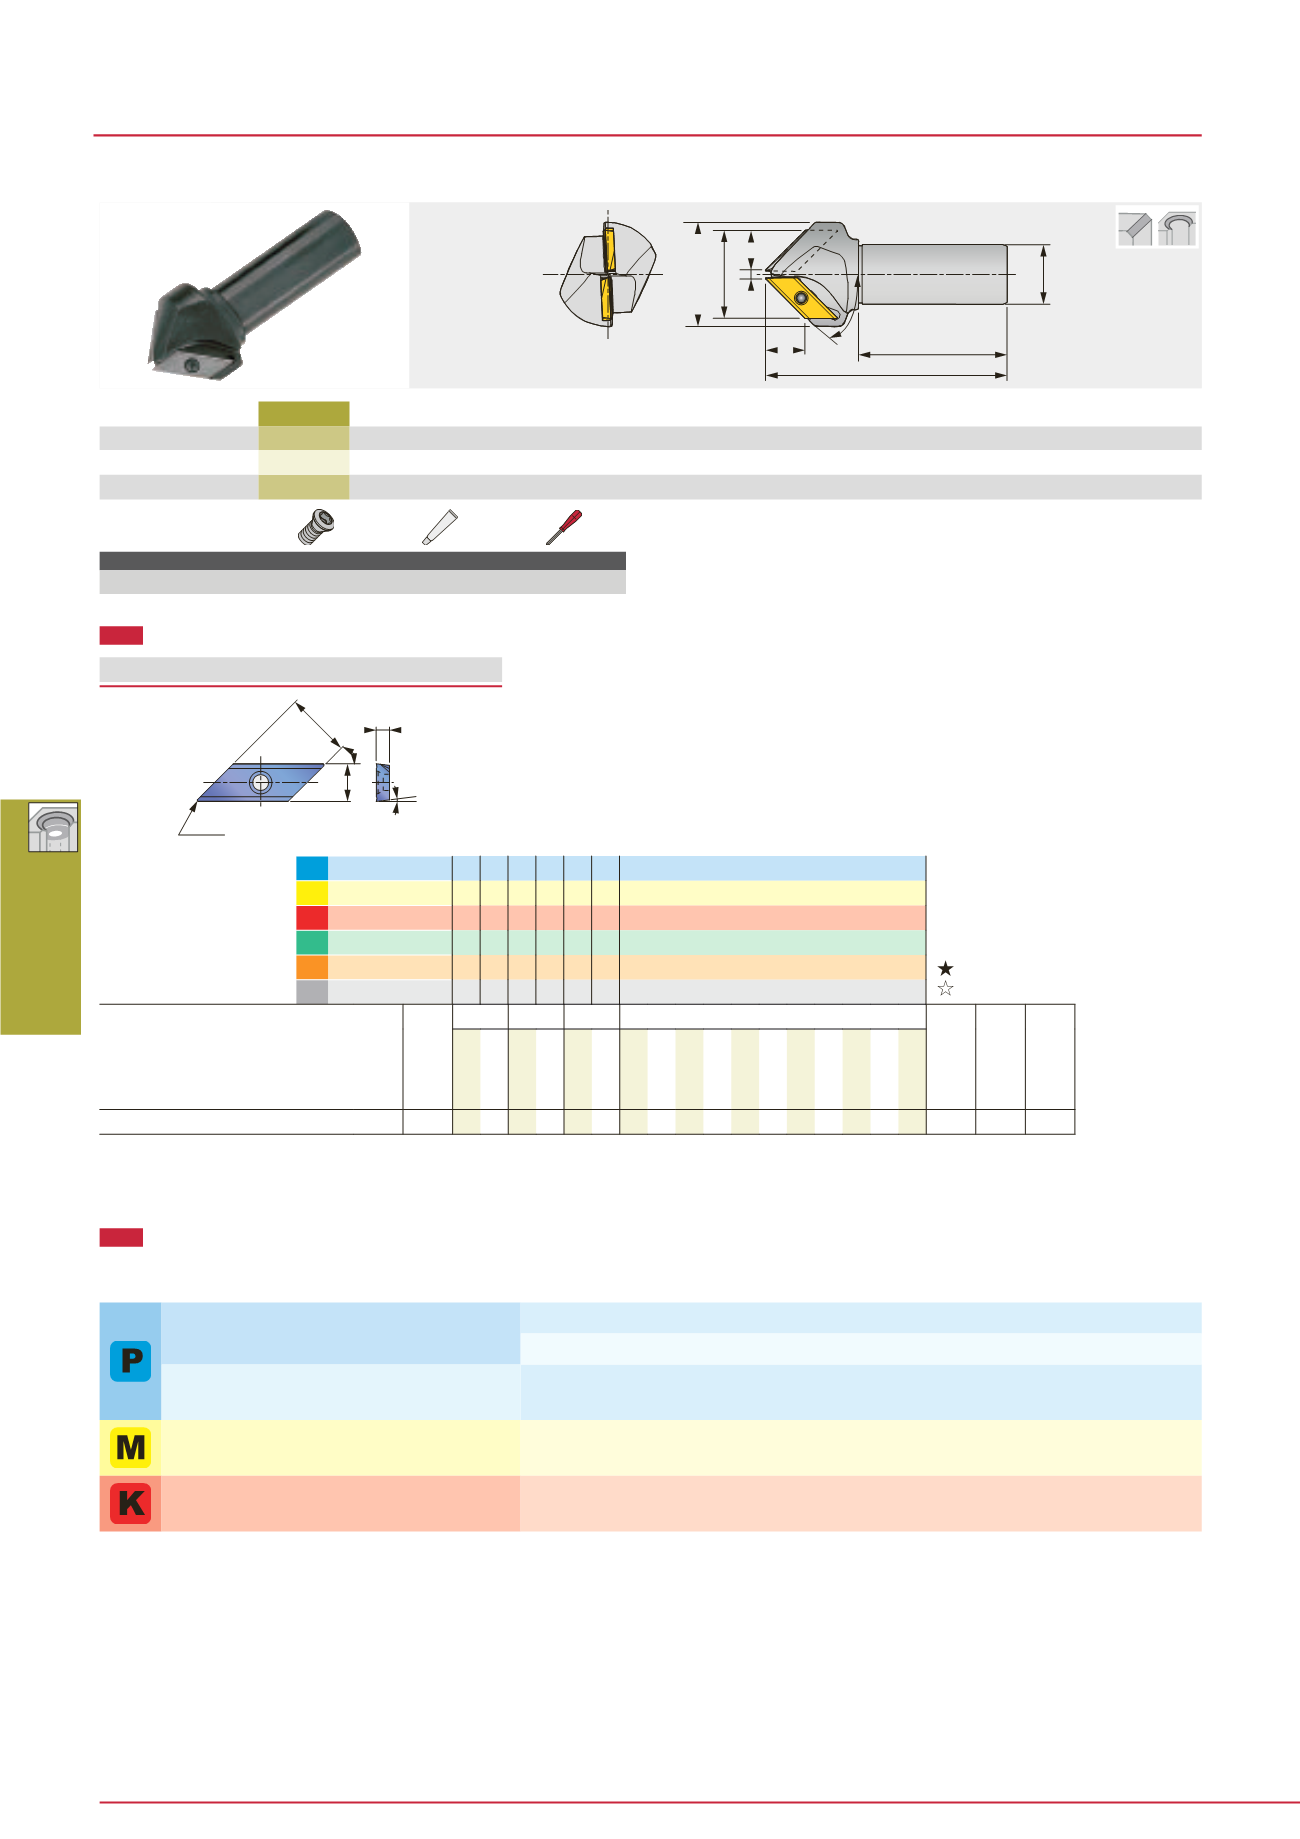
D260
Multi Function
Notes:
• When the hole diameter to be chamfered is small or the cutting edges near
the front end of tool are used, use at higher side of the revolution range
shown in the Table.
In contrast, when the hole diameter to be chamfered is large or the cutting
edges far from the tool's front end are used, use the lower side of the revo-
lution range shown in the Table.
• When chamfering a small diameter hole (smaller than ø10 mm) in a plunge-
milling mode, peck-feeding should not be used.
• When the hole diameter to be chamfered is smaller than ø10 mm or the
cutting edges near the tool's front end are used, the feed should be set
within 0.15 mm/t.
øD
1
B
A
ø5
ø32
h6
κ˚
øDc
L
R
s
Designation
øD
c
z
κ
°
øD
1
A
B
øD
s
ℓ
s
L
Insert
ECC31005R-30
34
1
30
40
14.5
25.5
32
80
130.2
XCET3104...
ECC31005R-45
46
2
45
56
20.5
20.5
32
80
130.1
XCET3104...
ECC31005R-60
55
2
60
72
25.5
14.5
32
80
130.1
XCET3104...
SPARE PARTS
Designation
Clamping screw Lubricant
Wrench
ECC31
...
CSTB-5S
M-1000
T-20D
ECC31
Indexable chamf
e
ring cutter with large parallelogram insert
XCET31
45°
A
B
T
7°
2-
r
ε
INSERT
P Steel
M Stainless
K Cast iron
N Non-ferrous
S Superalloys
H Hard meterials
Designation
r
ε
Coating Cermet
Un-
coated
A B T
AH330
NS740
UX30
XCET310404ER
0.4
l l l
22 12.7 4.5
l
: Line-up
: First choice
: Second choice
STANDARD CUTTING CONDITIONS
ISO
Workpiece material
Grade
No. of revolutions: n (min
-1
)
Feed per tooth
:
fz (mm/t)
Carbon steels C55, etc.
Alloy steels 42CrMo4, etc. < 300 HB
NS740
1000
-
3000
-
7000
0.1
-
0.25
UX30
700
- 2000
-
4900
0.1
-
0.25
Die steels
X40CrMoV5-1, etc. < 300 HB
AH330
1000
-
3000
- 7000
0.1
-
0.2
Stainless steels
X5CrNi18-10, etc. < 250 HB
AH330
1000
- 3000
- 7000
0.1
-
0.25
Cast irons 250, etc.
AH330
1000
- 3000
-
7000
0.1
-
0.25


