B014
Tur n
L i ne -
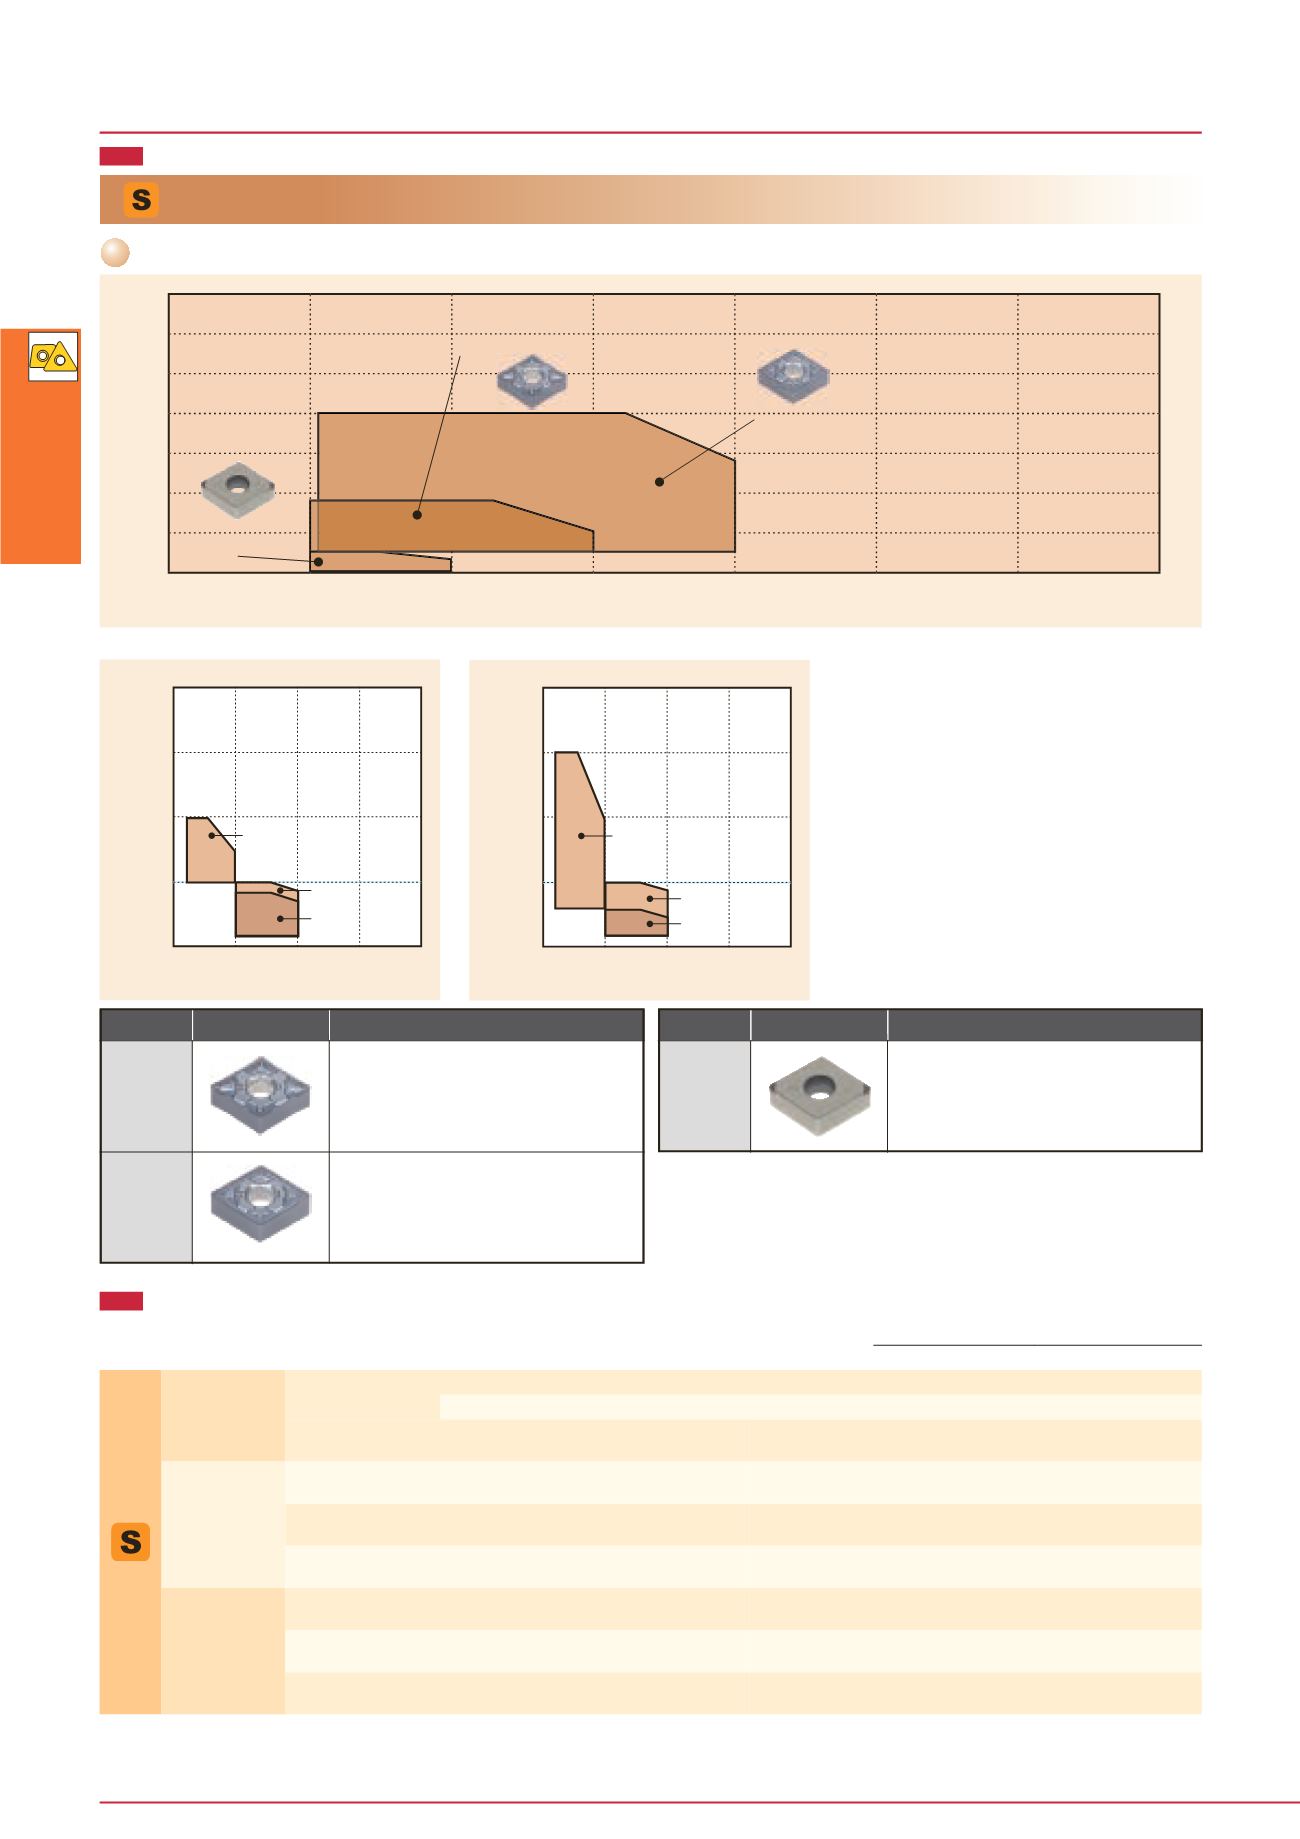
Ch i pbreaker Gu i de
BX950
BX480
AH8015
AH8005
BX950
M714B
AH8015
AH8005
Chipbreaker
Chipbreaker
Appearance
Appearance
Features
Features
T-CBN inserts.
Performs well in finishing of heat-resistant
or titanium alloys.
Suitable for finishing operation of
superalloys. Special protrusion provides
excellent chip control in lower depth of
cut.
The 1st recommended chipbreaker for
supperalloy turning. Optimized geometry
provides stable chip control in various
depth of cut.
Superalloys and titanium
Chipbreaker System for Turning (Negative Inserts)
Titanium alloys
Ni-base alloys
Depth of cut:
a
p (mm)
Feed:
f
(mm/rev)
Feed:
f
(mm/rev)
Feed:
f
(mm/rev)
Cutting speed:
V
c (m/min)
Cutting speed:
V
c (m/min)
No
chip-
breaker
BASIC CHIPBREAKERS: NEGATIVE INSERTS
Ni-base alloys: INCONEL718, etc.
Titanium alloys: Ti-6Al-4V, etc
ISO Operation Work condition Chip-
breaker
Grade Depth of cut
a
p (mm)
Feed
f
(mm/rev)
Cutting speed:
V
c (m/min)
Titanium alloys Ni-base alloys
Precision
finishing
Continuous
Without
BX950
0.1 - 0.5
0.05 - 0.2
100 - 200
70 - 300
Without
M714B
0.1 - 0.5
0.05 - 0.2
-
70 - 400
Light interrupted Without
BX480
0.1 - 0.5
0.05 - 0.2
100 - 200
-
Finishing
Continuous
HRF
AH8005
0.5 - 1.5
0.05 - 0.25
20 - 100
20 - 100
Light interrupted
HRF
AH8015
0.5 - 1.5
0.05 - 0.25
20 - 80
20 - 50
Heavy interrupted
HRF
AH8015
0.5 - 1.5
0.05 - 0.25
10 - 60
10 - 40
Finishing to
Medium cutting
Continuous
HRM AH8005
0.5 - 4.0
0.1 - 0.4
20 - 100
20 - 100
Light interrupted
HRM AH8015
0.5 - 4.0
0.1 - 0.4
20 - 80
20 - 50
Heavy interrupted
HRM AH8015
0.5 - 4.0
0.1 - 0.4
10 - 60
10 - 40
STANDARD CUTTING CONDITIONS
0.2 0.4 0.6 0.8
100
200
300
400
0.2 0.4 0.6 0.8
100
200
300
400
(T-CBN)
HRM
HRF
BX950
BX480
T-CBN
7
6
5
4
3
2
1
0
0.1
0.2
0.3
0.4
0.5
0.6
0.7
AH8015
AH8005
AH8015
AH8005
HRF
HRM
Insert


