B006
Tur n
L i ne -
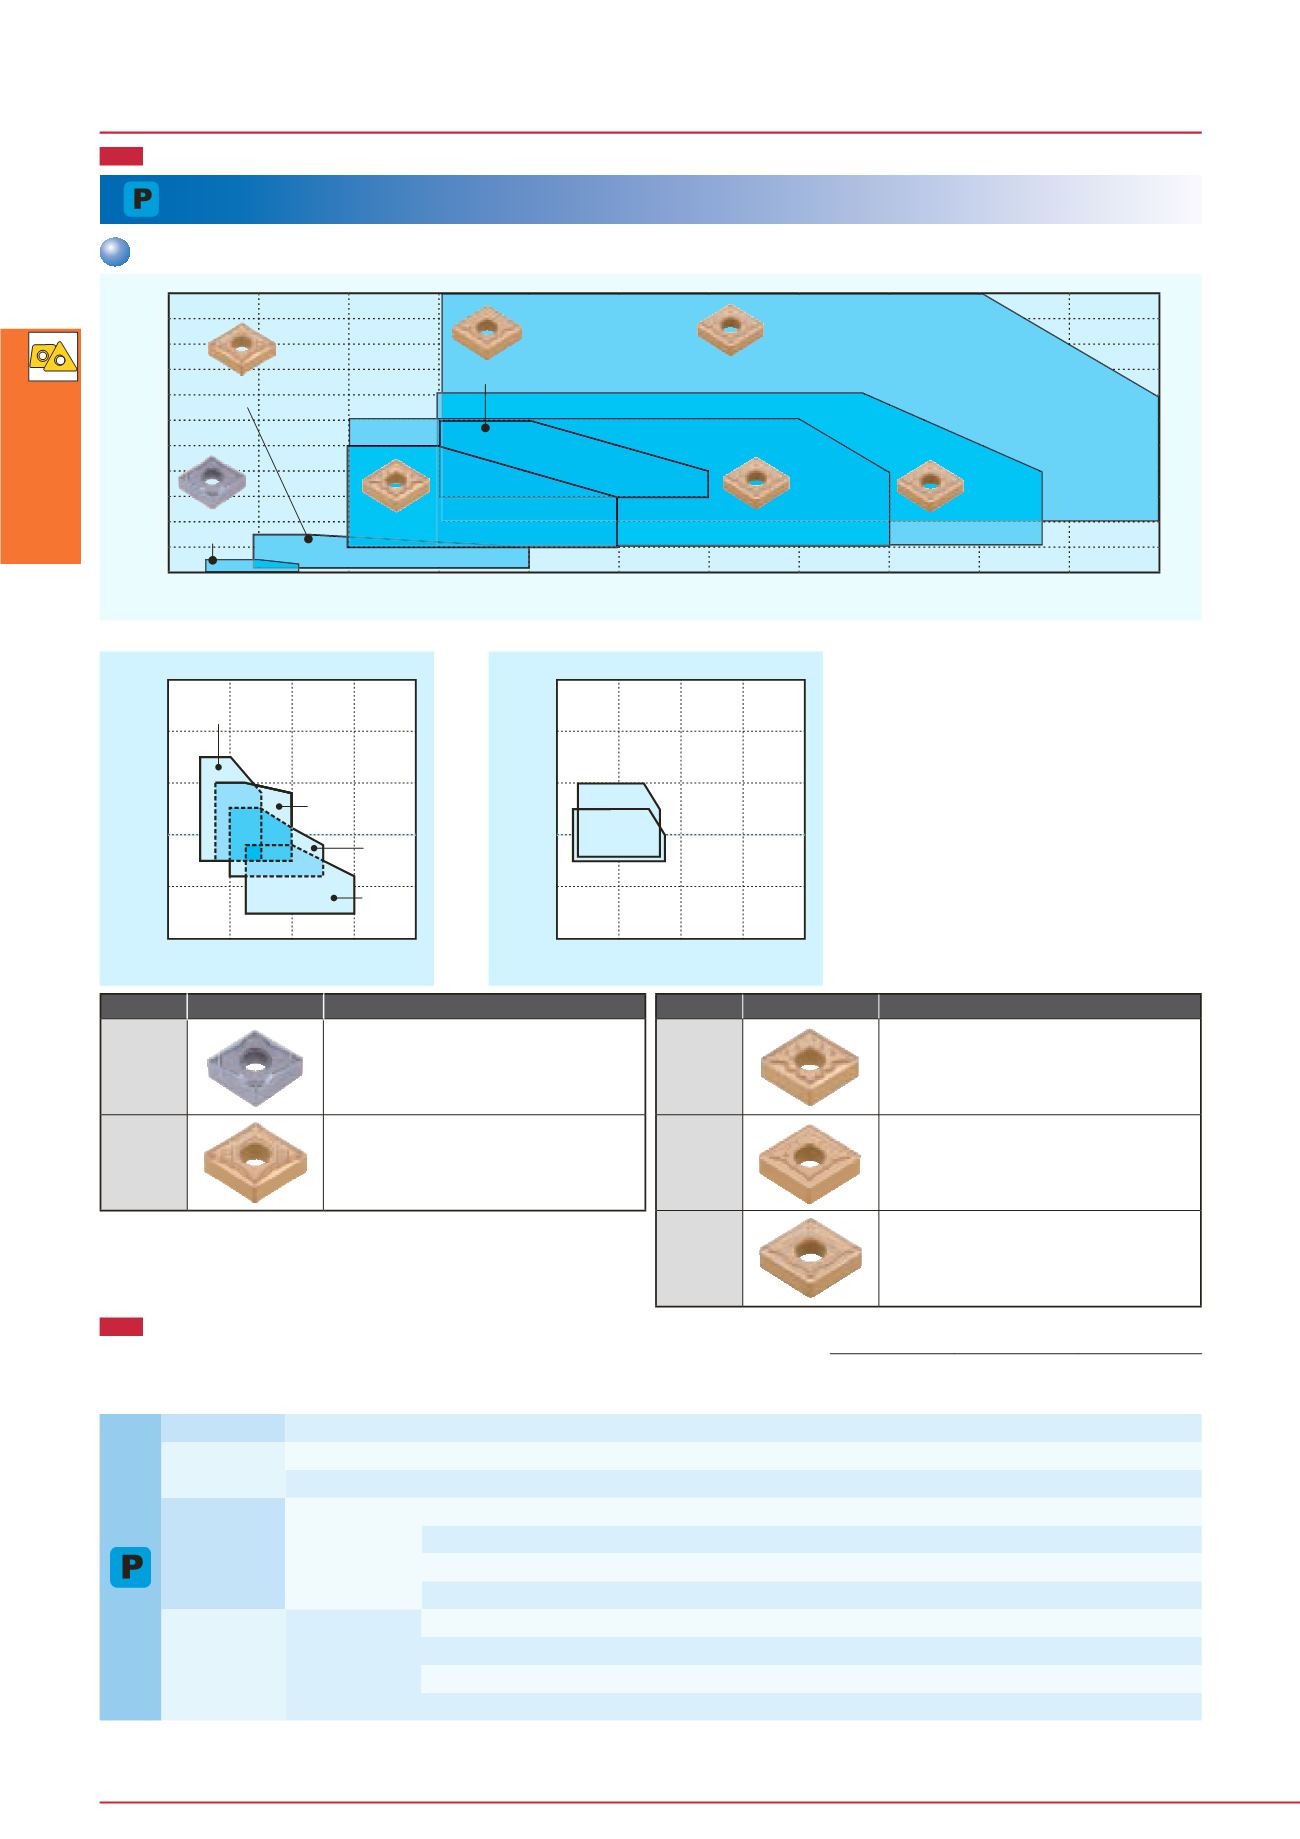
Ch i pbreaker Gu i de
TF
TSF
TM
TH
THS
GT9530
NS9530
T9125
T9115
T9135
T9105
BASIC CHIPBREAKERS: NEGATIVE INSERTS
Chipbreaker
Appearance
Features
Chipbreaker
Appearance
Features
Steel
Chipbreaker System for Turning (Negative Inserts)
CVD coated grades
Coated cermets / Cermets
Depth of cut:
a
p (mm)
Feed:
f
(mm/rev)
Feed:
f
(mm/rev)
Feed:
f
(mm/rev)
Cutting speed:
V
c (m/min)
Cutting speed:
V
c (m/min)
The sharp cutting edge and raised
projection near corner contribute to
excellent chip control at very small depths
of cut and low feeds.
Economical M-class tolerance and low
cost.
General purpose chipbreaker used for
medium cutting.
Unique chipbreaker geometry with sharp
edges and large rake angle assures free
cutting action in a wide range of cutting
conditions.
Excellent chip control in a broad range of
depth of cut.
Strong cutting edge being suitable for
interrupted and high feed operations.
Double-sided 3-dimensional chipbreaker
with a wide land and broad groove used
for medium to heavy cutting including
interruption and unfavorable surface
conditions.
Also performs well in high feed machining.
First choice chipbreaker for finishing steels.
The dimple structure decreases the contact
area between the insert surface and chips,
resulting in significant reduction of heat
occurrence.
ISO Operation Work condition Chip-
breaker
Grade Depth of cut
a
p (mm)
Feed
f
(mm/rev)
Cutting speed:
V
c (m/min)
Low carbon
steels,
Alloy steels
Medium
carbon steels,
Alloy steels
High carbon
steels,
Alloy steels
Precision finishing Continuous to light
interrupted
TF
NS9530 0.05 - 0.5 0.03 - 0.15
150 - 250
100 - 250
100 - 200
Finishing
Continuous to light
interrupted
TSF
GT9530
0.2 - 1.5
0.08 - 0.4
150 - 300
80 - 250
80 - 200
Heavy interrupted TSF
T9125
0.2 - 1.5
0.08 - 0.4
120 - 250
80 - 200
80 - 150
Medium
cutting
Continuous to
heavy interrupted
TM T9105
1.0 - 5.0
0.2 - 0.5
180 - 350
180 - 350
180 - 300
TM T9115
1.0 - 5.0
0.2 - 0.5
150 - 300
150 - 300
120 - 250
TM T9125
1.0 - 5.0
0.2 - 0.5
120 - 250
80 - 200
80 - 150
TM T9135
1.0 - 5.0
0.2 - 0.5
50 - 180
50 - 150
50 - 120
Medium
to heavy
cutting
Continuous to
heavy interrupted
TH
T9105
3.0 - 6.0
0.3 - 0.6
180 - 350
180 - 350
180 - 300
TH
T9115
3.0 - 6.0
0.3 - 0.6
150 - 300
150 - 300
120 - 250
TH
T9125
3.0 - 6.0
0.3 - 0.6
120 - 250
80 - 200
80 - 150
TH
T9135
3.0 - 6.0
0.3 - 0.6
50 - 180
50 - 150
50 - 120
Low carbon steels, Alloy steels: C10, 18CrMo4, E275A, 20Cr4, etc. Medium carbon steels, Alloy steels: C45, 42CrMo4, etc.
High carbon steels, Alloy steels: 41CrNiMo2, etc.
STANDARD CUTTING CONDITIONS
0
0.2 0.4 0.6 0.8
100
200
300
400
500
0.2 0.4 0.6 0.8
100
200
300
400
500
GT9530
NS9530
T9115
T9125
T9115
T9125
T9115
T9125
T9105
T9115
T9125
T9135
T9105
T9115
T9125
T9135
NS9530
T9105
T9115
T9125
T9135
TSF
TM
TH
12
THS
25
THS
19
THS
16
TF
11
10
9
8
7
6
5
4
3
2
1
0
0.1
0.2
0.3
0.4
0.5
0.6
0.7
0.8
0.9
1.0
1.1
Insert


