B012
Tur n
L i ne -
Ch i pbreaker Gu i de
Excels in sharpness of cutting
edges and effectively used for
machining non-ferrous metals
such as aluminium alloys and
copper alloys.
The wide chipbreaker width
contributes to excellent chip
control.
Performs well in high speed
finishing of non-ferrous materials.
With
chip-
breaker
Chip-
breaker
Appearance
Features
Non-ferrous Metal
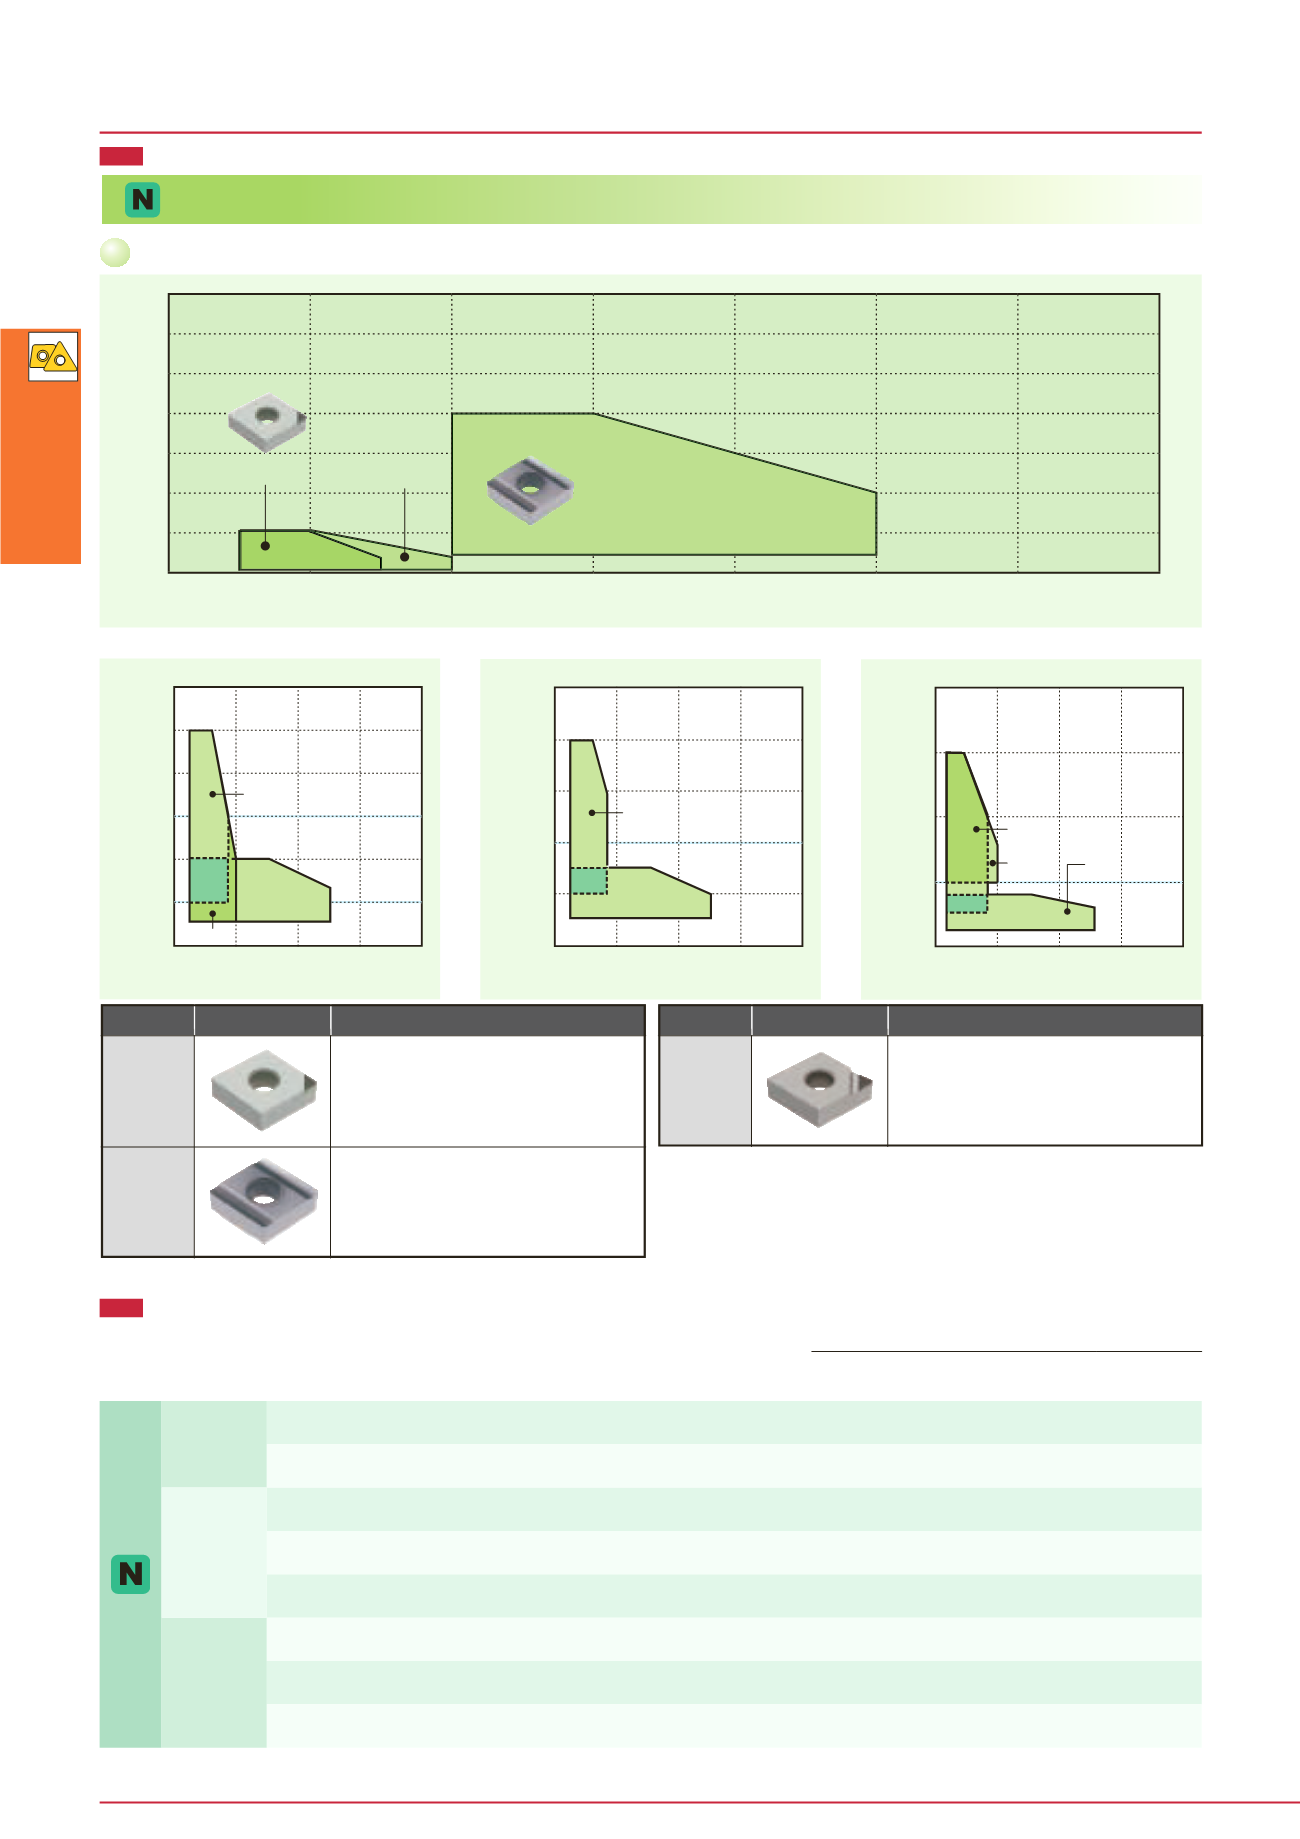
Chipbreaker System for Turning (Negative Inserts)
Chip-
breaker
Appearance
Features
Depth of cut:
a
p (mm)
Feed:
f
(mm/rev)
TH10
DX140
DX120
3000
500
1000
1500
2000
2500
0.2 0.4 0.6 0.8
Aluminium alloys (Si < 12%)
Feed:
f
(mm/rev)
Cutting speed:
V
c (m/min)
TH10
DX140
200
400
600
800
1000
0.2 0.4 0.6 0.8
Aluminium alloys (Si
≥
12%)
Feed:
f
(mm/rev)
Cutting speed:
V
c (m/min)
KS05F
DX140
DX120
0
2000
1000
0.2 0.4 0.6 0.8
Copper alloys
Feed:
f
(mm/rev)
Cutting speed:
V
c (m/min)
No
chip-
breaker
BASIC CHIPBREAKERS: NEGATIVE INSERTS
Cutting speed:
V
c (m/min)
ISO Operation
Work
condition
Chip-
breaker
Grade Depth of cut
a
p (mm)
Feed
f
(mm/rev)
Aluminium alloys
(Si < 12%)
Aluminium alloys
(Si > 12%)
Copper
alloys
Precision
finishing
Continuous
With
DX120
0.05 - 1.0 0.05 - 0.15
500 - 2500
400 - 800
500 - 1500
Light
interrupted
Without
DX140
0.05 - 1.0 0.05 - 0.20
300 - 2500
-
500 - 1500
Finishing
Continuous
Without
DX140
0.05 - 1.0
0.05 - 0.15
500 - 2500
400 - 800
500 - 1500
Light interrupted Without
DX140
0.05 - 1.0 0.05 - 0.15
300 - 1800
400 - 600
400 - 1200
Heavy
interrupted
P
TH10
0.5 - 4.0
0.2 - 0.5
100 - 500
100 - 200
100 - 200
Medium
cutting
Continuous
P
TH10
0.5 - 4.0
0.2 - 0.5
100 - 1000
100 - 300
100 - 300
Light interrupted
P
TH10
0.5 - 4.0
0.2 - 0.5
100 - 800
100 - 200
100 - 200
Heavy interrupted
P
TH10
0.5 - 4.0
0.2 - 0.5
100 - 500
100 - 200
100 - 200
STANDARD CUTTING CONDITIONS
(T-DIA)
(T-DIA)
P
7
6
5
4
3
2
1
0
0.1
0.2
0.3
0.4
0.5
0.6
0.7
P
T-DIA
DX140
TH10
DX120
Insert


