B018
Tur n
L i ne -
Ch i pbreaker Gu i de
T9125
T9115
AH725
GT9530
NS9530
Steel
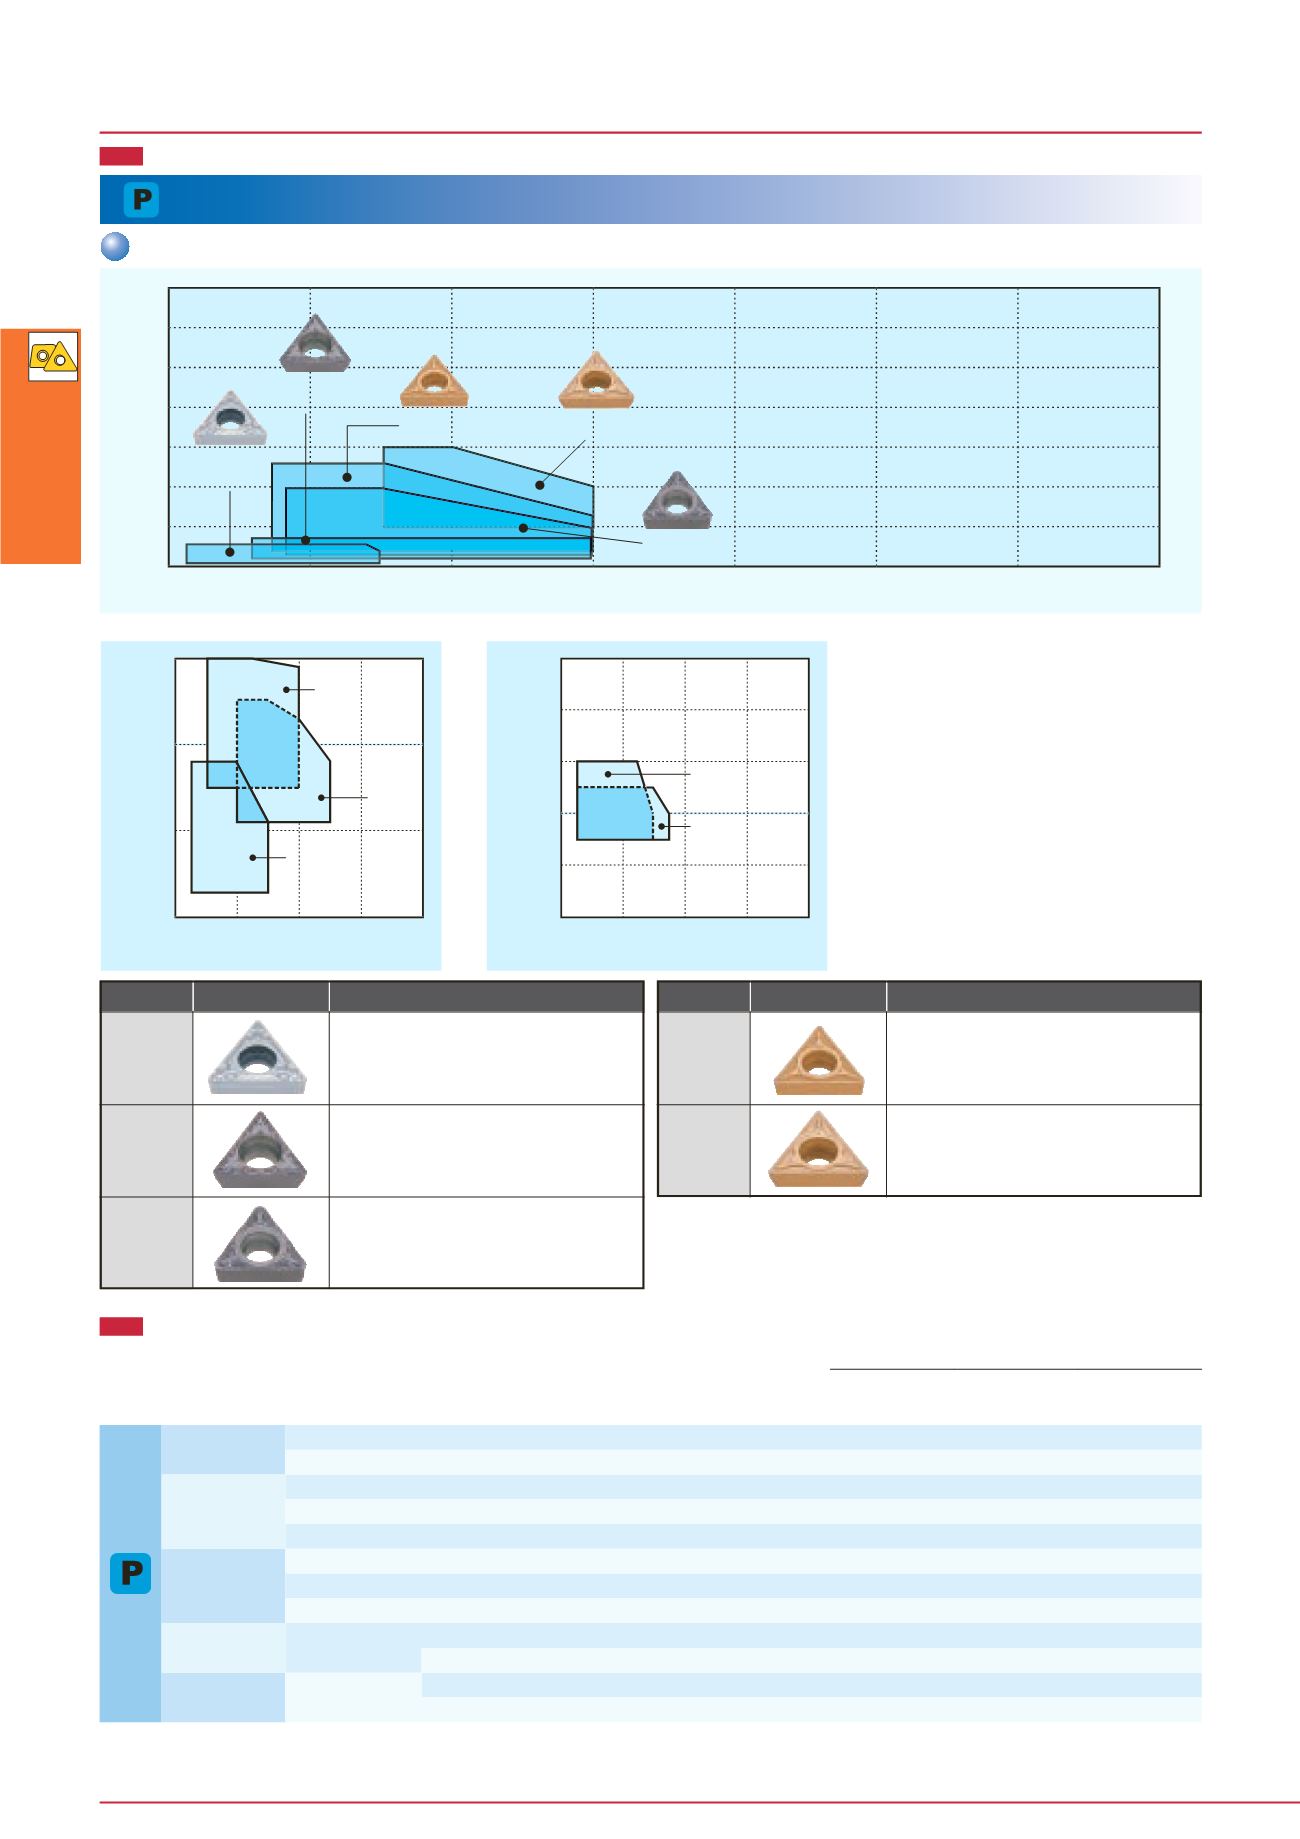
Chipbreaker System for Turning (Positive Inserts)
The sharp cutting edge and raised
projection near corner contribute to
excellent chip control at very small depth
of cut and low feed.
Developed chipbreaker for finishing at low
cutting depths. Optimal chip control due
to pre-positioned chipbreaker element.
3-dimensional chipbreaker designed to
have excellent chip control capability and
low cutting force in finishing to medium
cutting. Low cost, M-class positive insert
used for high efficiency boring in a wide
range of applications.
3-dimensional chipbreaker designed to
have excellent chip control capability and
low cutting force in finishing to medium
cutting. Low cost, M-class positive insert
used for high efficiency boring in a wide
range of applications.
Developed chipbreaker for medium
cutting. Excellent chip control due to
wide, positive chip flow zone.
Chipbreaker
Appearance
Features
Chipbreaker
Appearance
Features
CVD / PVD coated grades
Coated cermets / Cermets
Depth of cut:
a
p (mm)
Feed:
f
(mm/rev)
Feed:
f
(mm/rev)
Feed:
f
(mm/rev)
Cutting speed:
V
c (m/min)
Cutting speed:
V
c (m/min)
BASIC CHIPBREAKERS: POSITIVE INSERTS
ISO Operation Work condition Chip-
breaker
Grade Depth of cut
a
p (mm)
Feed
f
(mm/rev)
Cutting speed:
V
c (m/min)
Low carbon
steels,
Alloy steels
Medium car-
bon steels,
Alloy steels
High carbon
steels,
Alloy steels
Precision
finishing
Continuous
01
NS9530 0.05 - 0.5 0.03 - 0.15
150 - 250
80 - 220
80 - 180
Light interrupted
01
NS9530 0.05 - 0.5 0.03 - 0.15
150 - 250
80 - 220
80 - 180
Finishing
Continuous
PSS
NS9530
0.1 - 0.5
0.05 - 0.3
150 - 250
80 - 220
80 - 180
Light interrupted PSS
NS9530
0.1 - 0.5
0.05 - 0.3
150 - 250
80 - 220
80 - 180
Heavy interrupted PSS
NS9530
0.1 - 0.5
0.05 - 0.3
150 - 250
80 - 220
80 - 180
Finishing to light
cutting
Continuous
PS
NS9530
0.3 - 2.0
0.08 - 0.3
150 - 250
80 - 220
80 - 180
Light interrupted
PS
NS9530
0.3 - 2.0
0.08 - 0.3
150 - 250
80 - 220
80 - 180
Heavy interrupted PS
NS9530
0.3 - 2.0
0.08 - 0.3
150 - 250
80 - 220
80 - 180
Finishing to
Medium cutting
Continuous to
Heavy interrupted
PS
T9115
0.5 - 2.5
0.08 - 0.3
150 - 300
100 - 200
80 - 180
PS
T9125
0.5 - 2.5
0.08 - 0.3
120 - 250
80 - 180
80 - 120
Medium cutting Continuous to
Heavy interrupted
PM T9115
1.0 - 3.0
0.15 - 0.3
150 - 300
100 - 200
80 - 180
PM T9125
1.0 - 3.0
0.15 - 0.3
120 - 250
80 - 180
80 - 120
Low carbon steels, Alloy steels: C10, 18CrMo4, E275A, 20Cr4, etc. Medium carbon steels, Alloy steels: C45, 42CrMo4, etc.
Hi carbon steels, Alloy steels: 41CrNiMo2, etc.
STANDARD CUTTING CONDITIONS
7
6
5
4
3
2
1
0
0.1
0.2
0.3
0.4
0.5
0.6
0.7
NS9530
GT9530
NS9530
T9115
T9125
GT9530
NS9530
AH725
T9115
T9125
GT9530
NS9530
T9115
T9125
GT9530
NS9530
AH725
T9115
T9125
300
200
100
500
400
300
200
100
0
0.2
0.4
0.6
0.8
0
0.2
0.4
0.6
0.8
01
PSF
PS
PM
PSS
01
PSF
PS
PM
PSS
Insert


