Tungaloy
B005
10
01(TF)
CB
TS
CM
TSF
TM
A
THS
B
TRS
C
TUS
D
DM
P
HRF
W
HRM
PSF
HMM
PSS
SF
PS
SS
PM
SM
AL
S
RS
SH
W
SA
H
ZF
11
ZM
61
NS
S1
NM
J08,J10
AS
JS
AM
JRP
FW
JPP
SW
JSP
AFW
ASW
s
s
ø
d
ø
d
m
m
10
10
8
7
7
6
6
r
ε
N
R
L
9
X1
01
T1
02
T2
03
T3
04
05
06
07
09
1.39
1.59
1.98(1.79)
2.38
2.78
3.18
3.97
4.76
5.56
6.35
7.94
9.52
6
6.35
9.525
12.7
15.875
19.05
25.4
31.75
32
±0.05
±0.1
±0.15
±0.08
±0.13
±0.08
±0.18
±0.25
±0.13
±0.25
±0.08
±0.15
±0.2
±0.13
±0.18
±0.13
±0.27
±0.38
±0.2
±0.38
H
O
P
S
T
W
R
C,E,M
6.35
9.525
12.7
15.875
19.05
6.35
9.525
±0.05
±0.08
±0.1
±0.11
±0.15
±0.18
D
±0.05
±0.16
V
Y
TM
JS
-
- F
08
04
04
T3
N
7
8
9
R
L
N
F
E
W.T
S
00
02
04
08
12
16
20
24
28
32
0.03
0.2
0.4
0.8
1.2
1.6
2.0
2.4
2.8
3.2
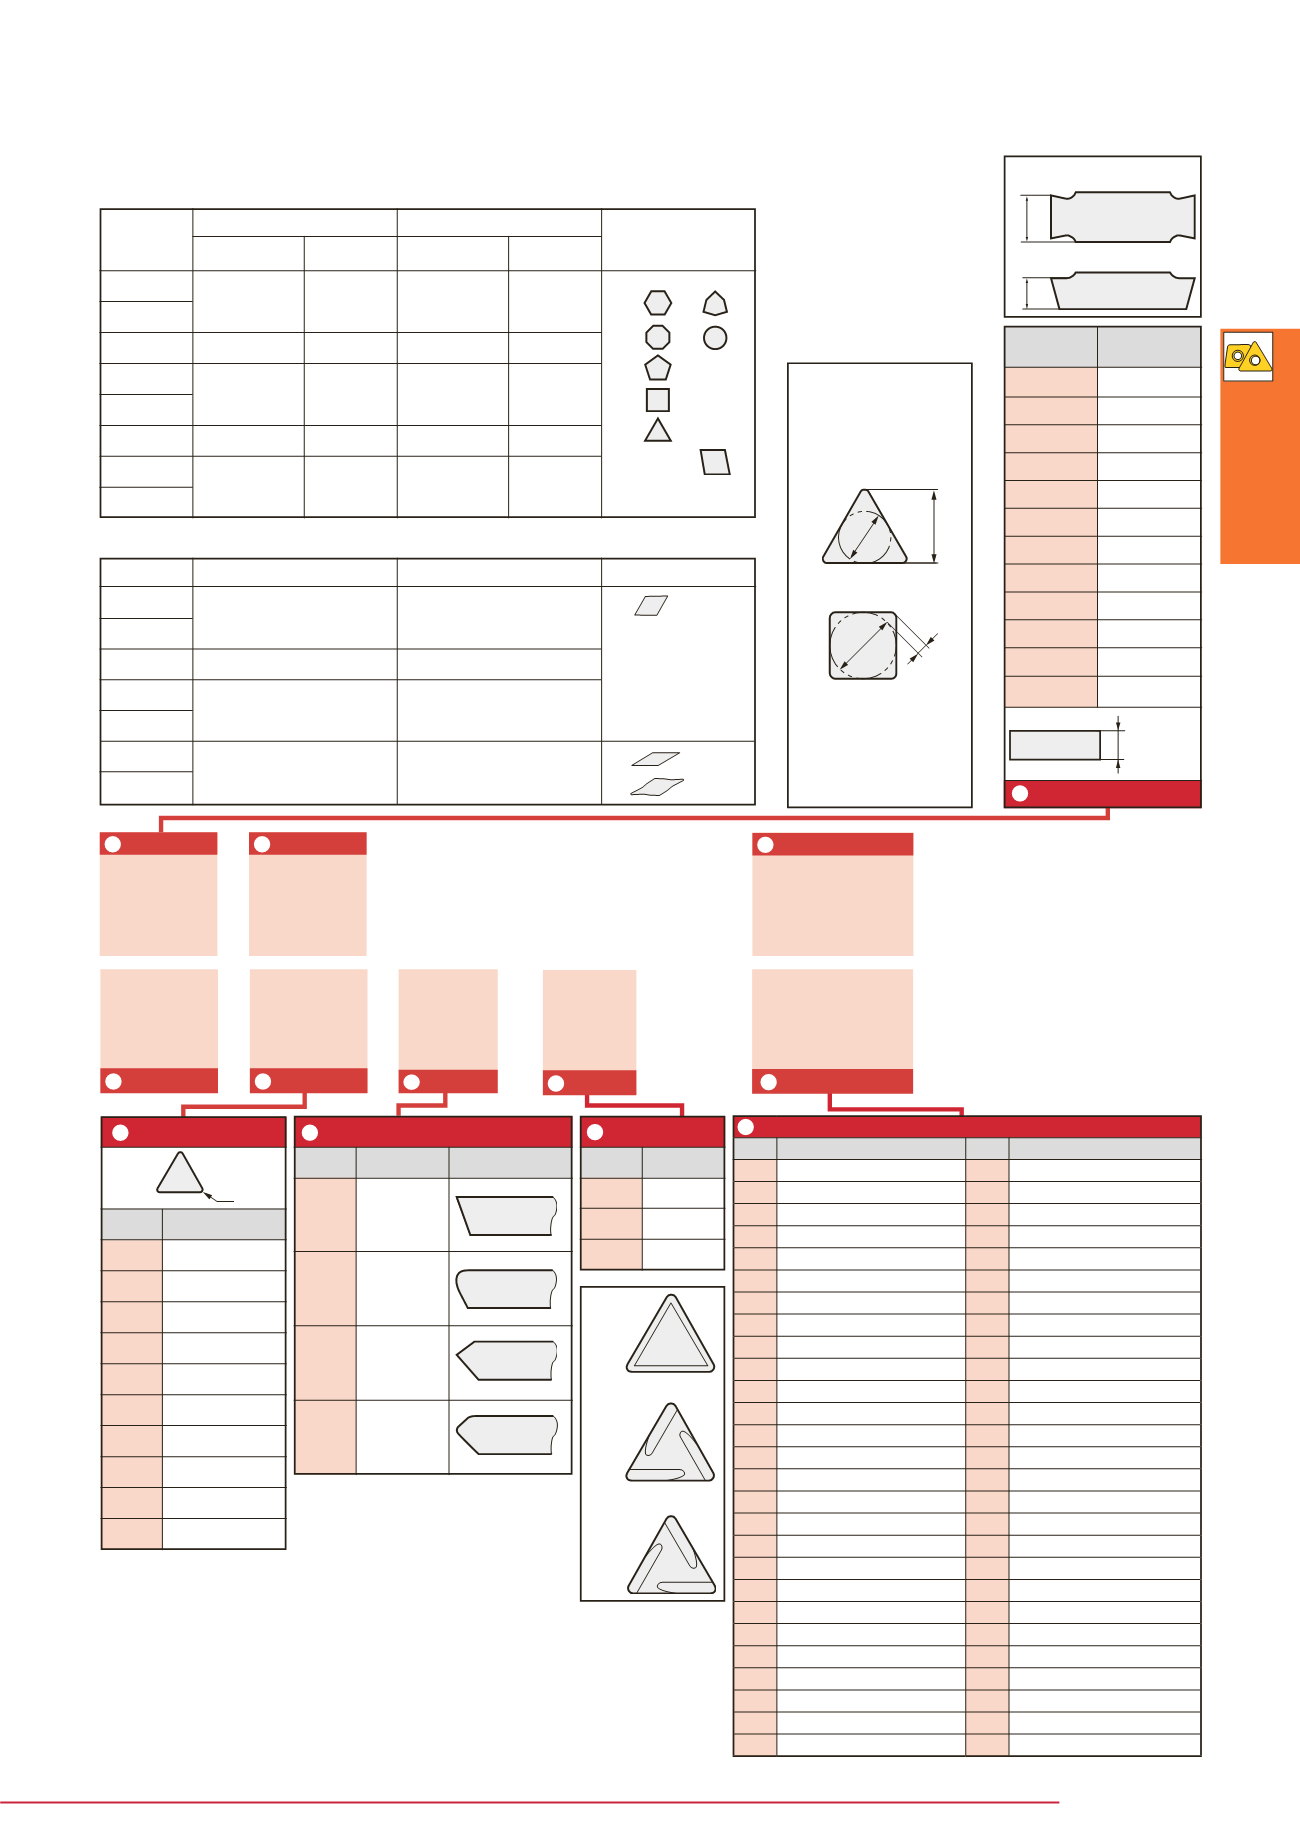
Insert
Detailed accuracy for J,K,L,M,N and U classes
For inserts with nose corner angles larger than 55˚
For M-type inserts with nose corner angles of 55˚ (Shape: D),
35˚ (Shape: V), 25˚ (Shape: Y)
Inscribed
circle
Tolerance on inscribed circle dia.
(ød)
Note on insert thickness
With regard to the insert
thickness for chipbreaker
inserts, the thickness (s)
drawn in the outlined insert
shapes on pages XX to XX is
defined as “s” (height from
the bottom face to the cutting
edge) shown in the figure at
right.
Tolerance on inscribed circle dia.
(ød)
Inscribed
circle
Tolerance on corner height (m)
Insert shapes applied
Tolerance on corner height (m) Insert shapes applied
Inscribed circle (ød)
Corner height (m)
Symbol
Thickness
(mm)
Thickness
Unit: mm
Unit: mm
[Example]
Negative insert
Pojitive insert
(Optional symbol)
(Optional symbol)
(Supplementary symbol)
Hand of insert
Symbols of major cutting edge
Corner radius
Symbol
Corner radius
r
ε
(mm)
Symbol
Condition of
cutting edge
Shape
Sharp
edge
Right
Left
Neutral
Symbol
Hand
Honed
rounded
edge
Honed
chamfered
edge
Combination
honed edge
Symbol
Applications
Medium cutting
Medium cutting of cast irons
Applications
Symbol
Chipbreakers
Finishing (Angular type)
Finishing (Right and left hand)
Finishing (Right and left hand)
Finishing of Aluminium alloys
All-
round
Thickness
Finishing (Positive type)
Finishing to medium cutting
(Positive type Basic selection)
Medium cutting (Positive type)
Finishing to medium cutting of
aluminium alloys
Finishing to light cutting
(Positive insert)
Medium cutting (For round inserts)
Finishing (Angular type)
Finishing (Parallel)
Finishing
Finishing (For KNMX type)
For small lathes
For small lathes
For small lathes
For small lathes
For small lathes
Precision finishing (Basic selection)
Finishing (Basic selection)
Finishing (Basic selection)
Medium cutting (Basic selection)
Medium to heavy cutting
(Basic selection)
Medium to heavy cutting
Heavy cutting
Medium cutting
Finishing
Finishing to medium cutting
Medium cutting
Finishing of stainless and mild steels
Medium cutting of stainless steels
Medium cutting of stainless steels
For heat-resisting alloys and stainless
steels
Finishing of stainless steels
Medium to heavy cutting of stainless
steels
Finishing and copying
Finishing to medium cutting and
copying
Finishing and copying
Finish to medium cutting and
copying
Small depth of cut and high feed
Small depth of cut and high feed
(Wiper type Inserts)
Small depth of cut and high feed
(Wiper type Inserts)
(class)
(class)
(class)
(class)
J,K,L,M,N
U
J,K,L,M,N
U
Small depth of cut and high feed
(For round inserts)
Medium cutting
Finishing (Right and left hand)
Finishing (Right and left hand)
Small depth of cut and high feed
Finishing (Wiper type)
Finishing to medium cutting
(Wiper type)


