E065
Tungaloy
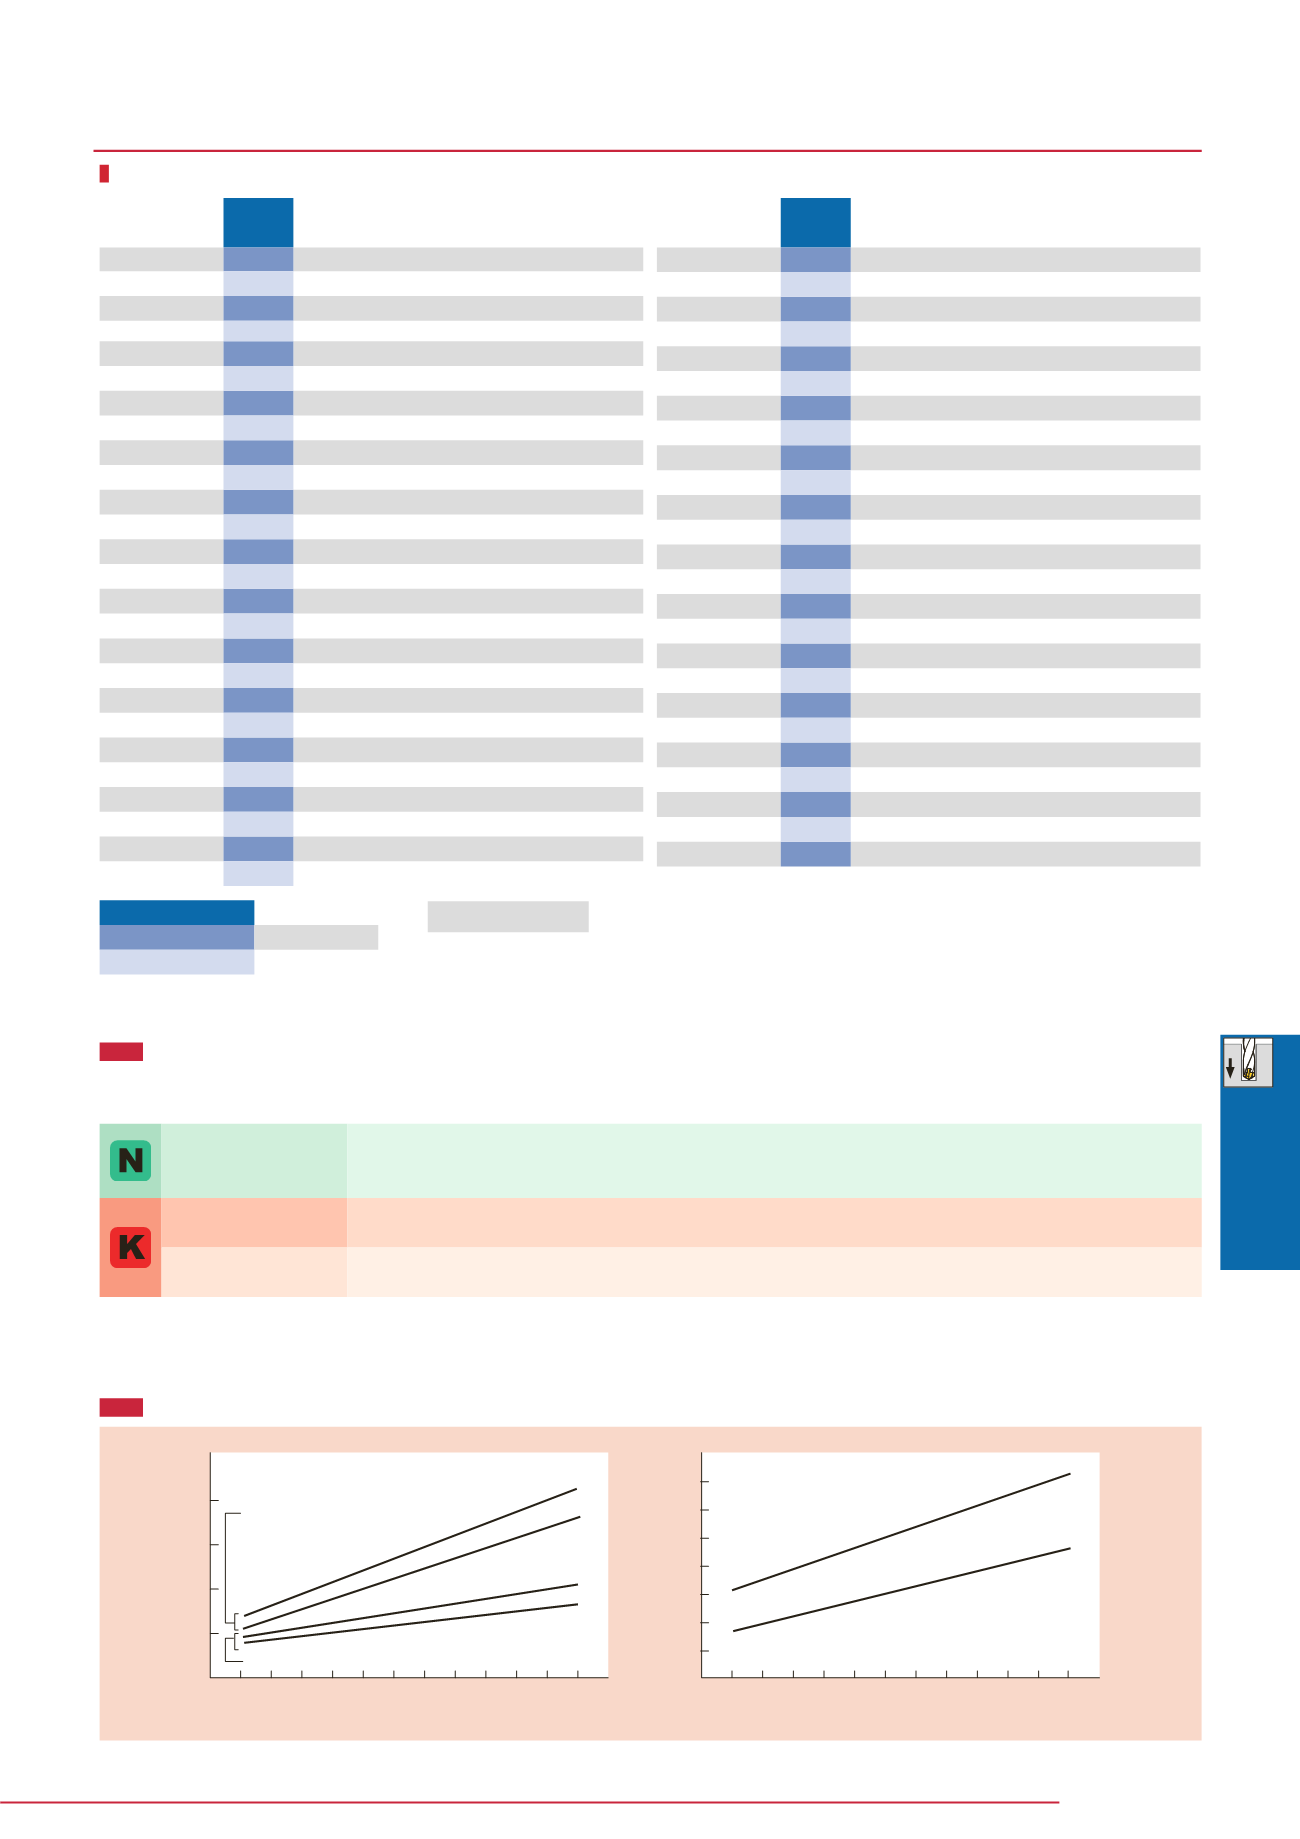
f
= 0.3 mm/rev
f
= 0.3 mm/rev
f
= 0.2 mm/rev
f
= 0.2 mm/rev
V
c = 120 m/min
V
c = 120 m/min
V
c = 100 m/min
V
c = 100 m/min
3200
2800
2400
2000
1600
1200
800
400
10
8
6
4
2
0
5 6 7 8 9 10 11 12 13 14 15 16
5 6 7 8 9 10 11 12 13 14 15 16
2-e ective Drill
• Supply the cutting fluid through the drill.
• The required fluid pressure is 0.5 to 1.0 MPa
• Use a water soluble cutting fluid containing a large amount of extreme pressure additive.
Cutting fluid
Designation
øD
c
G1F øD
s
ℓ
ℓ
s
L
FDC0500L
5
5
55
38
95
FDC0510L
5.1
6
61
40
105
FDC0520L
5.2
6
61
40
105
FDC0530L
5.3
6
61
40
105
FDC0540L
5.4
6
61
40
105
FDC0550L
5.5
6
61
40
105
FDC0560L
5.6
6
66
40
110
FDC0570L
5.7
6
66
40
110
FDC0580L
5.8
6
66
40
110
FDC0590L
5.9
6
66
40
110
FDC0600L
6
6
66
40
110
FDC0610L
6.1
7
72
40
115
FDC0620L
6.2
7
72
40
115
FDC0630L
6.3
7
72
40
115
FDC0640L
6.4
7
72
40
115
FDC0650L
6.5
7
72
40
115
FDC0660L
6.6
7
77
40
120
FDC0670L
6.7
7
77
40
120
FDC0680L
6.8
7
77
40
120
FDC0690L
6.9
7
77
40
120
FDC0700L
7
7
77
40
120
FDC0710L
7.1
8
83
42
125
FDC0720L
7.2
8
83
42
125
FDC0730L
7.3
8
83
42
125
FDC0740L
7.4
8
83
42
125
FDC0750L
7.5
8
83
42
125
Designation
øD
c
G1F øD
s
ℓ
ℓ
s
L
FDC0760L
7.6
8
88
42
130
FDC0770L
7.7
8
88
42
130
FDC0780L
7.8
8
88
42
130
FDC0790L
7.9
8
88
42
130
FDC0800L
8
8
88
42
130
FDC0810L
8.1
9
94
44
140
FDC0820L
8.2
9
94
44
140
FDC0830L
8.3
9
94
44
140
FDC0840L
8.4
9
94
44
140
FDC0850L
8.5
9
94
44
140
FDC0860L
8.6
9
99
44
145
FDC0870L
8.7
9
99
44
145
FDC0880L
8.8
9
99
44
145
FDC0890L
8.9
9
99
44
145
FDC0900L
9
9
99
44
145
FDC0910L
9.1
10
105
44
150
FDC0920L
9.2
10
105
44
150
FDC0930L
9.3
10
105
44
150
FDC0940L
9.4
10
105
44
150
FDC0950L
9.5
10
105
44
150
FDC0960L
9.6
10
110
46
160
FDC0970L
9.7
10
110
46
160
FDC0980L
9.8
10
110
46
160
FDC0990L
9.9
10
110
46
160
FDC1000L
10
10
110
46
160
ISO Workpiece material
Cutting speed: Vc (m/min)
Feed: f (mm/rev)
ø5 ~ ø8
ø8 ~ ø12
ø12 ~ ø16
ø5 ~ ø8
ø8 ~ ø12
ø12 ~ ø16
Aluminium alloys
100 - 140
120 - 160
140 - 180
0.1 - 0.25
0.15 - 0.3
0.15 - 0.3
Grey Cast irons
90 - 120
110 - 140
130 - 160
0.1 - 0.25
0.2 - 0.3
0.2 - 0.30
Ductile cast irons
60 - 80
70 - 90
70 - 100
0.1 - 0.25
0.15 - 0.3
0.15 - 0.3
STANDARD CUTTING CONDITIONS
CUTTING PERFORMANCE
Caution
:
When changing a tool, completely clean the chips which may be clogging in the collet or adapter.
Note:
1
The cutting conditions shown left may vary depending on the work material, coolant dilution ratio and coolant supply pressure used.
L/D = 8 (L type)
Work materials: FC300 (200HB)
• No. of revolutions (min -1 ) = Cutting speed
1000
3.14
Tool diameter
• Table feed (mm/min) = No. of revolutions
Feed per revolution
Work material: FC300 (200HB)
Cutting conditions:
V
c = 120 m/min
: Line-up
FDC
Net power consumption (kw)
Drill diameter øDc (mm)
Drill diameter øDc (mm)
Thrust force (N)
øDc
Tool diameter
tolerance (mm)
5 ≤ øDc ≤ 6
+0.02 ~ +0.01
6 < øD
c
≤ 10 +0.025 ~ +0.015


