E063
Tungaloy
2-e ective Drill
ISO Workpiece material
Cutting speed:
Vc (m/min)
Feed:
f (mm/rev)
Aluminium alloys (Brittle)
50 - 80
0.1 - 0.3
Aluminium alloys (Sticky)
40 - 60
0.1 - 0.2
Grey cast irons
40 - 60
0.1 - 0.3
Ductile cast irons
30 - 50
0.08 - 0.2
øDc h
8
øDs h
8
L
R
135°
Back taper 0.04~0.06/100
ø
D
c
=
ø
D
s
Designation
øD
c
T
olerance G1F ℓ
L
A
pplication
FDS0257
2.57 0
- 0.014
18
60
M3
FDS0337
3.37 0
- 0.018
18
60
M4
FDS0429
4.29 0
- 0.018
23
70
M5
FDS0511
5.11 0
- 0.018
28
80
M6
FDS0683
6.83 0
- 0.022
36
90
M8
FDS0860
8.6 0
- 0.022
46
110
M10
Designation
øD
c
T
olerance G1F ℓ
L
A
pplication
FDS0340
3.4 0
- 0.018
18
60
M3
FDS0450
4.5 0
- 0.018
23
70
M4
FDS0550
5.5 0
- 0.018
28
80
M5
FDS0660
6.6 0
- 0.022
36
90
M6
FDS0900
9
0
- 0.022
46
110
M8
FDS1100
11 0
- 0.027
55
120
M10
FDS
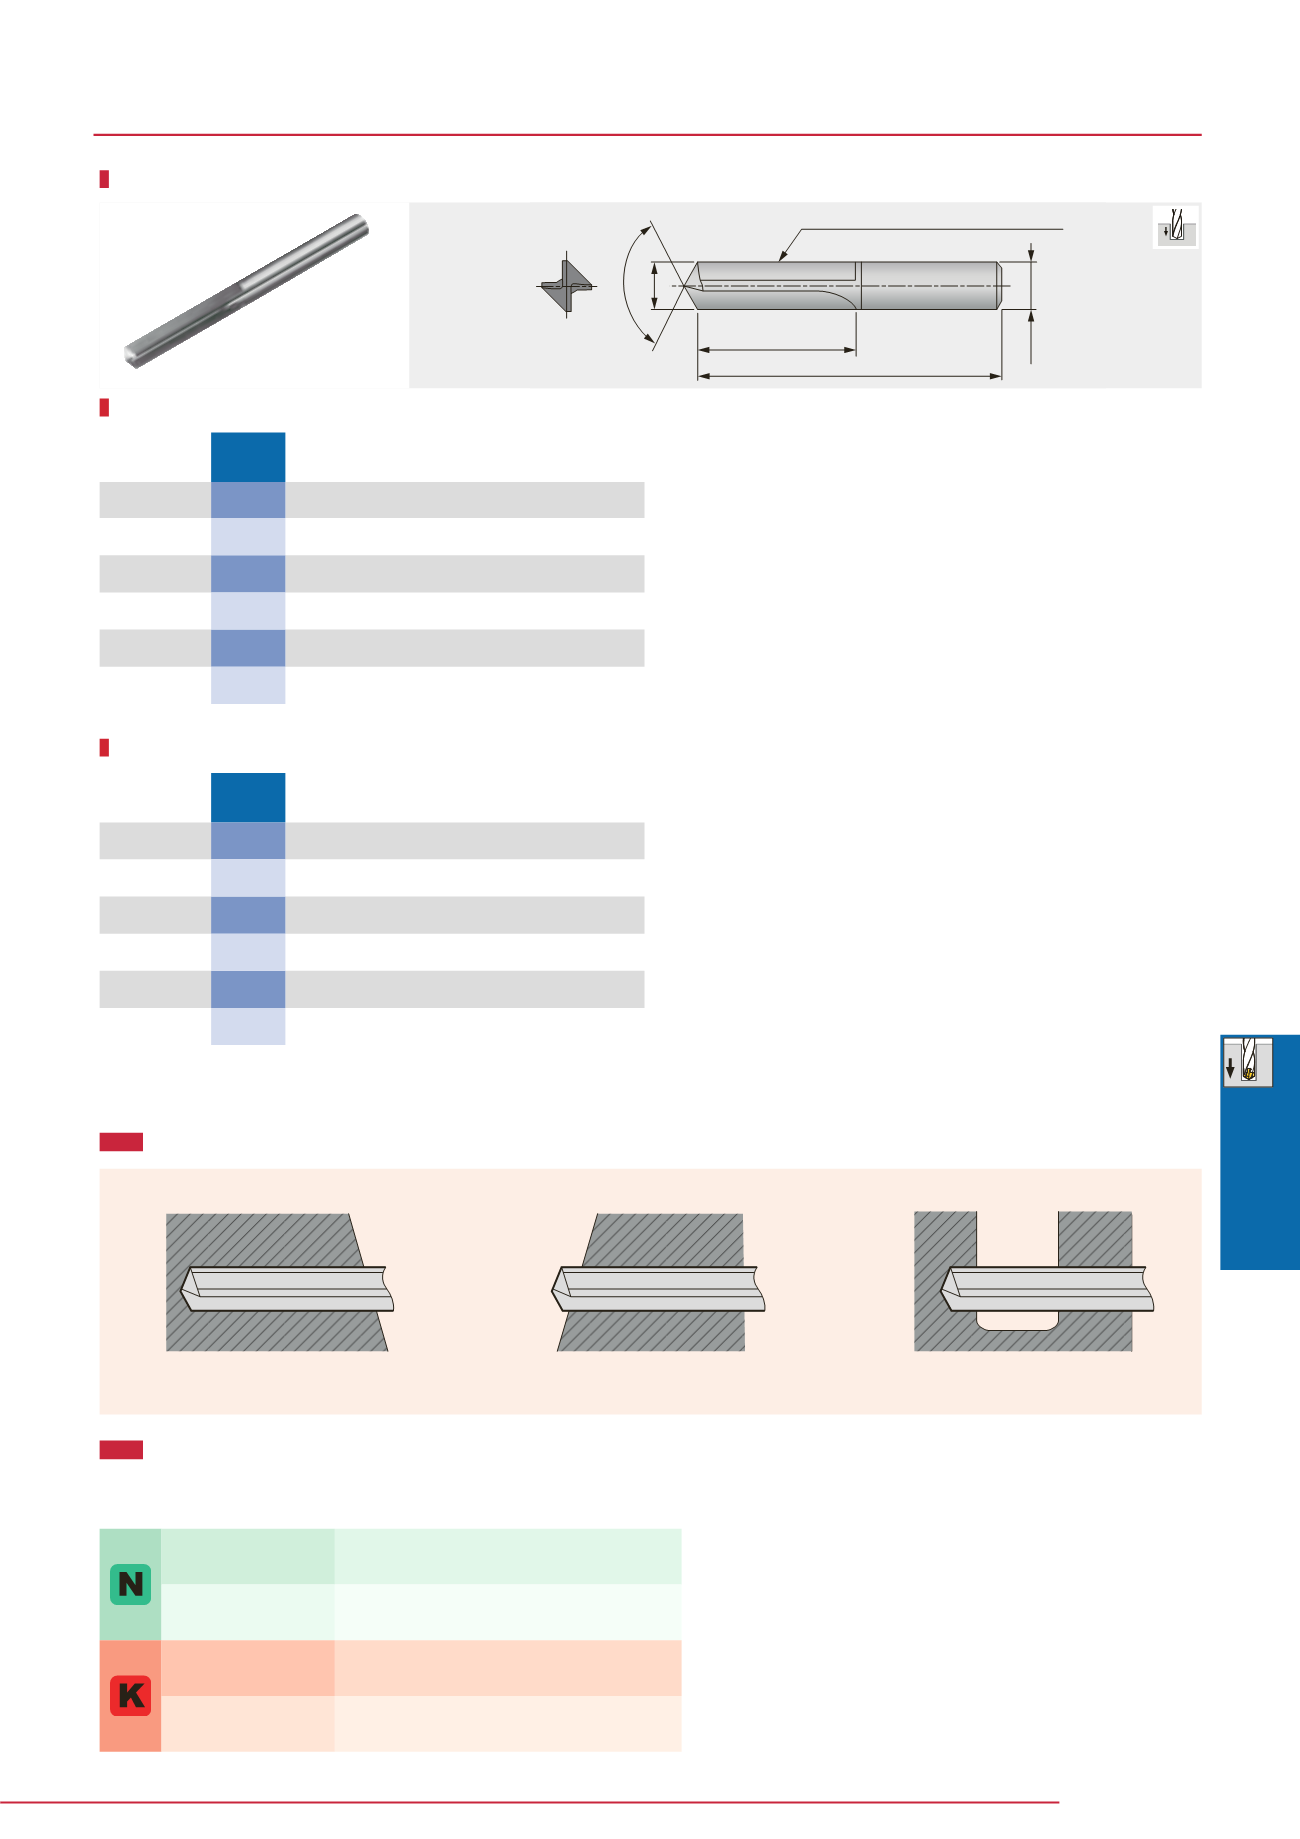
Straight flute soliddrill for pre-tap hole drilling of aluminum, without oil hole
APPLICATION EXAMPLES OF FD DRILLS (EFFECTIVE FOR FOLLOWING OPERATIONS)
STANDARD CUTTING CONDIOTIONS
Notes:• Other sized drills and step type drills can be made to order.
• When ordering, specify the diameter, overall length, shank specifications of the drill, the work material to be drilled, and the drilling depth.
For tupped holes
For bolt holes
L/D = 2 (S type)
Drilling into angled face
Drilling through angled face
Interrupted drilling
Note : Use a water soluble emulsion type cutting fluid.
Excessive run out as mounted on the machine may affect
drilled hole accuracies and tool life.
(Holding with a scroll chuck is not recommended.)
• No. of revolutions (min -1 ) = Cutting speed
1000
3.14
Tool
diameter
• Table feed (mm/min) = No. of revolutions
Feed per revolution
: Line-up


