E068
W1
W
A
A
30°~45°
2-e ective Drill
CAUTIONARY NOTES
REGRINDING
STANDARD CUTTING CONDITIONS
• No. of revolutions (min
-1
) = Cutting speed
1000
3.14
Tool diameter
• Table feed (mm/min) = No. of revolutions
Feed per revolution
ISO Workpiece
material
Cutting speed: Vc (m/min)
Feed: f (mm/rev)
ø0.4 ~ ø2 ø2 ~ ø13
ø0.4 ~ ø1
ø1 ~ ø2
ø2 ~ ø3
ø3 ~ ø5
ø5 ~ ø13
Grey cast irons
(200HB)
20 - 40
30 - 50
0.005 - 0.03
0.01 - 0.06
0.03 - 0.12
0.05 - 0.15
0.1 - 0.4
Ductile cast irons
(300HB)
20 - 40
30 - 50
0.005 - 0.02
0.01 - 0.05
0.03 - 0.1
0.03 - 0.1
0.07 - 0.25
Aluminium alloys
20 - 50
30 - 50
0.01 - 0.05
0.04 - 0.15
0.06 - 0.2
0.1 - 0.25
0.15 - 0.5
Copper alloys
20 - 50
30 - 50
0.01 - 0.05
0.04 - 0.15
0.06 - 0.2
0.1 - 0.25
0.15 - 0.5
Reinforced plastics
20 - 40
30 - 50
0.01 - 0.05
0.04 - 0.15
0.06 - 0.2
0.1 - 0.25
0.15 - 0.5
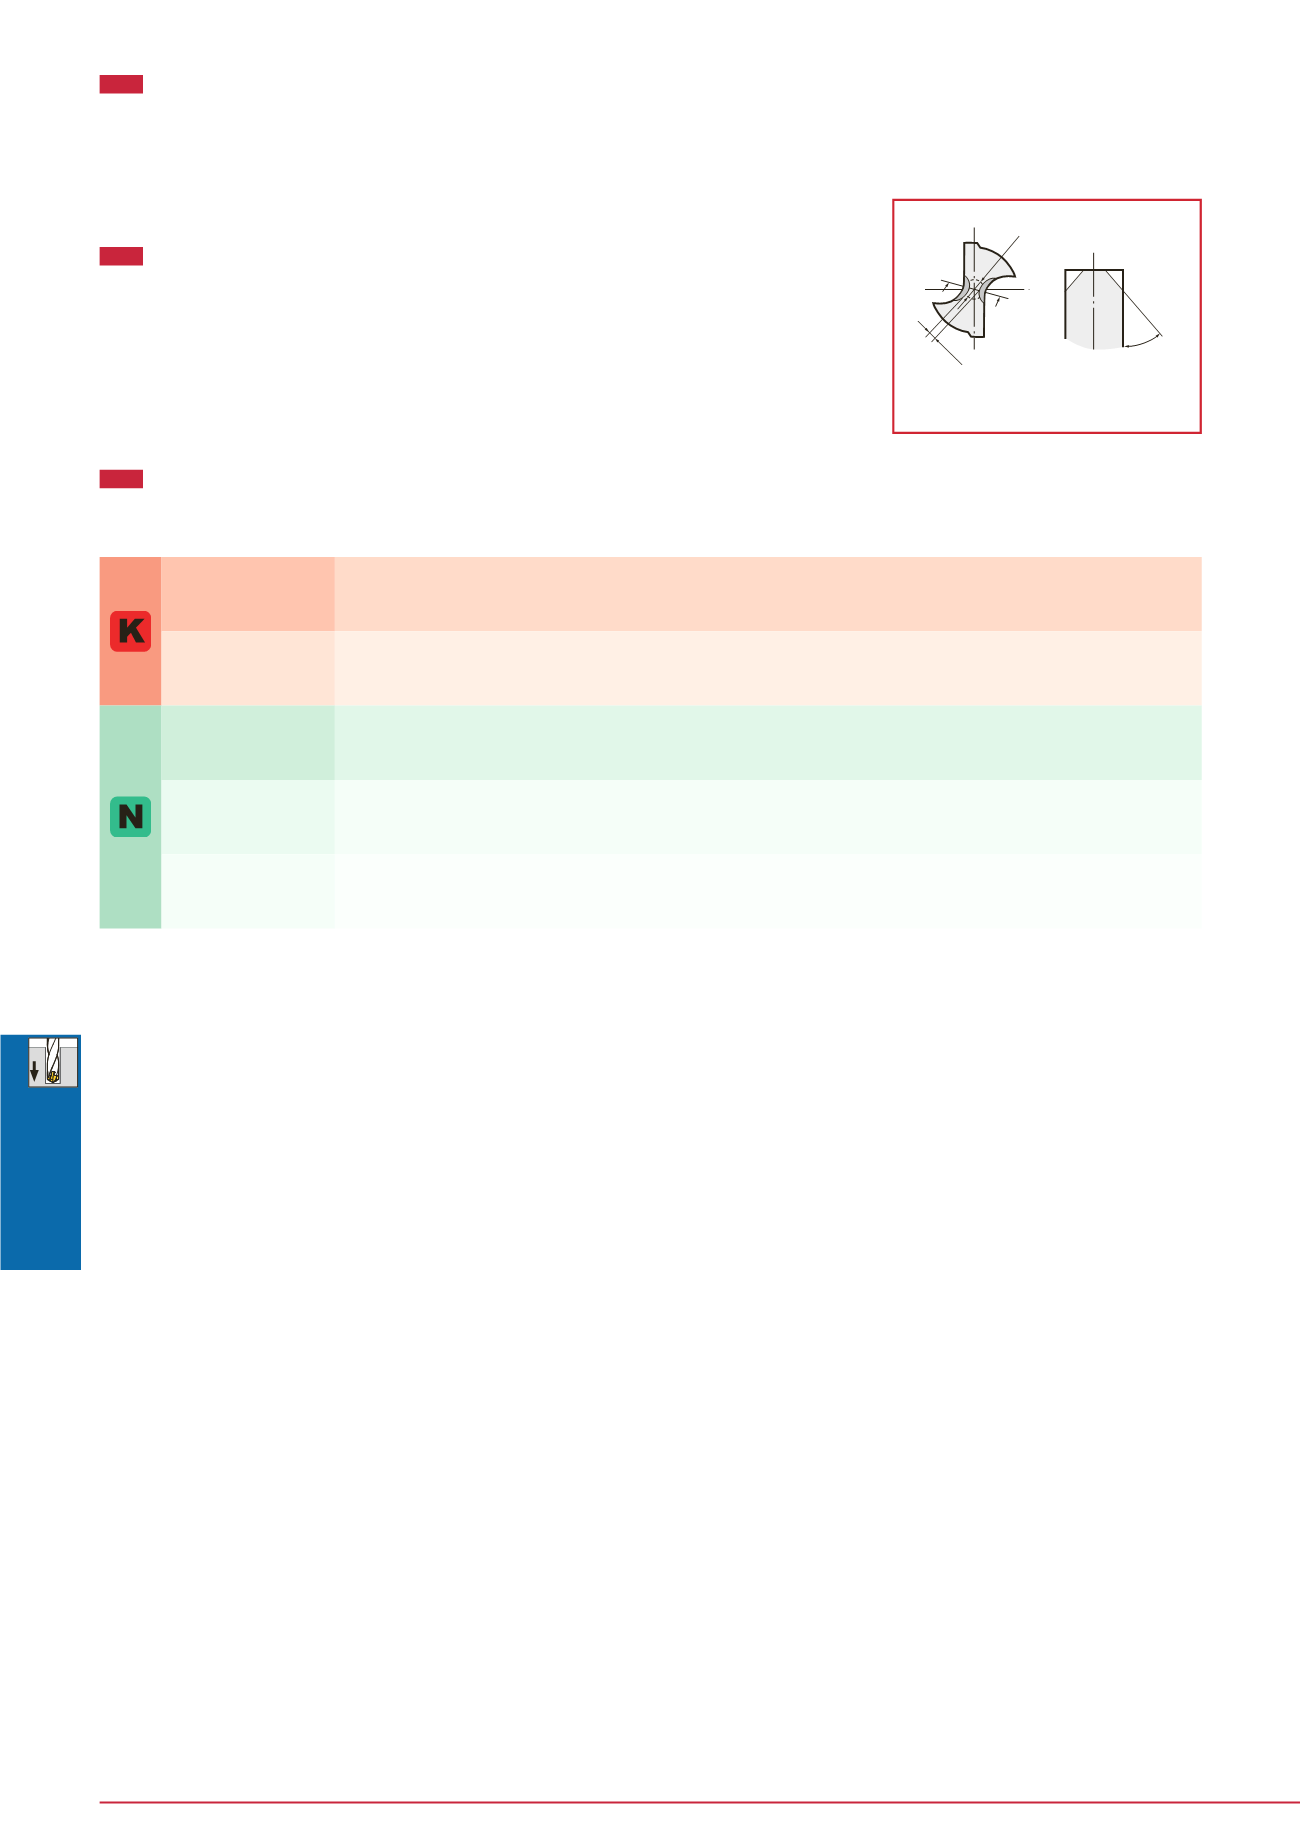
Section A-A
S-type thinning
• To prevent edge chipping, hone cutting edges as follows:
Honing width: 0.02 ~ 0.05 mm Honing angle: -20˚ to -30˚.
Chipping is likely to occur on edges whilst drilling hard
materials, a larger honing width is recommended.
• When drilling into an inclined surface, special care should
be taken to prevent drill breakage. Use of drill bushing is
recommended for such case.
• Carry out regrinding when corner wear reaches the margin width.
• Avoid using silicon carbide grinding wheels or hand grinding whenever possible.Use
diamond grinding wheels of 200 to 400 mesh.
• Apply web thinning for the drill above ø6 mm. S-type thinning shown in figure at right
is recommended. Preferable thinning width (W1) is about 1/2 to 1/3 of web thickness
(W).


