D169
Tungaloy
Face Milling
L
L
f
0.05
øDc
øD
øD
1
øDs
h6
Finishing insert
Proceeding insert
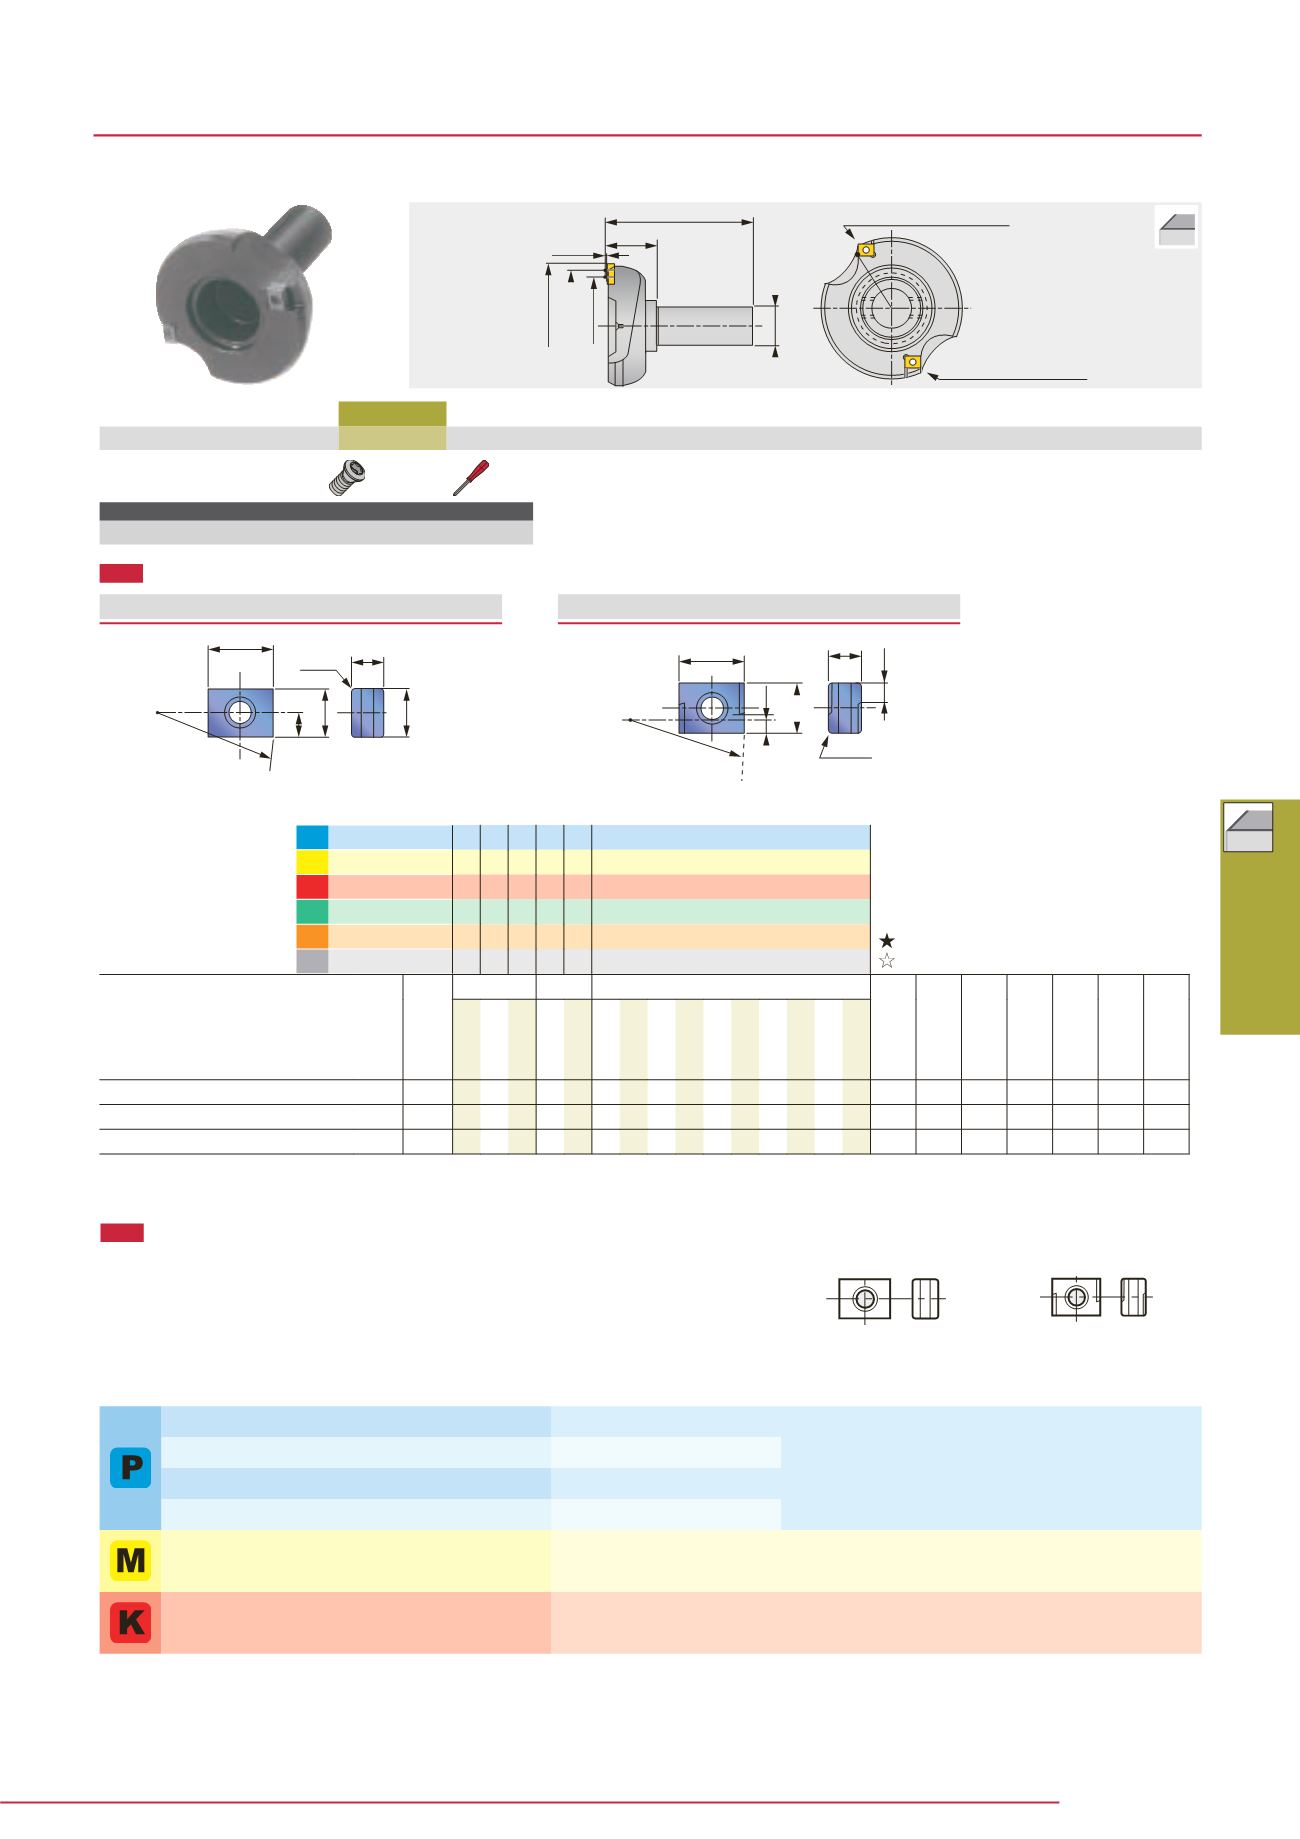
LNCQ0906-50S
LNCQ0906N-100 ( 50 ) L
INSERT
W
bs
A
B
T
r
ε
0.8
R
fig.2
P Steel
M Stainless
K Cast iron
N Non-ferrous
S Superalloys
H Hard materials
Designation
Max.
a
p
Coating Cermet
A B T R W bs fig
AH120
GH110
NS740
LNCQ0906N-100L
0.2
l l l
9.525 12.7 6.35 100 4.763 7.9 1
LNCQ0906N-50L
0.2
l l l
9.525 12.7 6.35 50 4.763 7.9 1
LNCQ0906R-50S
0.2
l l l
- 12.7 6.35 50 2.3 4 2
: First choice
: Second choice
EMS09
Endmill with negative rectangle insert for highly precision finishing
Designation Max. ap
øD
c
z
ø
D
øD
1
øD
s
L
f
L
Insert
EMS09080R
0.2
80
2
92
100.7
32
40
120
LNCQ0906...
SPARE PARTS
Designation
Clamping screw Wrench
EMS09080R
CSTB-4
T-15D
A.R. = +10°, R.R. = -30°
l
: Line-up
B
S
bs
W
R
T
fig.1
r
ε
0.8
ISO
LNCQ0906N-100(50)L LNCQ0906R-50S
Mild steels E275A, etc. < 180 HB
NS740
200 ~ 300
< 0.2
2 ~ 6
≤
0.2
1 ~ 2.5
Carbon steels C55, etc. < 300 HB
NS740
150 ~ 250
Alloy steels 42CrMo4, etc. < 300 HB
NS740
120 ~ 200
Die steels X40CrMoV5-1, etc. < 300 HB
NS740
100 ~ 150
Stainless steels
X5CrNi18-9, X5CrNiMo17-12-3, etc.
AH120
NS740
150 ~ 220
< 0.2
2 ~ 6
≤
0.2
1 ~ 2.5
Cast irons 250, etc.
GH110
AH120
120 ~ 200
< 0.2
2 ~ 6
≤
0.2
1 ~ 2.5
STANDARD CUTTING CONDITIONS
Workpiece material
Grade
Cutting
speed
vc (m/min)
Depth of cut
a
p
(mm)
Depth of cut
a
p
(mm)
Feed per tooth
f
(mm/rev)
Feed per tooth
f
(mm/rev)


