D175
Tungaloy
Slot Milling
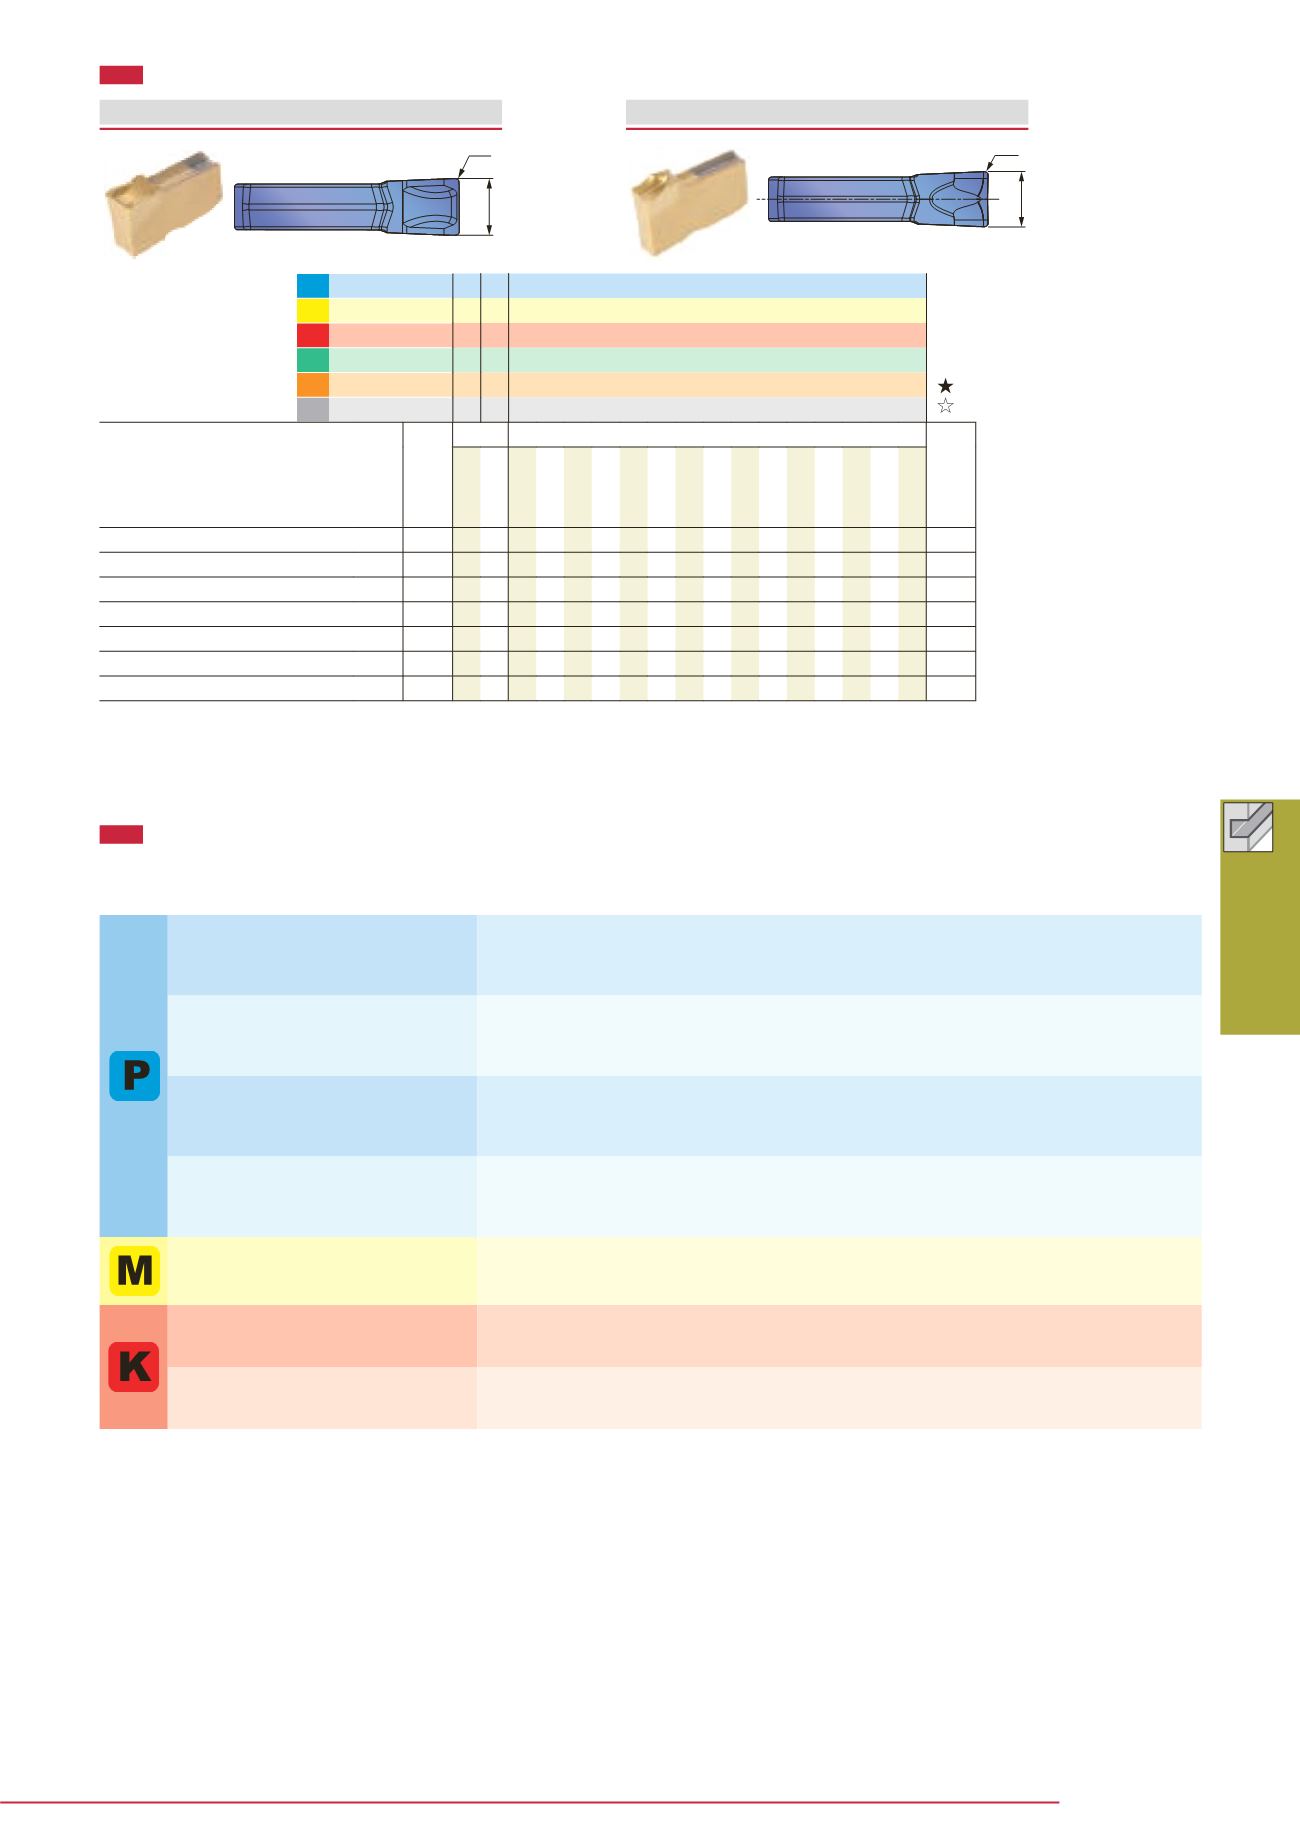
SSM
INSERT
SSS
W
r
ε
W
r
ε
STANDARD CUTTING CONDITIONS
Hardness
(HB)
Insert
Cutting speed
Vc (m/min)
Chip thickness
t (mm)
- 200
SSM...
150 - 230
0.05 - 0.15
200 - 300
SSM...
100 - 170
0.04 - 0.13
150 - 300
SSM...
90 - 160
0.04 - 0.13
- 300
SSM...
70 - 120
0.04 - 0.13
-
SSS...
90 - 200
0.04 - 0.13
150 - 250
SSM...
100 - 200
0.05 - 0.15
150 - 250
SSM...
80 - 130
0.05 - 0.15
Workpiece material
Low carbon steel
E275A, C15E4, etc.
High carbon steel
E355D, C55, etc.
Alloy steels
42CrMo4, 20Cr4, etc.
Tool steel
X153CrMoV12, X40CrMoV5-1, etc.
Stainless steel
X5CrNi18-9, X5CrNiMo17-12-3, etc.
Grey cast iron
250, 300, etc.
Ductile cast iron
400-15S, etc.
ISO
P Steel
M Stainless
K Cast iron
N Non-ferrous
S Superalloys
H Hard materials
Designation
r
ε
Coating
W±0.04
GH130
SSM22N
0.2
l
2.2
SSM31N
0.2
l
3.1
SSM41N
0.25
l
4.1
SSS16N
0.16
l
1.6
SSS22N
0.2
l
2.2
SSS31N
0.2
l
3.1
SSS41N
0.25
l
4.1
l
: Line-up
: First choice
: Second choice


