D168
Face Milling
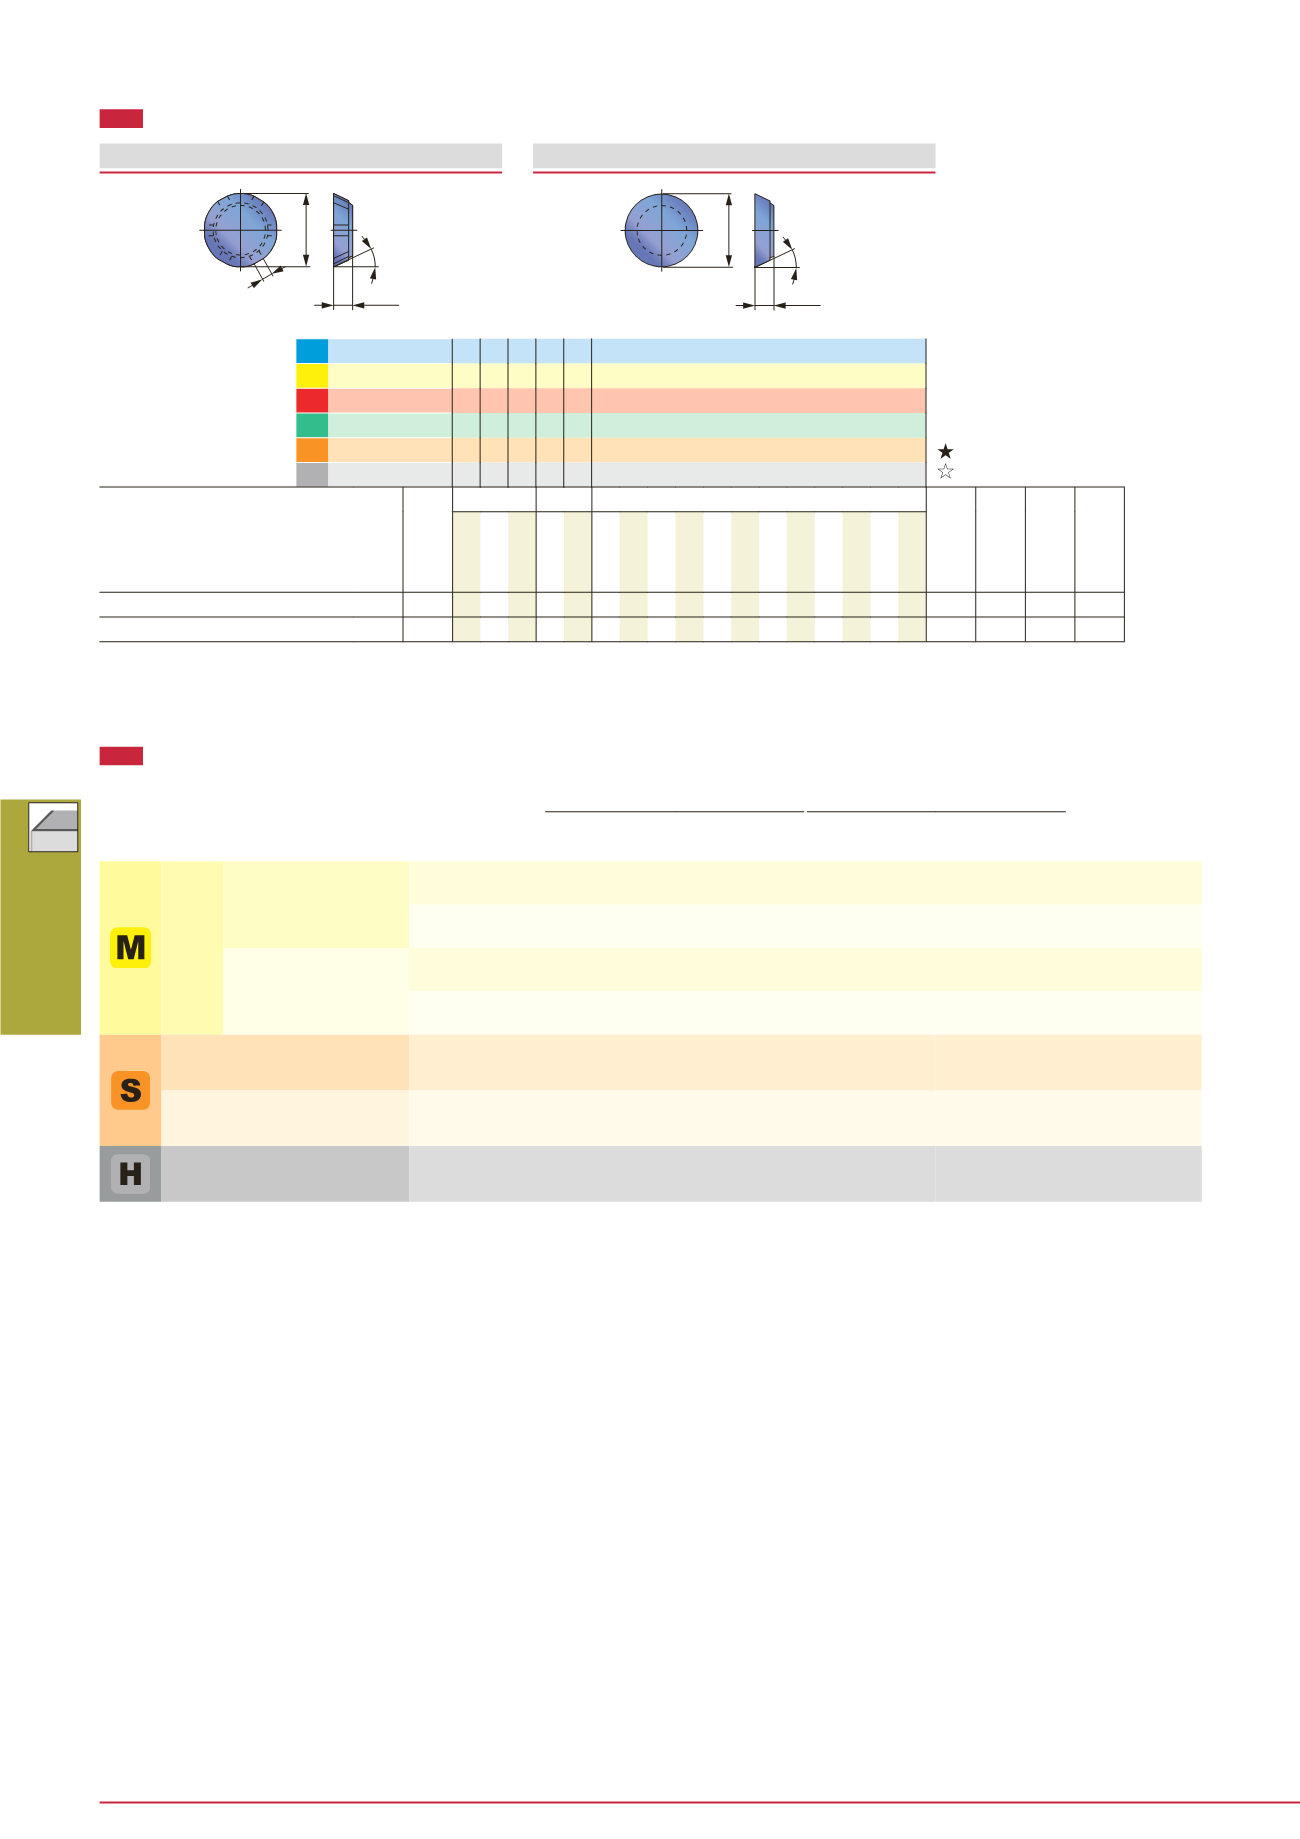
RFEN2004
ød
bs
T
θ
INSERT
P Steel
M Stainless
K Cast iron
N Non-ferrous
S Superalloys
H Hard materials
Designation
Max.
a
p
Coating
Un-
coated
ø
d
T
θ°
bs
AH120
GH330
UX30
KS20
RFEN2004ZFTN
3
l l l l
20 4.76 25 2.8
RFEN2004M0TN
10
l l l
20 4.76 25 -
: First choice
: Second choice
RFEN2004M0TN
ød
T
θ
l
: Line-up
STANDARD CUTTING CONDITIONS
Depth of cut = 1 ~ 3 mm Depth of cut = 0.4 ~ 1 mm
ISO Workpiece material
Grade
Cutting speed
vc(m/min)
Feed per tooth
fz (mm/t)
Cutting speed
vc(m/min)
Feed per tooth
fz (mm/t)
Cutting fluid
Stainless
steels
Austenitic, Ferritic
SUS304, X5CrNi18-9
< 300HB
AH120 GH330
150 ~ 250
0.20 ~ 0.35
180 ~ 250
0.2 ~ 0.5
Dry cutting
UX30
150 ~ 230
0.20 ~ 0.35
180 ~ 250
0.2 ~ 0.5
Dry cutting
Precipitatio hardening
SUS630,
X5CrNiCuNb16-4
< 35HRC
AH120 GH330
150 ~ 200
0.15 ~ 0.3
180 ~ 250
0.2 ~ 0.4
Dry cutting
UX30
130 ~ 180
0.15 ~ 0.3
150 ~ 200
0.2 ~ 0.4
Dry cutting
Superalloys
Inconel, Hastelloy etc.
KS20
20 ~ 30
0.10 ~ 0.15
20 ~ 50
0.2 ~ 0.4
Water insoluble
type
Titanium alloys
Ti-6Al-4V etc.
KS20
40 ~ 50
0.15 ~ 0.35
40 ~ 60
0.2 ~ 0.5 Water soluble type
or dry cutting
Hard materials
40 ~ 50HRC
KS20
20 ~ 50
0.05 ~ 0.1
20 ~ 50
0.05 ~ 0.2
Water insoluble
type
Note: Cutting width should be within 60 to 70 % of e²ective cutter diameter.
• No. of revolutions (min
-1
) = Cutting speed
1000 ÷ 3.14 ÷ Cutter diameter
• Table feed (mm/min) = No. of revolutions
Feed per tooth
No. of inserts
Note: • RFEN2004M0TN type inserts should not be used for finishing requiring surface finish better than 12s.
• RFEN2004ZFTN type inserts can be used both finishing and roughing at depth of cut up to 3mm.
• RFEN2004M0TN does not have flattened flanks.


