E097
Tungaloy
Indexable Drill
ISO
DS, AH6030
-
-
DS, AH725
-
DW, AH6030 DG, AH725
DJ, AH6030 DW, AH6030 DJ, AH9030 DW, AH725 DJ, AH9030 DW, AH6030
-
DS, AH6030
-
-
DS, AH725
-
DW, AH6030
-
DS, AH6030
-
-
DS, AH725
-
DW, AH6030 DG, AH725
DJ, AH9030 DW, AH9030
DJ, T1115
DW, AH725
-
DW, AH9030
-
DJ, AH9030 DW, AH9030
-
DW, AH725
-
DW, AH9030
-
DJ, AH725
DW, AH725 DS, AH6030
-
DW, AH725
DG, AH725
DS, AH6030
-
-
DW, AH725
-
DW, AH725
DG, AH725
DJ, AH9030 DW, AH9030
-
DW, AH725
-
DW, AH9030
-
ISO
Vc (m/min)
ø55 ~ ø62
ø63 ~ ø73
ø74 ~ ø80
Low carbon steels (C < 0.3)
C15E4, E275A, E355D, etc.
160 - 320
0.04 - 0.1
0.04 - 0.1
0.04 - 0.1
Carbon steels (C > 0.3)
C45, C55, etc.
80 - 250
0.08 - 0.18
0.08 - 0.18
0.1 - 0.2
Low alloy steels
15CrMo5, etc.
160 - 250
0.04 - 0.16
0.04 - 0.16
0.04 - 0.16
Alloy steels
42CrMo4, 20Cr4, etc.
80 - 200
0.08 - 0.18
0.08 - 0.18
0.08 - 0.2
Stainless steels (Austenitic)
X5CrNi18-9, X5CrNiMo17-12-2, etc.
100 - 200
0.04 - 0.12
0.04 - 0.12
0.06 - 0.14
Stainless steels (Martensitic and ferritic)
X5CrNi18-9, X5CrNiMo17-12-2, etc.
100 - 200
0.04 - 0.12
0.04 - 0.12
0.06 - 0.14
Stainless steels (Precipitation hardening)
SUS630 etc. (X5CrNiCuNb16-4, etc.)
80 - 120
0.04 - 0.1
0.04 - 0.1
0.06 - 0.12
Grey cast irons
250, etc.
80 - 250
0.08 - 0.2
0.08 - 0.2
0.1 - 0.22
Ductile cast irons
600-3, etc.
80 - 200
0.08 - 0.2
0.08 - 0.2
0.1 - 0.22
Aluminium alloys
AlCu4SiMg, AlSi11Cu3, etc.
200 - 400
0.15 - 0.25
0.15 - 0.25
0.18 - 0.28
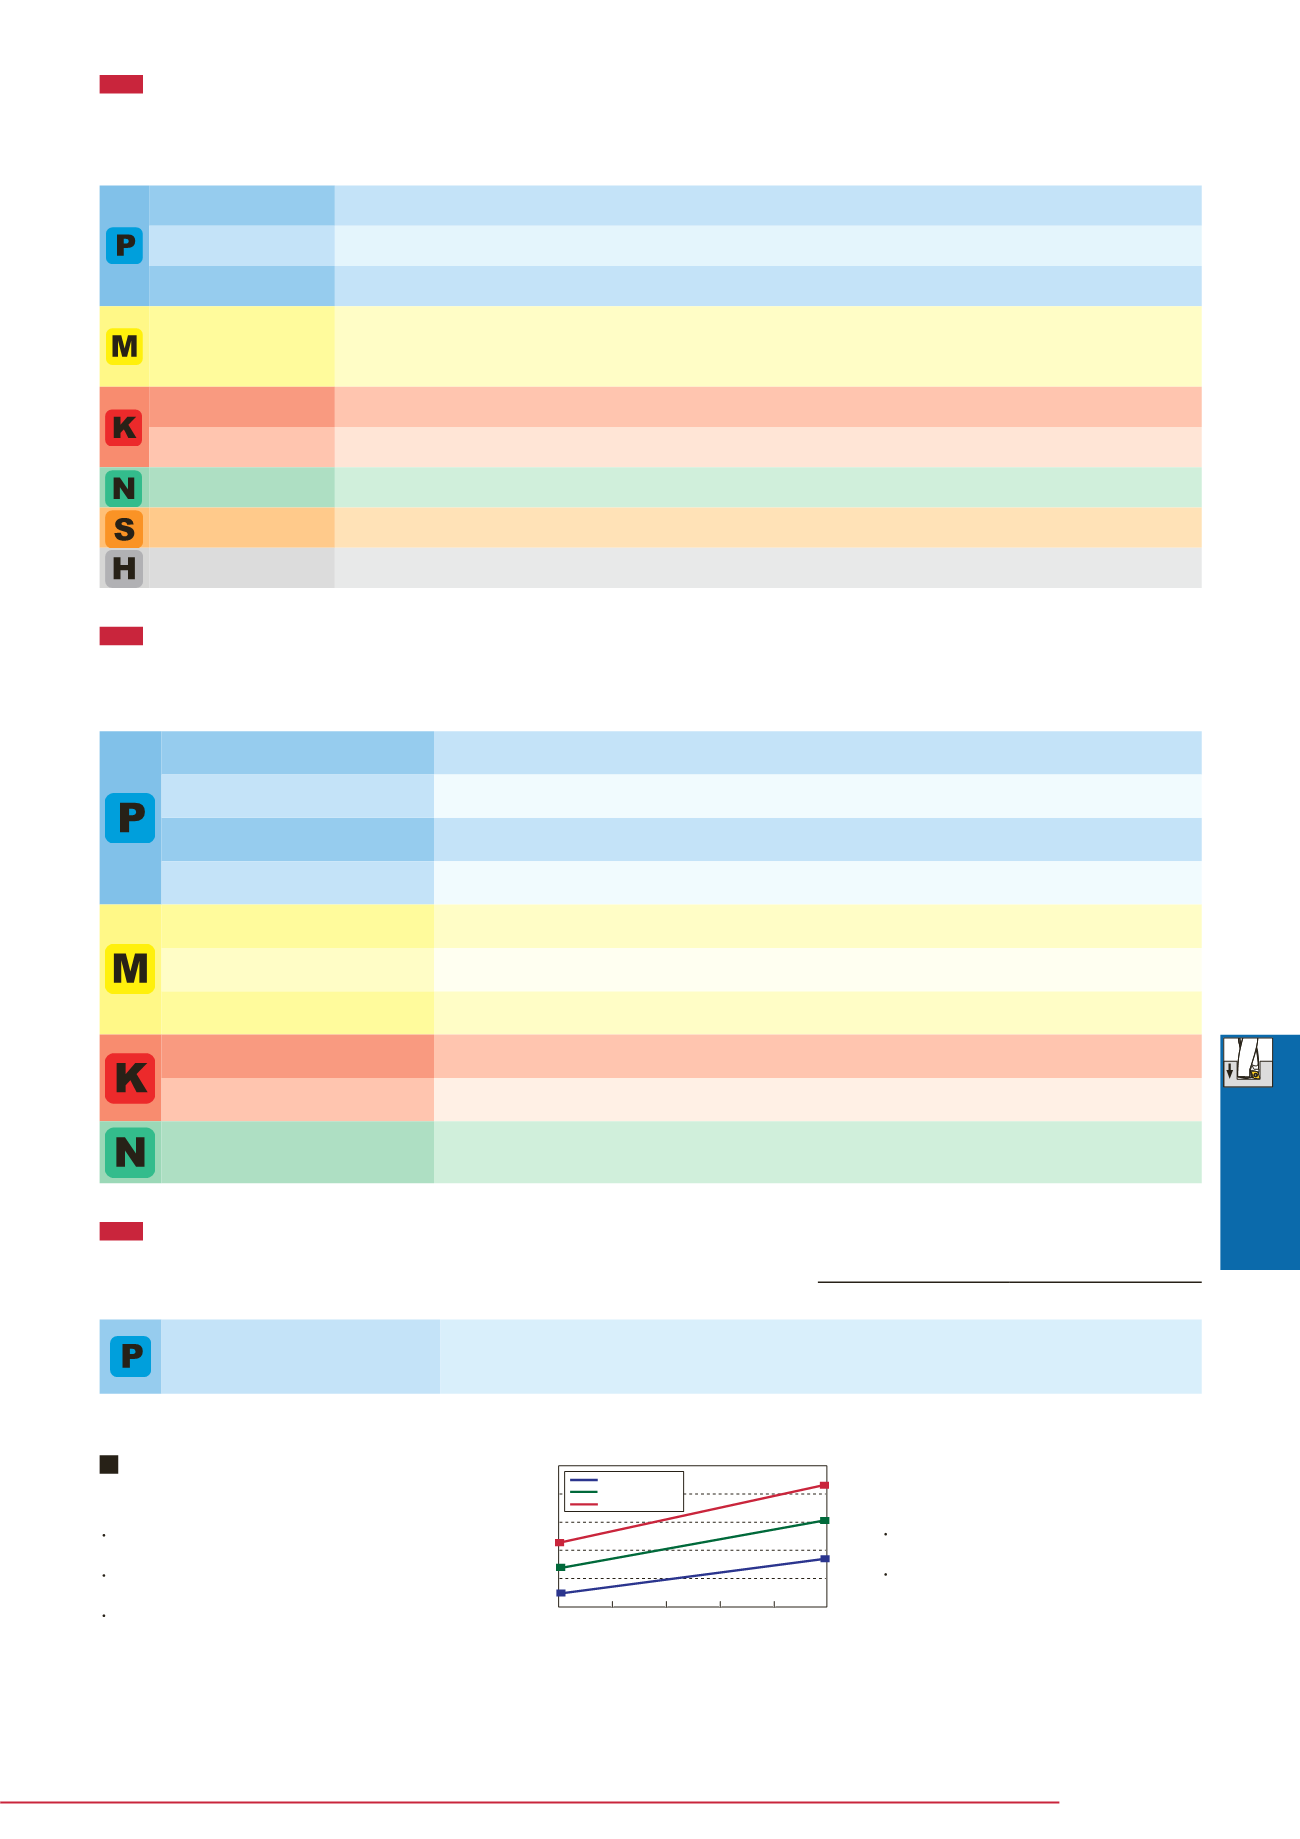
f
= 0.1 mm/rev
f
= 0.2 mm/rev
f
= 0.15 mm/rev
35
30
25
20
15
10
55
60
65
70
75
80
V
c = 180 m/min
Caution
Use drills on a fully covered machine to maintain
safety.
Use drills on a high powered machine such as a
BT50.
Figure on right shows reference of required
machine power.
Machine
Cutting coolant
Use water soluble type coolant
with internal supply.
Coolant pressure higher than 1MPa is
essential.
INSERTS RECOMMENDATION
STANDARD CUTTING CONDITIONS
STANDARD CUTTING CONDITIONS FOR DG CHIPBREAKER
Workpiece material First choice High feed High speed Chipping
resistance
Wear
resistance
Surface
finish
Chip
control
Troubleshooting
Low carbon steel
(C ≤ 0.3%)
Low alloy steel
Carbon steel (C > 0.3%)
Alloy steels
Stainless steel
Titanium alloys
Heat-resistant alloys
Grey cast iron
Ductile cast iron
Aluminium alloys
High hardened steels
Feed: f (mm/rev)
Cutting speed
Workpiece material
ISO
Workpiece material
Cutting speed
Vc (m/min)
Series
L/D
Feed
: f (mm/rev)
ø27 ~ ø32
ø33 ~ ø54
Low carbon steels (C < 0.3)
C15E4, E275A, E355D, etc.
60 - 180
2D, 3D
0.04 - 0.1
4D, 5D
Power consumption (kW)
Tool diameter: øDc (mm)


