E094
Indexable Drill
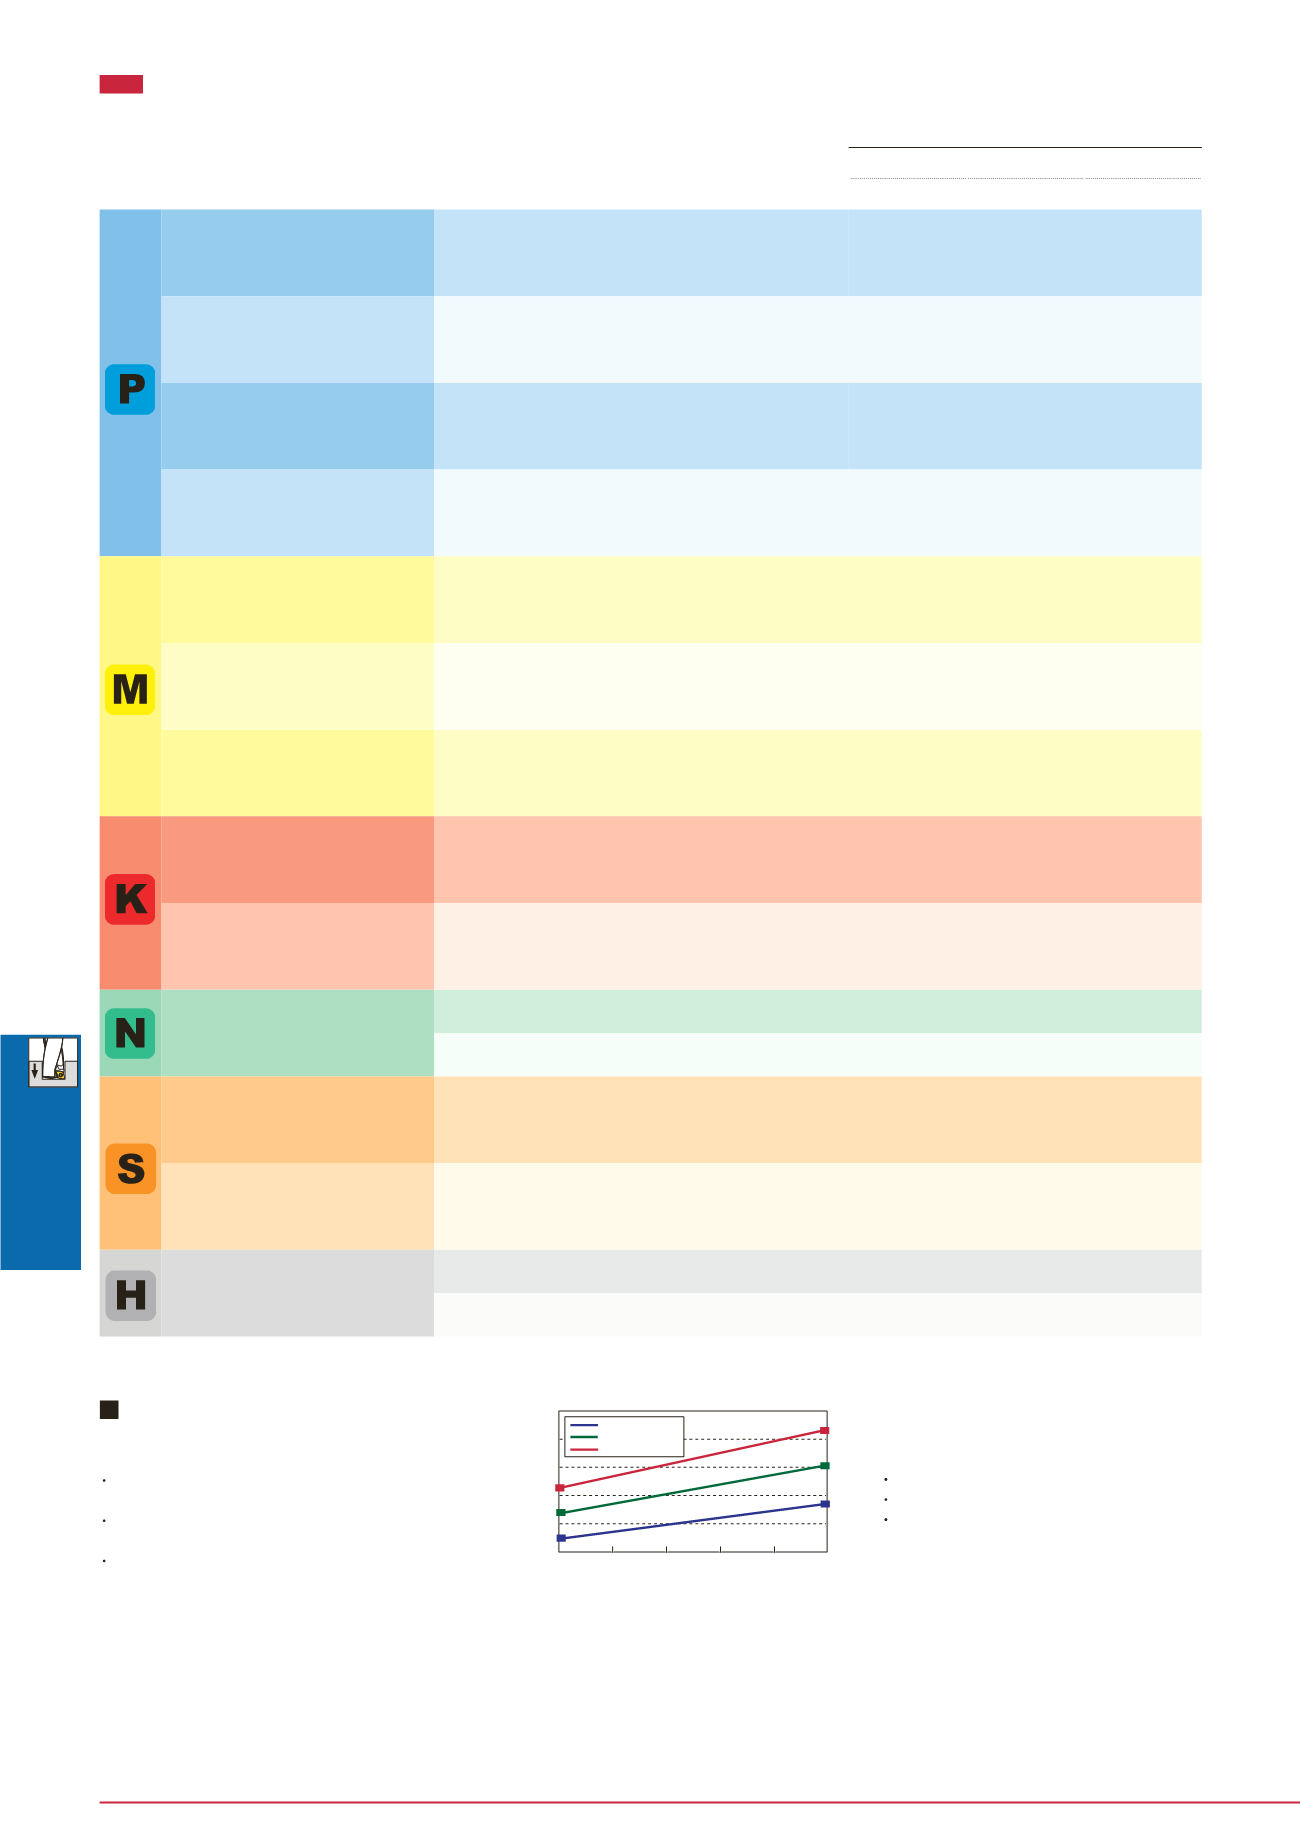
f
= 0.1 mm/rev
f
= 0.2 mm/rev
f
= 0.15 mm/rev
35
30
25
20
15
10
55
60
65
70
75
80
V
c = 180 m/min
Caution
Use drills on a fully covered machine to maintain
safety.
Use drills on a high powered machine such as a
BT50.
Figure on right shows reference of required
machine power.
Machine
ISO
øDc (mm)
Vc (m/min)
ø55 - 56
ø57 - 73
ø74 - 80
Low carbon steels (C<0.3)
C15E4, E275A, E355D, etc.
DS AH6030 160 - 250
0.04 - 0.1
0.04 - 0.1
0.04 - 0.1
DJ
AH9030 160 - 320
0.04 - 0.1
0.04 - 0.1
0.04 - 0.1
Carbon steels (C>0.3)
C45, C55, etc.
DJ
AH9030 80 - 250
0.06 - 0.16
0.06 - 0.18
0.08 - 0.2
DS AH6030 80 - 250
0.04 - 0.13
0.04 - 0.15
0.04 - 0.16
Low alloy steels
18CrMo4, etc.
DS AH6030 160 - 250 0.04 - 0.12
0.04 - 0.12
0.04 - 0.12
DJ
AH9030 160 -250 0.06 - 0.14
0.06 - 0.14
0.06 - 0.14
Alloy steels
42CrMo4, 20Cr4, etc.
DJ
AH9030
80 - 200
0.06 - 0.16
0.06 - 0.18
0.08 - 0.2
DS AH6030
80 - 200
0.04 - 0.13
0.04 - 0.14
0.04 - 0.15
Stainless steels (Austenitic)
X5CrNi189,
X5CrNiMo17-12-2, etc.
DS AH6030 100 - 200 0.04 - 0.12
0.04 - 0.12
0.04 - 0.12
DJ
AH9030 100 - 200 0.04 - 0.12
0.04 - 0.12
0.04 - 0.12
Stainless steels
(Martensitic and ferritic)
X6Cr17, X12CrS13, etc.
DS AH6030 100 - 200 0.04 - 0.12
0.04 - 0.12
0.04 - 0.12
DJ
AH9030 100 - 200 0.04 - 0.12
0.04 - 0.12
0.04 - 0.12
Stainless steels
(Precipitation hardening)
X5CrNiCuNb16-4, etc.
DS AH6030
80 - 120
0.04 - 0.1
0.04 - 0.1
0.04 - 0.1
DJ
AH9030
80 - 120
0.04 - 0.1
0.04 - 0.1
0.04 - 0.1
Grey cast irons
250, etc.
DJ
AH9030
80 - 250
0.06 - 0.18
0.08 - 0.2
0.08 - 0.22
DS AH6030 80 - 200 0.06 - 0.15
0.08 - 0.16
0.08 - 0.18
Ductile cast irons
700-2, etc.
DJ
AH9030
80 - 200
0.06 - 0.16
0.06 - 0.18
0.08 - 0.2
DS AH6030
80 - 150
0.06 - 0.15
0.08 - 0.16
0.08 - 0.18
Aluminium alloys
DS AH6030 200 - 400
0.1 - 0.2
0.1 - 0.23
0.1 - 0.25
DJ
AH9030 200 - 400
0.1 - 0.2
0.1 - 0.23
0.1 - 0.25
High temperature alloys
Innconel718, etc.
DS AH6030
20 - 60
0.04 - 0.08
0.04 - 0.1
0.04 - 0.1
DJ
AH9030
20 - 60
0.04 - 0.08
0.04 - 0.1
0.04 - 0.1
Titanium alloys
Ti-6Al-4V, etc.
DS AH6030
40 - 120
0.06 - 0.12
0.06 - 0.14
0.06 - 0.14
DJ
AH9030
40 - 120
0.06 - 0.12
0.06 - 0.14
0.06 - 0.14
High hardened steels
< 40HRC
DJ
AH9030
50 - 100
0.04 - 0.08
0.04 - 0.1
0.04 - 0.1
DS AH6030
40 - 80
0.04 - 0.08
0.04 - 0.1
0.04 - 0.1
STANDARD CUTTING CONDITIONS
Cutting
speed
Selection
criteria
Chip-
breaker Grade
First choice
For wear resistance
First choice
For impact resistance
First choice
For wear resistance
First choice
For impact resistance
First choice
―
First choice
―
First choice
―
First choice
For impact resistance
First choice
For impact resistance
First choice
―
First choice
―
First choice
―
First choice
For impact resistance
Workpiece material
Feed: f (mm/rev)
Cutting coolant
Use water soluble type coolant
with internal supply.
Coolant pressure higher than 1MPa is
essential.
Tool diameter: øDc (mm)
Power consumption (kW)


