D144
Face Milling
-
-
-
-
Notes:
(1) When requiring improved surface finish, use the wiper insert together
with regular inserts YDEN0905PDFR-WD.
(2) When requiring reduced burr occurrence, use the deburring inserts
together with regular inserts YDEN0905PDFR-BD.
(3) When using the cutter at speeds over 1500m/min, use an arbor or tool-
holder balanced to within G16.
(4) Wet cutting, using a water soluble cutting fluid, is recommended.
(5) When the length-to-diameter overhang ratio of the tool (L/D) exceeds 3,
reduce cutting speed and feed to 70 to 80% of the values given in the
table.
ISO
Workpiece material
Grade
Designation
Cutting speed
Vc (m/min)
Feed per tooth
fz (mm/t)
Aluminium alloy castings &
die castings Si < 13%
DX140
YDEN0905PDFR-D
500 ~ 4000
0.05 ~ 0.2
Aluminium alloy castings &
die castings Si ≥ 13%
DX140
YDEN0905PDFR-D
200 ~ 500
0.05 ~ 0.2
Rolled aluminium alloys
DX140
YDEN0905PDFR-D
500 ~ 4000
0.05 ~ 0.2
Copper alloys
DX140
YDEN0905PDFR-D
200 ~ 500
0.05 ~ 0.2
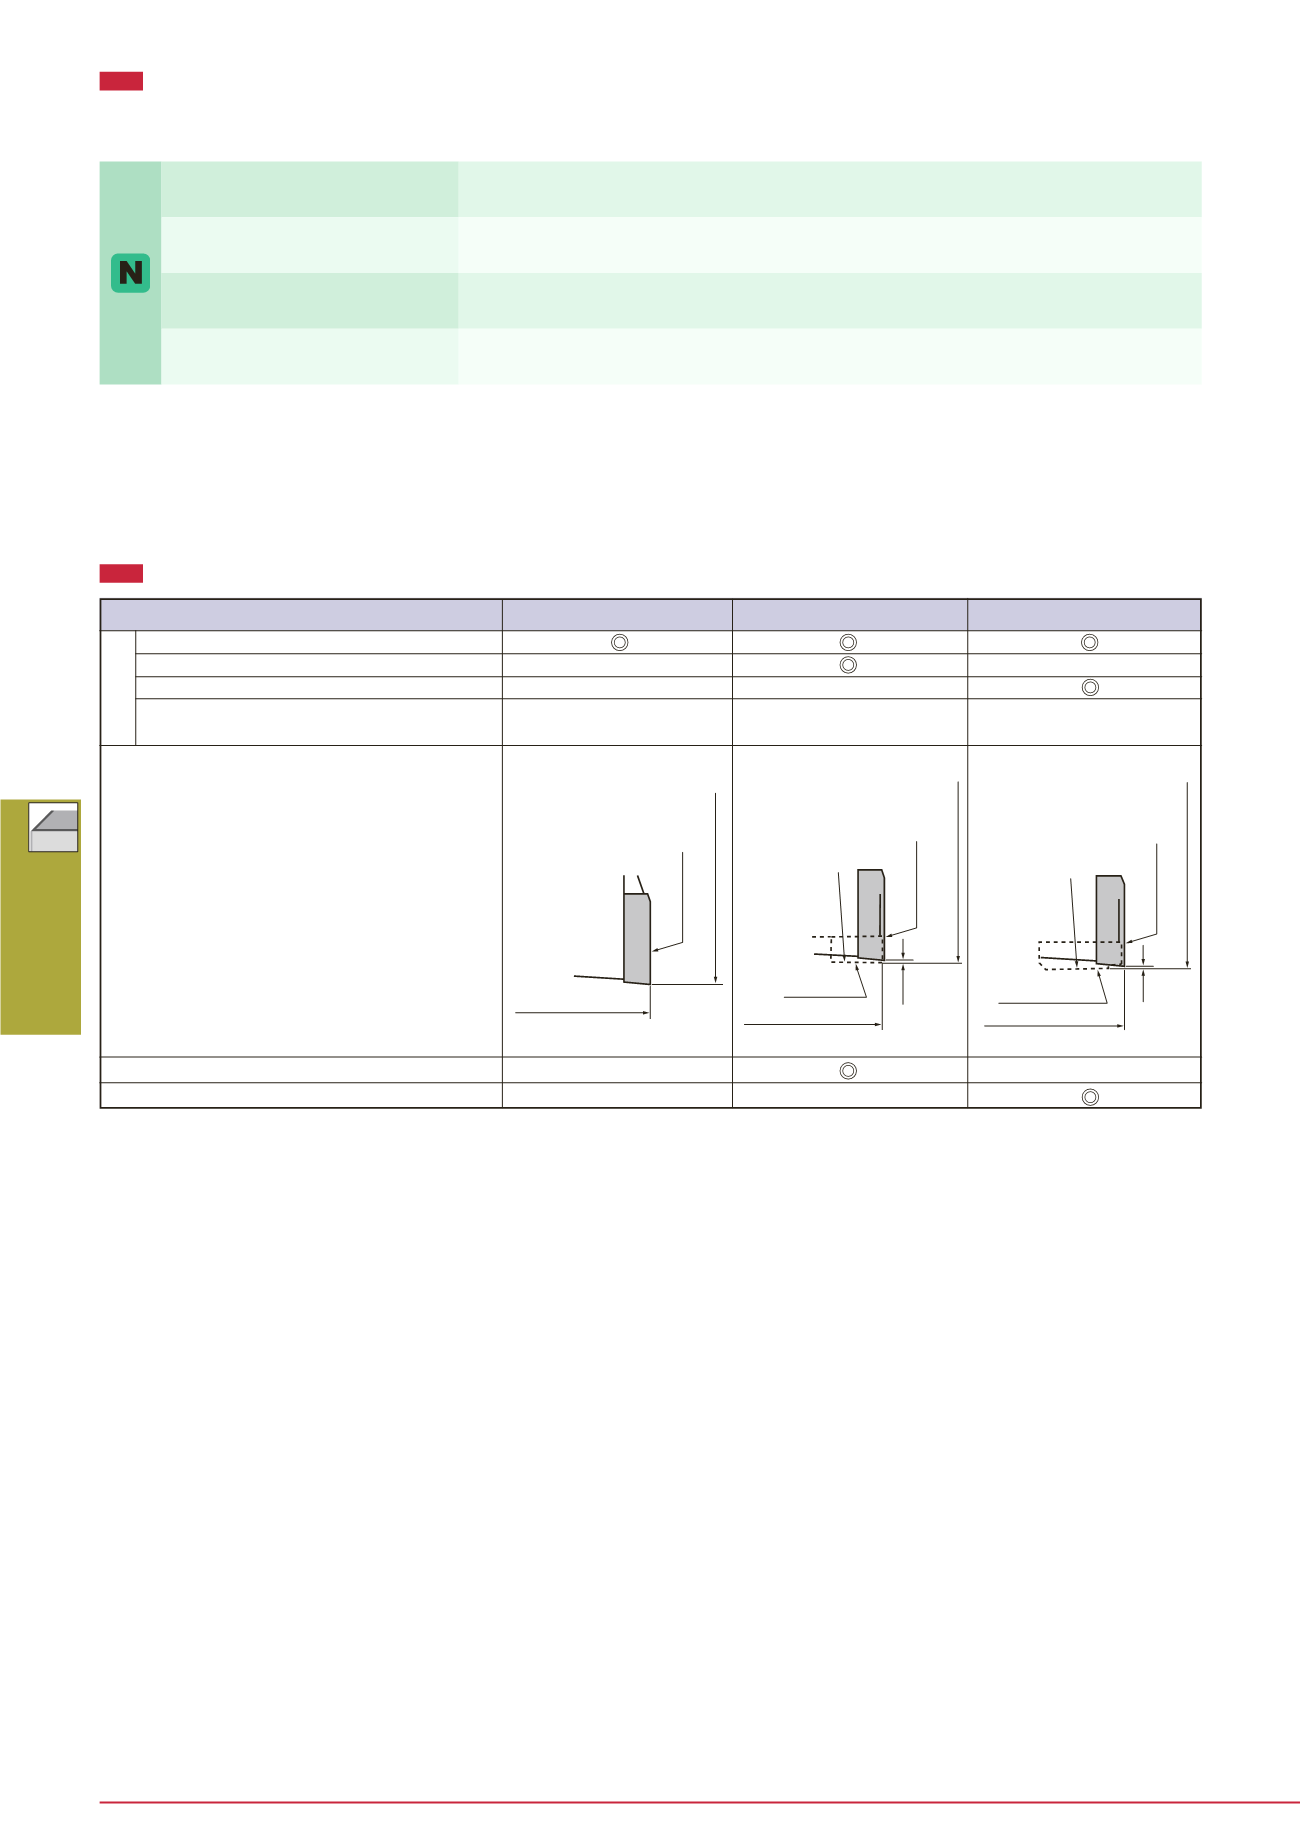
STANDARD CUTTING CONDITIONS
Applicable insert
General insert
YDEN0905PDFR-D
Wiper insert
YDEN0905PDFR-WD
Wiper insert for burr reduction
YDEN0905PDFR-BD
Number of Inserts by type
Specification of insert setting
Accuracy of machining surface (roughness and undulation)
Burr of machining surface
All general
General insert : Burr wiper insert
= 1 : 1
1 or 2 wiper inserts in
cutter body
For general
Burr reduction priority
Accuracy of machining surface priority
øD : Cutter diameter
General insert
F : Height from cutting edge
R
0.05
Wiper insert
øD : Cutter diameter
General insert
F : Height from cutting edge
R
0.2
Wiper insert for
burr reduction
øD : Cutter diameter
General insert
F : Height from cutting edge
HOW TO PUT EACH INSERT TOGETHER


