D116
ISO
ø4
120 - 180
12,000
120
ø5
120 - 180
9,600
120
ø6
120 - 180
8,000
120
ø8
120 - 180
6,000
120
ø10
120 - 180
4,800
120
ø12
120 - 180
4,000
100
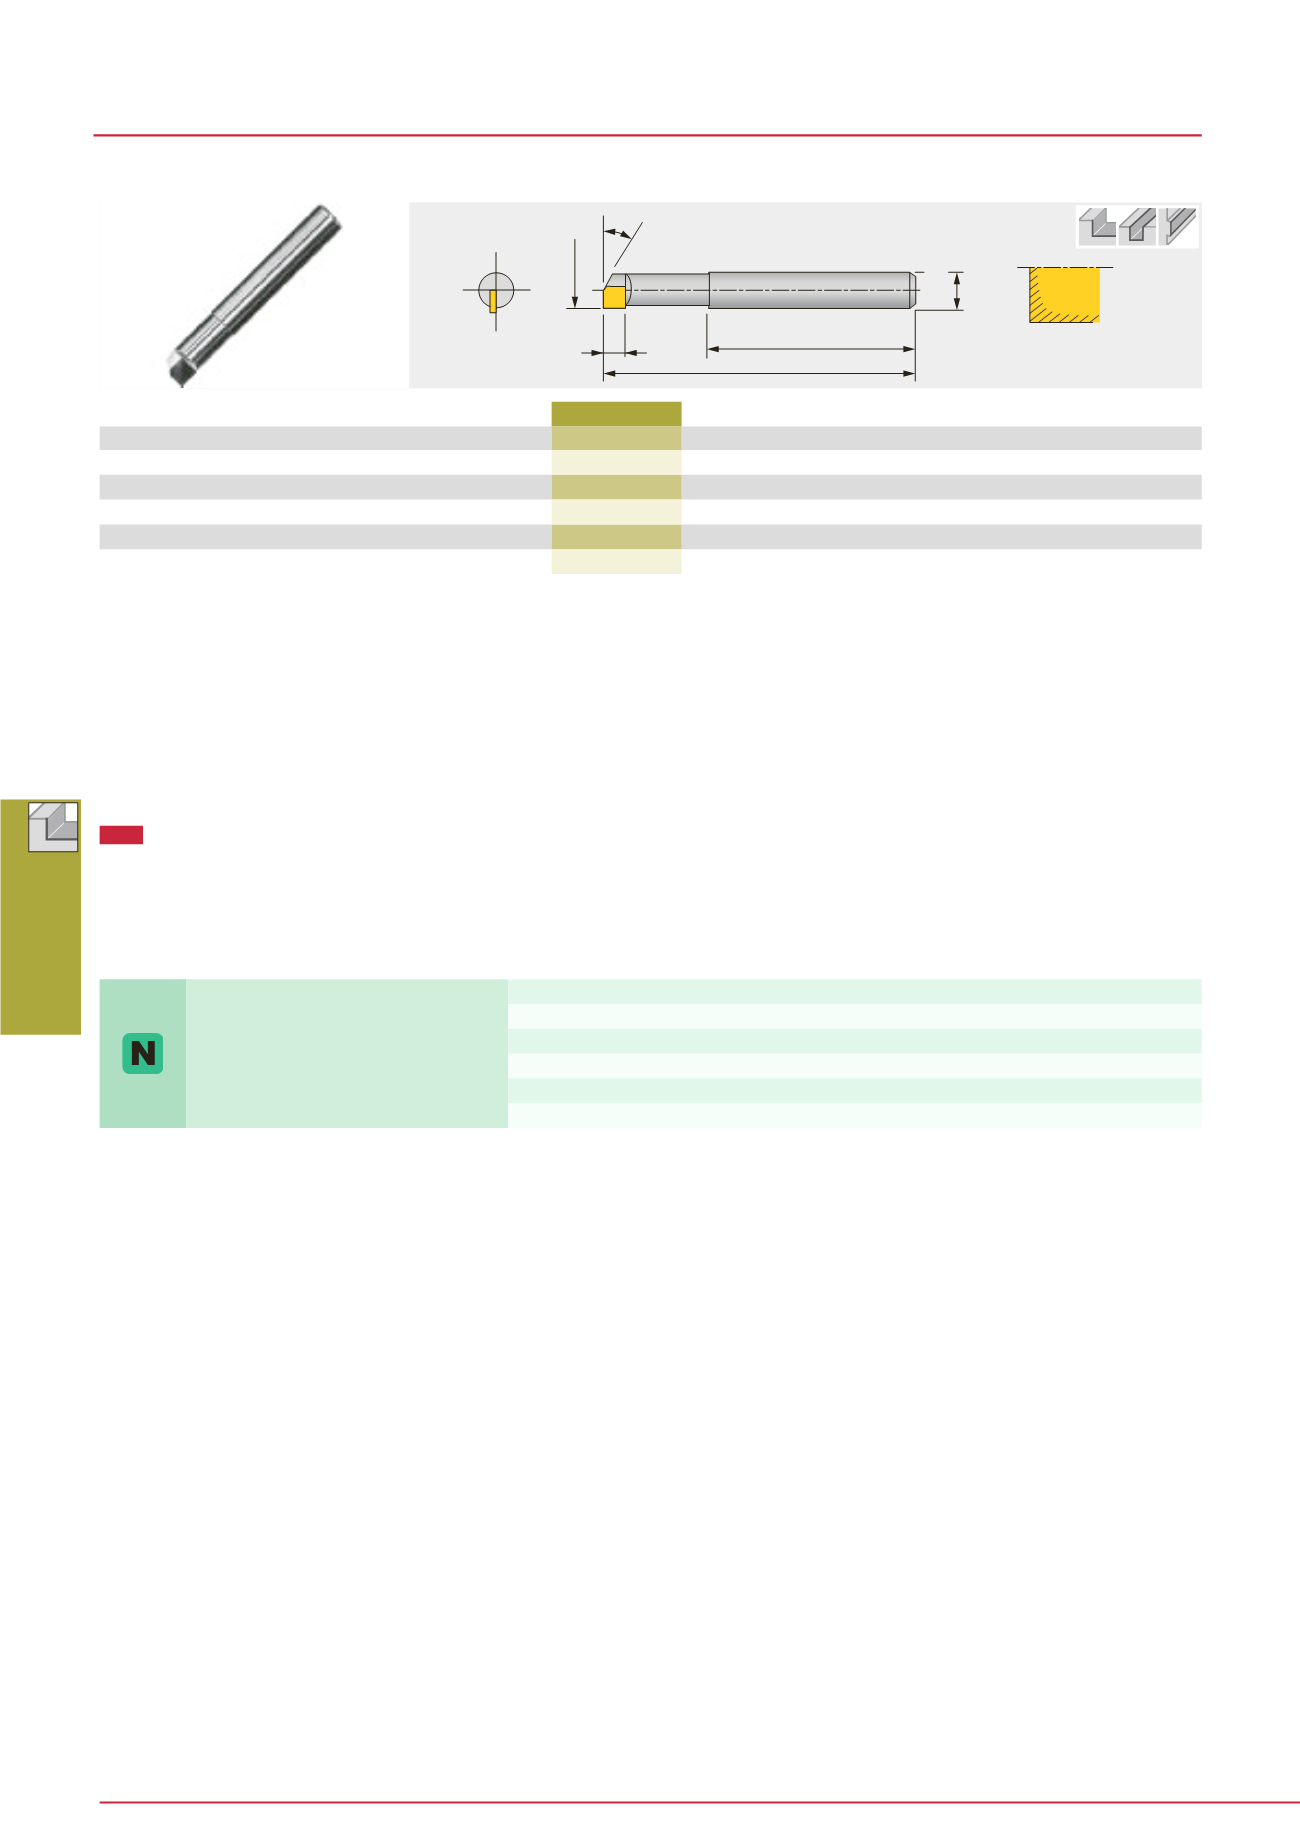
Shoulder Milling
DEB1000
30°
R
R
s
øDsh
7
L
øDc
–0.05
0
Designation
DX140
Z
øD
c
øD
s
ℓ
ℓ
s
L
DEB1040
1
4
6
3.5
32
45
DEB1050
1
5
6
3.5
35
50
DEB1060
1
6
6
3.5
35
50
DEB1080
1
8
8
5
37
55
DEB1100
1
10
10
5
40
60
DEB1120
1
12
12
5
45
65
DEB1000
T-DIA Endmill
Notes:
• As cutting edge is very sharp, please handle carefully.
• Please keep the overhang length from milling chuck of tool as short as possible.
STANDARD CUTTING CONDITIONS
Aluminium alloys, Copper alloys
- Set the protrusion length as short as possible. Reduce number
of revolutions and table feed in order to prevent chattering
when the protrusion length is long.
- Use the machine with high rigidity.
- Adjust the number of revolutions and the table feed according
to the situation of use. (depth of cut or machine rigidity etc.)
For side milling
a
p
≤ 3D,
a
e
= 0.1 mm
Corner of cutting edge:
Sharp edge
Workpiece material
Mill dia.
(mm)
Cutting Speed
Vc (m/min)
No. of revolutions
n (min
-1
)
Table feed
Vf (mm/min)
l
: Line-up


