D051
Tungaloy
Shoulder Milling
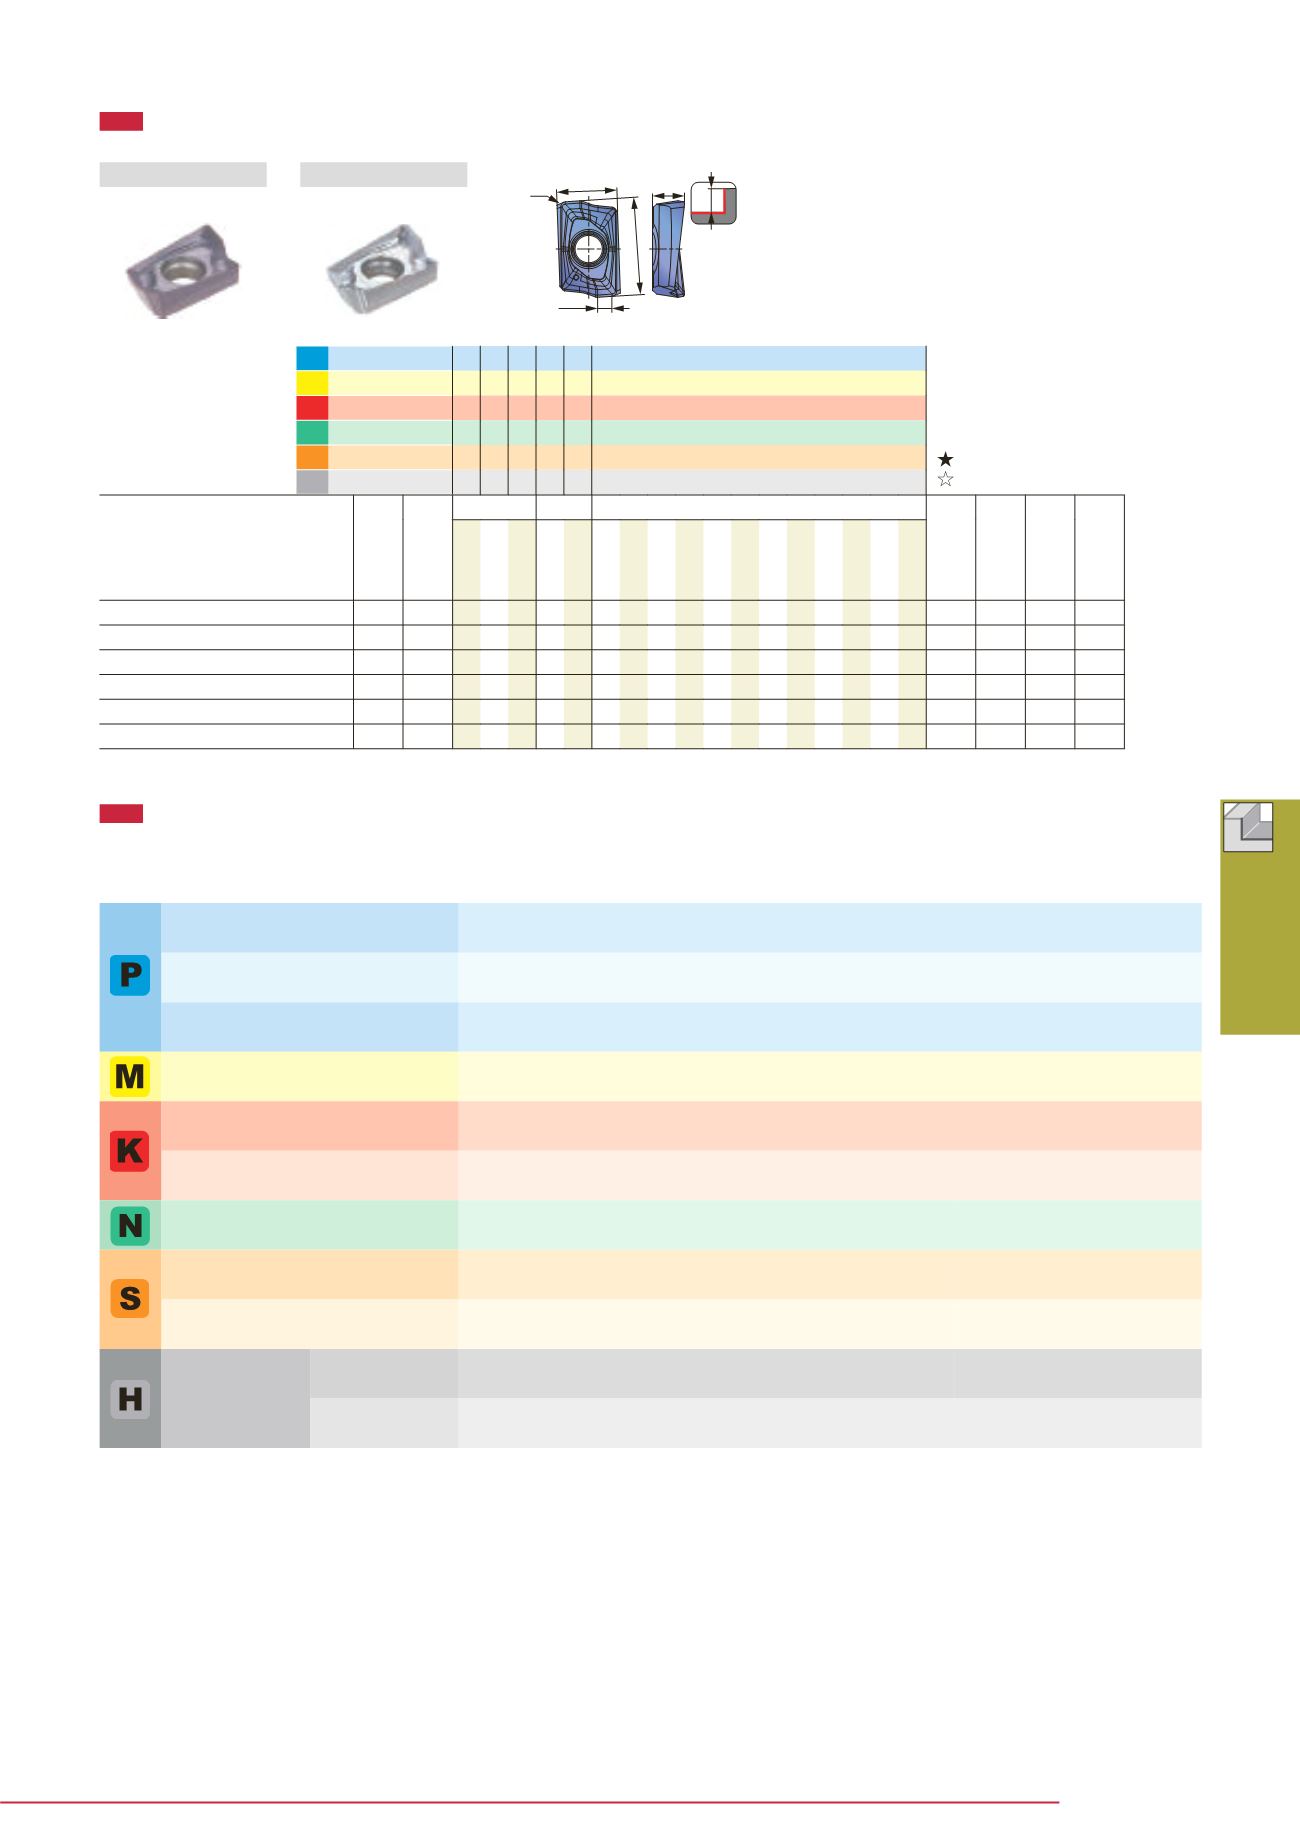
AVGT-AJ
AVGT-MJ
r
ε
B
A
T
bs
ap
INSERT
STANDARD CUTTING CONDITIONS
P Steel
M Stainless
K Cast iron
N Non-ferrous
S Superalloys
H Hard materials
Designation
r
ε Max.
a
p
Coating
Un-
coated
A B T bs
AH120
AH3135
KS05F
AVGT060302PBER-MJ
0.2 6
l l
8 5 2.7 1.5
AVGT060304PBER-MJ
0.4 6
l l
8 5 2.7 1.3
AVGT060308PBER-MJ
0.8 6
l l
8 5 2.6 0.9
AVGT060302PBFR-AJ
0.2 6
l
8 5 2.7 1.5
AVGT060304PBFR-AJ
0.4 6
l
8 5 2.7 1.3
AVGT060308PBFR-AJ
0.8 6
l
8 5 2.6 0.9
l
: Line-up
: First choice
: Second choice
ISO
- 300 HB
AH3135
MJ
230 - 430
0.07 - 0.12
- 300 HB
AH3135
MJ
150 - 350
0.07 - 0.12
30 - 40 HRC
AH120
MJ
100 - 230
0.07 - 0.12
-
AH3135
MJ
150 - 220
0.06 - 0.1
150 - 250 HB
AH120
MJ
200 - 330
0.07 - 0.12
150 - 250 HB
AH120
MJ
150 - 240
0.07 - 0.12
-
KS05F
AJ
650 - 1000
0.07 - 0.12
-
AH120
MJ
70 - 90
0.06 - 0.1
-
AH120
MJ
45 - 65
0.06 - 0.09
40 - 50 HRC
AH120
MJ
45 - 70
0.05 - 0.08
50 - 60 HRC
AH120
MJ
40 - 65
0.04 - 0.06
First choice
First choice
First choice
First choice
First choice
First choice
First choice
First choice
First choice
First choice
First choice
Chip-
breaker
Low carbon steel
C15E4, E275A, etc.
Carbon steel and alloy steel
C55, 42CrMo4, etc.
Prehardened steel
NAK80, PX5, etc.
Stainless steel
X5CrNi18-9, X5CrNiMo17-12-3, etc.
Grey cast iron
250, 300, etc.
Ductile cast iron
600-3, etc.
Aluminium alloys
Si < 13%
Titanium alloys
Ti-6AI-4V, etc.
Superalloys
nconel718, etc.
Hardened steel
X40CrMoV5-1, etc.
X153CrMoV12, etc.
Cutting speed
Vc (m/min)
Feed per tooth
fz (mm/t)
Workpiece material
Grade
Hardness
Priority


