D071
Tungaloy
Shoulder Milling
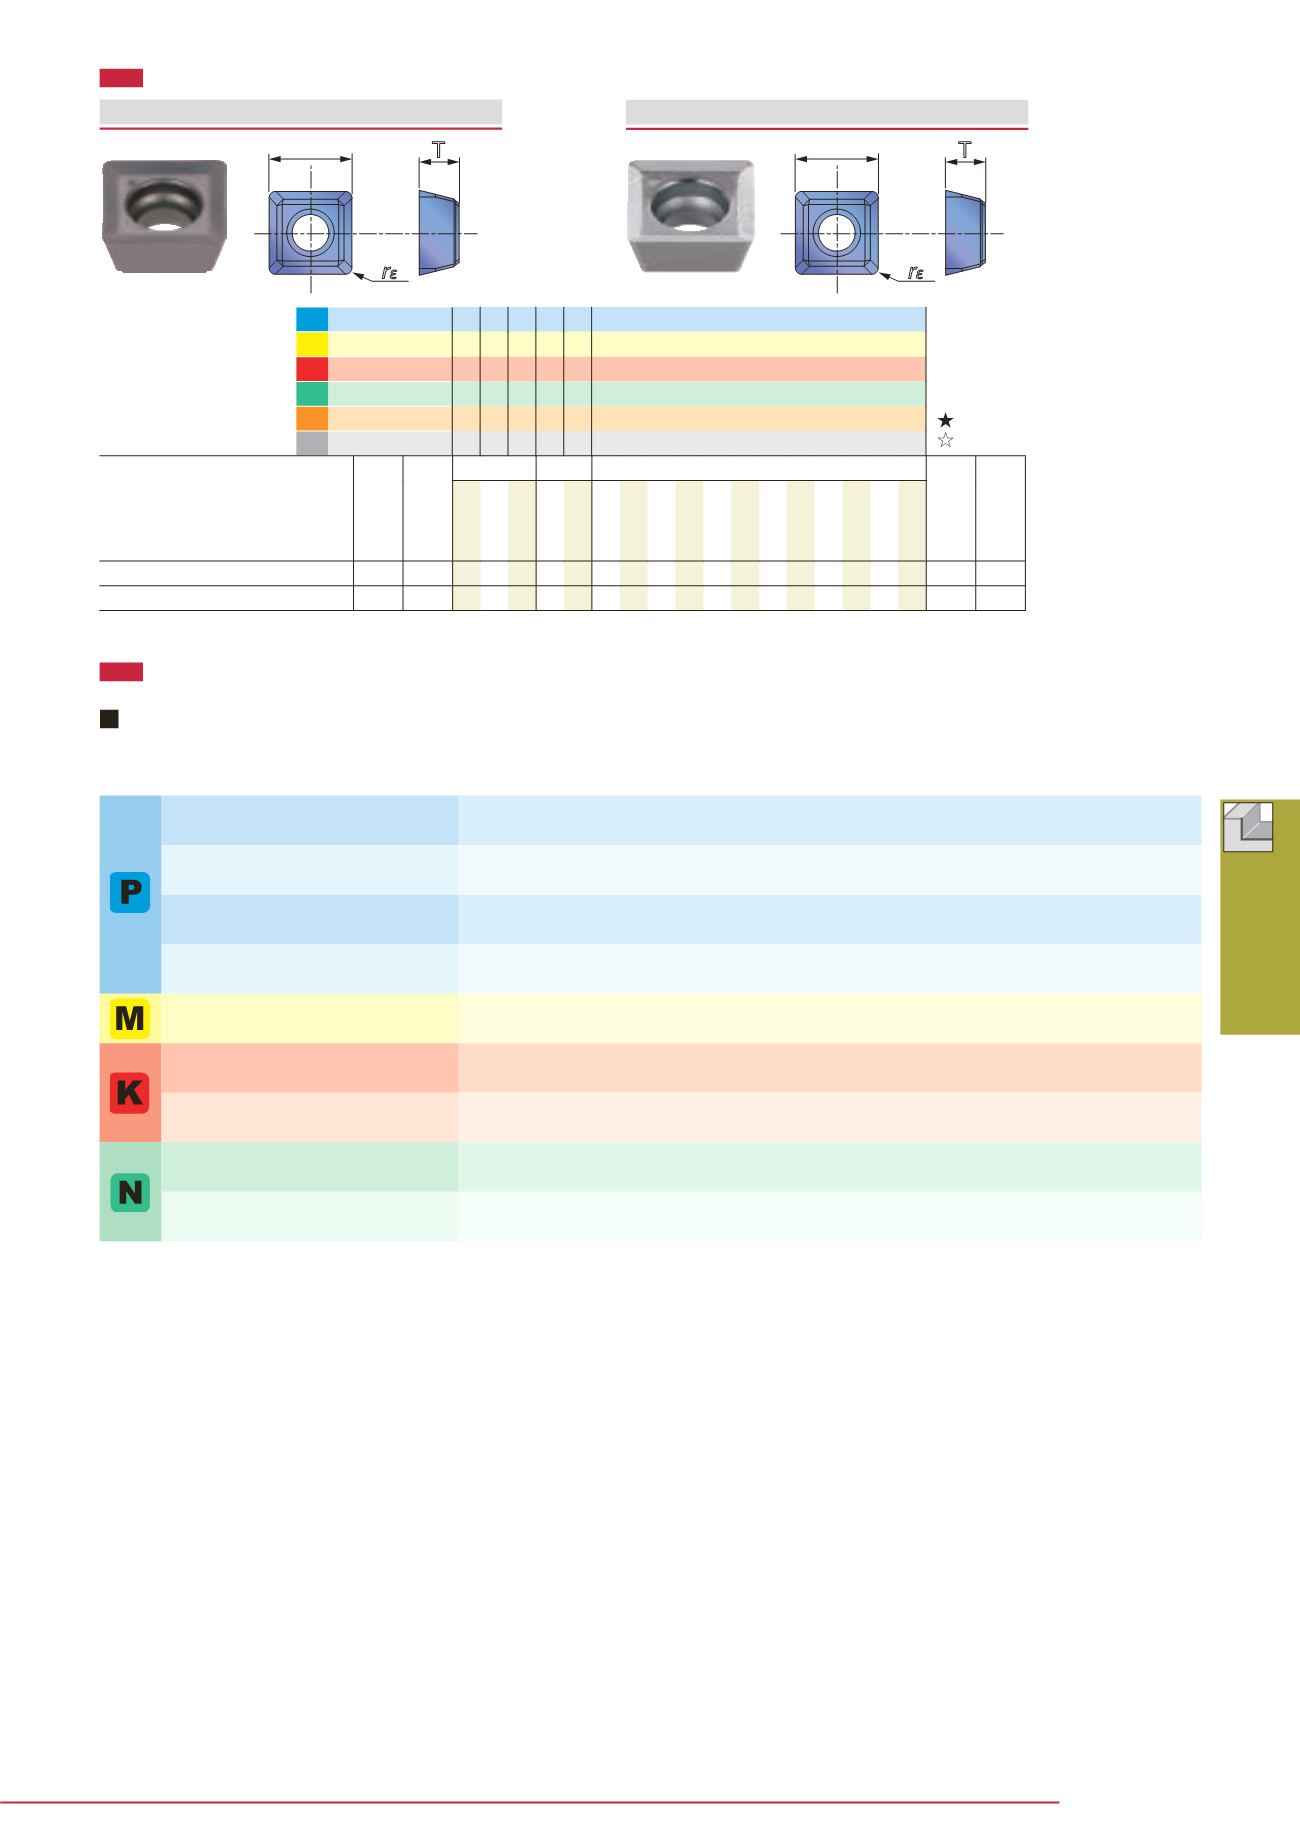
SDHT05-AJ
r
ε
T
ød
r
ε
T
ød
INSERT
SDMT05-MJ
ISO
~ 200
AH725
230 - 320
0.04 - 0.1
200 ~ 300
AH725
150 - 230
0.04 - 0.1
150 ~ 300
AH725
150 - 230
0.04 - 0.1
~ 300
AH725
110 - 130
0.03 - 0.09
-
AH140
100 - 200
0.03 - 0.09
150 ~ 250
AH725
200 - 300
0.05 - 0.12
150 ~ 250
AH725
160 - 240
0.05 - 0.12
-
TH10
350 - 500
0.05 - 0.15
-
TH10
100 - 200
0.05 - 0.15
STANDARD CUTTING CONDITIONS
* For deep and wide cutting, set the
V
c and
f
z to the lower recommended limits and check the vibration and spindle load of the machine.
Bore, shank type
TPD05/EPD05
Low carbon steels
C15E4, etc.
High carbon steels
C45, etc.
Alloyed steels
42CrMo4, etc.
Tool steels
X153CrMoV12, etc.
Stainless steels
X5CrNi18-9, etc.
Grey cast irons
250, etc.
Ductile cast irons
450-10S, etc.
Aluminium alloys
Si < 13%
Aluminium alloys
Si ≥ 13%
Cutting speed
Vc (m/min)
Feed per tooth
fz (mm/t)
Workpiece material
Grade
Brinell hardness
HB
P Steel
M Stainless
K Cast iron
N Non-ferrous
S Superalloys
H Hard materials
Designation
r
ε Max.
a
p
Coating
Un-
coated
T ø
d
AH140
AH725
TH10
SDMT050204PN-MJ
0.4 4
l l
2.38 5.09
SDHT050204FN-AJ
0.4 4
l
2.39 5.09
l
: Line-up
: First choice
: Second choice


