C031
Tungaloy
2−
r
ε
G
2°
w
20.0
8.0
4.50
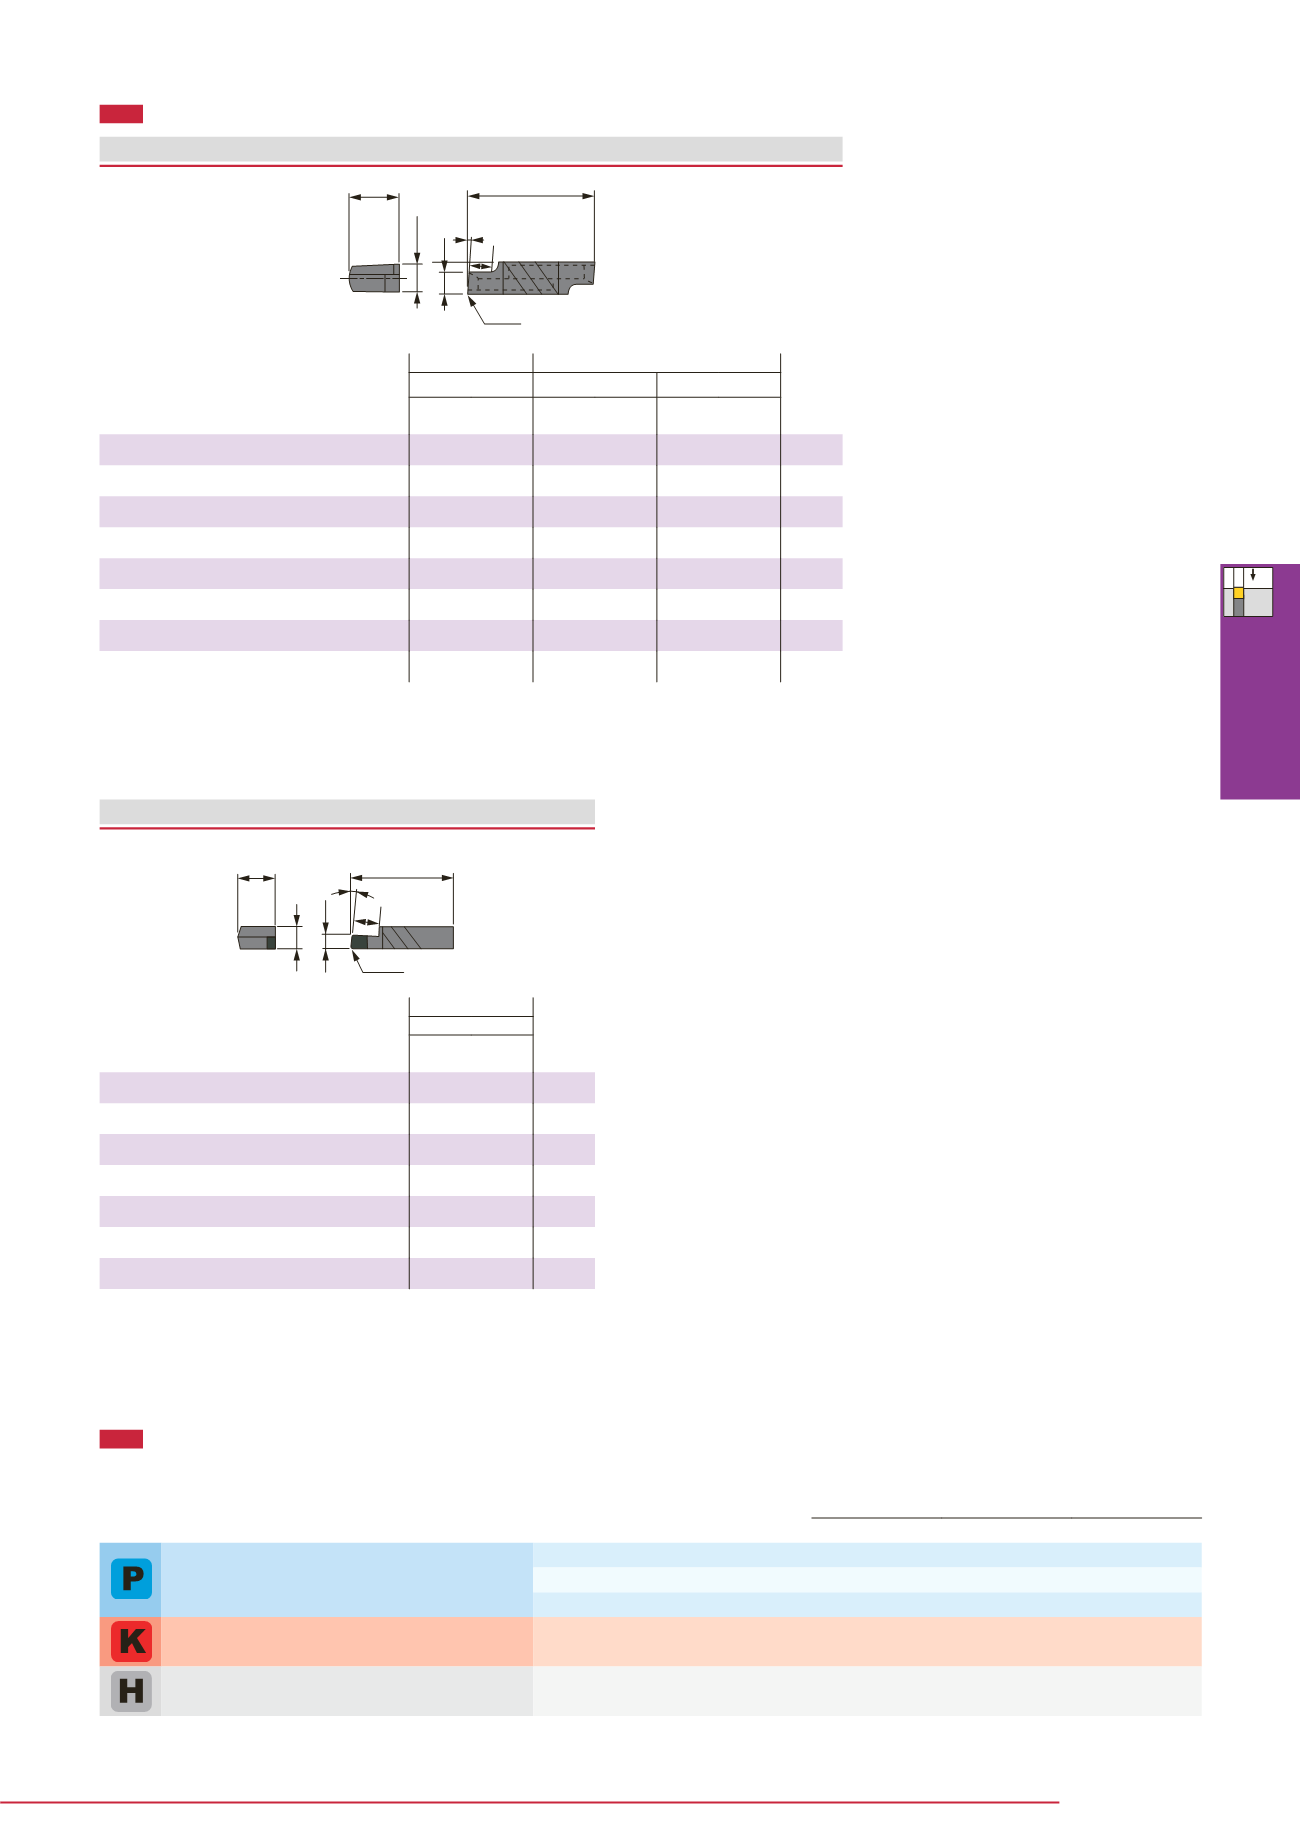
Designation W
±0.05
r
ε
Cermet
Uncoated
NS9530
TH10
UX30
R L R L R L G
XGR/L6310-02
1
0.2
● ● ● ● ● ●
1.5
XGR/L6315-02
1.5 0.2
● ● ● ● ● ●
2.3
XGR/L6320-02
2
0.2
● ● ● ● ● ●
3
XGR/L6325-02
2.5 0.2
● ● ● ● ● ●
3.8
XGR/L6330-02
3
0.2
● ● ● ● ● ●
4.5
XGR/L6335-02
3.5 0.2
● ● ● ● ● ●
5.3
XGR/L6340-02
4
0.2
● ● ● ● ● ●
6
XGR/L6345-02
4.5 0.2
● ● ● ● ● ●
6
XGR/L
INSERT
Right hand (R) shown.
T
-
CBN
Designation W
±0.05
r
ε
BX360
R L G
XGR/L6315S-QBN
1.5 0.2
●
2.3
XGR/L6320S-QBN
2
0.2
●
3
XGR/L6325S-QBN
2.5 0.2
●
3.8
XGR/L6330S-QBN
3
0.2
●
4.5
XGR/L6335S-QBN
3.5 0.2
●
5.3
XGR/L6340S-QBN
4
0.2
●
6
XGR/L6345S-QBN
4.5 0.2
●
6
2
−r
ε
G
20
4.5
8.0
2°
w
XGR/L-QBN
●
:
Line-up
Right hand (R) shown.
STANDARD CUTTING CONDITIONS
Note;
For internal machining, use right-hand toolholder (GX-****RI) with left-hand insert (XGL****),
and use left-hand toolholder (GX-****LI) with right-hand insert (XGR****).
For external machining, use right-hand toolholder (GX-****RE) with right-hand insert (XGR****),
and use left-hand toolholder (GX-****LE) with left-hand insert (XGL****).
Note;
For internal machining, use right-hand toolholder (GX-****RI) with left-hand insert (XGL****),
and use left-hand toolholder (GX-****LI) with right-hand insert (XGR****).
For external machining, use right-hand toolholder (GX-****RE) with right-hand insert (XGR****),
and use left-hand toolholder (GX-****LE) with left-hand insert (XGL****).
ISO
W
< 2 mm
W
= 2 ~ 4 mm
W
> 4 mm
NS9530
80 - 200
0.05 - 0.1
0.08 - 0.2
0.08 - 0.25
TX10S
60 - 150
0.05 - 0.1
0.08 - 0.2
0.08 - 0.25
UX30
60 - 150
0.05 - 0.1
0.08 - 0.2
0.08 - 0.25
TH10
60 - 150
0.05 - 0.1
0.08 - 0.2
0.08 - 0.25
BX360
50 - 180
0.05 - 0.15
0.05 -
0.15
0.05 -
0.15
Cutting speed
v
c
(m/min)
Feed
f
(mm/rev)
Workpiece material
Carbon steels
Cast irons , Light alloys
Grade
Hardened steels
●
:
Line-up
Grooving Tool


