C027
Tungaloy
Designation
Cermet
Uncoated
W
±0.025
r
ε
NS9530
TH10
UX30
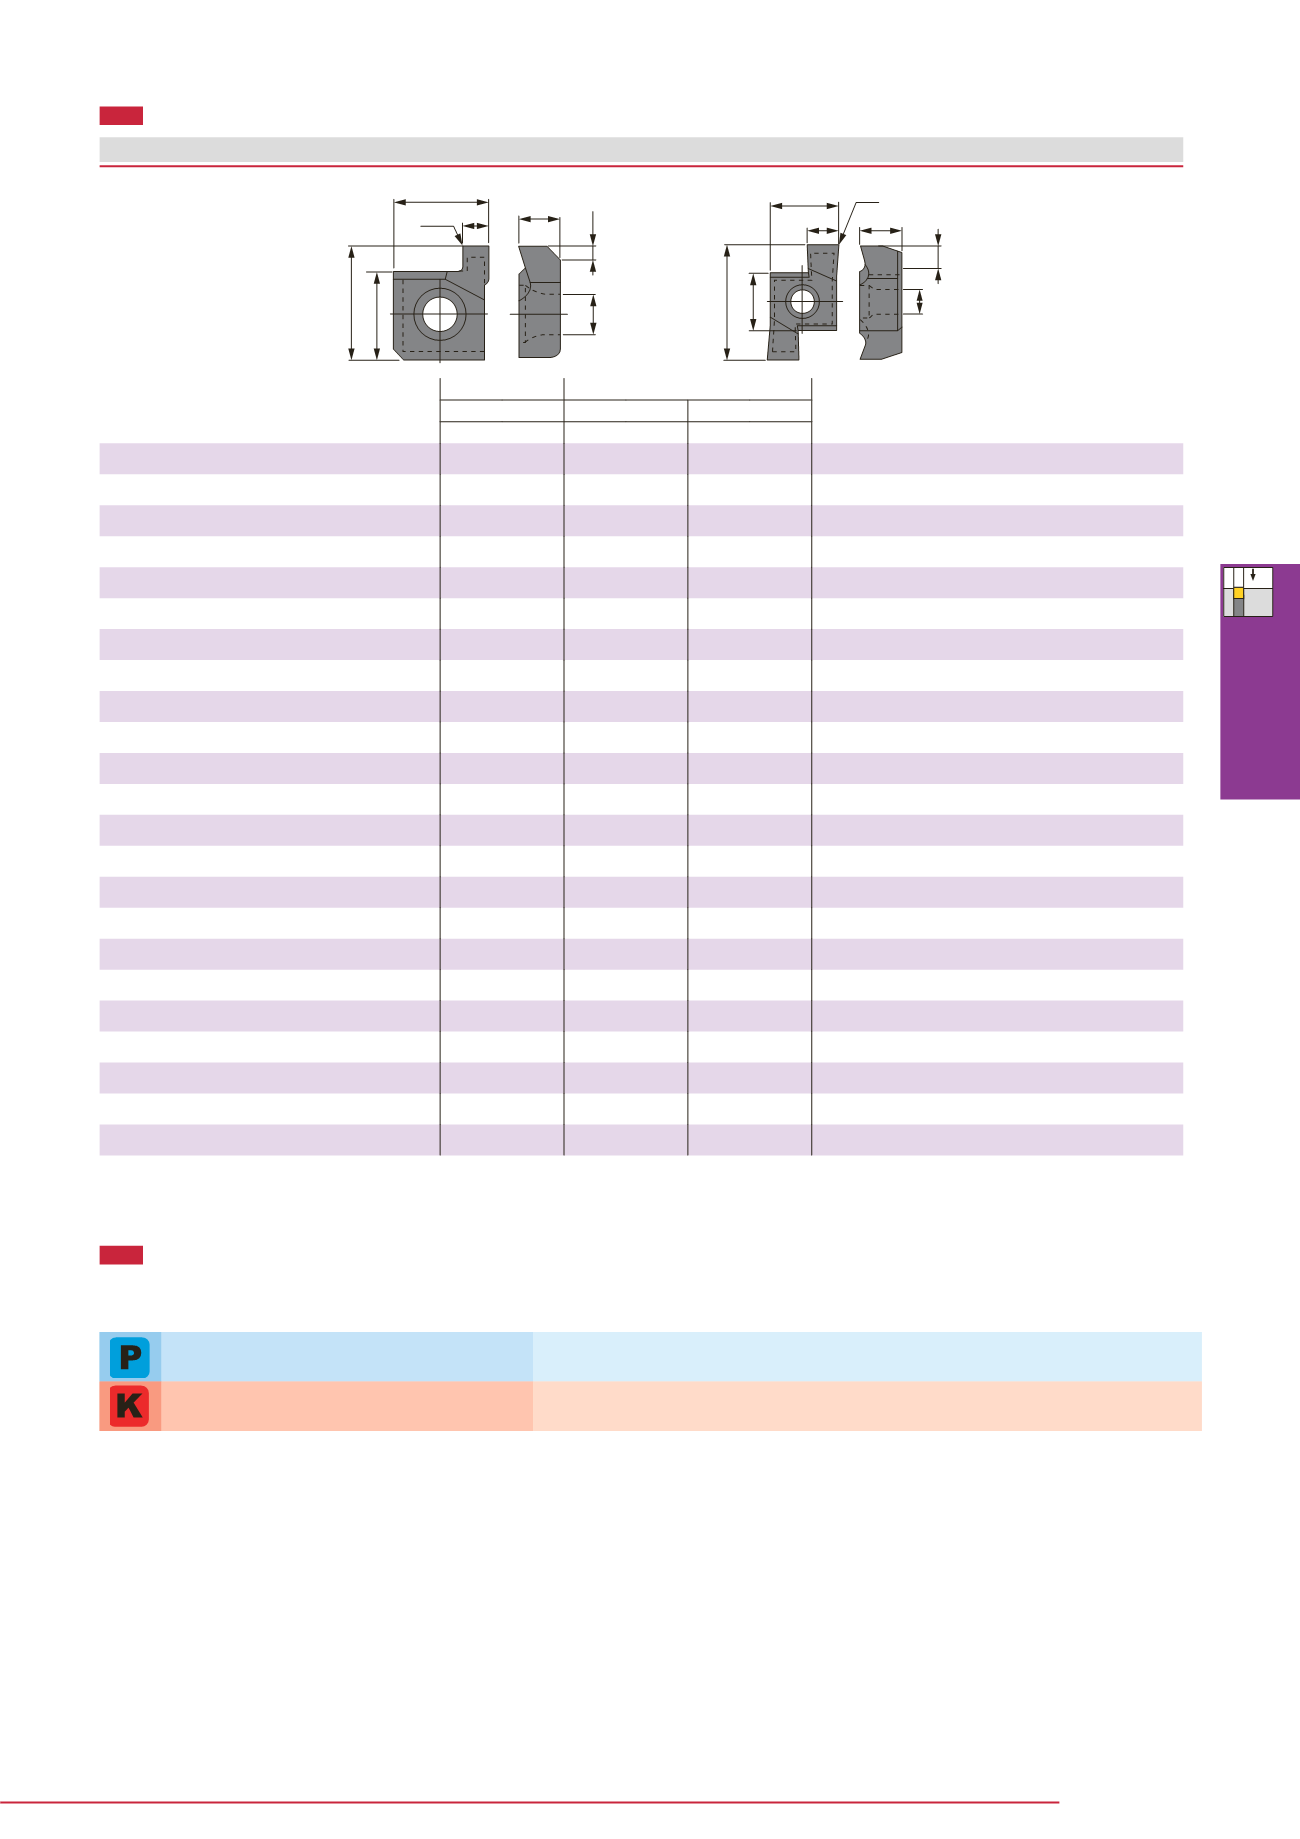
A B T øD L
G
R L R L R L
6GR/L100
1
0.2
●
●
● ●
4.76 6.44 2.34 2.3 5.56 1.5
6GR/L150
1.5
0.2
●
● ● ● ●
4.76 6.44 2.34 2.3 5.56 1.5
6GR/L200
2
0.2
●
● ● ● ●
4.76 6.44 2.34 2.3 5.56 1.5
7GR/L100
1
0.2
●
●
●
5.56 7.36 3.08 2.58 5.56 1.5
7GR/L150
1.5
0.2
●
●
●
5.56 7.36 3.08 2.58 5.56 1.5
7GR/L200
2
0.2
●
● ● ● ●
5.56 7.36 3.08 2.58 5.56 1.5
8GR/L150
1.5
0.2
●
●
●
5.56 10.16 3.87 2.58 6.15
2
8GR/L200
2
0.2
●
● ● ●
5.56 10.16 3.87 2.58 6.15
2
8GR/L250
2.5
0.2
●
● ● ● ●
5.56 10.16 3.87 2.58 6.15
2
8GR/L300
3
0.2
●
● ● ● ●
5.56 10.16 3.87 2.58 6.15
2
8GR/L350
3.5
0.2
●
●
5.56 10.16 3.87 2.58 6.15
2
9GR/L150
1.5
0.2
● ● ●
● ●
6.35 12.95 4.66 2.86 7.74
2
9GR/L200
2
0.2
● ● ● ● ● ●
6.35 12.95 4.66 2.86 7.74
3
9GR/L250
2.5
0.2
● ● ●
● ●
6.35 12.95 4.66 2.86 7.74
3
9GR/L300
3
0.2
● ● ● ● ● ●
6.35 12.95 4.66 2.86 7.74
3
9GR/L350
3.5
0.2
● ● ●
● ●
6.35 12.95 4.66 2.86 7.74
3
15GR/L200
2
0.2
●
●
●
9.2 20.8 5.1 4.8 10.8
3
15GR/L250
2.5
0.2
●
●
●
9.2 20.8 5.1 4.8 10.8
3
15GR/L300
3
0.2
●
●
● ●
9.2 20.8 5.1 4.8 10.8
3
15GR/L350
3.5
0.2
●
●
●
9.2 20.8 5.1 4.8 10.8
3
15GR/L400
4
0.2
●
●
●
9.2 20.8 5.1 4.8 10.8
4
15GR/L450
4.5
0.2
● ● ●
9.2 20.8 5.1 4.8 10.8
4
15GR/L500
5
0.2
●
●
9.2 20.8 5.1 4.8 10.8
5
● : Line-up
Right hand (R) shown.
Note:
When using a right or left hand insert, the right hand insert is used with right hand toolholder and the left hand insert is used with left hand toolholder.
A
B
L
w T
T
øD G
øD
r
ε
r
ε
A
B
L
w
G
Notes:
• Cutting conditions shown above are a guideline only.
• When grooving close to the minimum bore diameter or with long reach conditions, reduce the conditions shown above by approximately 50%.
• To help chip evacuation, use water-soluble cutting fluid. The fluid should be applied sufficiently to the cutting point.
• When using without cutting fluid, reduce both the cutting speeds and feeds shown on the above by 50% at least.
Right hand (R) shown.
* *GR/L
INSERT
ISO
40 - 150
0.05 - 0.15
60 - 200
0.05 - 0.15
Medium carbon steels (S45C)
Cast irons, Light alloys
STANDARD CUTTING CONDITIONS
Cutting speed
Vc (m/min)
Feed
f (mm/rev)
Workpiece material
Medium carbon steels
Cast ir
t alloys
Grooving Tool


