Tungaloy
B403
16ERA60
0.5 ~ 1.5
48 ~ 16
0.06
16ERG60
1.75 ~ 3
14 ~ 8
0.22
Lead
Pitch
Thread
Thread
Partial-profile
insert
Full-profile
insert
Surface turned
in preceding
operation
Finishing
stock
0.1~0.2
Crest (finished
with threading
insert)
Thread height
Trapezoidal thread
Portion to be
finished later
Crest (finished
in preceding
operation)
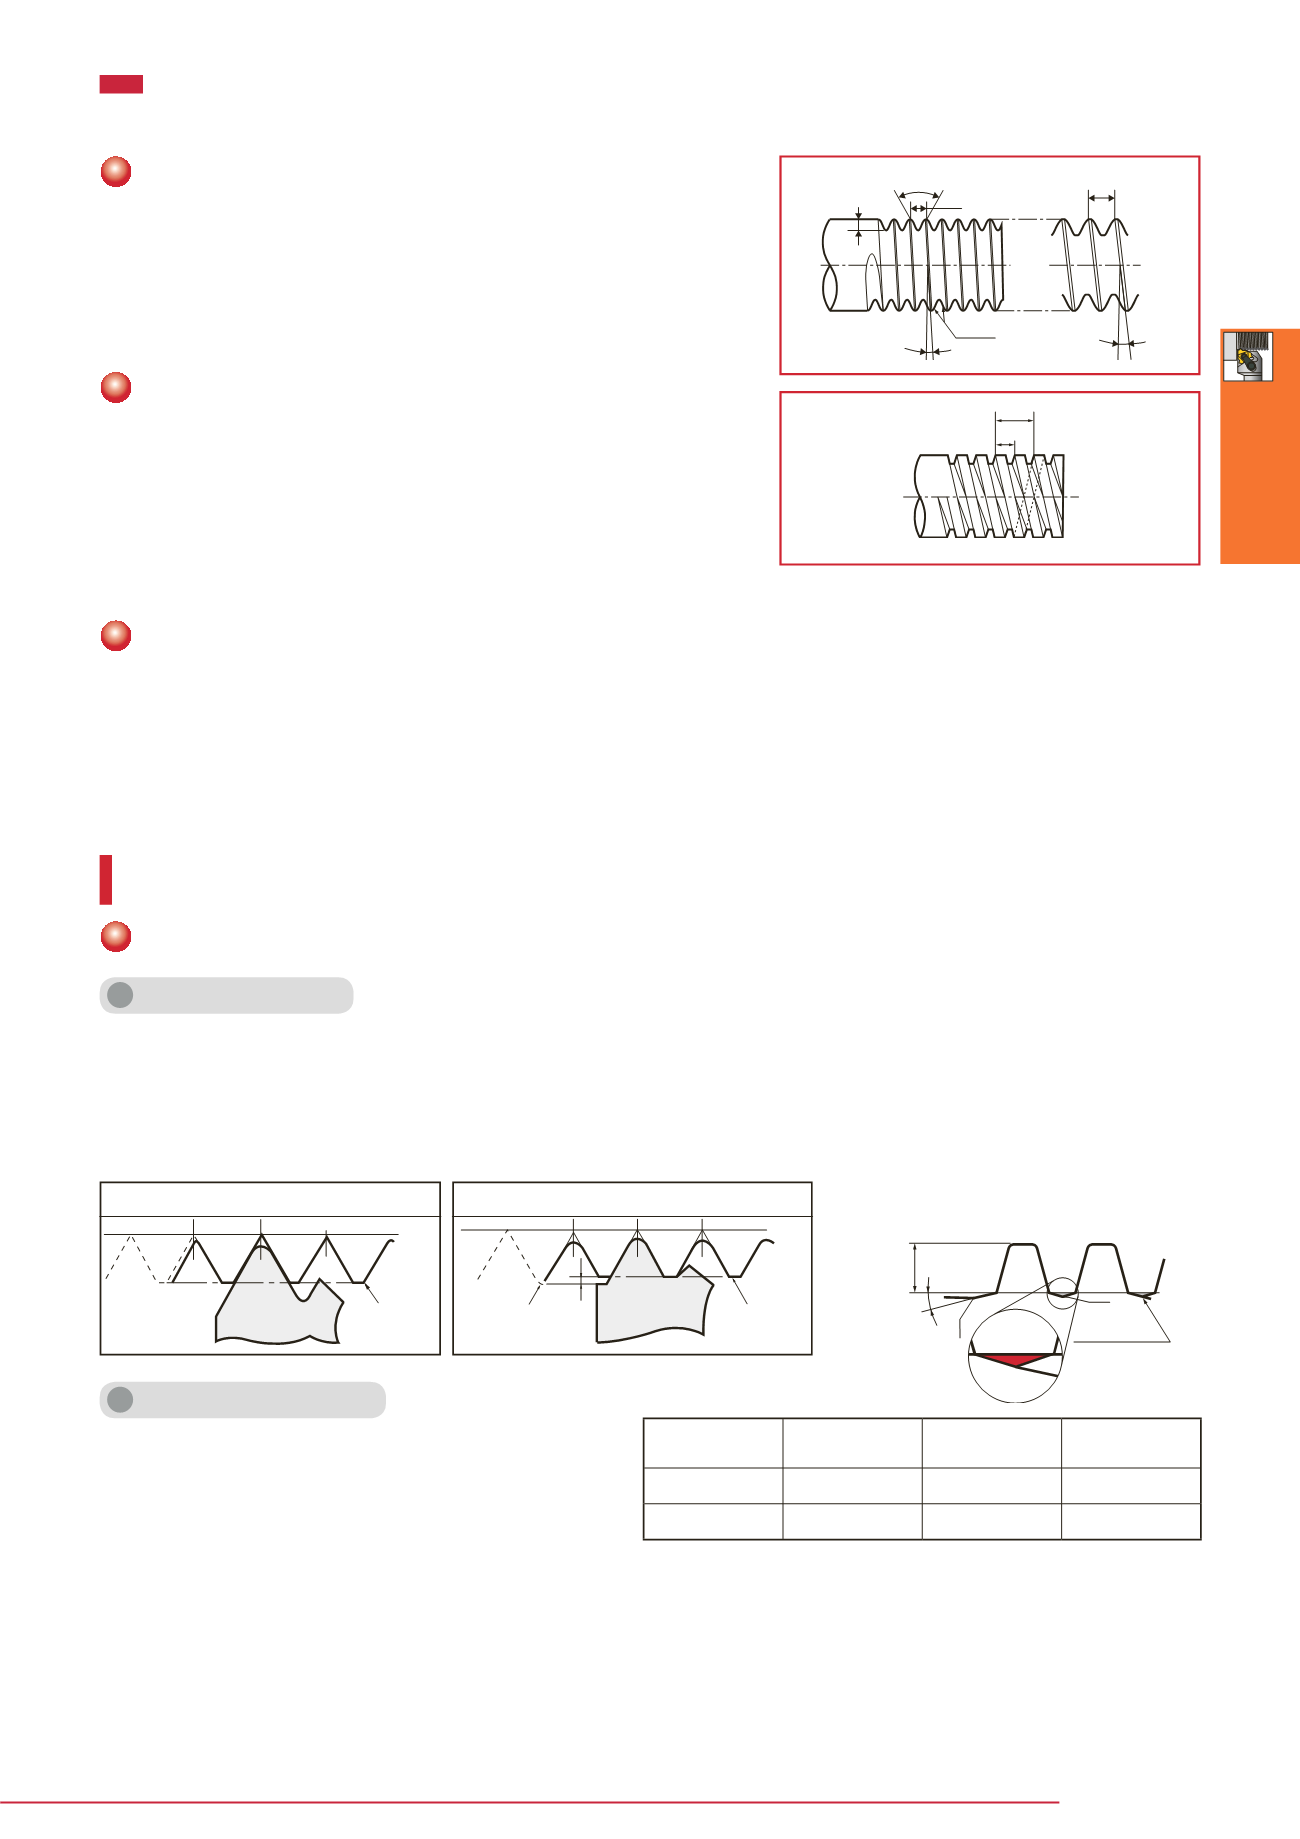
When machining trapezoidal threads:
1. Lead is the axial distance a screw advances in one rotation. In single
start screw, the lead is equal to the pitch.
2. The inclination angle of a threaded groove is called lead angle. In screws
of the same diameter, the lead angle increases as the pitch increases.
3. The side face of a completed thread groove is called flank. The distance
between the crest and the root is called thread height.
Relationship between lead, lead angle and pitch
1. The single start thread has a single groove. Two start thread or three
start thread has two grooves or three grooves respectively.
2. The pitch of multi start thread is the distance of adjoining groove.
3. When viewing the section of the multi start thread, the pitch is same as
that of the single start thread. The lead of the two or three start thread is
twice or three times the pitch. The multi start thread is mainly used for
trapezoidal threads.
Single and multi start thread
Tolerance classes of screw threads are expressed as follows:
Metric coarse external thread: 6h, 6g Metric coarse internal
thread: 5H, 6H
These classes are ranked with tolerances of thread diameter,
pitch, thread angle, etc. For fastening applications, 6H- and
6g-class (former JIS second class) threads, manufactured
by cutting or rolling, are generally used. 5H- and 4h-class
threads (former JIS first class) are generally finished by
grinding.
For example, M8-6g means metric coarse external thread of
6g tolerance class.
Tolerance class of threads
TAC threading insert
Difference between full-profile and partial-profile insert
In the full-profile insert, the major diameter of the thread is
finished by the profiled finishing edge as shown in Figure below.
Therefore, about 0.1 mm of finishing stock must be left on the
outer surface of the workpiece before threading. In trapezoidal
threads, since slants of 15º to 30º are left on the crest of the
thread as shown in Figure below, these portions must be
finished by another tool later.
Full-profile insert could produce no burr and good thread by the
profiled finishing edge.
Full-profile insert
Partial-profile insert
Full-profile insert
Partial-profile insert
Partial-profile inserts can not be used for finishing of the
crest, but can be applied to a wide range of pitches.
Corner radii of inserts are fitted to the thread of the smallest pitch.
For example
Designation Pitch (mm)
TPI
15° ~ 30°
Thread height
Thread angle
Pitch P (small) = lead
Pitch P (large)
Lead angle
(large)
Lead angle (small)
Flank
Fundamenta l s of screw threads
Two start thread
Insert radius
r
ε
(mm)
Threading Tool


