Tungaloy
B161
300
250
200
150
100
50
0
300
100
400
200
0
600
120
50
0
300
100
120
50
0
300
150
0
55
60
65
800
1200
1600
2000
400
0
300
500
800
1000
500
1000
1500
500
1000
0
1.0
2.0
3.0
4.0
1500
BX470
BX480
BX470
BX480
BX470
BX470
BX330
BX470 / BX480
Hv = 4100 ~ 4300
BX470 BX480
BX480
BX930
BX950
BX910
BX930
BX950
BX930
T5100
BXC90
BXC90
BXC90
BX910
BX910
0.5
0.4
0.3
0.2
0.1
0
(FX105)
V
c
V
c
= 120 m / min
= 250 m / min
FCD400 FCD700
Insert
PCD / CBN
Application area
Application area
T-CBN series for machining sintered metals
Ferrous Sintered metal
Valve seat
(Plunge cutting)
Valve seat
(Traverse cutting)
Cutting speed
V
c
(m/min)
SMF40X0 series material (JPMA standard)
Cutting speed
V
c
(m/min)
Cutting speed
V
c
(m/min)
Hardness of workpiece material (Hv)
Hardness of workpiece material (Hv)
Priority on burr prevention and
surface finish
Priority on wear resistance and
versatility
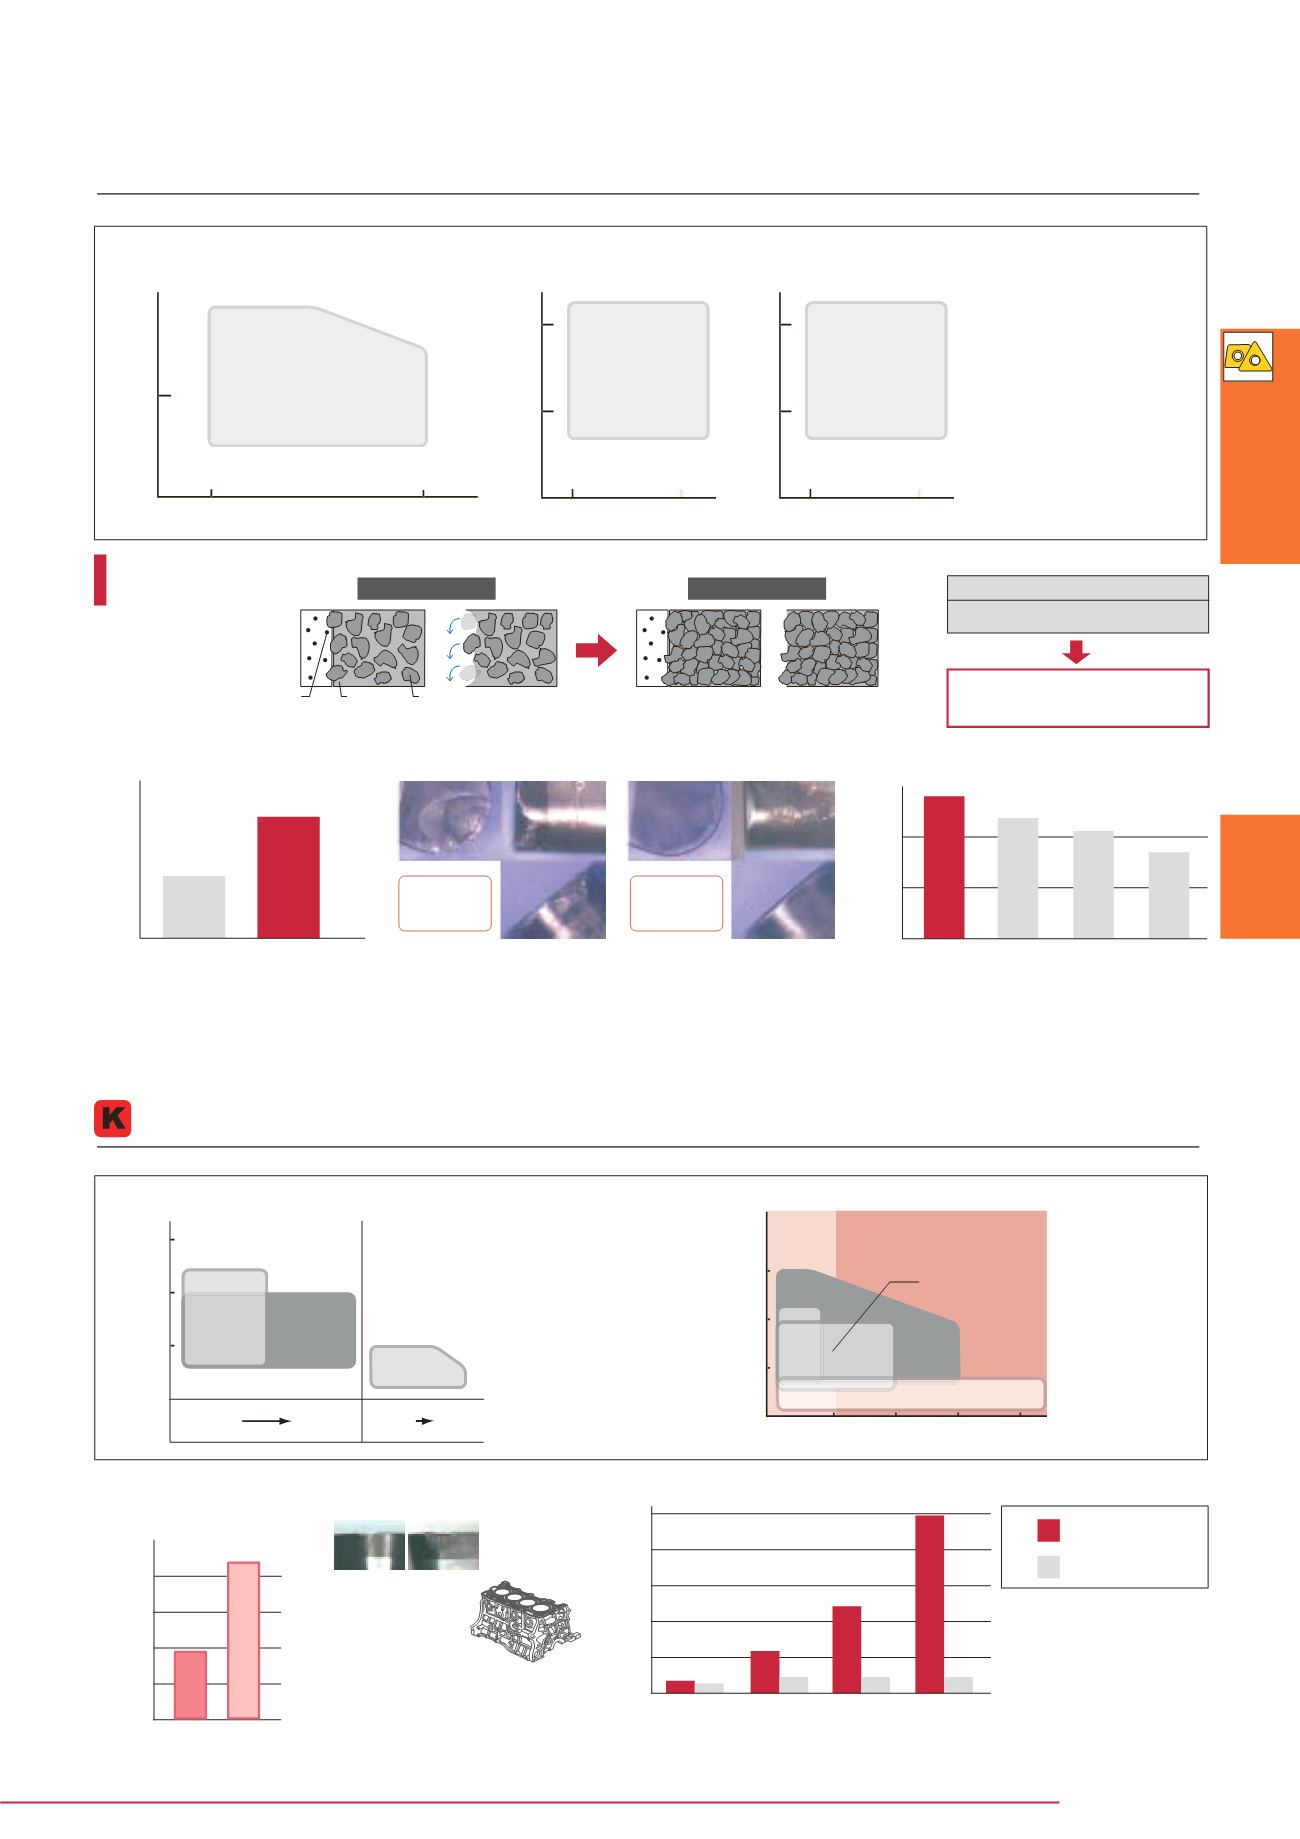
Features of
BX470 and BX480
Machining of
Sintered metal
including hard particles
Conventional grade
Hard particle
Binder
CBN grain
Binder phase are selectively worn away by hard particles.
Wear proceeds with falling-out of CBN grains,
By increasing CBN content, wear of binder layer is suppressed.
Improved wear resistance
Features of
BX470
and
BX480
CBN content: 95 vol%
The world highest CBN content as a
commercially available material.
Number of machined parts
Conventional grade
Cutting conditions
Hardness of workpiece material (HRC)
e
e
Workpiece material: Sintered metal (> HRA60)
Insert: DCMW11T308
Depth of cut: ap = 0.2 ~ 0.5 mm
Feed :
f
= 0.07 mm/rev
Coolant : Water soluble type
Interrupted cutting
BX470/BX480
Tool failure after machining
Sintered metal
BX480
(Facing of gears)
Conventional
PCBN grade
After machining
150 pcs.
BX480
After machining
300 pcs.
Cutting conditions
Workpiece material: Sintered metal (> HRA60), Nitriding,
Hard particles included
Cutting speed:
Vc
= 110 m/min
Depth of cut:
a
p = 0.15 mm
Feed:
f
= 0.1 mm/rev
Coolant : Water soluble type
Interrupted cutting
BX470
(Tool life criterion: Burr occurrence)
Number of passes
Competitor A Competitor B
Cutting conditions
Workpiece material: Ferrous Sintered metal
Cutting speed:
V
c = 100 m/min
Depth of cut:
a
p = 0.15 ~ 0.3 mm
Feed:
f
= 0.07 ~ 0.25 mm/rev
Dry and interrupted cutting
T-CBN series for machining grey and ductile cast irons
Cutting speed
V
c
(m/min)
FC and FCA (JIS)
FCD (JIS)
Continuous
Interrupted
· General purpose, first choice
grade.
· Dedicated grade for machining
ductile
Cast iron
· Suitable for interrupted
machining
· Excels in impact resistance
For machining cylinder liners
Depth of cut
(mm)
Cutting speed
V
c
(m/min)
Solid coated T-CBN grades
Area for
finishing
series
(Coated carbide)
Conventional
PCBN
grades
Ceramic grades
Area for roughing
· One-piece solid
structure
· Applicable for small
to large depths of cut
Machining of cylinder liners (Machining example of
BX910
)
Wear width after machining
120 pcs.
Max. flank wear width
VBmax (mm)
Competitor
Tool failure after machining 120 pcs.
Competitor
Cutting conditions
Workpiece material:
Cylinder liner (Spin casting)
Machining type: Finish boring
Cutting speed:
V
c = 1,000 m/min
Machine: Special purpose machine
Coolant: Wet
Tool life comparison in machining of disc brakes
Number of machine parts (pcs.)
Cutting speed:
V
c (m/min)
Ceramic
Cutting conditions
Workpiece material: Disc rotor
(JIS FC250)
Insert: SNGN 120412 BXC90
Depth of cut:
a
p = 0.7 mm
Feed:
f
= 0.35 mm/rev
Coolant: Dry
Tool life criterion:
Conditions of finished surface


