E112
Deep Hole Drill
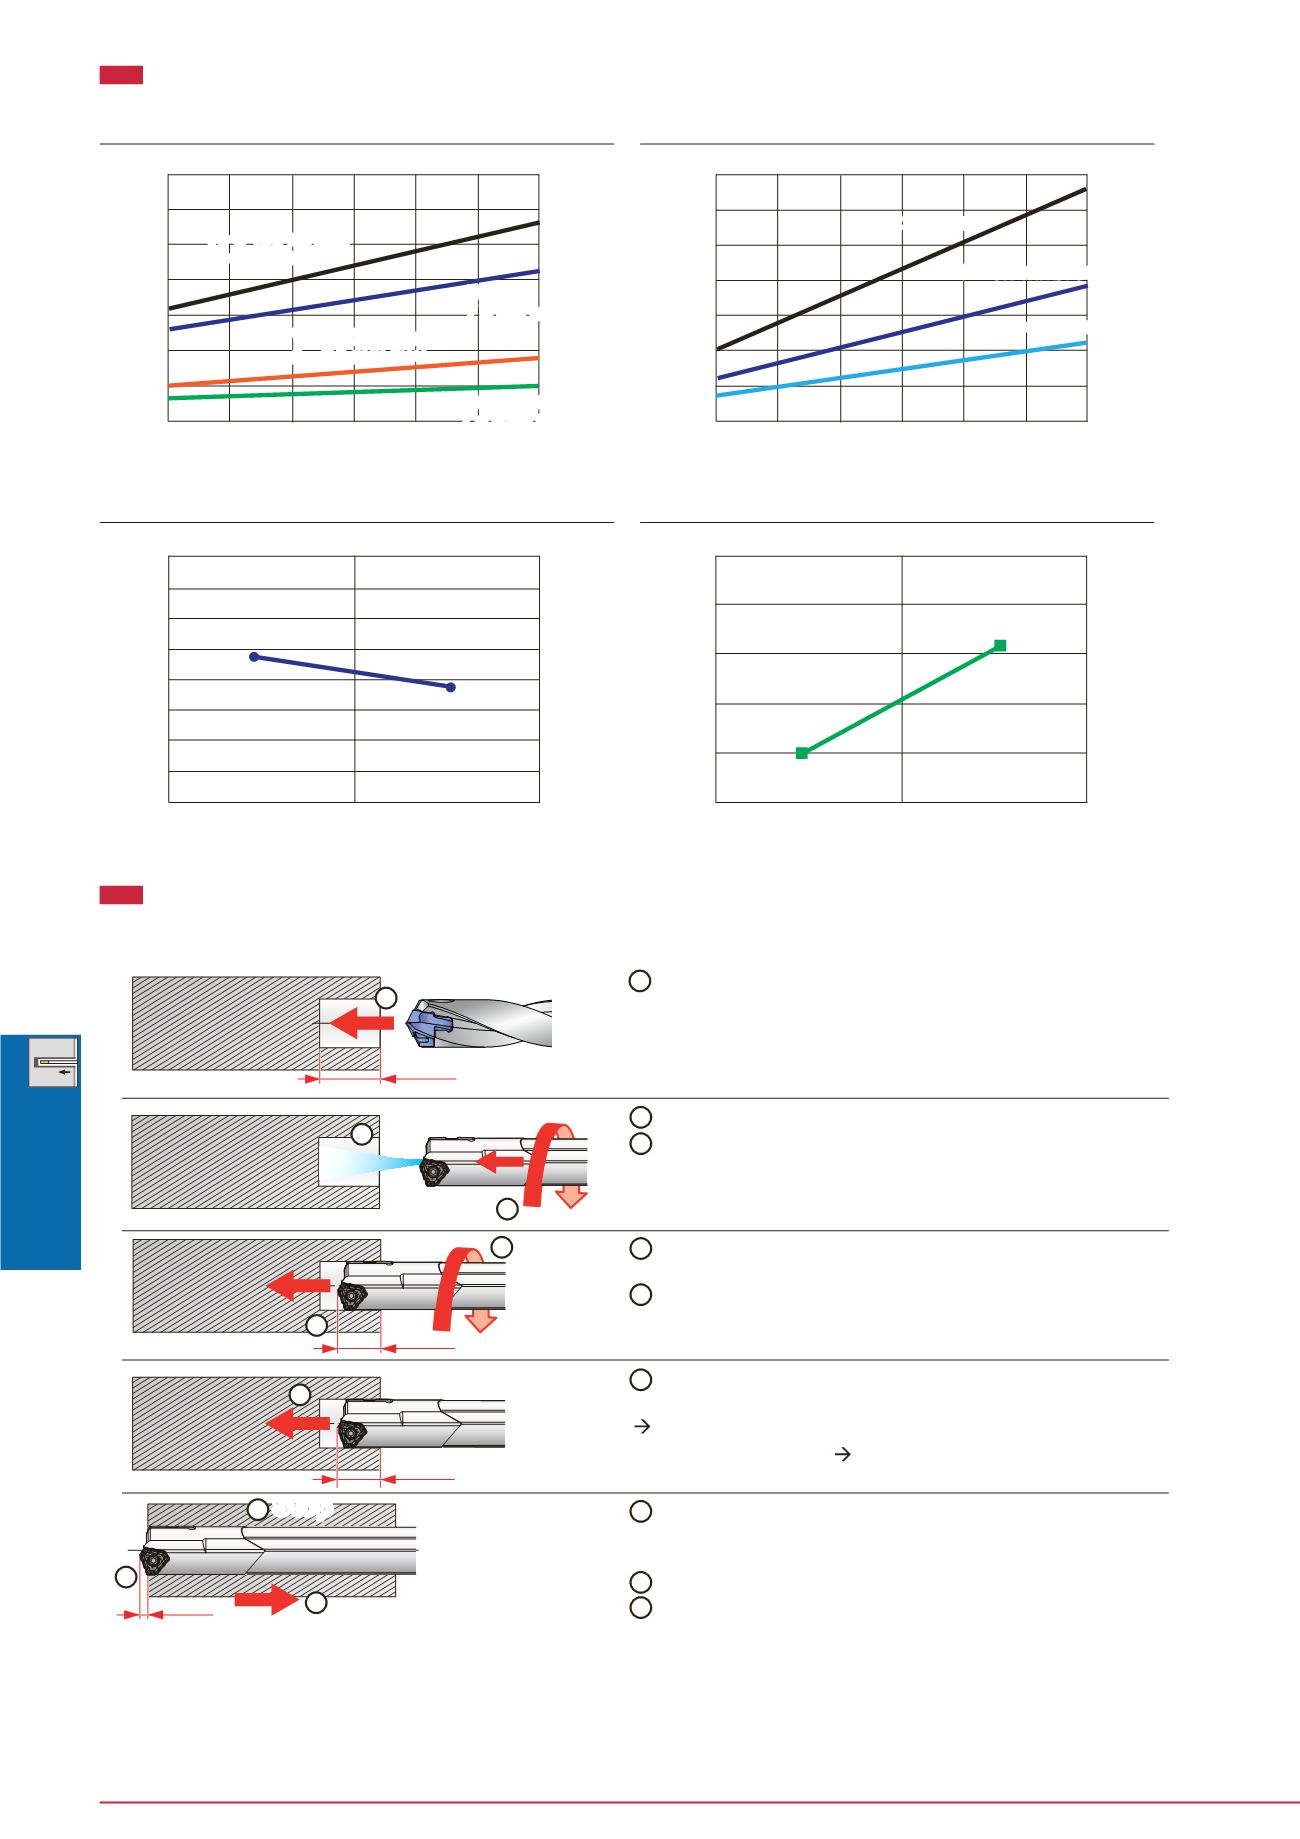
REQUIRED SPINDLE POWER AND COOLANT PRESSURE
DRILLING PROCEDURE ON MACHINING CENTERS AND LATHES
14
12
10
8
6
4
2
0
70
60
50
40
30
20
10
0
16
18
20
22
24
26
28
16
18
20
22
24
26
28
4
3.5
3
2.5
2
1.5
1
0.5
0
70
60
50
40
30
20
16
28
16
28
Vc = 100 m/min
f
= 0.2 mm/rev
Vc = 80 m/min
f
= 0.2 mm/rev
f
= 0.2 mm/rev
f
= 0.1 mm/rev
f
= 0.05 mm/rev
Vc = 50 m/min
f
= 0.1 mm/rev
Vc = 50 m/min
f
= 0.05 mm/rev
Pc (kW)
T (Nm)
P (MPa)
Q (l/min)
5 mm
10 mm
10 mm
15 mm
1
2
3
4
5
6
7
8
9
1
2
3
4
5
6
7
8
9
Net power
Coolant pressure (Recommended value)
Torque
Coolant flow rate (Recommended value)
Drill dia.: ø
D
c
(mm
)
Drill dia.: ø
D
c
(mm
)
Drill dia.: ø
D
c
(mm
)
Drill dia.: ø
D
c
(mm
)
Drill the guide hole
Hole diameter tolerance: +0.01 - +0.1 mm
Hole depth: H = 15 mm
Please use DrillMeister or TDX + EZ sleeve to make a guide hole
Caution: Do not rotate the drill at machining speed outside the hole
Start coolant
Slowly insert DeepTriDrill into the guide hole
No. of revolution:
n
= 50 - 100 min
-1
Feed speed:
V
f = 100 - 300 mm/min
At the entrance (H = 10 - 15 mm)
Feed:
f
= 80% of programmed feed
Hole depth: H
≥
15 mm
Feed:
f
= 100%
Stop the drill at 10 mm depth
Start rotating at machining speed
Start feed
For through hole
Stop the rotation and coolant
Return the drill
(Head back to the starting position)
Stop
Continue drilling until the drill head passes through the
workpiece by 5 mm
Proceed as instructed below in order to maximize the tool performance safely.


