D241
Tungaloy
Multi Function
ISO
Workpiece material
Hardness
Cutting speed
Vc (m/min)
Feed
f (mm/rev)
Low carbon steels
C45, C55, etc.
- 300 HB
40 - 80
0.04 - 0.08
High carbon steels
42CrMo4, 15Cr3, etc.
- 300 HB
30 - 50
0.04 - 0.08
Prehardened steel
PX5, NAK80, etc.
30 - 40 HRC
20 - 30
0.04 - 0.08
Stainless steels
X5CrNi18-9, X5CrNiMo17-12-2, etc.
- 200 HB
15 - 25
0.04 - 0.08
Grey cast irons
250, 300, etc.
150 - 250 HB
60 - 100
0.05 - 0.09
Ductile cast irons
400-15S, etc.
150 - 250 HB
60 - 100
0.04 - 0.08
Titanium alloys
Ti-6Al-4V, etc.
-
15 - 25
0.04 - 0.07
Heat-resistant alloys
Inconel 718, etc.
-
10 - 20
0.03 - 0.06
Hardened steel
X40CrMoV5 1, 55NiCrMoV6, etc.
40 - 50 HRC
15 - 25
0.04 - 0.07
X153CrMoV12, HS18-0-1, etc.
50 - 60 HRC
10 - 20
0.03 - 0.06
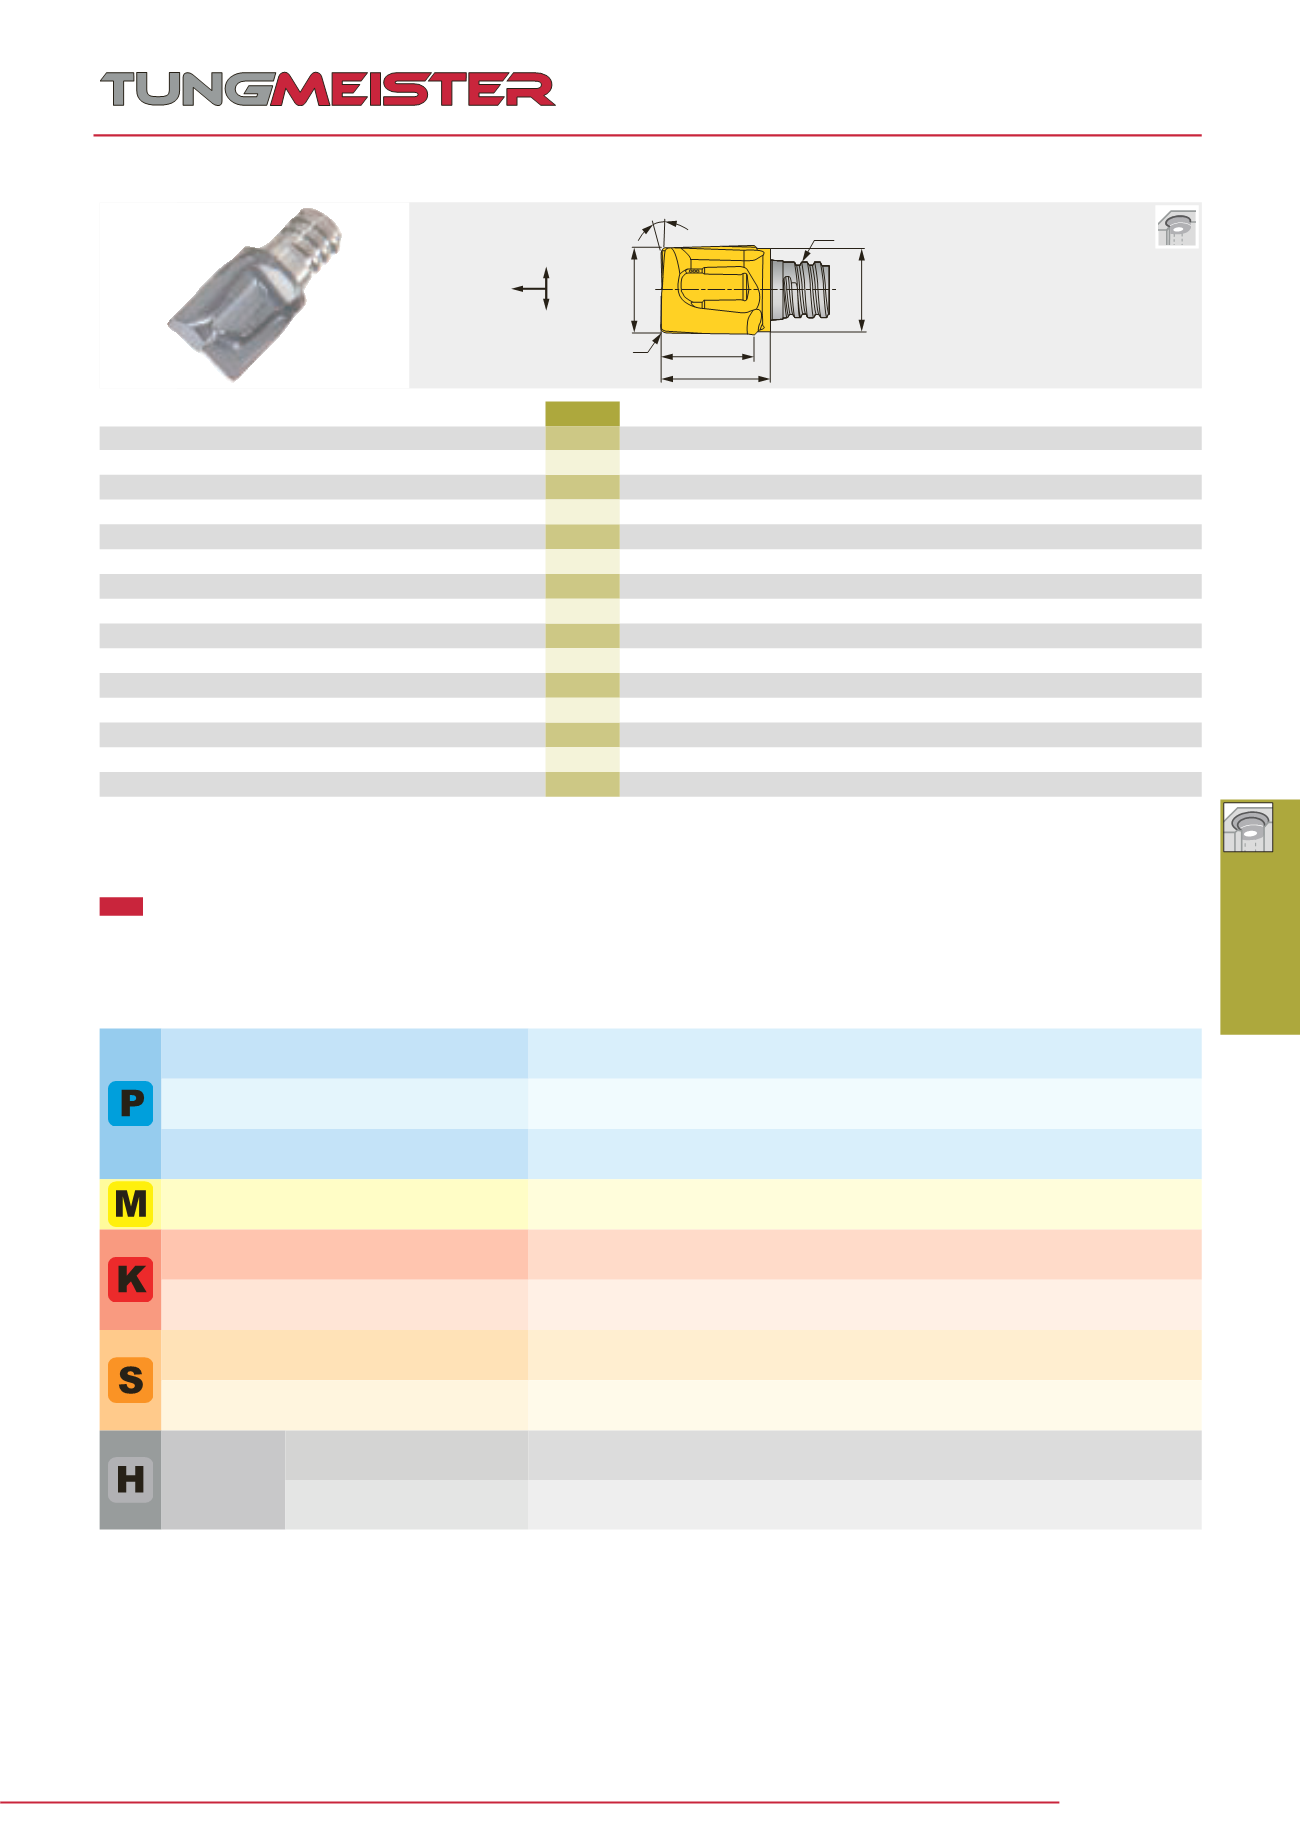
øDc
h6
S
ød
1
L
ap r
3°
ap = Max. depth of cut, S = Connection screw size
Designation
AH725 z
Helx
øD
c
ød
1
Max. ap r
S
L
Wrench Torque*
VGC078L08.0R02-02S05
l
2
10°
7.8
7.60
8.0
0.20
S05
10.0 KEYV-S05
7.0
VGC080L08.0R04-02S05
l
2
10°
8
7.60
8.0
0.40
S05
10.0 KEYV-S05
7.0
VGC080L08.0R10-02S05
l
2
10°
8
7.60
8.0
1.00
S05
10.0 KEYV-S05
7.0
VGC080L08.0R20-02S05
l
2
10°
8
7.60
8.0
2.00
S05
10.0 KEYV-S05
7.0
VGC098L09.0R03-02S06
l
2
10°
9.8
9.50
9.5
0.30
S06
12.4 KEYV-S06
10.0
VGC100L09.0R04-02S06
l
2
10°
10
9.50
9.5
0.40
S06
12.4 KEYV-S06
10.0
VGC100L09.0R10-02S06
l
2
10°
10
9.50
9.5
1.00
S06
12.4 KEYV-S06
10.0
VGC100L09.0R20-02S06
l
2
10°
10
9.50
9.5
2.00
S06
12.4 KEYV-S06
10.0
VGC117L10.0R03-02S08
l
2
10°
11.7 11.50 10.0
0.30
S08
14.2 KEYV-S08
15.0
VGC120L10.0R04-02S08
l
2
10°
12
11.50 10.0
0.40
S08
14.2 KEYV-S08
15.0
VGC120L10.0R10-02S08
l
2
10°
12
11.50 10.0
1.00
S08
14.2 KEYV-S08
15.0
VGC120L10.0R20-02S08
l
2
10°
12
11.50 10.0
2.00
S08
14.2 KEYV-S08
15.0
VGC157L15.0R03-02S10
l
2
10°
15.7 15.20 15.0
0.30
S10
19.0 KEYV-S10
28.0
VGC160L15.0R04-02S10
l
2
10°
16
15.20 15.0
0.40
S10
19.0 KEYV-S10
28.0
VGC160L15.0R08-02S10
l
2
10°
16
15.20 15.0
0.80
S10
19.0 KEYV-S10
28.0
VGC* * -02. . .
TungMeister head for counter boring
STANDARD CUTTING CONDITIONS
・
When drilling, the step feed (woodpeckering feed) operation should be applied with the depth of 0.3 - 0.5 mm per step.
・
Apply the same cutting conditions as the VEE type head when conducting shoulder milling or slotting operations.
• Can drill with step feed
*Torque: Recommended torque (Nm) for clamping.
Packing quantity = 2 pcs.
l
: Line-up
Counter boring (VGC)


