C127
Tungaloy
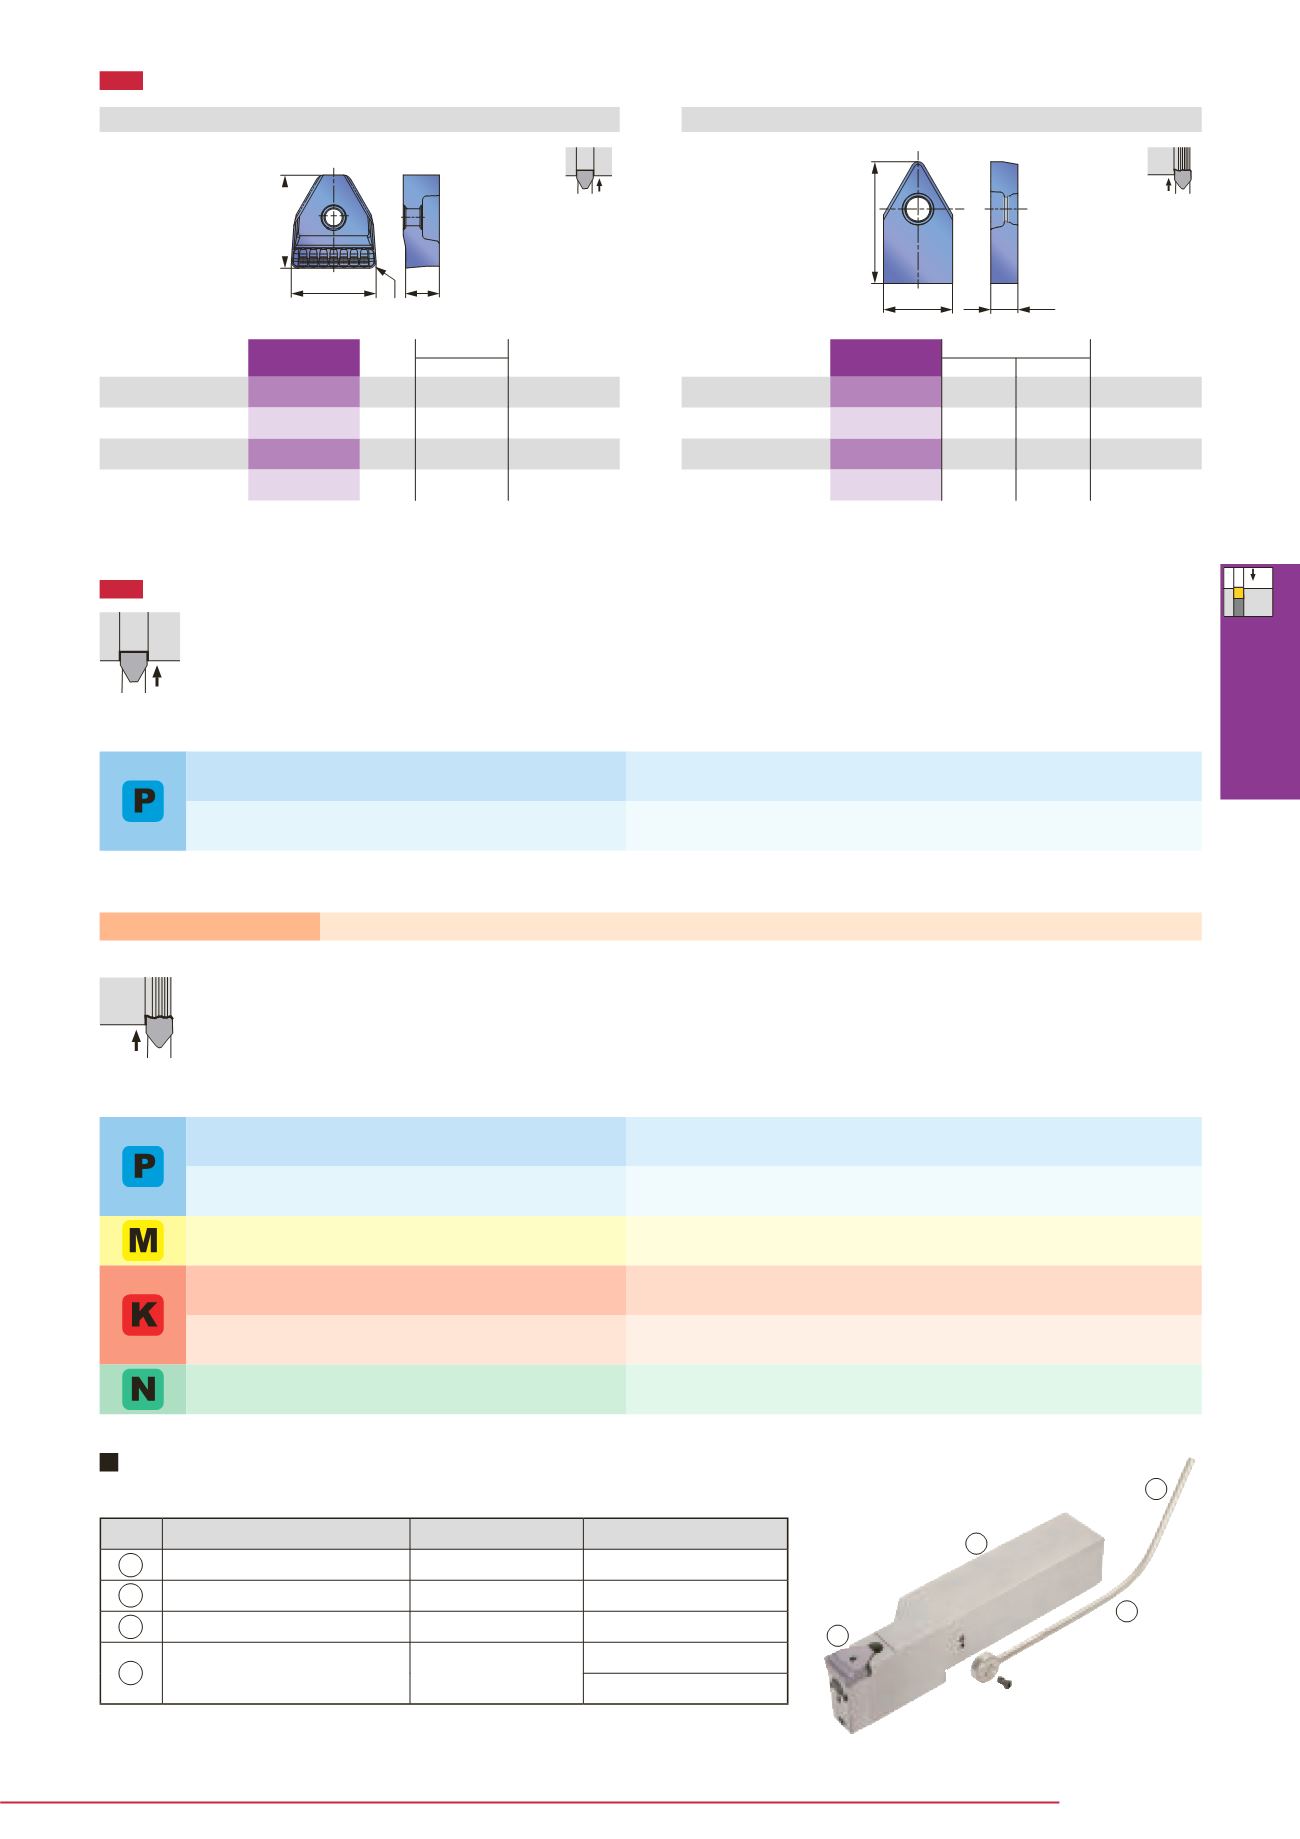
Grooving Tool
INSERT
STANDARD CUTTING CONDITIONS
ISO
(HB)
Vc (m/min)
< 300
AH725
50 - 180
< 300
UX30
50 - 120
ISO
(HB)
Vc (m/min)
< 200
UX30
50 - 150
< 300
UX30
50 - 120
< 200
UX30
50 - 120
-
TH10
50 - 150
-
TH10
50 - 120
-
TH10
100 - 500
10
15
20
25
0.2 - 0.4
0.2 - 0.4
0.3 - 0.5
0.3 - 0.5
L
s
r
ε
W*
L
W
s
W*
r
ε
L s
AH725
PSGM10-08
10
0.8
●
11
4
PSGM15-15
15
1.5
●
15
5
PSGM20-20
20
2
●
22 6.5
PSGM25-20
25
2
●
22 6.5
Designation
W ± 0.025
Uncoated
L s
UX30 TH10
PSGB10
10.2
● ●
18
4
PSGB15
15.2
● ●
20
5
PSGB20
20.2
● ●
27 6.5
PSGB25
25.2
● ●
27 6.5
Alloy steel
42CrMo4, etc.
Alloy steel
42CrMo4, etc.
●
: Line-up
●
: Line-up
*Stocked products are blanks (semi-finished) for formed inserts
*: Tolerance
W
± 0.08 (
W
= 10 mm), ± 0.1 (
W
≥ 15 mm)
Coating
Designation
1
2
4
3
For wide grooving
Blanks for wide profile grooving*
Wide grooving
Cutting speed
Grade
Hardness
Workpiece material
Feed: f (mm/rev)
PSGM type insert
Groove width: W (mm)
Forming
Cutting speed
Grade
Hardness
Steel
C45, etc.
Stainless steel
X10CrNiS18-9, etc.
Ductile cast iron
450-10S, etc.
Alloy steel
42CrMo4, etc.
Grey cast iron
250, etc.
Aluminium alloy
Si < 12%, etc.
Workpiece material
FPGR...
-
PSGM...
-
SGCU-341
-
1
2
3
4
Spare parts for internal coolant supply attachment
(Order separately)
Parts name
No.
Designation
Note
Body
G 1/8 thread
NPT 1/8 thread
Commercial items
can be used
Insert
Connector
Coolant supply attachment


