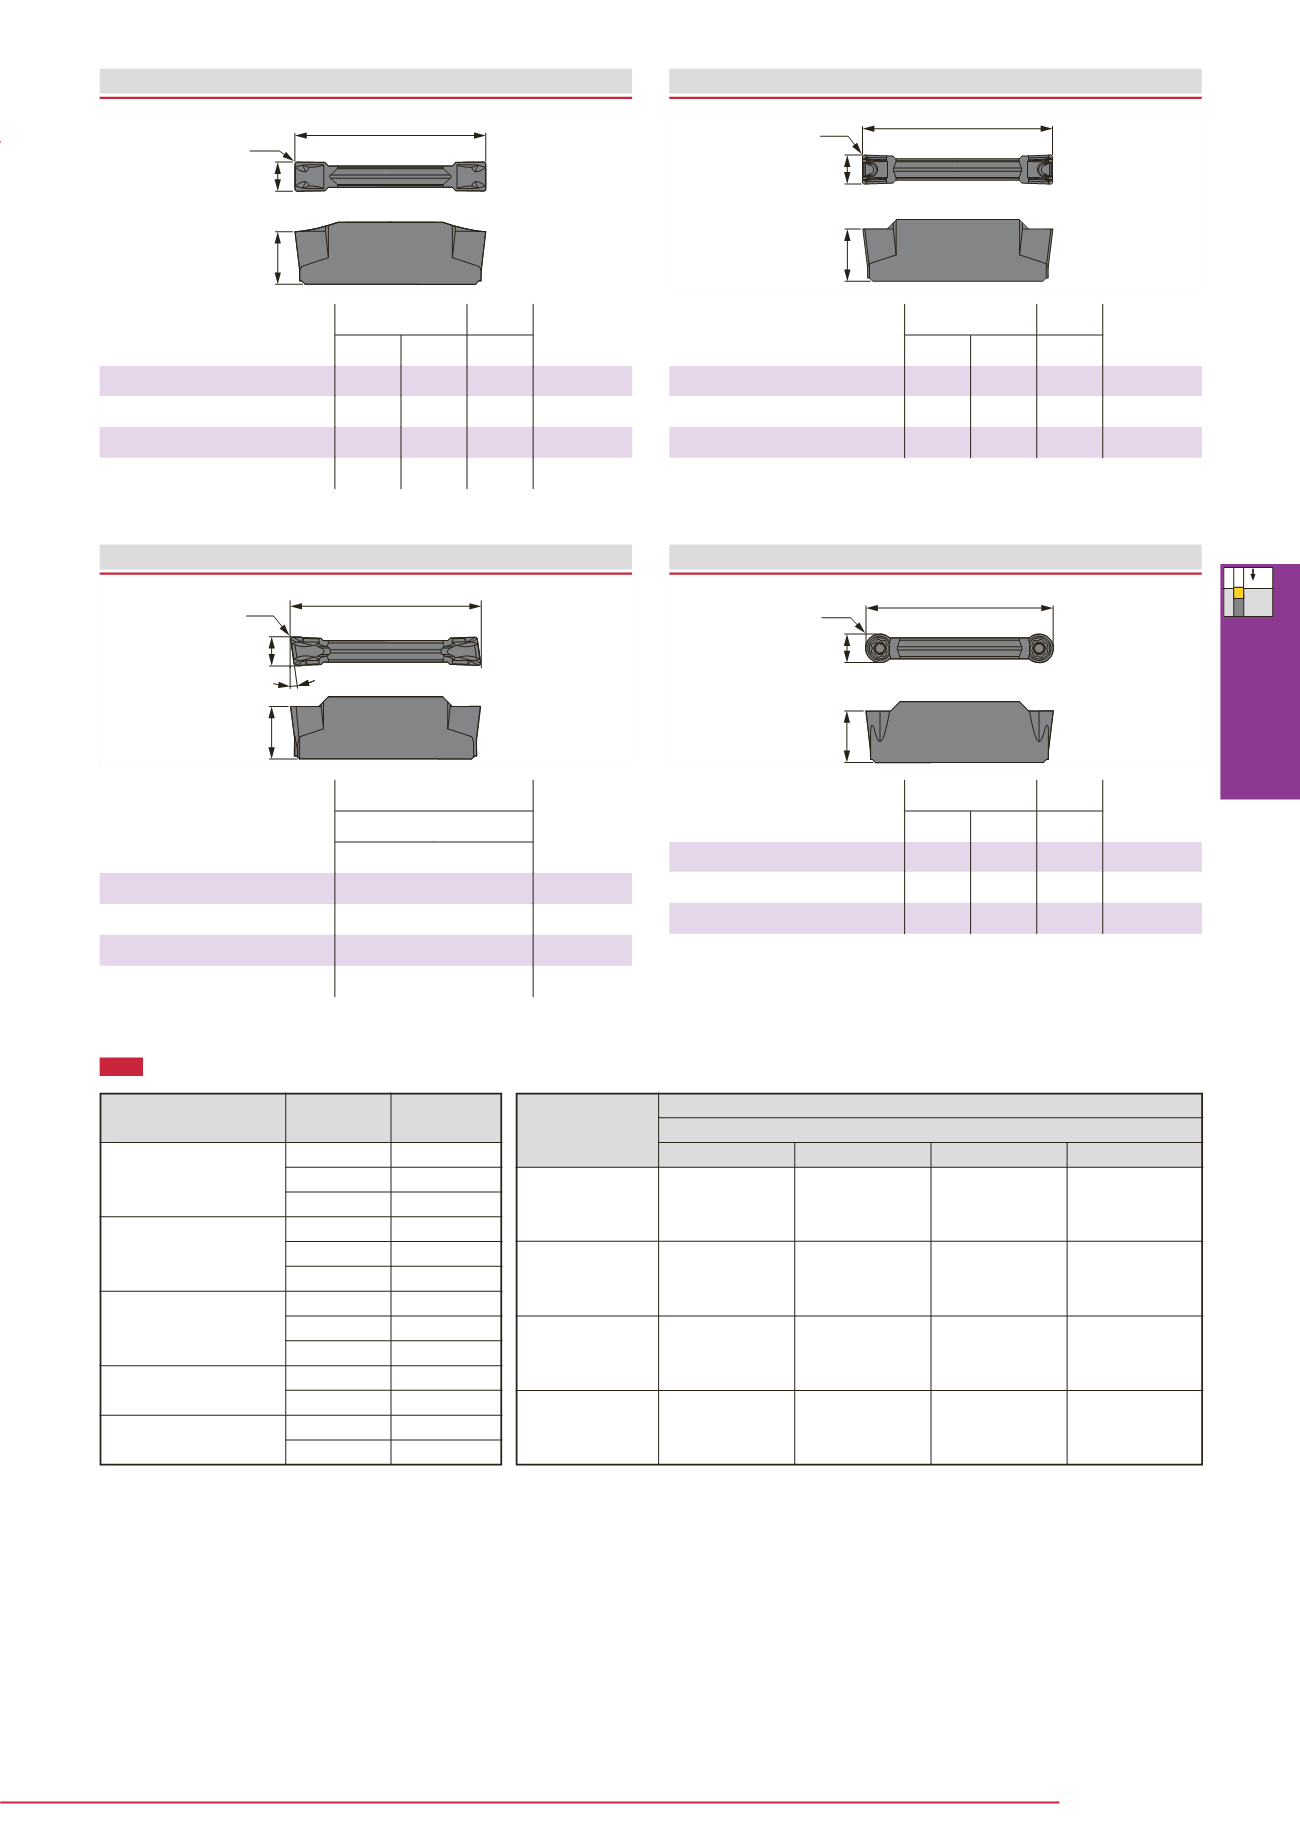
C091
Tungaloy
Grooving Tool
L
r
ε
h
w
8˚
L
r
ε
w
h
L
r
ε
h
w
L
r
ε
w
h
Designation W
+0.1
0
r
ε
Coating Cermet
L h
T9125 GH730 NS9530
WGE20
2 0.2
● ● ●
20 4.7
WGE30
3 0.2
● ● ●
20 5.5
WGE40
4 0.2
● ● ●
25 5.7
WGE50
5 0.2
● ● ●
25 5.9
Coating
Designation W
+0.1
0
r
ε
GH730
L h
R
L
WGE20R/L
2 0.2
●
●
20 4.7
WGE30R/L
3 0.2
●
●
20 5.5
WGE40R/L
4 0.2
●
●
25 5.7
WGE50R/L
5 0.2
●
●
25 5.9
Designation W
+0.1
0
r
ε
Coating Cermet
L h
T9125 GH730 NS9530
WGT30
3 0.4
● ● ●
20 5.5
WGT40
4 0.4
● ● ●
25 5.7
WGT50
5 0.4
● ● ●
25 5.9
Designation W
+0.1
0
r
ε
Coating Cermet
L h
T9125 GH730 NS9530
WGR30
3 1.5
● ● ●
20 5.5
WGR40
4 2
● ● ●
25 5.7
WGR50
5 2.5
● ●
25 5.9
T9125
NS9530
GH730
T9125
NS9530
GH730
T9125
NS9530
GH730
T9125
GH730
T9125
GH730
80 ~ 200
100 ~ 200
50 ~ 180
80 ~ 180
80 ~ 180
50 ~ 150
80 ~ 150
80 ~ 150
50 ~ 120
80 ~ 150
50 ~ 120
80 ~ 200
50 ~ 180
2
3
4
5
0.06 ~ 0.20
0.04 ~ 0.10
-
-
0.06 ~ 0.25
0.04 ~ 0.14
a
p = 0.5 ~ 1.5
f
= 0.06 ~ 0.2
a
p = 0.5 ~ 1.4
f
= 0.05 ~ 0.25
0.07 ~ 0.27
0.04 ~ 0.14
a
p = 0.5 ~ 2.0
f
= 0.06 ~ 0.25
a
p = 0.5 ~ 1.5
f
= 0.05 ~ 0.26
0.07 ~ 0.30
0.04 ~ 0.14
a
p = 0.5 ~ 2.5
f
= 0.06 ~ 0.27
a
p = 0.5 ~ 1.6
f
= 0.05 ~ 0.3
WGE
WGER/L
WGT
WGR
STANDARD CUTTING CONDITIONS
●
: Line-up
●
: Line-up
●
:
Line-up
●
:
Line-up
Right hand (R) shown.
For general parting off
and grooving
For traversing
For parting off
(with hand)
For profiling
Note: For diameter compensation values in traversing, see page
C104
.
Workpiece material
Recommended
grade
Cutting speed
v
c
(m/min)
Low carbon steels
Alloy steels
( ~ HB150)
Medium carbon steels
Alloy steels
(HB150 ~ 250)
High carbon steels
Alloy steels
(HB250 ~ )
Stainless steels
Grey and
ductile cast irons
Operation
Grooving
(WGE )
Parting off
(WGE R/L)
Traversing
(WGT )
Profiling
(WGR )
Feed:
f
(mm/rev)
Groove width:
W
(mm)


