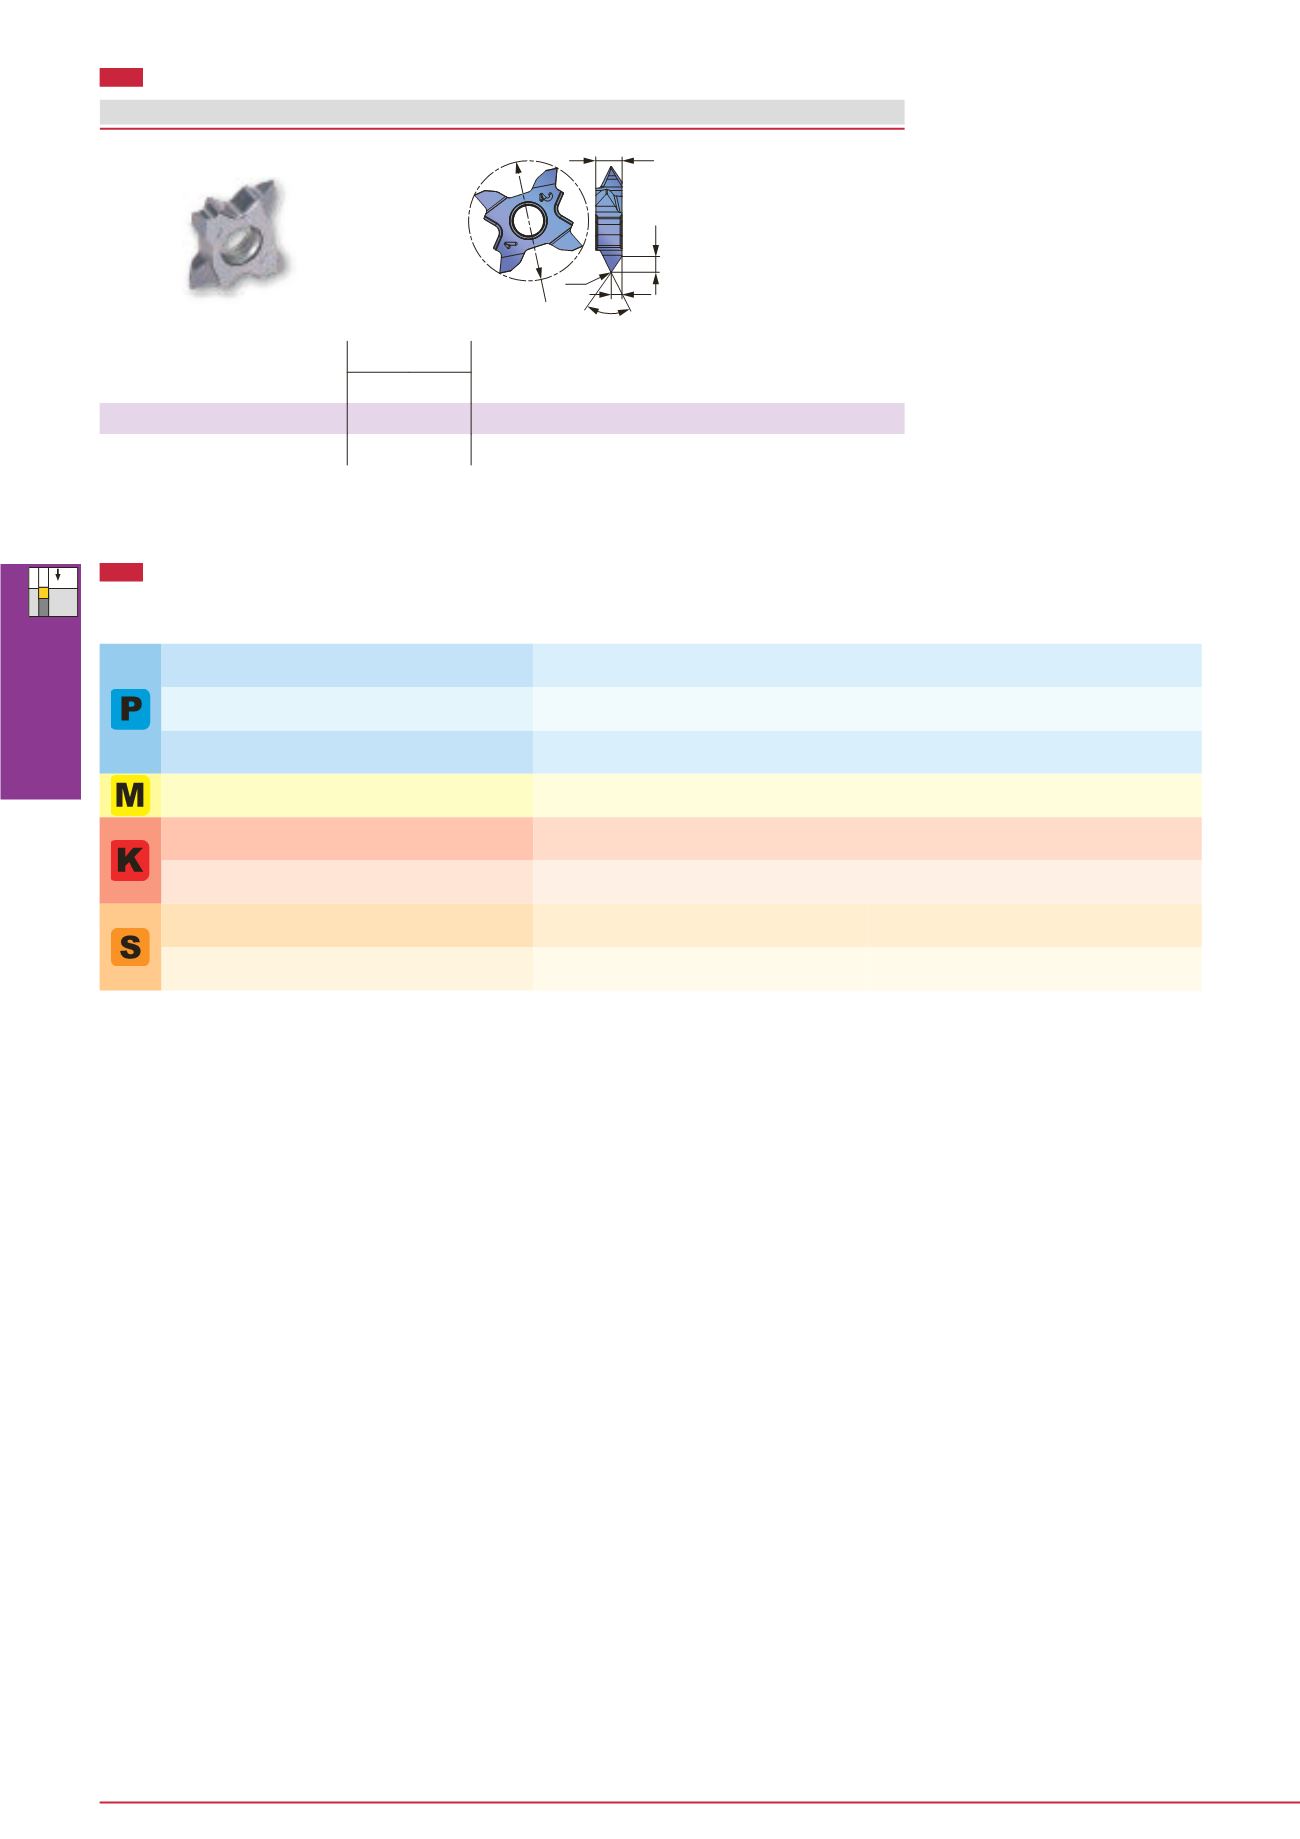
C052
TCT18R/L (For Threading)
INSERT
ISO
Workpiece material
Grade
Cutting speed
Vc (m/min)
Pitch (mm)
TPI
AH725
60 - 150
0.8 - 3
32 - 8
AH725
60 - 150
0.8 - 3
32 - 8
AH725
60 - 150
0.8 - 3
32 - 8
AH725
50 - 80
0.8 - 3
32 - 8
AH725
50 - 100
0.8 - 3
32 - 8
AH725
50 - 100
0.8 - 3
32 - 8
AH725
30 - 100
0.8 - 3
32 - 8
AH725
30 - 100
0.8 - 3
32 - 8
ød
r
ε
f
T
S
θ°
Designation
r
ε
AH725 pitch
min
pitch
max
R L
f
S θ°
T ød
TCT18R/L-60N-010
0.1
● ●
0.8
3
1.6 2.67 60
4
18
TCT18R/L-60N-020
0.2
● ●
1.5
3
1.6 2.57 60
4
18
●
:
Line-up
STANDARD CUTTING CONDITIONS
Low carbon steels
(C15, C20 etc.)
Carbon steels, Alloy steels
(C55, 42CrMoS4 etc.)
Prehardened steels
(NAK80, PX5 etc.)
Stainless steels
(X5CrNi18-9, X5CrNiMo17-12-2 etc)
Grey cast irons
(250, 300 etc.)
Ductile cast irons
(400-15, 600-3 etc.)
Titanium alloys (Ti-6AI-4V, etc.)
Superalloys (Inconel718, etc.)
Grooving Tool


